Promuove pacchetto AM01-AM12 a riferimento primario; elabora guida ADDMAN e review particle damping
Su decisione dell'utente, il pacchetto di note AM01-AM12 (basato su fonti
NIST, Loughborough University, norme e produttori) viene promosso a
riferimento tecnico primario per le rispettive famiglie di processo,
distribuito in 01 Fondamenti, 02 Processi, 14 Glossario e 10 Fonti
(AM90 - Fonti, bibliografia a 38 fonti). Le note equivalenti derivate
dal corso video freeCodeCamp/GaugeHow restano come approfondimento,
con un rimando "Vedi anche" alla nuova nota primaria.

Elabora inoltre i restanti documenti acquisiti in 00 Inbox:
- Yu et al. 2026, review su additively manufactured particle damping
  structures: scheda fonte, riassunto e nota di concetto in
  04 Progettazione.
- ADDMAN (2024), "A Guide to Designing for Additive Manufacturing"
  (guida di produttore via MinerU): scheda fonte, riassunto e tre
  note di concetto (regole dimensionali, regole/difetti per processo,
  strumenti software).
- iamrapid.com e IQS Directory: schede fonte minime per tracciabilita',
  contenuto ridondante rispetto a fonti di qualita' superiore, nessuna
  nota derivata.
- Scartati duplicati esatti gia' archiviati in 90 Allegati.

Aggiorna tutti gli indici coinvolti e sposta gli originali elaborati
da 00 Inbox a 90 Allegati.

Co-Authored-By: Claude Sonnet 5 <noreply@anthropic.com>
This commit is contained in:

 Claude Sonnet 5
+466
@@ -0,0 +1,466 @@
|
||||
## Published by: Elsevier
|
||||
|
||||
### Published by
|
||||
|
||||
[](https://www.sciencedirect.com/journal/additive-manufacturing-letters "Go to Additive Manufacturing Letters on ScienceDirect")
|
||||
|
||||
## Short reviewAdditively manufactured particle damping structures: A review of manufacturing and filling approaches, design variables and evidence comparability
|
||||
|
||||
,,,,,
|
||||
|
||||
[View **PDF**](https://www.sciencedirect.com/science/article/pii/S2772369026000642/pdfft?md5=cba1ac2d869f0e06cdfb0cbb3e12bde4&pid=1-s2.0-S2772369026000642-main.pdf)
|
||||
|
||||
[10.1016/j.addlet.2026.100417](https://doi.org/10.1016/j.addlet.2026.100417)
|
||||
|
||||
## Highlights
|
||||
|
||||
## Keywords
|
||||
|
||||
Additive manufacturing
|
||||
|
||||
;
|
||||
|
||||
Particle damping
|
||||
|
||||
;
|
||||
|
||||
Powder bed fusion
|
||||
|
||||
;
|
||||
|
||||
Structural damping
|
||||
|
||||
;
|
||||
|
||||
Vibration mitigation
|
||||
|
||||
- [Previous article in this issue](https://www.sciencedirect.com/science/article/pii/S2772369026000575)
|
||||
- [Next article in this issue](https://www.sciencedirect.com/science/article/pii/S2772369026000629)
|
||||
|
||||
## 1\. Introduction
|
||||
|
||||
Lightweight and functional additively manufactured components are increasingly used in high performance applications,, where vibration can limit structural performance, process stability or functional precision. Additional damping is attractive in such cases, but external damping devices can add mass, occupy design space or disturb the component function,. Particle damping offers a compact passive approach in which vibration energy is dissipated through relative particle motion, impacts and frictional contacts when particles have sufficient freedom to move inside a cavity,.
|
||||
|
||||
Additive manufacturing changes how this mechanism can be integrated. Internal cavities, local architecture and particle filled volumes can be designed together with the structural load path, so particle damping can be integrated within the printed component instead of added as a separate damping element,,. In additively manufactured particle damping structures (AMPDs), the damping medium may be unfused build powder retained during powder bed fusion of metals using a laser beam (PBF-LB/M) or particles introduced after fabrication. summarizes these manufacturing and filling approaches and their integration into AMPD structures. This integration has been studied, for example, for blade like parts,,, machining tools,, vibration sensitive optical holders and topology based lightweight design concepts.
|
||||
|
||||

|
||||
|
||||
Download: Download high-res image (277KB)
|
||||
|
||||
The recent AMPD literature has moved beyond isolated feasibility demonstrations. Retained powder beams,, blades, walls, gears, optical holders and tooling elements have shown measurable reductions in vibration response or increases in damping under specific test conditions. These examples indicate a broad application space, but they are spread across different manufacturing and filling approaches, powder or particle states, cavity designs, reported frequency ranges and evaluation methods.
|
||||
|
||||
This creates a comparability problem that goes beyond terminology. Similar AMPD terminology can describe retained build powder, particles introduced after fabrication or related particle damping concepts, although these approaches differ in how the damping medium is created, controlled and qualified,,,. Reported damping improvements therefore cannot be interpreted as transferable design evidence by metric value alone. The central question is whether these case specific AMPD results can be organized into transferable design guidance without merging physically different manufacturing and filling approaches.
|
||||
|
||||
Prior reviews provide complementary foundations for this question. Gagnon et al. synthesize particle-damper modeling, discrete-element calibration and experimental testing, while Ehlers et al. focus on design guidelines for laser-beam-melted retained-powder dampers. Niedermeyer et al. examine compressor-blade requirements and AMPD potential, and Zhu et al. review tuned particle dampers across mechanisms, models and applications. The present review builds on these reviews by comparing AMPD manufacturing and filling approaches, their testing methods and the way performance is reported. This comparison shows which findings can be considered together and where differences among evidence units still limit broader design guidance.
|
||||
|
||||
This review addresses that question by organizing a structured AMPD evidence table with 108 publication records around explicit boundaries between manufacturing and filling approaches. It focuses on where AMPD has been applied, which reported frequency ranges and validation evidence are available, and which cavity, powder or particle, excitation, metric and reporting variables should be considered before results are compared across evidence units. It also derives a compact reporting set that improves comparability in future AMPD work.
|
||||
|
||||
## 2\. Evidence base and classification framework
|
||||
|
||||
The synthesis uses a structured AMPD evidence table with 108 publication records (R1–R108). Scopus was used as the primary database, with complementary Web of Science searches, Google Scholar checks, and backward and forward citation tracking. The first complete search round was completed on 14 January 2026, and the final update search was conducted on 12 June 2026 using the same retrieval logic.
|
||||
|
||||
The first author conducted the keyword searches, compiled the evidence table and manually checked its publication records and classifications against the corresponding sources. Eligibility and ambiguous cases were assessed using the documented rules. Supplementary File 1 is the AMPD evidence table with the publication records, evidence-unit assignments and coded data. Supplementary File 2 is the AMPD Search and Mapping Protocol with the search and figure classification rules. The verified table was then processed using a MATLAB script to generate the figures and supporting count tables.
|
||||
|
||||
A publication record is one bibliographic row in the evidence table. For,,,, an evidence unit is the smallest independently countable contribution, such as a distinct specimen group, experimental data set or original model contribution. Potentially duplicate and overlapping publication records were checked during selection, and alternate publication records based on the same specimens, data or experiment were combined into one evidence unit. Similar authorship or topic alone was not treated as evidence of duplication. Publication records containing both unique and reused evidence were retained and flagged in the evidence table.
|
||||
|
||||
In the manuscript, the evidence table has two practical roles. It defines how the publication records are grouped by manufacturing and filling approach, and it keeps the evidence unit counts traceable. Publication records were classified as AMPD when additive manufacturing defined the damping structure and loose unfused powder or inserted particles were the damping medium. Related publication records were kept when they helped compare manufacturing and filling approaches, but they were not included in the direct retained-powder or post-filled AMPD evidence unit counts. Publication records representing reviews, providing limited detail or showing substantial overlap were retained for context when useful, but were not treated as evidence units in the figures when they mainly synthesized or reused earlier data. Each publication record was coded for process, powder and cavity descriptors, validation level, reported frequency ranges, excitation regime, response metrics, baseline information, limitations and its role in forming evidence units.
|
||||
|
||||
## 3\. Manufacturing and filling approach boundaries
|
||||
|
||||
Manufacturing and filling approach is the primary classification variable. It describes how the damping medium is created, retained or introduced in the additively manufactured structure.
|
||||
|
||||
summarizes 79 independent AMPD evidence units derived from the 108 publication records in the evidence table. These comprise 29 direct retained-powder evidence units without designed internal structures, 35 direct retained-powder evidence units with designed internal structures and 15 post-filled evidence units. The horizontal bars show the number of evidence units in each manufacturing and filling category, and the colored segments show validation level. The evidence table lists the publication records corresponding to each evidence unit.,, examine the 64 direct retained-powder evidence units.
|
||||
|
||||
Validation level was classified independently of manufacturing and filling approach. It describes the context in which a result was obtained. The five definitions are given in.
|
||||
|
||||
separates direct retained-powder AMPD into two categories according to the presence of designed internal structures. In both categories, loose or partially mobile unfused build powder remains inside sealed printed volumes and contributes to damping,,. Many use PBF-LB/M, which leaves unfused powder inside closed cavities,,. The first category contains 29 evidence units with simple sealed cavities and no designed internal structures. Examples include wall, specimen and beam evidence units,,,.
|
||||
|
||||
Table 1. Definitions of the validation levels used in this review.
|
||||
|
||||
| Level | Definition |
|
||||
| --- | --- |
|
||||
| Concept | Concept or contextual contribution without original numerical analysis or physical testing. |
|
||||
| Numerical | Modeling, simulation or optimization as the primary contribution, without new physical damping tests. |
|
||||
| Specimen | Tests on coupons, beams, blocks, dampers or other bench-scale specimens. |
|
||||
| Component | Tests on a functional component or subsystem outside its final service environment. |
|
||||
| Application | Tests under application-relevant loading or environmental conditions, or with a functional performance metric. |
|
||||
|
||||

|
||||
|
||||
Download: Download high-res image (256KB)
|
||||
|
||||

|
||||
|
||||
Download: Download high-res image (263KB)
|
||||
|
||||
Table 2. Representative comparisons within evidence units for the three AMPD categories in.
|
||||
|
||||
| Category and source | Comparison | Test and reported result | Main insight |
|
||||
| --- | --- | --- | --- |
|
||||
| Direct retained-powder, simple cavity. Westbeld et al.. | AlSi10Mg specimens with mobile or sintered powder were compared with solid references. The evidence unit included 44 cavity specimens, 18 solid specimens and four measurements per specimen. | Periodic chirp at 800 mm/s <sup>2</sup> over 50–8000 Hz. Global sintering produced no significant particle damping. Mobile powder produced a maximum relative loss factor increase of 1425%. | Powder mobility determines whether damping is activated. |
|
||||
| Direct retained-powder, internal pockets. Scott-Emuakpor et al.. | Four IN718 AMPD blades were compared with four fully fused blades. | A 0–6000 Hz sweep was followed by modal and fatigue tests. Mean quality factor decreased by about 45% and 60% at two modes, while fatigue resistance increased. | Modal response and durability should be evaluated together. |
|
||||
| Post-filled TPMS tool. Han et al.. | Four tool variants were compared with a solid tool under 16 cutting condition groups. Repeat count was not reported. | Dry turning with modes near 1299, 1303 and 5119 Hz. At 145 g fill mass, damping ratio reached 0.03 and energy dissipation efficiency reached 48%. Low fill could underperform the solid tool. | Fill state and operating condition determine the functional benefit. |
|
||||
|
||||
The second category contains 35 evidence units with designed internal structures. Examples include divided cavities, ribs, lattice cavities, resonant features and flexure guided structures,,,,,. Internal design adds a distinct design variable by changing how the powder volume is arranged within the printed structure.
|
||||
|
||||
The third category contains 15 post-filled AMPD evidence units. In this category, additive manufacturing creates the host structure, cavity, insert or module, while the particle damping medium is introduced and sealed after fabrication. Mixed retained and inserted cases are included in this category. Examples include additively manufactured toolholder and machining evidence units,, post-filled inserts or modules, and TPMS-based particle dampers,. Six related publication records outside these definitions remain as unplotted context in the evidence table,,,.
|
||||
|
||||
gives one representative comparison from each AMPD category in. The complete performance summary is provided in the evidence table.
|
||||
|
||||
The distribution of validation levels in shows where the available evidence is concentrated. Most evidence in the two direct retained-powder categories comes from specimen tests, including walls and beams,,,,. Component and application evidence is less common and appears in blades,, gears, optical holders and post-filled machining systems. Nine numerical evidence units address particle behavior, packing density control and design optimization,,,. Section therefore examines cavity placement and internal design in the 64 direct retained-powder evidence units.
|
||||
|
||||
## 4\. Direct retained-powder design variables
|
||||
|
||||
After the manufacturing and filling approach boundaries in, focuses on the direct retained-powder subset. It maps the cavity placement and cavity design classifications of 64 independent evidence units. The figure shows how retained powder volumes are positioned and shaped internally, so the following discussion can focus on design patterns instead of repeating the approach boundary.
|
||||
|
||||
Each direct retained-powder evidence unit contributes to one primary placement class and one primary cavity design class in. Detailed class definitions and precedence rules for cases with multiple applicable descriptions are provided in Supplementary File 2.
|
||||
|
||||
The placement axis describes the logic used to locate the powder volume. Mode targeted evidence units place cavities with respect to modal or operational response, including modal displacement, antinode, strain or forced response regions,,. Neutral axis evidence units use a low strain or neutral axis region as the placement reference when damping space must be balanced with stiffness or functional geometry,,. Multiple cavities describe distributed powder pockets or chamber arrays within one structure,,. Component layout covers cases where the available part geometry or functional space drives the cavity position, as in gears, instrumentation rake bodies and tooling elements,,. Cavity variation is retained as the fallback placement category when cavity position is compared together with size, number or other cavity design parameters and no single placement rule dominates,,.
|
||||
|
||||
The design axis describes the internal form of the powder containing volume. Simple cavity evidence units use closed or sealed powder volumes without designed internal structures,. Divided cavities split the powder space into chambers, pockets or partitioned regions,. Internal features add ribs, stiffening features or other obstacles inside the cavity,,. Lattice cavity evidence units combine retained powder with lattice type members or chambered lattice structures,,. Local resonator evidence units couple retained powder to a resonant substructure or absorber type design,. In this classification, multiple cavities and divided cavities are not duplicates. The first describes distributed placement of powder volumes, while the second describes subdivision of the cavity interior.
|
||||
|
||||
The plotted counts show where direct retained-powder AMPD design evidence is concentrated. Cavity variation is the largest placement category with 28 evidence units, followed by mode targeted placement with 20 evidence units. Multiple cavities and component layout each contain 6 evidence units, and neutral axis placement contains 4 evidence units. On the design axis, simple cavities and divided cavities form the largest categories with 29 and 19 evidence units, followed by internal features with 7 evidence units. Local resonators appear in 5 evidence units and lattice cavities in 4 evidence units. The most populated cells are cavity variation with simple cavities, mode targeted placement with simple cavities and mode targeted placement with divided cavities. This pattern shows that the direct retained-powder literature is weighted toward modal placement, cavity design comparisons and simple or partitioned cavity designs.
|
||||
|
||||
This classification supports a more specific design interpretation. Cavity placement can matter as much as cavity volume because retained powder must move relative to the cavity walls under the active response,,. At the same time, cavity design strategy changes both powder motion and structural response, because partitions, ribs, lattice members and resonant substructures can modify particle travel distance, contact conditions, local stiffness and coupling to a target mode,,,. Their benefit is conditional because the same feature that redirects particles can also reduce clearance, restrict powder mobility or change the load carrying geometry,,. Geometry descriptors should therefore be read together with powder state and baseline definition. Cavity ratio, cavity volume fraction, unfused powder volume percentage, particle filling ratio and packing density describe related but different quantities, and they should not be treated as interchangeable damping predictors,,,.
|
||||
|
||||
This design classification provides the context for comparing reported frequency ranges, excitation regimes and validation metrics in Section.
|
||||
|
||||
## 5\. Validation evidence and metric comparability
|
||||
|
||||
After the manufacturing and filling approach boundaries in and the direct retained-powder design variables in, the next comparison is how these designs have been tested. maps the frequency information reported for 64 direct retained-powder AMPD evidence units. It separates impact-hammer FRF, impulse or free decay, shock or transient loading, harmonic or swept-sine testing, random or broadband testing, mixed or operational testing and numerical or modeling-only work as primary evaluation methods. Detailed method definitions and assignment rules are provided in Supplementary File 2, while the primary and secondary method classifications for each evidence unit are listed in Supplementary File 1.
|
||||
|
||||
The 64 evidence units comprise 26 harmonic or swept-sine, 15 impact-hammer FRF, 9 numerical or modeling-only, 7 mixed or operational, 5 impulse or free-decay and 2 shock or transient evaluations. None uses random or broadband testing as its primary method, although broadband input appears as a secondary method in some mixed or operational evidence units.
|
||||
|
||||

|
||||
|
||||
Download: Download high-res image (1MB)
|
||||
|
||||
Of the 64 evidence units, 18 report continuous ranges, 6 discrete point sets, 28 modal-frequency sets and 8 local bands. Four lack a verifiable numeric frequency or mode and remain listed as no numeric beside their source labels. Filled circles mark continuous-range endpoints and discrete points, filled diamonds mark modal frequencies and filled squares mark local-band endpoints. Each source mark uses the color assigned to its validation level. Ranges beginning at 0 Hz are shown from the 1-Hz limit of the logarithmic axis.
|
||||
|
||||
The frequency information in becomes meaningful when the input method and response metric are read together. Impact-hammer FRF tests identify modes and describe damping or response amplitude around resonance. Impulse or free-decay tests obtain modal damping from the response after release or impulse. Shock or transient tests quantify the decay after a short input through measures such as quality factor and damping ratio. Harmonic or swept-sine tests resolve changes in resonance, loss metrics and dissipated energy across frequency and amplitude.
|
||||
|
||||
Mixed or operational tests connect the vibration response to functional measures such as stress, fatigue or transmissibility,. Numerical evidence units examine particle motion and particle–wall interactions, with experimental calibration determining their design relevance. The absence of random or broadband excitation as a primary method leaves service representative broadband loading as a validation gap.
|
||||
|
||||
These metrics describe different parts of the structural response. Interpreting a lower FRF peak requires checking mass, stiffness and resonance shift together with damping. Comparison across evidence units therefore requires the input type and amplitude, frequency or mode, response location, metric definition and baseline to be reported together. A useful next step is to test several modes with more than one input method on the same specimens and baseline. This would connect modal damping, FRF amplitude, energy loss and functional response under controlled conditions.
|
||||
|
||||
Excitation amplitude is a design variable in AMPD because the particle motion changes as the input increases. At low input, the powder can move with the cavity walls and dissipate little energy. As relative motion develops, sliding and collisions increase dissipation. Further increases can produce saturation, softening, hysteresis or jump behavior,,. Characterizing this working range requires damping measurements at several specified amplitudes. Frequency sweeps should therefore be repeated at controlled amplitudes and in both sweep directions, with response amplitude and activation or saturation thresholds reported. The resulting frequency and amplitude maps would show whether a design remains effective across its intended load range.
|
||||
|
||||
PBF-LB/M feedstock powder introduces a second design dimension. Micrometer scale powder has a greater relative influence of attractive and surface forces than the millimeter scale particles used in many classical dampers,. Its mobility also depends on material, particle size distribution, surface condition, packing density and compaction,,,. The same nominal cavity geometry can therefore show different damping when the powder material or state changes. Controlled comparisons across materials should hold cavity geometry, structural baseline and excitation constant while varying powder material, size distribution, packing and compaction. maps testing conditions and validation levels, while the evidence table records the particle descriptors and powder state needed for this comparison.
|
||||
|
||||

|
||||
|
||||
Download: Download high-res image (349KB)
|
||||
|
||||
Table 3. Baseline comparisons for three recurring research purposes in the reviewed AMPD literature.
|
||||
|
||||
| Purpose | Suitable comparison | Supported interpretation |
|
||||
| --- | --- | --- |
|
||||
| Mechanism attribution | Compare retained-powder specimens with corresponding empty cavity, solid or altered powder state specimens. Keep the boundary condition and excitation consistent, and report changes in mass, stiffness, natural frequency and mode shape,,. | Whether the measured response is consistent with particle mobility and dissipation at the tested mode, amplitude and powder state. |
|
||||
| Design trade-off under stated constraints | Compare feasible designs under the same functional requirements and report the relevant mass, stiffness, strength, manufacturing and frequency constraints,,. | The vibration benefit obtained within the tested design constraints, including damping and changes in resonance. |
|
||||
| Functional performance and durability | Compare the AMPD design with a functional reference under the same mounting, loading and environmental conditions, and include repeated specimens or cyclic states where available,,. | The functional benefit and its repeatability or stability over the tested conditions and duration. |
|
||||
|
||||
Taken together, the 64 evidence units comprise 41 specimen evidence units, 9 numerical evidence units, 7 component evidence units and 7 application evidence units. The distribution is concentrated at specimen level, while component and application evidence each account for 7 evidence units.
|
||||
|
||||
The testing and frequency evidence in must be interpreted together with the reported response metric and baseline because a reduction in vibration response can arise from particle dissipation, changes in mass or stiffness, a shift in resonance, or a combination of these effects. The baseline must therefore be chosen according to the question being tested. summarizes the baseline implications derived from analysis through three recurring research purposes: identifying the contribution of particle mobility, evaluating vibration performance under stated design constraints, and testing functional performance and durability. For each purpose, the table links a suitable comparison with the conclusion that the available evidence can support. The reporting information needed for these comparisons is examined in Section.
|
||||
|
||||
## 6\. Reporting completeness and comparability needs
|
||||
|
||||
Comparisons across AMPD evidence units become difficult when important experimental information is incomplete or reported in different ways. therefore examines the reporting completeness of 64 direct retained-powder AMPD evidence units. The fields cover the information needed to describe their designs, tests and validation results, with detailed definitions in Supplementary File 2 and the corresponding evidence in Supplementary File 1. Each field is classified as Reported, Partly reported, Not reported or Not applicable. The applicable denominator includes the first three statuses, while Not applicable is shown separately.
|
||||
|
||||
shows that basic descriptions of AMPD design and testing are available in most evidence units. AM process and material and boundary condition each reach the Reported threshold in 60 evidence units. Cavity metric reaches it in 59 evidence units, geometry in 58 evidence units and excitation level in 50 evidence units. The largest gaps are concentrated in particle fill ratio, packing density or powder state, repeatability or uncertainty, and lifecycle or degradation. The following paragraphs discuss why these four areas remain incomplete and how they affect comparison and reproducibility.
|
||||
|
||||
Particle fill ratio and packing density describe two linked controls of retained powder motion. Fill ratio sets the powder amount relative to cavity volume, while packing density and powder state determine how that material is arranged and constrained. In, particle fill ratio is Reported in 5 evidence units, Partly reported in 56 and Not reported in 3. Packing density or powder state is Reported in 38 evidence units, Partly reported in 25 and Not reported in 1. The distinction is mechanically important. Fill ratio governs the overall free space available for particle motion. Packing density, compaction and cohesion govern the internal contact network, frictional sliding and the excitation threshold required to mobilize the powder,,,. Identical cavity geometry and nominal fill ratio can therefore produce different damping after processing or repeated loading changes the powder state. Future AMPD work should report a clearly defined volume or mass basis together with the measured powder state before and after testing, allowing particle activation and energy dissipation to be linked to a reproducible internal condition.
|
||||
|
||||
Repeatability or uncertainty is Reported in 33 evidence units, Partly reported in 28, Not reported in 1 and Not applicable in 2. The large Partly reported group mainly contains specimen or repeat counts without a measure of variation. Repeated measurements on one specimen characterize variation in the test and response. Measurements across specimens and builds capture variation introduced by manufacturing and the retained powder state. Local packing, compaction and powder redistribution can change the damping response under nominally identical geometry and loading,,. Repeated runs can provide a precise mean for one specimen. Reproducibility across specimens and builds requires separate replication. Future AMPD work should distinguish repeated runs, specimens and builds and report dispersion or uncertainty at each level together with the corresponding powder state.
|
||||
|
||||
Table 4. Proposed minimum AMPD reporting checklist for future work.
|
||||
|
||||
| Reporting item | Minimum information | Risk if omitted |
|
||||
| --- | --- | --- |
|
||||
| Approach identity | Identify retained build powder, post-filled particles or another related approach. Report sealing and powder removal where relevant. | Routes may be compared although their damping media are created and controlled differently. |
|
||||
| Cavity and structure | Report cavity placement, wall thickness, internal design, mass change and geometry relevant to stiffness. | Geometry or stiffness effects may be attributed to powder damping. |
|
||||
| Powder or particle state | Report particle material and size, retained powder condition, packing density or fill measure, and heat treatment or compaction history. | Fill ratio, packing density and powder state may be treated as equivalent. |
|
||||
| Test condition | Report input type and amplitude, frequency range or test points, mounting and signal chain. | Results may be compared across different particle activation conditions. |
|
||||
| Baseline and metric | Define the reference and report AMPD and reference mass, powder or particle mass where available, natural-frequency shift, stiffness change or a justified proxy, and the response or functional metric. | Mass, stiffness and detuning may confound interpretation of the damping benefit. |
|
||||
| Repeatability and service | Report specimen and repeat counts, uncertainty, repeated excitation effects, degradation and powder state after testing. | Initial performance may be interpreted as repeatable or durable. |
|
||||
|
||||
Lifecycle or degradation is Reported in 25 evidence units, Partly reported in 2, Not reported in 34 and Not applicable in 3, making it the largest Not reported group in. Most evidence units therefore characterize AMPD performance in its initial state, leaving stability under mechanical and thermal history unresolved. Retained powder damping is state dependent. Repeated resonance passes and high strain dwell can compact, redistribute or locally fuse the powder,,. Heat treatment can form sintered contacts and reduce particle mobility, while later excitation can fragment some contacts and change the response again. Degradation can therefore involve transitions between loose, compacted, trapped and sintered powder states, with corresponding changes in activation and energy dissipation,. Application validation should track damping against load cycles, amplitude and thermal history and document the powder state before and after testing. This would show whether the damping response remains stable, changes gradually or undergoes an irreversible loss.
|
||||
|
||||
These reporting gaps motivate the AMPD reporting checklist in. The checklist combines the weak reporting fields in with the manufacturing and filling approach, cavity design and validation variables discussed above. It lists the minimum information that future AMPD work should report before results are compared across manufacturing and filling approaches, cavity designs, test conditions and baselines.
|
||||
|
||||
## 7\. Design implications
|
||||
|
||||
This section discusses the design implications of the reviewed evidence and priorities for future AMPD research.
|
||||
|
||||
The first design implication from the manufacturing and filling categories in and is that the AMPD route should be selected according to the design variable that must remain controllable in the intended application. Direct retained-powder designs without designed internal structures provide control through cavity placement and geometry, designed internal structures add coupled control through internal design, and post-filled designs provide independent control of particle morphology and fill ratio after fabrication,,,,,,,. This route decision should precede detailed cavity optimization.
|
||||
|
||||
The second design implication from Section and is that cavity placement and cavity design form one optimization problem for direct retained-powder AMPDs. The target mode, load path and functional response define where retained powder motion is useful, while structural and manufacturing constraints define which internal design is feasible,,,,,,. The selected combination should then be judged using application measures such as cutting stability, forced response or optical stability,,.
|
||||
|
||||
The third design implication from the validation levels in Section and is that each level should answer a different question through its test method, frequency evidence and reported metric. Numerical evidence units can identify candidate modes and response bands and screen particle activation trends,,. At specimen level, harmonic or swept-sine tests and impact-hammer FRFs should map activation, amplitude dependence and modal damping across several amplitudes and modes,,. Component tests should retain the relevant modal or local frequency information while adding mounting, stiffness, resonance shifts and modal coupling,,. Across both routes, application tests should reproduce operational inputs and connect frequency response to functional measures such as forced response, fatigue, cutting stability or optical stability,,,,,,. Repeatability and response stability under repeated excitation or service exposure then become part of qualification,,,,. Validation should therefore progress from mechanism and activation maps, through integrated component response, to functional performance and stability over time.
|
||||
|
||||
The fourth design implication from the reporting completeness analysis in Section and is that a transferable AMPD design must be defined across its full lifecycle. Its initial particle or powder condition, variation across specimens and builds, and changes during repeated use form one continuous design record that links the manufactured state to reproducibility and stability under operating conditions,,,,,.
|
||||
|
||||
In summary, the preceding design implications point to four research priorities. First, shared reference geometries and open data for each evidence unit should connect damping metrics to matched baselines. Second, nondestructive indicators of retained powder state should be calibrated against mobility and dynamic response. Third, lifecycle tests should quantify compaction, sintering, recovery, leakage and fatigue interactions. Fourth, multiscale models should propagate manufacturing, material-batch, boundary-condition and internal-state variability into response uncertainty. Together, these priorities connect AMPD design choices with the modeling, validation and reporting needed to compare performance across machines, materials, heat treatments and service conditions.
|
||||
|
||||
## 8\. Conclusions
|
||||
|
||||
This review connects the classification of AMPD manufacturing and filling approaches with cavity design, testing methods, reported performance and the evidence still needed for reliable comparison and qualification. The main conclusions follow this sequence from route selection and design to validation, reporting completeness and future development:
|
||||
|
||||
- •
|
||||
The evidence table contains 108 publication records and yields 79 independent AMPD evidence units, comprising 64 direct retained-powder evidence units and 15 post-filled evidence units. The detailed design, frequency and reporting analyses use the 64 direct evidence units, while the 15 post-filled evidence units remain in the route and performance comparisons. Six related publication records remain in the evidence table as context. Because the two AMPD routes create and control the damping medium differently, the manufacturing and filling approach is the starting point for design interpretation.
|
||||
- •
|
||||
The review also establishes a common framework for comparing direct retained-powder AMPD evidence units across cavity placement, internal design, validation level, testing method, frequency evidence and reported performance. This framework places each result within the design and test conditions under which it was obtained. The synthesis retains the original response metric and comparison baseline, making differences among evidence units visible and supporting more consistent interpretation.
|
||||
- •
|
||||
The largest reporting gaps concern particle fill ratio, packing density and particle or powder state, repeatability or uncertainty, and lifecycle or degradation. Reporting these fields links the initial internal condition to variation across specimens and builds and to changes during repeated use or service. This evidence supports evaluation of reproducibility and stability under the intended operating conditions.
|
||||
|
||||
This review therefore provides a unified basis for future AMPD research by connecting route selection, performance interpretation and the evidence required for reproducible and transferable design across materials, manufacturing processes and operating conditions.
|
||||
|
||||
## CRediT authorship contribution statement
|
||||
|
||||
**Weijia Yu:** Writing – review & editing, Writing – original draft, Visualization, Software, Methodology, Investigation, Formal analysis, Data curation, Conceptualization. **Marcus Oel:** Writing – review & editing. **Jens Niedermeyer:** Writing – review & editing. **Lennart Mesecke:** Writing – review & editing. **Ina Meyer:** Writing – review & editing. **Roland Lachmayer:** Writing – review & editing, Supervision.
|
||||
|
||||
## Declaration of generative AI and AI-assisted technologies in the manuscript preparation process
|
||||
|
||||
During the preparation of this work the authors used OpenAI Codex and ChatGPT to support language polishing, editorial revision, and preparation checks for the manuscript, figures and supplementary materials. The tools were not used to independently generate scientific content, evidence classification decisions, data, results or interpretations. After using these tools, the authors reviewed, verified and edited the content as needed and take full responsibility for the content of the published article.
|
||||
|
||||
## Funding
|
||||
|
||||
This research did not receive any specific grant from funding agencies in the public, commercial, or not-for-profit sectors.
|
||||
|
||||
## Declaration of competing interest
|
||||
|
||||
The authors declare that they have no known competing financial interests or personal relationships that could have appeared to influence the work reported in this paper.
|
||||
|
||||
## Appendix A. Supplementary data
|
||||
|
||||
The following is the Supplementary material related to this article. [Download: Download zip file (3MB)](https://ars.els-cdn.com/content/image/1-s2.0-S2772369026000642-mmc1.zip "Download zip file (3MB)")
|
||||
|
||||
MMC S1. AMPD evidence table, search and mapping protocol, MATLAB code, and supporting figure-classification files.
|
||||
|
||||
## Data availability
|
||||
|
||||
The evidence table, search and mapping protocol, and figure generation files supporting this review are supplied as supplementary material. Supplementary file 1 contains the AMPD evidence table in Excel format and includes the master evidence table used for screening, extraction, manufacturing and filling approach classification, figure classification and synthesis. Supplementary file 2 combines the AMPD Search and Mapping Protocol with the figure generation and classification note for the four evidence figures shown as manuscript Figures 2 to 5, including search sources, eligibility rules, controlled vocabulary, figure filters, derived classes and classification rules. Supplementary file 3 is the MATLAB script used to generate the four evidence figures from the supplied evidence table, including supporting count tables. Zenodo version 3 is registered at [10.5281/zenodo.21980315](https://doi.org/10.5281/zenodo.21980315), and the all-versions concept DOI is [10.5281/zenodo.20112102](https://doi.org/10.5281/zenodo.20112102). The Zenodo metadata are public, while the deposited files are embargoed until 31 December 2026. The supplementary files supplied with the resubmission provide the immediately accessible reproducibility package.
|
||||
|
||||
## References
|
||||
|
||||
[^1]: ## 1\. Introduction
|
||||
|
||||
Lightweight and functional additively manufactured components are increasingly used in high performance applications,, where vibration can limit structural performance, process stability or functional precision. Additional damping is attractive in such cases, but external damping devices can add mass, occupy design space or disturb the component function,. Particle damping offers a compact passive approach in which vibration energy is dissipated through relative particle motion, impacts and frictional contacts when particles have sufficient freedom to move inside a cavity,.
|
||||
|
||||
Additive manufacturing changes how this mechanism can be integrated. Internal cavities, local architecture and particle filled volumes can be designed together with the structural load path, so particle damping can be integrated within the printed component instead of added as a separate damping element,,. In additively manufactured particle damping structures (AMPDs), the damping medium may be unfused build powder retained during powder bed fusion of metals using a laser beam (PBF-LB/M) or particles introduced after fabrication. summarizes these manufacturing and filling approaches and their integration into AMPD structures. This integration has been studied, for example, for blade like parts,,, machining tools,, vibration sensitive optical holders and topology based lightweight design concepts.
|
||||
|
||||

|
||||
|
||||
Download: Download high-res image (277KB)
|
||||
|
||||
The recent AMPD literature has moved beyond isolated feasibility demonstrations. Retained powder beams,, blades, walls, gears, optical holders and tooling elements have shown measurable reductions in vibration response or increases in damping under specific test conditions. These examples indicate a broad application space, but they are spread across different manufacturing and filling approaches, powder or particle states, cavity designs, reported frequency ranges and evaluation methods.
|
||||
|
||||
This creates a comparability problem that goes beyond terminology. Similar AMPD terminology can describe retained build powder, particles introduced after fabrication or related particle damping concepts, although these approaches differ in how the damping medium is created, controlled and qualified,,,. Reported damping improvements therefore cannot be interpreted as transferable design evidence by metric value alone. The central question is whether these case specific AMPD results can be organized into transferable design guidance without merging physically different manufacturing and filling approaches.
|
||||
|
||||
Prior reviews provide complementary foundations for this question. Gagnon et al. synthesize particle-damper modeling, discrete-element calibration and experimental testing, while Ehlers et al. focus on design guidelines for laser-beam-melted retained-powder dampers. Niedermeyer et al. examine compressor-blade requirements and AMPD potential, and Zhu et al. review tuned particle dampers across mechanisms, models and applications. The present review builds on these reviews by comparing AMPD manufacturing and filling approaches, their testing methods and the way performance is reported. This comparison shows which findings can be considered together and where differences among evidence units still limit broader design guidance.
|
||||
|
||||
This review addresses that question by organizing a structured AMPD evidence table with 108 publication records around explicit boundaries between manufacturing and filling approaches. It focuses on where AMPD has been applied, which reported frequency ranges and validation evidence are available, and which cavity, powder or particle, excitation, metric and reporting variables should be considered before results are compared across evidence units. It also derives a compact reporting set that improves comparability in future AMPD work.
|
||||
|
||||
## 2\. Evidence base and classification framework
|
||||
|
||||
The synthesis uses a structured AMPD evidence table with 108 publication records (R1–R108). Scopus was used as the primary database, with complementary Web of Science searches, Google Scholar checks, and backward and forward citation tracking. The first complete search round was completed on 14 January 2026, and the final update search was conducted on 12 June 2026 using the same retrieval logic.
|
||||
|
||||
The first author conducted the keyword searches, compiled the evidence table and manually checked its publication records and classifications against the corresponding sources. Eligibility and ambiguous cases were assessed using the documented rules. Supplementary File 1 is the AMPD evidence table with the publication records, evidence-unit assignments and coded data. Supplementary File 2 is the AMPD Search and Mapping Protocol with the search and figure classification rules. The verified table was then processed using a MATLAB script to generate the figures and supporting count tables.
|
||||
|
||||
A publication record is one bibliographic row in the evidence table. For,,,, an evidence unit is the smallest independently countable contribution, such as a distinct specimen group, experimental data set or original model contribution. Potentially duplicate and overlapping publication records were checked during selection, and alternate publication records based on the same specimens, data or experiment were combined into one evidence unit. Similar authorship or topic alone was not treated as evidence of duplication. Publication records containing both unique and reused evidence were retained and flagged in the evidence table.
|
||||
|
||||
In the manuscript, the evidence table has two practical roles. It defines how the publication records are grouped by manufacturing and filling approach, and it keeps the evidence unit counts traceable. Publication records were classified as AMPD when additive manufacturing defined the damping structure and loose unfused powder or inserted particles were the damping medium. Related publication records were kept when they helped compare manufacturing and filling approaches, but they were not included in the direct retained-powder or post-filled AMPD evidence unit counts. Publication records representing reviews, providing limited detail or showing substantial overlap were retained for context when useful, but were not treated as evidence units in the figures when they mainly synthesized or reused earlier data. Each publication record was coded for process, powder and cavity descriptors, validation level, reported frequency ranges, excitation regime, response metrics, baseline information, limitations and its role in forming evidence units.
|
||||
|
||||
## 3\. Manufacturing and filling approach boundaries
|
||||
|
||||
Manufacturing and filling approach is the primary classification variable. It describes how the damping medium is created, retained or introduced in the additively manufactured structure.
|
||||
|
||||
summarizes 79 independent AMPD evidence units derived from the 108 publication records in the evidence table. These comprise 29 direct retained-powder evidence units without designed internal structures, 35 direct retained-powder evidence units with designed internal structures and 15 post-filled evidence units. The horizontal bars show the number of evidence units in each manufacturing and filling category, and the colored segments show validation level. The evidence table lists the publication records corresponding to each evidence unit.,, examine the 64 direct retained-powder evidence units.
|
||||
|
||||
Validation level was classified independently of manufacturing and filling approach. It describes the context in which a result was obtained. The five definitions are given in.
|
||||
|
||||
separates direct retained-powder AMPD into two categories according to the presence of designed internal structures. In both categories, loose or partially mobile unfused build powder remains inside sealed printed volumes and contributes to damping,,. Many use PBF-LB/M, which leaves unfused powder inside closed cavities,,. The first category contains 29 evidence units with simple sealed cavities and no designed internal structures. Examples include wall, specimen and beam evidence units,,,.
|
||||
|
||||
Table 1. Definitions of the validation levels used in this review.
|
||||
|
||||
| Level | Definition |
|
||||
| --- | --- |
|
||||
| Concept | Concept or contextual contribution without original numerical analysis or physical testing. |
|
||||
| Numerical | Modeling, simulation or optimization as the primary contribution, without new physical damping tests. |
|
||||
| Specimen | Tests on coupons, beams, blocks, dampers or other bench-scale specimens. |
|
||||
| Component | Tests on a functional component or subsystem outside its final service environment. |
|
||||
| Application | Tests under application-relevant loading or environmental conditions, or with a functional performance metric. |
|
||||
|
||||

|
||||
|
||||
Download: Download high-res image (256KB)
|
||||
|
||||

|
||||
|
||||
Download: Download high-res image (263KB)
|
||||
|
||||
Table 2. Representative comparisons within evidence units for the three AMPD categories in.
|
||||
|
||||
| Category and source | Comparison | Test and reported result | Main insight |
|
||||
| --- | --- | --- | --- |
|
||||
| Direct retained-powder, simple cavity. Westbeld et al.. | AlSi10Mg specimens with mobile or sintered powder were compared with solid references. The evidence unit included 44 cavity specimens, 18 solid specimens and four measurements per specimen. | Periodic chirp at 800 mm/s <sup>2</sup> over 50–8000 Hz. Global sintering produced no significant particle damping. Mobile powder produced a maximum relative loss factor increase of 1425%. | Powder mobility determines whether damping is activated. |
|
||||
| Direct retained-powder, internal pockets. Scott-Emuakpor et al.. | Four IN718 AMPD blades were compared with four fully fused blades. | A 0–6000 Hz sweep was followed by modal and fatigue tests. Mean quality factor decreased by about 45% and 60% at two modes, while fatigue resistance increased. | Modal response and durability should be evaluated together. |
|
||||
| Post-filled TPMS tool. Han et al.. | Four tool variants were compared with a solid tool under 16 cutting condition groups. Repeat count was not reported. | Dry turning with modes near 1299, 1303 and 5119 Hz. At 145 g fill mass, damping ratio reached 0.03 and energy dissipation efficiency reached 48%. Low fill could underperform the solid tool. | Fill state and operating condition determine the functional benefit. |
|
||||
|
||||
The second category contains 35 evidence units with designed internal structures. Examples include divided cavities, ribs, lattice cavities, resonant features and flexure guided structures,,,,,. Internal design adds a distinct design variable by changing how the powder volume is arranged within the printed structure.
|
||||
|
||||
The third category contains 15 post-filled AMPD evidence units. In this category, additive manufacturing creates the host structure, cavity, insert or module, while the particle damping medium is introduced and sealed after fabrication. Mixed retained and inserted cases are included in this category. Examples include additively manufactured toolholder and machining evidence units,, post-filled inserts or modules, and TPMS-based particle dampers,. Six related publication records outside these definitions remain as unplotted context in the evidence table,,,.
|
||||
|
||||
gives one representative comparison from each AMPD category in. The complete performance summary is provided in the evidence table.
|
||||
|
||||
The distribution of validation levels in shows where the available evidence is concentrated. Most evidence in the two direct retained-powder categories comes from specimen tests, including walls and beams,,,,. Component and application evidence is less common and appears in blades,, gears, optical holders and post-filled machining systems. Nine numerical evidence units address particle behavior, packing density control and design optimization,,,. Section therefore examines cavity placement and internal design in the 64 direct retained-powder evidence units.
|
||||
|
||||
## 4\. Direct retained-powder design variables
|
||||
|
||||
After the manufacturing and filling approach boundaries in, focuses on the direct retained-powder subset. It maps the cavity placement and cavity design classifications of 64 independent evidence units. The figure shows how retained powder volumes are positioned and shaped internally, so the following discussion can focus on design patterns instead of repeating the approach boundary.
|
||||
|
||||
Each direct retained-powder evidence unit contributes to one primary placement class and one primary cavity design class in. Detailed class definitions and precedence rules for cases with multiple applicable descriptions are provided in Supplementary File 2.
|
||||
|
||||
The placement axis describes the logic used to locate the powder volume. Mode targeted evidence units place cavities with respect to modal or operational response, including modal displacement, antinode, strain or forced response regions,,. Neutral axis evidence units use a low strain or neutral axis region as the placement reference when damping space must be balanced with stiffness or functional geometry,,. Multiple cavities describe distributed powder pockets or chamber arrays within one structure,,. Component layout covers cases where the available part geometry or functional space drives the cavity position, as in gears, instrumentation rake bodies and tooling elements,,. Cavity variation is retained as the fallback placement category when cavity position is compared together with size, number or other cavity design parameters and no single placement rule dominates,,.
|
||||
|
||||
The design axis describes the internal form of the powder containing volume. Simple cavity evidence units use closed or sealed powder volumes without designed internal structures,. Divided cavities split the powder space into chambers, pockets or partitioned regions,. Internal features add ribs, stiffening features or other obstacles inside the cavity,,. Lattice cavity evidence units combine retained powder with lattice type members or chambered lattice structures,,. Local resonator evidence units couple retained powder to a resonant substructure or absorber type design,. In this classification, multiple cavities and divided cavities are not duplicates. The first describes distributed placement of powder volumes, while the second describes subdivision of the cavity interior.
|
||||
|
||||
The plotted counts show where direct retained-powder AMPD design evidence is concentrated. Cavity variation is the largest placement category with 28 evidence units, followed by mode targeted placement with 20 evidence units. Multiple cavities and component layout each contain 6 evidence units, and neutral axis placement contains 4 evidence units. On the design axis, simple cavities and divided cavities form the largest categories with 29 and 19 evidence units, followed by internal features with 7 evidence units. Local resonators appear in 5 evidence units and lattice cavities in 4 evidence units. The most populated cells are cavity variation with simple cavities, mode targeted placement with simple cavities and mode targeted placement with divided cavities. This pattern shows that the direct retained-powder literature is weighted toward modal placement, cavity design comparisons and simple or partitioned cavity designs.
|
||||
|
||||
This classification supports a more specific design interpretation. Cavity placement can matter as much as cavity volume because retained powder must move relative to the cavity walls under the active response,,. At the same time, cavity design strategy changes both powder motion and structural response, because partitions, ribs, lattice members and resonant substructures can modify particle travel distance, contact conditions, local stiffness and coupling to a target mode,,,. Their benefit is conditional because the same feature that redirects particles can also reduce clearance, restrict powder mobility or change the load carrying geometry,,. Geometry descriptors should therefore be read together with powder state and baseline definition. Cavity ratio, cavity volume fraction, unfused powder volume percentage, particle filling ratio and packing density describe related but different quantities, and they should not be treated as interchangeable damping predictors,,,.
|
||||
|
||||
This design classification provides the context for comparing reported frequency ranges, excitation regimes and validation metrics in Section.
|
||||
|
||||
## 5\. Validation evidence and metric comparability
|
||||
|
||||
After the manufacturing and filling approach boundaries in and the direct retained-powder design variables in, the next comparison is how these designs have been tested. maps the frequency information reported for 64 direct retained-powder AMPD evidence units. It separates impact-hammer FRF, impulse or free decay, shock or transient loading, harmonic or swept-sine testing, random or broadband testing, mixed or operational testing and numerical or modeling-only work as primary evaluation methods. Detailed method definitions and assignment rules are provided in Supplementary File 2, while the primary and secondary method classifications for each evidence unit are listed in Supplementary File 1.
|
||||
|
||||
The 64 evidence units comprise 26 harmonic or swept-sine, 15 impact-hammer FRF, 9 numerical or modeling-only, 7 mixed or operational, 5 impulse or free-decay and 2 shock or transient evaluations. None uses random or broadband testing as its primary method, although broadband input appears as a secondary method in some mixed or operational evidence units.
|
||||
|
||||

|
||||
|
||||
Download: Download high-res image (1MB)
|
||||
|
||||
Of the 64 evidence units, 18 report continuous ranges, 6 discrete point sets, 28 modal-frequency sets and 8 local bands. Four lack a verifiable numeric frequency or mode and remain listed as no numeric beside their source labels. Filled circles mark continuous-range endpoints and discrete points, filled diamonds mark modal frequencies and filled squares mark local-band endpoints. Each source mark uses the color assigned to its validation level. Ranges beginning at 0 Hz are shown from the 1-Hz limit of the logarithmic axis.
|
||||
|
||||
The frequency information in becomes meaningful when the input method and response metric are read together. Impact-hammer FRF tests identify modes and describe damping or response amplitude around resonance. Impulse or free-decay tests obtain modal damping from the response after release or impulse. Shock or transient tests quantify the decay after a short input through measures such as quality factor and damping ratio. Harmonic or swept-sine tests resolve changes in resonance, loss metrics and dissipated energy across frequency and amplitude.
|
||||
|
||||
Mixed or operational tests connect the vibration response to functional measures such as stress, fatigue or transmissibility,. Numerical evidence units examine particle motion and particle–wall interactions, with experimental calibration determining their design relevance. The absence of random or broadband excitation as a primary method leaves service representative broadband loading as a validation gap.
|
||||
|
||||
These metrics describe different parts of the structural response. Interpreting a lower FRF peak requires checking mass, stiffness and resonance shift together with damping. Comparison across evidence units therefore requires the input type and amplitude, frequency or mode, response location, metric definition and baseline to be reported together. A useful next step is to test several modes with more than one input method on the same specimens and baseline. This would connect modal damping, FRF amplitude, energy loss and functional response under controlled conditions.
|
||||
|
||||
Excitation amplitude is a design variable in AMPD because the particle motion changes as the input increases. At low input, the powder can move with the cavity walls and dissipate little energy. As relative motion develops, sliding and collisions increase dissipation. Further increases can produce saturation, softening, hysteresis or jump behavior,,. Characterizing this working range requires damping measurements at several specified amplitudes. Frequency sweeps should therefore be repeated at controlled amplitudes and in both sweep directions, with response amplitude and activation or saturation thresholds reported. The resulting frequency and amplitude maps would show whether a design remains effective across its intended load range.
|
||||
|
||||
PBF-LB/M feedstock powder introduces a second design dimension. Micrometer scale powder has a greater relative influence of attractive and surface forces than the millimeter scale particles used in many classical dampers,. Its mobility also depends on material, particle size distribution, surface condition, packing density and compaction,,,. The same nominal cavity geometry can therefore show different damping when the powder material or state changes. Controlled comparisons across materials should hold cavity geometry, structural baseline and excitation constant while varying powder material, size distribution, packing and compaction. maps testing conditions and validation levels, while the evidence table records the particle descriptors and powder state needed for this comparison.
|
||||
|
||||

|
||||
|
||||
Download: Download high-res image (349KB)
|
||||
|
||||
Table 3. Baseline comparisons for three recurring research purposes in the reviewed AMPD literature.
|
||||
|
||||
| Purpose | Suitable comparison | Supported interpretation |
|
||||
| --- | --- | --- |
|
||||
| Mechanism attribution | Compare retained-powder specimens with corresponding empty cavity, solid or altered powder state specimens. Keep the boundary condition and excitation consistent, and report changes in mass, stiffness, natural frequency and mode shape,,. | Whether the measured response is consistent with particle mobility and dissipation at the tested mode, amplitude and powder state. |
|
||||
| Design trade-off under stated constraints | Compare feasible designs under the same functional requirements and report the relevant mass, stiffness, strength, manufacturing and frequency constraints,,. | The vibration benefit obtained within the tested design constraints, including damping and changes in resonance. |
|
||||
| Functional performance and durability | Compare the AMPD design with a functional reference under the same mounting, loading and environmental conditions, and include repeated specimens or cyclic states where available,,. | The functional benefit and its repeatability or stability over the tested conditions and duration. |
|
||||
|
||||
Taken together, the 64 evidence units comprise 41 specimen evidence units, 9 numerical evidence units, 7 component evidence units and 7 application evidence units. The distribution is concentrated at specimen level, while component and application evidence each account for 7 evidence units.
|
||||
|
||||
The testing and frequency evidence in must be interpreted together with the reported response metric and baseline because a reduction in vibration response can arise from particle dissipation, changes in mass or stiffness, a shift in resonance, or a combination of these effects. The baseline must therefore be chosen according to the question being tested. summarizes the baseline implications derived from analysis through three recurring research purposes: identifying the contribution of particle mobility, evaluating vibration performance under stated design constraints, and testing functional performance and durability. For each purpose, the table links a suitable comparison with the conclusion that the available evidence can support. The reporting information needed for these comparisons is examined in Section.
|
||||
|
||||
## 6\. Reporting completeness and comparability needs
|
||||
|
||||
Comparisons across AMPD evidence units become difficult when important experimental information is incomplete or reported in different ways. therefore examines the reporting completeness of 64 direct retained-powder AMPD evidence units. The fields cover the information needed to describe their designs, tests and validation results, with detailed definitions in Supplementary File 2 and the corresponding evidence in Supplementary File 1. Each field is classified as Reported, Partly reported, Not reported or Not applicable. The applicable denominator includes the first three statuses, while Not applicable is shown separately.
|
||||
|
||||
shows that basic descriptions of AMPD design and testing are available in most evidence units. AM process and material and boundary condition each reach the Reported threshold in 60 evidence units. Cavity metric reaches it in 59 evidence units, geometry in 58 evidence units and excitation level in 50 evidence units. The largest gaps are concentrated in particle fill ratio, packing density or powder state, repeatability or uncertainty, and lifecycle or degradation. The following paragraphs discuss why these four areas remain incomplete and how they affect comparison and reproducibility.
|
||||
|
||||
Particle fill ratio and packing density describe two linked controls of retained powder motion. Fill ratio sets the powder amount relative to cavity volume, while packing density and powder state determine how that material is arranged and constrained. In, particle fill ratio is Reported in 5 evidence units, Partly reported in 56 and Not reported in 3. Packing density or powder state is Reported in 38 evidence units, Partly reported in 25 and Not reported in 1. The distinction is mechanically important. Fill ratio governs the overall free space available for particle motion. Packing density, compaction and cohesion govern the internal contact network, frictional sliding and the excitation threshold required to mobilize the powder,,,. Identical cavity geometry and nominal fill ratio can therefore produce different damping after processing or repeated loading changes the powder state. Future AMPD work should report a clearly defined volume or mass basis together with the measured powder state before and after testing, allowing particle activation and energy dissipation to be linked to a reproducible internal condition.
|
||||
|
||||
Repeatability or uncertainty is Reported in 33 evidence units, Partly reported in 28, Not reported in 1 and Not applicable in 2. The large Partly reported group mainly contains specimen or repeat counts without a measure of variation. Repeated measurements on one specimen characterize variation in the test and response. Measurements across specimens and builds capture variation introduced by manufacturing and the retained powder state. Local packing, compaction and powder redistribution can change the damping response under nominally identical geometry and loading,,. Repeated runs can provide a precise mean for one specimen. Reproducibility across specimens and builds requires separate replication. Future AMPD work should distinguish repeated runs, specimens and builds and report dispersion or uncertainty at each level together with the corresponding powder state.
|
||||
|
||||
Table 4. Proposed minimum AMPD reporting checklist for future work.
|
||||
|
||||
| Reporting item | Minimum information | Risk if omitted |
|
||||
| --- | --- | --- |
|
||||
| Approach identity | Identify retained build powder, post-filled particles or another related approach. Report sealing and powder removal where relevant. | Routes may be compared although their damping media are created and controlled differently. |
|
||||
| Cavity and structure | Report cavity placement, wall thickness, internal design, mass change and geometry relevant to stiffness. | Geometry or stiffness effects may be attributed to powder damping. |
|
||||
| Powder or particle state | Report particle material and size, retained powder condition, packing density or fill measure, and heat treatment or compaction history. | Fill ratio, packing density and powder state may be treated as equivalent. |
|
||||
| Test condition | Report input type and amplitude, frequency range or test points, mounting and signal chain. | Results may be compared across different particle activation conditions. |
|
||||
| Baseline and metric | Define the reference and report AMPD and reference mass, powder or particle mass where available, natural-frequency shift, stiffness change or a justified proxy, and the response or functional metric. | Mass, stiffness and detuning may confound interpretation of the damping benefit. |
|
||||
| Repeatability and service | Report specimen and repeat counts, uncertainty, repeated excitation effects, degradation and powder state after testing. | Initial performance may be interpreted as repeatable or durable. |
|
||||
|
||||
Lifecycle or degradation is Reported in 25 evidence units, Partly reported in 2, Not reported in 34 and Not applicable in 3, making it the largest Not reported group in. Most evidence units therefore characterize AMPD performance in its initial state, leaving stability under mechanical and thermal history unresolved. Retained powder damping is state dependent. Repeated resonance passes and high strain dwell can compact, redistribute or locally fuse the powder,,. Heat treatment can form sintered contacts and reduce particle mobility, while later excitation can fragment some contacts and change the response again. Degradation can therefore involve transitions between loose, compacted, trapped and sintered powder states, with corresponding changes in activation and energy dissipation,. Application validation should track damping against load cycles, amplitude and thermal history and document the powder state before and after testing. This would show whether the damping response remains stable, changes gradually or undergoes an irreversible loss.
|
||||
|
||||
These reporting gaps motivate the AMPD reporting checklist in. The checklist combines the weak reporting fields in with the manufacturing and filling approach, cavity design and validation variables discussed above. It lists the minimum information that future AMPD work should report before results are compared across manufacturing and filling approaches, cavity designs, test conditions and baselines.
|
||||
|
||||
## 7\. Design implications
|
||||
|
||||
This section discusses the design implications of the reviewed evidence and priorities for future AMPD research.
|
||||
|
||||
The first design implication from the manufacturing and filling categories in and is that the AMPD route should be selected according to the design variable that must remain controllable in the intended application. Direct retained-powder designs without designed internal structures provide control through cavity placement and geometry, designed internal structures add coupled control through internal design, and post-filled designs provide independent control of particle morphology and fill ratio after fabrication,,,,,,,. This route decision should precede detailed cavity optimization.
|
||||
|
||||
The second design implication from Section and is that cavity placement and cavity design form one optimization problem for direct retained-powder AMPDs. The target mode, load path and functional response define where retained powder motion is useful, while structural and manufacturing constraints define which internal design is feasible,,,,,,. The selected combination should then be judged using application measures such as cutting stability, forced response or optical stability,,.
|
||||
|
||||
The third design implication from the validation levels in Section and is that each level should answer a different question through its test method, frequency evidence and reported metric. Numerical evidence units can identify candidate modes and response bands and screen particle activation trends,,. At specimen level, harmonic or swept-sine tests and impact-hammer FRFs should map activation, amplitude dependence and modal damping across several amplitudes and modes,,. Component tests should retain the relevant modal or local frequency information while adding mounting, stiffness, resonance shifts and modal coupling,,. Across both routes, application tests should reproduce operational inputs and connect frequency response to functional measures such as forced response, fatigue, cutting stability or optical stability,,,,,,. Repeatability and response stability under repeated excitation or service exposure then become part of qualification,,,,. Validation should therefore progress from mechanism and activation maps, through integrated component response, to functional performance and stability over time.
|
||||
|
||||
The fourth design implication from the reporting completeness analysis in Section and is that a transferable AMPD design must be defined across its full lifecycle. Its initial particle or powder condition, variation across specimens and builds, and changes during repeated use form one continuous design record that links the manufactured state to reproducibility and stability under operating conditions,,,,,.
|
||||
|
||||
In summary, the preceding design implications point to four research priorities. First, shared reference geometries and open data for each evidence unit should connect damping metrics to matched baselines. Second, nondestructive indicators of retained powder state should be calibrated against mobility and dynamic response. Third, lifecycle tests should quantify compaction, sintering, recovery, leakage and fatigue interactions. Fourth, multiscale models should propagate manufacturing, material-batch, boundary-condition and internal-state variability into response uncertainty. Together, these priorities connect AMPD design choices with the modeling, validation and reporting needed to compare performance across machines, materials, heat treatments and service conditions.
|
||||
|
||||
## 8\. Conclusions
|
||||
|
||||
This review connects the classification of AMPD manufacturing and filling approaches with cavity design, testing methods, reported performance and the evidence still needed for reliable comparison and qualification. The main conclusions follow this sequence from route selection and design to validation, reporting completeness and future development:
|
||||
|
||||
- •
|
||||
The evidence table contains 108 publication records and yields 79 independent AMPD evidence units, comprising 64 direct retained-powder evidence units and 15 post-filled evidence units. The detailed design, frequency and reporting analyses use the 64 direct evidence units, while the 15 post-filled evidence units remain in the route and performance comparisons. Six related publication records remain in the evidence table as context. Because the two AMPD routes create and control the damping medium differently, the manufacturing and filling approach is the starting point for design interpretation.
|
||||
- •
|
||||
The review also establishes a common framework for comparing direct retained-powder AMPD evidence units across cavity placement, internal design, validation level, testing method, frequency evidence and reported performance. This framework places each result within the design and test conditions under which it was obtained. The synthesis retains the original response metric and comparison baseline, making differences among evidence units visible and supporting more consistent interpretation.
|
||||
- •
|
||||
The largest reporting gaps concern particle fill ratio, packing density and particle or powder state, repeatability or uncertainty, and lifecycle or degradation. Reporting these fields links the initial internal condition to variation across specimens and builds and to changes during repeated use or service. This evidence supports evaluation of reproducibility and stability under the intended operating conditions.
|
||||
|
||||
This review therefore provides a unified basis for future AMPD research by connecting route selection, performance interpretation and the evidence required for reproducible and transferable design across materials, manufacturing processes and operating conditions.
|
||||
|
||||
## CRediT authorship contribution statement
|
||||
|
||||
**Weijia Yu:** Writing – review & editing, Writing – original draft, Visualization, Software, Methodology, Investigation, Formal analysis, Data curation, Conceptualization. **Marcus Oel:** Writing – review & editing. **Jens Niedermeyer:** Writing – review & editing. **Lennart Mesecke:** Writing – review & editing. **Ina Meyer:** Writing – review & editing. **Roland Lachmayer:** Writing – review & editing, Supervision.
|
||||
|
||||
## Declaration of generative AI and AI-assisted technologies in the manuscript preparation process
|
||||
|
||||
During the preparation of this work the authors used OpenAI Codex and ChatGPT to support language polishing, editorial revision, and preparation checks for the manuscript, figures and supplementary materials. The tools were not used to independently generate scientific content, evidence classification decisions, data, results or interpretations. After using these tools, the authors reviewed, verified and edited the content as needed and take full responsibility for the content of the published article.
|
||||
|
||||
## Funding
|
||||
|
||||
This research did not receive any specific grant from funding agencies in the public, commercial, or not-for-profit sectors.
|
||||
|
||||
[^2]: Additive manufacturing changes how this mechanism can be integrated. Internal cavities, local architecture and particle filled volumes can be designed together with the structural load path, so particle damping can be integrated within the printed component instead of added as a separate damping element,,. In additively manufactured particle damping structures (AMPDs), the damping medium may be unfused build powder retained during powder bed fusion of metals using a laser beam (PBF-LB/M) or particles introduced after fabrication. summarizes these manufacturing and filling approaches and their integration into AMPD structures. This integration has been studied, for example, for blade like parts,,, machining tools,, vibration sensitive optical holders and topology based lightweight design concepts.
|
||||
|
||||

|
||||
|
||||
Download: Download high-res image (277KB)
|
||||
|
||||
[^3]: | Category and source | Comparison | Test and reported result | Main insight |
|
||||
| --- | --- | --- | --- |
|
||||
| Direct retained-powder, simple cavity. Westbeld et al.. | AlSi10Mg specimens with mobile or sintered powder were compared with solid references. The evidence unit included 44 cavity specimens, 18 solid specimens and four measurements per specimen. | Periodic chirp at 800 mm/s <sup>2</sup> over 50–8000 Hz. Global sintering produced no significant particle damping. Mobile powder produced a maximum relative loss factor increase of 1425%. | Powder mobility determines whether damping is activated. |
|
||||
| Direct retained-powder, internal pockets. Scott-Emuakpor et al.. | Four IN718 AMPD blades were compared with four fully fused blades. | A 0–6000 Hz sweep was followed by modal and fatigue tests. Mean quality factor decreased by about 45% and 60% at two modes, while fatigue resistance increased. | Modal response and durability should be evaluated together. |
|
||||
| Post-filled TPMS tool. Han et al.. | Four tool variants were compared with a solid tool under 16 cutting condition groups. Repeat count was not reported. | Dry turning with modes near 1299, 1303 and 5119 Hz. At 145 g fill mass, damping ratio reached 0.03 and energy dissipation efficiency reached 48%. Low fill could underperform the solid tool. | Fill state and operating condition determine the functional benefit. |
|
||||
|
||||
[^4]: PBF-LB/M feedstock powder introduces a second design dimension. Micrometer scale powder has a greater relative influence of attractive and surface forces than the millimeter scale particles used in many classical dampers,. Its mobility also depends on material, particle size distribution, surface condition, packing density and compaction,,,. The same nominal cavity geometry can therefore show different damping when the powder material or state changes. Controlled comparisons across materials should hold cavity geometry, structural baseline and excitation constant while varying powder material, size distribution, packing and compaction. maps testing conditions and validation levels, while the evidence table records the particle descriptors and powder state needed for this comparison.
|
||||
|
||||

|
||||
|
||||
Download: Download high-res image (349KB)
|
||||
|
||||
Table 3. Baseline comparisons for three recurring research purposes in the reviewed AMPD literature.
|
||||
|
||||
| Purpose | Suitable comparison | Supported interpretation |
|
||||
| --- | --- | --- |
|
||||
| Mechanism attribution | Compare retained-powder specimens with corresponding empty cavity, solid or altered powder state specimens. Keep the boundary condition and excitation consistent, and report changes in mass, stiffness, natural frequency and mode shape,,. | Whether the measured response is consistent with particle mobility and dissipation at the tested mode, amplitude and powder state. |
|
||||
| Design trade-off under stated constraints | Compare feasible designs under the same functional requirements and report the relevant mass, stiffness, strength, manufacturing and frequency constraints,,. | The vibration benefit obtained within the tested design constraints, including damping and changes in resonance. |
|
||||
| Functional performance and durability | Compare the AMPD design with a functional reference under the same mounting, loading and environmental conditions, and include repeated specimens or cyclic states where available,,. | The functional benefit and its repeatability or stability over the tested conditions and duration. |
|
||||
|
||||
[^5]: | Purpose | Suitable comparison | Supported interpretation |
|
||||
| --- | --- | --- |
|
||||
| Mechanism attribution | Compare retained-powder specimens with corresponding empty cavity, solid or altered powder state specimens. Keep the boundary condition and excitation consistent, and report changes in mass, stiffness, natural frequency and mode shape,,. | Whether the measured response is consistent with particle mobility and dissipation at the tested mode, amplitude and powder state. |
|
||||
| Design trade-off under stated constraints | Compare feasible designs under the same functional requirements and report the relevant mass, stiffness, strength, manufacturing and frequency constraints,,. | The vibration benefit obtained within the tested design constraints, including damping and changes in resonance. |
|
||||
| Functional performance and durability | Compare the AMPD design with a functional reference under the same mounting, loading and environmental conditions, and include repeated specimens or cyclic states where available,,. | The functional benefit and its repeatability or stability over the tested conditions and duration. |
|
||||
@@ -0,0 +1,386 @@
|
||||
|
||||
|
||||
## Introduction
|
||||
|
||||
Welcome to "Design for Additive Manufacturing," an extensive guide from [iamrapid.com](https://iamrapid.com/), your trusted 3D printing service provider based in Bangalore, India. This guide will delve into the intricacies of designing specifically for additive manufacturing (AM). This transformative approach allows for creating complex geometries, optimized structures, and customized solutions like never before.
|
||||
|
||||
Additive manufacturing, also known as 3D printing, is reshaping the way products are conceptualized, designed, and manufactured. Its potential is not limited to rapid prototyping, but extends to full-scale production, making it a game-changer in industries such as aerospace, healthcare, automotive, and consumer goods. To fully exploit the capabilities of this technology, it's essential to grasp the principles and best practices for design that can harness the unique benefits of AM.
|
||||
|
||||
Embark on a journey with us as we delve into the crucial considerations, techniques, and tips for designing parts that are not just manufacturable, but also optimized for performance, cost, and innovation. Whether you're a seasoned engineer, a product designer, or an eager enthusiast, this guide is your key to mastering the evolving landscape of additive manufacturing.
|
||||
|
||||
Let's unlock the potential of your designs and bring your ideas to life with the power of 3D printing!
|
||||
|
||||
## What is Additive Manufacturing?
|
||||
|
||||
Additive manufacturing, commonly known as 3D printing, creates objects by adding material layer by layer directly from digital models. Unlike traditional subtractive manufacturing methods that remove material to shape a part, additive manufacturing builds parts with precision and minimal waste. This innovative approach allows for producing complex geometries and customized solutions that were previously unattainable. To understand this further,[click here.](https://iamrapid.com/knowledge-hub/additive-manufacturing-workflow/)
|
||||
|
||||
### Importance of Design in Additive Manufacturing
|
||||
|
||||
Design is the cornerstone of successful additive manufacturing (AM), dictating not only the feasibility and functionality of the final product but also its efficiency, cost, and environmental impact. Understanding and leveraging the principles of AM-specific design can significantly enhance the advantages offered by this transformative technology. Below, we explore the various aspects that underscore the critical importance of design in additive manufacturing.
|
||||
|
||||
- ##### Optimizing for Complex Geometries:
|
||||
AM excels in creating complex geometries that traditional manufacturing methods cannot quickly achieve. **Engineers and Designers can develop intricate structures by designing with AM in mind**, such as lattice frameworks, organic shapes, and internal channels. These designs improve product performance by enhancing strength-to-weight ratios and integrating multiple functions into a single part.
|
||||
|
||||
- ##### Enhancing Material Efficiency and Sustainability:
|
||||
Additive manufacturing builds objects layer by layer, allowing for precise material placement and minimal waste. This contrasts sharply with subtractive manufacturing, which often generates significant material waste.**Designing parts specifically for AM promotes efficient material use**, contributing to sustainability and reducing the overall environmental footprint of manufacturing processes.
|
||||
|
||||
- ##### Facilitating Customization and Personalization:
|
||||
**AM's design flexibility enables the production of customized and personalized products** without extensive retooling. This capability is particularly valuable in healthcare, where tailored implants and prosthetics can significantly improve patient outcomes. This flexibility also benefits consumer goods, allowing for personalized designs catering to individual preferences.
|
||||
|
||||
- ##### Reducing Time to Market:
|
||||
**Designing for AM can accelerate the product development cycle.** Rapid prototyping allows designers to create quickly and test product iterations, refining designs based on real-time feedback. This process reduces development time and speeds up the transition from concept to market-ready product, giving companies a competitive edge in responding to market demands.
|
||||
|
||||
- ##### Achieving Cost-Effectiveness:
|
||||
While the initial setup for AM can be expensive, the long-term benefits often outweigh these costs. **Optimizing designs for AM can reduce the number of parts, streamline assembly processes, and minimize inventory costs.** Additionally, on-demand production eliminates the need for extensive inventories, leading to further cost savings in storage and logistics.
|
||||
|
||||
- ##### Driving Enhanced Performance and Innovation:
|
||||
**Designing for AM encourages innovation by allowing engineers/designers to explore new structures and materials.** This can lead to high-performance components with superior mechanical properties, thermal resistance, or other desired characteristics. The ability to experiment and iterate on designs fosters continuous improvement and technological advancement.
|
||||
|
||||
- ##### Overcoming Traditional Manufacturing Constraints:
|
||||
Traditional manufacturing methods impose various design constraints due to tooling, machining, and fabrication limitations. **AM frees designers from these constraints, enabling greater creative freedom.** This allows for exploring unconventional designs that offer superior performance, aesthetics, and functionality, leading to more innovative products.
|
||||
|
||||
- ##### Integrating Multifunctional Components:
|
||||
**AM allows for creating multifunctional components that combine several parts into one, reducing the need for assembly and improving overall reliability.** Manufacturers can produce more compact and efficient products by designing parts with integrated functions. This integration is particularly advantageous in industries like aerospace and automotive, where space and weight savings are critical.
|
||||
|
||||
- ##### Supporting Distributed Manufacturing:
|
||||
**Designing for AM supports distributed manufacturing, where production can be decentralized and localized.** This approach reduces transportation costs, lowers carbon footprints, and enables on-demand production closer to the end user. Distributed manufacturing enhances supply chain resilience and responsiveness, particularly during disruption.
|
||||
|
||||
- ##### Promoting Continuous Improvement and Iteration:
|
||||
**The iterative nature of AM aligns well with continuous improvement methodologies.** Designers can rapidly prototype, test, and refine products based on real-world feedback, leading to ongoing enhancements. This iterative process fosters innovation and quality improvement, ensuring products remain competitive and meet evolving customer needs.
|
||||
|
||||
By understanding and applying AM-specific design principles, companies can fully harness the potential of additive manufacturing, driving advancements across various industries and shaping the future of production. As you continue to explore and implement AM, thoughtful design will be your key to unlocking its vast possibilities.
|
||||
|
||||
### Types of Additive Manufacturing Processes in Brief
|
||||
|
||||
3D printing technologies, also commonly known as additive manufacturing (Are 3D Printing and Additive Manufacturing the same? [Click here to know](https://iamrapid.com/knowledge-hub/additive-manufacturing-workflow/)), encompass a variety of processes that create objects layer by layer from digital models. Here is a brief overview of the most common 3D printing technologies:
|
||||
|
||||
1. ##### Fused Deposition Modeling (FDM)
|
||||
|
||||
FDM, also known as Fused Filament Fabrication (FFF), is one of the most widely used 3D printing technologies. It works by extruding thermoplastic filament through a heated nozzle, layer by layer, to build up the desired object. FDM is popular for its affordability, ease of use, and versatility, making it ideal for prototyping and hobbyist projects. [Click here](https://iamrapid.com/knowledge-hub/FDM-3D-printing/) to learn more in-depth about FDM.
|
||||
2. ##### Stereolithography (SLA)
|
||||
|
||||
SLA uses a laser to cure liquid resin into hardened plastic in a process called photopolymerization. This technology is known for producing high-resolution, highly detailed parts with smooth surface finishes. SLA is widely used in industries requiring precision, such as jewelry, dental, and medical device manufacturing. [Click here](https://iamrapid.com/knowledge-hub/SLA-3D-printing/) to learn more about SLA.
|
||||
3. ##### Selective Laser Sintering (SLS)
|
||||
|
||||
SLS utilizes a high-powered laser to fuse small particles of polymer powder into a solid structure. Each layer of powder is spread across the build platform and selectively sintered by the laser. SLS is valued for its ability to produce durable, complex geometries without supporting structures, making it suitable for functional prototypes and end-use parts. [Click here](https://iamrapid.com/knowledge-hub/SLS-3D-printing/) to learn more about SLS.
|
||||
4. ##### Digital Light Processing (DLP)
|
||||
|
||||
Similar to SLA, DLP uses light to cure resin, but it differs in that it uses a digital projector screen to flash each layer simultaneously rather than tracing it with a laser. This results in faster print times compared to SLA. DLP is known for high speed and accuracy, making it ideal for detailed models and small parts. [Click here](https://iamrapid.com/3d-printing-services/sla/) to learn more in-depth about DLP.
|
||||
5. ##### Binder Jetting
|
||||
|
||||
Binder jetting involves laying down a layer of powder and then selectively depositing a liquid binder to glue the particles together. This process is repeated layer by layer to build the object. Binder jetting can use various materials, including metals, ceramics, and sand, and is often used for full-color prototypes and metal casting molds. [Click here](https://iamrapid.com/3d-printing-services/) to learn more about Binder Jetting.
|
||||
6. ##### Direct Metal Laser Sintering (DMLS) / Selective Laser Melting (SLM)
|
||||
|
||||
DMLS and SLM are similar technologies that create metal parts by sintering or melting metal powder with a laser. DMLS typically operates at lower temperatures and doesn't fully melt the powder. In contrast, SLM fully melts the powder to form solid metal parts. Both are used for producing robust and complex metal components in the aerospace, automotive, and medical industries. [Click here](https://iamrapid.com/3d-printing-services/dmls/) to learn more about DMLS/SLM.
|
||||
7. ##### Multi Jet Fusion (MJF)
|
||||
Developed by HP, MJF uses an inkjet array to selectively apply fusing agents to a bed of nylon powder, which is then fused by heating elements. This technology allows for the rapid production of highly detailed and durable parts and is particularly effective for functional prototypes and low-volume production runs. [Click here](https://iamrapid.com/3d-printing-services/mjf/) to learn more about MJF.
|
||||
|
||||
### Materials Used in Additive Manufacturing
|
||||
|
||||
In DfAM, having prior knowledge about the materials, their properties, and their applications can significantly enhance the design process. This understanding allows for creating more optimal, manufacturable designs, ensuring that the chosen material aligns with the final product's intended use and performance requirements. By integrating material knowledge early in the design phase, designers can better leverage the full potential of additive manufacturing technologies.
|
||||
|
||||
Below is a brief overview of the primary material categories used in additive manufacturing, highlighting their overall use case scenarios.
|
||||
|
||||
##### 1\. Plastics
|
||||
|
||||
- Thermoplastics: Commonly used in Fused Deposition Modeling (FDM), thermoplastics like [ABS](https://iamrapid.com/materials/ABS/), [PLA](https://iamrapid.com/materials/PLA/), and [PETG](https://iamrapid.com/materials/PETG/) are valued for their ease of use, affordability, and versatility. These materials are ideal for prototyping, hobbyist projects, and functional parts.
|
||||
- High-Performance Plastics:Materials like Nylon, Polycarbonate (PC), and PEEK are used for more demanding applications due to their enhanced mechanical properties, heat resistance, and chemical stability. These are often used in industrial and engineering applications.
|
||||
|
||||
##### 2\. Metals
|
||||
|
||||
- Stainless Steel: Widely used in Direct Metal Laser Sintering (DMLS) and Selective Laser Melting (SLM), stainless steel offers excellent strength, durability, and corrosion resistance. It is used in the aerospace, automotive, and medical industries.
|
||||
- Titanium: Known for its high strength-to-weight ratio and biocompatibility, titanium is used in medical implants, aerospace components, and high-performance engineering parts.
|
||||
- Aluminum: Lightweight and strong, aluminum is used in the AM to produce lightweight parts with good mechanical properties, making it ideal for automotive and aerospace applications.
|
||||
- Other Metals: Cobalt-chrome, Inconel, and copper alloys are used in specialized applications requiring high temperature resistance, corrosion resistance, or electrical conductivity.
|
||||
|
||||
##### 3\. Resins
|
||||
|
||||
- Standard Resins: Used in Stereolithography (SLA) and Digital Light Processing (DLP), standard resins are ideal for creating high-detail prototypes and models. They offer smooth surface finishes and delicate features.
|
||||
- Engineering Resins: These resins, including rigid, flexible, and high-temperature variants, enhance mechanical properties for functional prototypes and end-use parts. Applications include dental, medical, and industrial components.
|
||||
- Biocompatible Resins: Specifically designed for medical and dental applications, these resins meet strict regulatory standards for use in products that come into contact with the human body.
|
||||
|
||||
##### 4\. Composites
|
||||
|
||||
- Fiber-Reinforced Composites: Combining polymers with reinforcing fibers like carbon fiber or fiberglass. These materials offer superior strength and stiffness while remaining lightweight. They are used in aerospace, automotive, and sports equipment.
|
||||
- Metal Matrix Composites (MMCs): TThese composites combine metal powders with ceramic or carbon fibers, enhancing mechanical properties and wear resistance. They are used in high-performance applications where traditional metals may not suffice.
|
||||
- Ceramic Composites: These materials combine ceramic powders with polymers or other binders to create parts with high heat resistance and mechanical strength. Applications include aerospace components and high-temperature industrial parts.
|
||||
|
||||
### Design for Manufacturability (DFM)
|
||||
|
||||
|
||||
|
||||
Design for Manufacturability (DFM) involves optimizing a product design to ensure it can be manufactured quickly and efficiently. In the context of AM, DFM principles help maximize the advantages of additive processes while minimizing potential challenges.
|
||||
|
||||
1. Part Orientation: The orientation of a part during printing affects its strength, surface finish, and print time. Optimal part orientation can improve mechanical properties, reduce the need for supports, and enhance surface quality. Designers should consider the orientation to balance these factors effectively.
|
||||
2. Layer Thickness: The layer thickness in AM influences the resolution, surface finish, and build time. Thinner layers produce finer details and smoother surfaces but increase print time. Designers must choose an appropriate layer thickness based on the required detail and efficiency.
|
||||
3. Support Structures: While AM can create overhangs and intricate features, these often require support structures. Minimizing the need for supports through strategic part orientation and design can reduce post-processing efforts, material waste, and overall print time.
|
||||
4. Surface Finish: The surface finish of AM parts can vary depending on the process and material used. Designers should account for the required surface finish in their designs, considering post-processing steps like sanding, polishing, or coating to achieve the desired result.
|
||||
5. Tolerances and Accuracy: AM processes can produce parts with varying degrees of precision. Designers must understand the specific tolerances of the chosen AM technology to ensure the proper fit and function of assembled components. This involves designing parts with adequate tolerances for their intended applications.
|
||||
6. Post-Processing Requirements: Post-processing can include removing supports, surface finishing, and other treatments to achieve the final part specifications. Designing parts to minimize post-processing can save time and costs, making manufacturing more efficient.
|
||||
|
||||
### Design for Assembly (DFA)
|
||||
|
||||
|
||||
|
||||
Design for Assembly (DFA) focuses on simplifying the assembly process of a product. With AM, many traditional assembly constraints can be bypassed, allowing for more integrated and streamlined designs.
|
||||
|
||||
1. Part Consolidation: The orientation of a part during printing affects its strength, surface finish, and print time. Optimal part orientation can improve mechanical properties, reduce the need for supports, and enhance surface quality. Designers should consider the orientation to balance these factors effectively.
|
||||
2. Snap-Fit and Interlocking Features: The layer thickness in AM influences the resolution, surface finish, and build time. Thinner layers produce finer details and smoother surfaces but increase print time. Designers must choose an appropriate layer thickness based on the required detail and efficiency.
|
||||
3. Modular Design: While AM can create overhangs and intricate features, these often require support structures. Minimizing the need for supports through strategic part orientation and design can reduce post-processing efforts, material waste, and overall print time.
|
||||
4. Ease of Handling: The surface finish of AM parts can vary depending on the process and material used. Designers should account for the required surface finish in their designs, considering post-processing steps like sanding, polishing, or coating to achieve the desired result.
|
||||
|
||||
### Design for Functionality
|
||||
|
||||
|
||||
|
||||
Design for Functionality ensures that the product meets its intended purpose and performs reliably under the specified conditions. AM allows designers to incorporate unique functional features directly into the parts.
|
||||
|
||||
1. Customization and Personalization: AM excels at producing customized and personalized parts without additional cost. Designers can create tailored solutions for individual users or specific applications, such as medical implants, consumer products, and bespoke components.
|
||||
2. Integration of Features: Functional features such as hinges, channels for fluid or airflow, and embedded electronics can be directly integrated into the design. This reduces the need for separate components and enhances the product's overall Functionality.
|
||||
3. Material Selection: The choice of material impacts the final product's Functionality. As discussed earlier, Designers must select materials with the necessary mechanical properties, durability, and environmental resistance for the intended application. AM allows for using a wide range of materials, from plastics and metals to composites and ceramics.
|
||||
4. Performance Optimization: By leveraging AM's capabilities, designers can optimize parts for specific performance criteria, such as weight reduction, improved strength, thermal management, and vibration damping. This often involves advanced simulation and testing to refine the design.
|
||||
|
||||
### Design for Cost Efficiency
|
||||
|
||||
|
||||
|
||||
Design for Cost Efficiency involves creating designs that minimize production costs while maintaining quality and performance. AM offers several innovative design strategies for achieving cost efficiency.
|
||||
|
||||
1. Material Efficiency: Designing parts to use material efficiently can significantly reduce costs. This includes minimizing waste through optimized geometries and internal structures and selecting cost-effective materials that meet performance requirements.
|
||||
2. Production Time: Reducing print time is crucial for cost efficiency. Designers can achieve this by optimizing part orientation, reducing the need for supports, and simplifying geometries where possible. Faster production times lead to lower operational costs and higher throughput.
|
||||
3. Post-Processing Minimization: Post-processing can be a significant cost driver in AM. Designing parts that require minimal post-processing, such as support removal, surface finishing, and assembly, can lower overall production costs and accelerate time-to-market.
|
||||
4. Batch Production and Scaling: While AM is often used for low-volume and customized production, it can also be cost-effective for small to medium quantities batch production. Designing parts for efficient batch processing, including nested arrangements and multi-part builds, can maximize the efficiency of the AM process.
|
||||
|
||||
Understanding and applying these design principles is essential for fully leveraging additive manufacturing's capabilities. These principles help navigate AM's unique opportunities and challenges, ensuring designs are practical, feasible, and economically viable. Staying informed and adaptive in design strategies is critical to achieving sustained success and innovation in this evolving field.
|
||||
|
||||
In addition to the principles mentioned, countless other highly design-specific optimizations exist. These optimizations often rely on the creativity and logical reasoning of the designer. Whether it's finding innovative ways to reduce material usage, improving structural integrity, or enhancing aesthetic appeal, the possibilities for optimization in additive manufacturing are virtually limitless. Designers play a pivotal role in pushing the boundaries of what's possible, continually exploring new techniques, and moving the technology forward. As AM continues to evolve, the collaboration between advanced software tools and human ingenuity will drive unprecedented design and manufacturing innovation levels.
|
||||
|
||||
## CAD Software for Additive Manufacturing
|
||||
|
||||
|
||||
|
||||
Additive manufacturing (AM) heavily relies on Computer-Aided Design (CAD) software to translate innovative ideas into tangible prototypes or end-use products. The CAD software you choose depends on what you are designing. For example, Figurines require freedom to design organic curves and surfaces; another example is Spare parts, which require precision modeling with low tolerances. So, choosing the right software that satisfies your design needs is essential, as it impacts the efficiency, precision, and complexity achievable in your additive manufacturing endeavors. Let's explore some popular CAD software tools.
|
||||
|
||||
### Popular CAD Software Tools
|
||||
|
||||
- Autodesk Fusion 360: Known for its comprehensive cloud-based CAD/CAM/CAE capabilities, Fusion 360 enables seamless collaboration and iteration throughout the design process. Its robust tools for parametric modeling, mesh editing, and generative design make it a go-to choice for additive manufacturing enthusiasts seeking versatility and integration.
|
||||
- SolidWorks: Renowned as an industry standard for mechanical design, SolidWorks specializes in providing powerful parametric modeling capabilities paired with intuitive user interfaces. Its extensive library of features and add-ons facilitates intricate part design and assembly, making it ideal for additive manufacturing applications requiring precision and complexity.
|
||||
- Tinkercad: Tinkercad stands out for its user-friendly, browser-based interface, catering to beginners and educators. Its intuitive drag-and-drop tools allow users to quickly create 3D models suitable for additive manufacturing projects, making it an excellent starting point for early enthusiasts and students exploring the world of 3D design.
|
||||
- Blender: While primarily recognized as a versatile 3D modeling and animation software, Blender's specialty lies in its robust toolset and open-source nature. Its powerful sculpting and mesh editing features enable users to create complex geometries and organic shapes suitable for various designing & AM processes, making it a compelling choice for artists and designers seeking creative freedom.
|
||||
|
||||
Let's take a moment to gather ourselves. We've explored the world of additive manufacturing, including its various processes, available materials, essential design principles, and popular CAD software tools. With this understanding, it's time to examine how you can effectively apply this knowledge as a designer/engineer. So, let's delve into the Design for Additive Manufacturing (DfAM) workflow.
|
||||
|
||||
#### Conceptualization and Ideation
|
||||
|
||||
|
||||
- ##### Define Objectives and Constraints:
|
||||
- - Clearly define the project's goals, including functional requirements, performance targets, and regulatory constraints.
|
||||
- Consider limitations imposed by the chosen additive manufacturing process, such as minimum feature size, build volume, and material compatibility.
|
||||
- ##### Generate and Explore Ideas:
|
||||
- - Conduct brainstorming sessions, sketching exercises, and idea-generation workshops to explore various design possibilities.
|
||||
- Encourage cross-disciplinary collaboration and input from stakeholders to ensure diverse perspectives are considered.
|
||||
- ##### Concept Development and Selection:
|
||||
- - Refine initial concepts based on feasibility, novelty, and alignment with project objectives.
|
||||
- Evaluate and prioritize concepts using technical feasibility, market demand, and potential impact criteria.
|
||||
|
||||
#### CAD Modeling
|
||||
|
||||
|
||||
- ##### Create Detailed 3D Models:
|
||||
- - Utilize CAD software to develop detailed digital models of the intended product or part, considering geometry, dimensions, tolerances, and material properties.
|
||||
- Incorporate features such as fillets, chamfers, and draft angles to improve manufacturability and part quality.
|
||||
- ##### Optimize Designs for Additive Manufacturing:
|
||||
- - Explore design freedom offered by additive manufacturing, including lattice structures, topology optimization, and organic shapes.
|
||||
- Consider design considerations specific to additive manufacturing processes, such as support structures, build orientation, and layer thickness.
|
||||
- Leverage parametric modeling techniques to explore design variations and optimize for performance, cost, and time-to-market.
|
||||
|
||||
#### Simulation and Analysis
|
||||
|
||||
|
||||
- ##### Virtual Testing and Analysis:
|
||||
- - Utilize simulation software to predict and evaluate the behavior of designs under various operating conditions.
|
||||
- Perform structural analysis, thermal simulations, and fluid flow simulations to identify potential performance issues and optimize designs.
|
||||
- ##### Evaluate Manufacturability:
|
||||
- - Assess the manufacturability of designs by simulating the additive manufacturing process in slicing software, which includes build orientation, support structures, and material deposition.
|
||||
- Identify potential issues such as warping, residual stresses, and poor surface finish, and iterate on designs to address them.
|
||||
|
||||
#### Design Optimization
|
||||
|
||||
|
||||
- ##### Iterative Refinement:
|
||||
- - Iterate designs based on simulation results, mock-up feedback, and stakeholder input to address identified issues and optimize performance.
|
||||
- Balance trade-offs between design complexity, part quality, and manufacturing efficiency to achieve the desired outcomes.
|
||||
- ##### Utilize Advanced Optimization Techniques:
|
||||
- - Leverage topology optimization, generative design, and machine learning algorithms to explore design spaces and identify optimal solutions.
|
||||
- Consider multi-objective optimization approaches to simultaneously optimize for conflicting objectives such as weight reduction, stiffness, and cost.
|
||||
- ##### Validate Design Changes:
|
||||
- - Validate design changes through re-simulation and testing to ensure that proposed modifications achieve the desired improvements without introducing new issues.
|
||||
|
||||
#### Prototyping and Testing
|
||||
|
||||
|
||||
- ##### Select Appropriate Additive Manufacturing Method and Materials:
|
||||
- - Choose the most suitable additive manufacturing process based on factors such as part complexity, material properties, surface finish requirements, and production volume. Which additive manufacturing method is right for you? Click here to know.
|
||||
- ##### Fabricate Prototypes:
|
||||
- - Utilize the selected additive manufacturing method to fabricate physical prototypes with accuracy and fidelity to the digital design.
|
||||
- Ensure that the manufacturing parameters, like layer thickness, build orientation, and material selection, are optimized to achieve the desired part quality and performance
|
||||
- ##### Conduct Rigorous Testing:
|
||||
- - Perform comprehensive testing and validation of the prototypes to assess their functional performance, durability, and reliability under real-world conditions.
|
||||
- Use a combination of mechanical testing, environmental testing, and functional testing to evaluate the prototypes' suitability for their intended application.
|
||||
|
||||
#### Final Design Adjustments
|
||||
|
||||
|
||||
- ##### Incorporate Feedback and Lessons Learned:
|
||||
- - Incorporate feedback from prototyping, testing, and stakeholder reviews into final design adjustments.
|
||||
- Address any remaining issues or concerns identified during the development process to ensure the final design meets all requirements and expectations.
|
||||
- ##### Document Design Changes:
|
||||
- - Utilize the selected additive manufacturing method to fabricate physical prototypes with accuracy and fidelity to the digital design.
|
||||
- Ensure that the manufacturing parameters, like layer thickness, build orientation, and material selection, are optimized to achieve the desired part quality and performance
|
||||
- ##### Document Design Changes:
|
||||
- - Document all design changes, revisions, and decisions made throughout the development process to maintain traceability and accountability.
|
||||
- Create detailed design documentation, including engineering drawings, specifications, and Bill of Materials (BOM), to guide manufacturing and assembly processes.
|
||||
- ##### Document Design Changes:
|
||||
- - Finalize the design for production, ensuring that all necessary preparations are made for manufacturing, assembly, and quality control.
|
||||
- Coordinate with manufacturing partners and suppliers to transfer the design into production and ensure a smooth transition from development to deployment.
|
||||
|
||||
#### Final Production through Additive Manufacturing (Optional Step Based on Application of the Design)
|
||||
|
||||
- ##### Scale-Up for Production:
|
||||
- - Transition the optimized design from prototyping to full-scale production using additive manufacturing technologies.
|
||||
- Scale production volumes by optimizing manufacturing processes, streamlining workflows, and maximizing machine utilization.
|
||||
- ##### Manufacturing Process Optimization:
|
||||
- - Fine-tune manufacturing parameters, such as build speed, layer thickness, and material handling, to optimize production efficiency and part quality.
|
||||
- Implement continuous improvement initiatives to identify and address bottlenecks, minimize waste, and enhance productivity throughout the manufacturing process.
|
||||
- ##### Quality Assurance and Control:
|
||||
- - Establish rigorous quality assurance and control measures to ensure manufactured parts' consistency, reliability, and repeatability.
|
||||
- Implement inspection protocols, quality control checks, and validation procedures to verify compliance with design specifications and regulatory requirements.
|
||||
- ##### Supply Chain Integration:
|
||||
- - Integrate additive manufacturing into the broader supply chain ecosystem by collaborating with suppliers, manufacturers, and logistics partners.
|
||||
- Explore opportunities for on-demand manufacturing, distributed production, and agile supply chain strategies to meet evolving market demands and customer requirements.
|
||||
- ##### Post-Processing and Finishing:
|
||||
- - Implement post-processing techniques, such as surface finishing, heat treatment, Painting, and machining, to enhance manufactured parts' aesthetics, functionality, and performance.
|
||||
- Develop standardized post-processing workflows and procedures to ensure consistency and quality across production batches.
|
||||
|
||||
In summary, the Design for Additive Manufacturing (DfAM) workflow provides a structured framework for designers to create innovative, efficient, and manufacturable designs. By following a systematic approach encompassing conceptualization, CAD modeling, simulation, optimization, prototyping, final adjustments, and final production, designers can harness the full potential of additive manufacturing technologies.
|
||||
|
||||
### FDM Design Tips
|
||||
|
||||
- Minimize Overhangs: Keep overhangs below 45 degrees to reduce the need for support.
|
||||
- Consider Layer Orientation: Align layers to maximize strength along the load-bearing direction.
|
||||
- Ensure Adequate Wall Thickness: Use 1-2 mm thick walls for structural integrity.
|
||||
- Add Filets to Corners: Reduce stress concentrations by rounding corners.
|
||||
- Use Chamfers: Replace sharp edges with chamfers to improve print quality and reduce support needs.
|
||||
|
||||
### SLA Design Tips
|
||||
|
||||
- Thin Walls and Fine Details: Keep overhangs below 45 degrees to reduce the need for support.
|
||||
- Include Drainage Holes: Align layers to maximize strength along the load-bearing direction.
|
||||
- Minimize Supports: Use 1-2 mm thick walls for structural integrity.
|
||||
- Avoid Large Flat Surfaces: Reduce stress concentrations by rounding corners.
|
||||
- Prepare for Post-Processing: Replace sharp edges with chamfers to improve print quality and reduce support needs.
|
||||
|
||||
### SLS Design Tips
|
||||
|
||||
- Maintain Minimum Wall Thickness: Use 1-1.5 mm for adequate strength.
|
||||
- Add Escape Holes: Include 2 mm holes for powder removal in cavities.
|
||||
- Design for Moving Parts: Allow 0.5 mm clearance for interlocking parts.
|
||||
- Leverage Surface Texture: Utilize the rough texture for functional or aesthetic purposes.
|
||||
|
||||
### DMLS Design Tips
|
||||
|
||||
- Optimize for Support Removal: Design with easy access for removing supports.
|
||||
- Maintain Consistent Wall Thickness: Use uniform wall thickness to prevent thermal stress.
|
||||
- Include Filets and Chamfers: Reduce sharp edges to minimize stress concentrations.
|
||||
- Plan for Post-Processing: Design for ease of surface finishing and heat treatment.
|
||||
|
||||
### MJF Design Tips
|
||||
|
||||
- Uniform Wall Thickness: Aim for 1-2 mm to prevent warping and ensure strength.
|
||||
- Clearance for Moving Parts: Ensure at least 0.5 mm clearance for articulated parts.
|
||||
- Utilize Escape Holes: Design with holes for powder removal in internal cavities.
|
||||
- Minimize Supports: Use MJF's minimal support requirement by designing self-supporting features.
|
||||
|
||||
For a tabulated summary of the design rules for different 3D printing technologies, refer to the chart below.
|
||||
|
||||
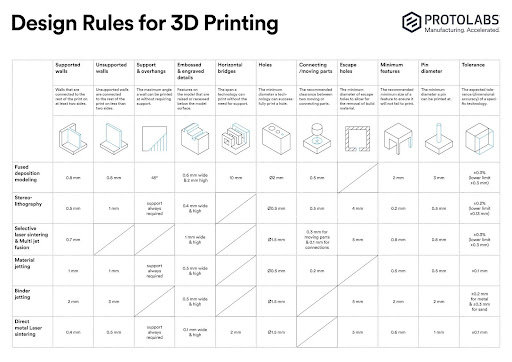
|
||||
|
||||
## Case Studies and Examples
|
||||
|
||||
### Successful Design Projects
|
||||
|
||||
#### General Electric (GE) - Jet Engine Fuel Nozzles
|
||||
|
||||
- Project Overview: General Electric utilized additive manufacturing to redesign the fuel nozzles for their LEAP jet engines. Traditional manufacturing methods required 20 separate parts to be assembled into a single nozzle.
|
||||
- For the design for additive manufacturing (DFAM), GE engineers consolidated the design into a single piece using direct metal laser sintering (DMLS). This significantly reduced the nozzle's complexity and weight while enhancing its durability and performance.
|
||||
- Outcome: The new fuel nozzle design reduced weight by 25% and offered five times the durability of traditionally manufactured nozzles. Integrating multiple components into one streamlined piece also reduced potential points of failure.
|
||||
|
||||
#### Adidas - Futurecraft 4D Shoes
|
||||
|
||||
- Project Overview: Adidas collaborated with Carbon, a leading 3D printing company, to produce the midsole for their Futurecraft 4D shoes. The goal was to create a high-performance shoe with customizable features tailored to individual athletes.
|
||||
- For the design for additive manufacturing (DFAM): Using Digital Light Synthesis (DLS), Adidas created intricate lattice structures in the midsole, optimizing the balance between cushioning and support.
|
||||
- Outcome: The Futurecraft 4D shoes offered enhanced performance and comfort, with the ability to fine-tune the midsole's properties for specific athletic needs. The project demonstrated the potential of additive manufacturing to revolutionize the footwear industry with bespoke designs and rapid prototyping.
|
||||
|
||||
#### Airbus - A350 XWB Cabin Brackets
|
||||
|
||||
- Project Overview: Airbus implemented additive manufacturing to produce over 1,000 parts, including cabin brackets, for its A350 XWB aircraft. These components needed to be lightweight yet strong enough to meet strict aerospace standards.
|
||||
- For the design for additive manufacturing (DFAM): Airbus used Selective Laser Sintering (SLS) to manufacture the brackets from high-performance thermoplastics. This process allowed for complex geometries and weight-optimized designs that were not feasible with traditional manufacturing.
|
||||
- Outcome: Using additive manufacturing in the A350 XWB led to significant weight savings, improved fuel efficiency, and reduced manufacturing costs. This project's success has encouraged the broader adoption of additive manufacturing in the aerospace industry.
|
||||
|
||||
## Common Design Challenges and Solutions
|
||||
|
||||
#### Challenge: Warping in Fused Deposition Modeling (FDM)
|
||||
|
||||
**Solution:** To mitigate warping, designers can use features such as brims and rafts to improve bed adhesion and reduce thermal stress. Additionally, optimizing the part orientation and incorporating gradual transitions in geometry can minimize warping.
|
||||
|
||||
#### Challenge: Surface Finish in Stereolithography (SLA)
|
||||
|
||||
**Solution:** Post-processing techniques, such as sanding, chemical smoothing, and coating, can enhance the surface finish of SLA prints. Designers should also consider using higher resolution settings during printing to reduce the layer visibility.
|
||||
|
||||
#### Challenge: Support Structure Removal in Direct Metal Laser Sintering (DMLS)
|
||||
|
||||
**Solution:** Designing parts with self-supporting angles and minimizing overhangs can reduce the need for support structures. Using lattice structures and strategic support placements can facilitate easier removal and minimize material waste.
|
||||
|
||||
#### Challenge: Inconsistent Material Properties in Multi Jet Fusion (MJF)
|
||||
|
||||
**Solution:** Conduct thorough testing and validation to understand the material properties of MJF-produced parts. Implementing design adjustments, such as uniform wall thickness and consistent part orientation, can enhance material consistency.
|
||||
|
||||
The case studies and examples discussed above highlight the transformative potential of additive manufacturing across various industries. From aviation and footwear to complex aerospace components, Overcoming common design challenges through strategic solutions has demonstrated the feasibility and benefits of this technology.
|
||||
|
||||
## Future Trends in Additive Manufacturing Design
|
||||
|
||||
#### Advances in Materials
|
||||
|
||||
The development of new materials, including high-performance polymers, biocompatible resins, and advanced metal alloys, is expanding additive manufacturing applications. These materials offer improved mechanical properties, biocompatibility, and environmental resistance, opening new possibilities for healthcare, aerospace, and automotive industries.
|
||||
|
||||
#### Innovations in 3D Printing Technologies
|
||||
|
||||
The relentless progress in 3D printing technologies, such as multi-material printing and hybrid manufacturing, is not just enhancing the capabilities and efficiency of additive manufacturing, but also reshaping the very limits of design and manufacturing. These innovations are empowering the production of more intricate and functional parts, heralding a new era in the industry.
|
||||
|
||||
### Impact of AI and Machine Learning
|
||||
|
||||
Artificial intelligence (AI) and machine learning are revolutionizing additive manufacturing, providing powerful tools to enhance design and production processes.
|
||||
|
||||
#### Text-to-3D Generative Software
|
||||
|
||||
Text-to-3D generative software enables users to create 3D models from textual descriptions, significantly streamlining the design process. These tools use natural language processing (NLP) and generative algorithms to interpret textual input and generate accurate, detailed 3D models. This approach simplifies rapid prototyping, allows for extensive customization, and makes 3D design more accessible.
|
||||
|
||||
**Example: Meshy.ai:** Meshy.ai is a leading example of text-to-3D generative software. It allows users to input descriptions, such as "ergonomic office chair," and instantly produces detailed 3D models that can be refined and printed. This tool reduces the time and expertise required for initial model creation, making it a valuable resource for designers and manufacturers.
|
||||
|
||||
#### Generative Design
|
||||
|
||||
Generative design utilizes AI to create multiple options based on specified parameters and constraints, such as material type, weight, and strength. This process involves using algorithms to explore and optimize designs, often producing innovative solutions that human designers might not conceive. Generative design enhances the creation of complex geometries, optimizes performance, and promotes sustainability by reducing material waste.
|
||||
|
||||
**Example: Autodesk Fusion 360:** Autodesk Fusion 360 is a prominent generative design tool. Engineers can input design goals and constraints into the software, generating numerous design iterations that meet these criteria. This allows for selecting the most optimal solution, streamlining the design process, and enhancing efficiency.
|
||||
|
||||
## Conclusion
|
||||
|
||||
Designing for additive manufacturing (AM) isn't just a new approach, it's a transformative one. It opens up possibilities for creating complex, customized, and efficient products that were once unimaginable.
|
||||
|
||||
By understanding various AM processes and materials, designers can fully leverage AM's unique advantages, sparking a new era of design and manufacturing. This guide has covered essential design principles, key considerations, and a comprehensive workflow for AM. AM's benefits, such as customization, complex geometries, reduced material waste, faster prototyping, and cost-effective production, highlight its potential to revolutionize manufacturing.
|
||||
|
||||
As a leading 3D printing partner, [iamrapid.com](https://iamrapid.com/) offers online 3D printing services with an instant quotation system, providing transparent quotes within seconds. At [iamrapid.com](https://iamrapid.com/), you don't just get instant quotations; our advanced quotation software also performs model analysis, including wall thickness analysis, orientation optimization, and repairing parts for optimal printing.
|
||||
|
||||
Moreover, [iamrapid.com](https://iamrapid.com/) excels in complete product design development services, handling the entire design process from ideation to final production-ready design. For further assistance, iamrapid.com is here to support you every step of the way, ensuring your additive manufacturing journey is smooth and successful.
|
||||
|
||||
In summary, designing for additive manufacturing (AM) is a dynamic field with significant opportunities for innovation and efficiency. By following the principles and best practices outlined in this guide, designers can harness AM's full potential to create groundbreaking products.
|
||||
File diff suppressed because it is too large
Load Diff
File diff suppressed because it is too large
Load Diff
File diff suppressed because one or more lines are too long
Reference in New Issue
Block a user