Aggiunge .gitignore ed elabora i restanti documenti in 00 Inbox
Aggiunge .gitignore per stato locale di Obsidian e file di sessione
di Claude Code, e smette di tracciare .obsidian/workspace.json.

Elabora e traduce in italiano gli ultimi documenti grezzi in Inbox:
- Zhou et al. 2024, "Additive Manufacturing: A Comprehensive Review"
  (Sensors, peer-reviewed, CC BY 4.0): scheda fonte e riassunto.
- 5 schede tecniche ADDITIVA (AlSi10Mg, Inconel 718, Scalmalloy,
  Stainless Steel 316L, Ti6Al4V per SLM/DMLS): scheda fonte condivisa
  e 5 note di concetto in 03 Materiali con dati di produttore.

Aggiorna gli indici correlati, rimuove un duplicato della trascrizione
del corso gia' processata e sposta tutti gli originali elaborati da
00 Inbox a 90 Allegati.

Co-Authored-By: Claude Sonnet 5 <noreply@anthropic.com>
This commit is contained in:

 Claude Sonnet 5
+11
@@ -0,0 +1,11 @@
|
||||
# Obsidian: stato locale della finestra, non contenuto del vault
|
||||
.obsidian/workspace.json
|
||||
.obsidian/workspace-mobile.json
|
||||
.obsidian/.trash/
|
||||
|
||||
# Claude Code: stato di sessione locale, non configurazione del progetto
|
||||
.claude/scheduled_tasks.lock
|
||||
|
||||
# File di sistema
|
||||
.DS_Store
|
||||
Thumbs.db
|
||||
Vendored
-212
@@ -1,212 +0,0 @@
|
||||
{
|
||||
"main": {
|
||||
"id": "f5eb1ed854c44144",
|
||||
"type": "split",
|
||||
"children": [
|
||||
{
|
||||
"id": "7781a64056133fc2",
|
||||
"type": "tabs",
|
||||
"children": [
|
||||
{
|
||||
"id": "b15d4de93fabba2b",
|
||||
"type": "leaf",
|
||||
"state": {
|
||||
"type": "markdown",
|
||||
"state": {
|
||||
"file": "10 Fonti/SRC - freeCodeCamp GaugeHow - 3D Printing and Additive Manufacturing Full Course.md",
|
||||
"mode": "source",
|
||||
"source": false
|
||||
},
|
||||
"icon": "lucide-file",
|
||||
"title": "SRC - freeCodeCamp GaugeHow - 3D Printing and Additive Manufacturing Full Course"
|
||||
}
|
||||
},
|
||||
{
|
||||
"id": "2c560b492383128b",
|
||||
"type": "leaf",
|
||||
"state": {
|
||||
"type": "markdown",
|
||||
"state": {
|
||||
"file": "00 Inbox/Da elaborare.md",
|
||||
"mode": "source",
|
||||
"source": false
|
||||
},
|
||||
"icon": "lucide-file",
|
||||
"title": "Da elaborare"
|
||||
}
|
||||
}
|
||||
],
|
||||
"currentTab": 1
|
||||
}
|
||||
],
|
||||
"direction": "vertical"
|
||||
},
|
||||
"left": {
|
||||
"id": "79f9f8f206dd48d7",
|
||||
"type": "split",
|
||||
"children": [
|
||||
{
|
||||
"id": "46bc67c98ca85dec",
|
||||
"type": "tabs",
|
||||
"children": [
|
||||
{
|
||||
"id": "4a186108fcacf10b",
|
||||
"type": "leaf",
|
||||
"state": {
|
||||
"type": "file-explorer",
|
||||
"state": {
|
||||
"sortOrder": "alphabetical",
|
||||
"autoReveal": false,
|
||||
"showSearch": false,
|
||||
"searchQuery": ""
|
||||
},
|
||||
"icon": "lucide-folder-closed",
|
||||
"title": "Esplora file"
|
||||
}
|
||||
},
|
||||
{
|
||||
"id": "26e5b64151c28c96",
|
||||
"type": "leaf",
|
||||
"state": {
|
||||
"type": "search",
|
||||
"state": {
|
||||
"query": "",
|
||||
"matchingCase": false,
|
||||
"explainSearch": false,
|
||||
"collapseAll": false,
|
||||
"extraContext": false,
|
||||
"sortOrder": "alphabetical"
|
||||
},
|
||||
"icon": "lucide-search",
|
||||
"title": "Ricerca"
|
||||
}
|
||||
},
|
||||
{
|
||||
"id": "04f5a1c358acb2d0",
|
||||
"type": "leaf",
|
||||
"state": {
|
||||
"type": "bookmarks",
|
||||
"state": {
|
||||
"showSearch": false,
|
||||
"searchQuery": ""
|
||||
},
|
||||
"icon": "lucide-bookmark",
|
||||
"title": "Segnalibri"
|
||||
}
|
||||
}
|
||||
]
|
||||
}
|
||||
],
|
||||
"direction": "horizontal",
|
||||
"width": 300
|
||||
},
|
||||
"right": {
|
||||
"id": "1613e81d97340acc",
|
||||
"type": "split",
|
||||
"children": [
|
||||
{
|
||||
"id": "66aec59f069e23c6",
|
||||
"type": "tabs",
|
||||
"children": [
|
||||
{
|
||||
"id": "e0b696c89dbe4389",
|
||||
"type": "leaf",
|
||||
"state": {
|
||||
"type": "backlink",
|
||||
"state": {
|
||||
"file": "00 Inbox/Da elaborare.md",
|
||||
"collapseAll": false,
|
||||
"extraContext": false,
|
||||
"sortOrder": "alphabetical",
|
||||
"showSearch": false,
|
||||
"searchQuery": "",
|
||||
"backlinkCollapsed": false,
|
||||
"unlinkedCollapsed": true
|
||||
},
|
||||
"icon": "links-coming-in",
|
||||
"title": "Riferimenti"
|
||||
}
|
||||
},
|
||||
{
|
||||
"id": "c653df34554b6dbf",
|
||||
"type": "leaf",
|
||||
"state": {
|
||||
"type": "outgoing-link",
|
||||
"state": {
|
||||
"file": "00 Inbox/Da elaborare.md",
|
||||
"linksCollapsed": false,
|
||||
"unlinkedCollapsed": true
|
||||
},
|
||||
"icon": "links-going-out",
|
||||
"title": "Collegamenti in uscita"
|
||||
}
|
||||
},
|
||||
{
|
||||
"id": "7116ed142fe5d75a",
|
||||
"type": "leaf",
|
||||
"state": {
|
||||
"type": "tag",
|
||||
"state": {
|
||||
"sortOrder": "frequency",
|
||||
"useHierarchy": true,
|
||||
"showSearch": false,
|
||||
"searchQuery": ""
|
||||
},
|
||||
"icon": "lucide-tags",
|
||||
"title": "Etichette"
|
||||
}
|
||||
},
|
||||
{
|
||||
"id": "85a8bbecc80ccecb",
|
||||
"type": "leaf",
|
||||
"state": {
|
||||
"type": "all-properties",
|
||||
"state": {
|
||||
"sortOrder": "frequency",
|
||||
"showSearch": false,
|
||||
"searchQuery": ""
|
||||
},
|
||||
"icon": "lucide-archive",
|
||||
"title": "Tutte le proprietà"
|
||||
}
|
||||
},
|
||||
{
|
||||
"id": "551d3b30a7743dcd",
|
||||
"type": "leaf",
|
||||
"state": {
|
||||
"type": "outline",
|
||||
"state": {
|
||||
"file": "00 Inbox/Da elaborare.md",
|
||||
"followCursor": false,
|
||||
"showSearch": false,
|
||||
"searchQuery": ""
|
||||
},
|
||||
"icon": "lucide-list",
|
||||
"title": "Struttura"
|
||||
}
|
||||
}
|
||||
]
|
||||
}
|
||||
],
|
||||
"direction": "horizontal",
|
||||
"width": 300,
|
||||
"collapsed": true
|
||||
},
|
||||
"left-ribbon": {
|
||||
"hiddenItems": {
|
||||
"switcher:Apri selettore rapido": false,
|
||||
"graph:Apri vista grafo": false,
|
||||
"canvas:Crea nuova lavagna": false,
|
||||
"templates:Inserisci modello": false,
|
||||
"bases:Crea nuova Base": false
|
||||
}
|
||||
},
|
||||
"active": "2c560b492383128b",
|
||||
"lastOpenFiles": [
|
||||
"00 Inbox/3D Printing & Additive Manufacturing – Full Course.md",
|
||||
"00 Inbox/Da elaborare.md",
|
||||
"11 Riassunti/RIA - freeCodeCamp GaugeHow - 3D Printing and Additive Manufacturing Full Course.md",
|
||||
"10 Fonti/SRC - freeCodeCamp GaugeHow - 3D Printing and Additive Manufacturing Full Course.md",
|
||||
"01 Fondamenti/Flusso di lavoro e formati file per la stampa 3D.md"
|
||||
]
|
||||
}
|
||||
@@ -16,6 +16,8 @@ sources: []
|
||||
Raccogli qui appunti veloci e riferimenti da classificare. Sposta i file binari e gli originali già elaborati in `90 Allegati` e collegali dalla relativa scheda fonte.
|
||||
|
||||
- [x] freeCodeCamp/GaugeHow — 3D Printing & Additive Manufacturing Full Course: trascrizione acquisita, tradotta e trasformata in note; originale spostato in [[90 Allegati/3D Printing & Additive Manufacturing – Full Course|3D Printing & Additive Manufacturing – Full Course]], vedi [[SRC - freeCodeCamp GaugeHow - 3D Printing and Additive Manufacturing Full Course]].
|
||||
- [x] Zhou et al. 2024, "Additive Manufacturing: A Comprehensive Review" (Sensors, CC BY 4.0): riassunto e scheda fonte creati, originale spostato in `90 Allegati`, vedi [[SRC - Zhou et al. 2024 - Additive Manufacturing A Comprehensive Review]].
|
||||
- [x] ADDITIVA — schede tecniche leghe metalliche per SLM/DMLS (AlSi10Mg, Inconel 718, Scalmalloy, Stainless Steel 316L, Titanium Ti6Al4V): tradotte in 5 note di concetto in `03 Materiali`, originali spostati in `90 Allegati`, vedi [[SRC - ADDITIVA - Schede tecniche leghe metalliche per AM]].
|
||||
|
||||
[[Metodo di lavoro]]
|
||||
|
||||
|
||||
@@ -0,0 +1,52 @@
|
||||
---
|
||||
id: "am-aluminium-alsi10mg-slm-dmls"
|
||||
title: "Aluminium AlSi10Mg per SLM/DMLS"
|
||||
type: "concetto"
|
||||
status: "da_verificare"
|
||||
created: "2026-09-10"
|
||||
updated: "2026-09-10"
|
||||
language: "it"
|
||||
tags: ["am/concetto", "am/materiale"]
|
||||
aliases: ["AlSi10Mg", "Alluminio AlSi10Mg"]
|
||||
sources: ["[[SRC - ADDITIVA - Schede tecniche leghe metalliche per AM]]"]
|
||||
material: "lega di alluminio (AlSi10Mg)"
|
||||
process: "powder bed fusion (SLM/DMLS)"
|
||||
---
|
||||
|
||||
# Aluminium AlSi10Mg per SLM/DMLS
|
||||
|
||||
## In breve
|
||||
AlSi10Mg è una lega di alluminio da fonderia (Al-Si-Mg) processabile per powder bed fusion metallica (SLM/DMLS), con buon rapporto resistenza/peso, usata tipicamente per componenti a parete sottile e geometrie complesse. [Fonte: scheda tecnica produttore ADDITIVA; [[SRC - ADDITIVA - Schede tecniche leghe metalliche per AM]]]
|
||||
|
||||
## Spiegazione
|
||||
Lega da fonderia con buona colabilità; nei processi convenzionali di fusione viene tipicamente trattata termicamente con ciclo T6 (solubilizzazione, tempra, invecchiamento artificiale) per migliorare le proprietà meccaniche. Nel processo SLM/DMLS, la fusione e risolidificazione molto rapide producono nello stato "as-built" proprietà meccaniche indicate dal produttore come paragonabili a quelle di un getto trattato T6 (affermazione del produttore, non una misura comparativa indipendente in questa scheda). Applicazioni tipiche indicate: automotive e aerospaziale, in particolare scatole cambio, alloggiamenti e staffe soggette a carichi significativi. Lavorabilità post-stampa dichiarata: lavorazione meccanica, elettroerosione, saldatura, pallinatura (shot-peening), lucidatura, rivestimento.
|
||||
|
||||
## Condizioni di applicazione
|
||||
Dati riferiti al processo SLM/DMLS in polvere metallica, stato "as-built" (dopo stampa) o "stress relieved" (distensione: 300 °C per 2 ore, con rampa 20→300 °C in 1 ora, secondo la scheda). Macchina, fornitore di polvere e parametri di processo (potenza laser, velocità di scansione, spessore layer) non specificati: i valori sono indicativi del produttore ADDITIVA e non generalizzabili ad altri fornitori/macchine.
|
||||
|
||||
## Dati o formule
|
||||
Composizione chimica (% in peso, dato produttore): Al bilancio; Si 9,0–11,0%; Mg 0,20–0,45%; Fe ≤0,55%; Mn ≤0,45%; Ti ≤0,15%; Cu ≤0,10%; Zn ≤0,10%; Ni ≤0,05%; C ≤0,05%.
|
||||
|
||||
Designazioni citate: USA UNS A03600–A13600; EN AC-43000; ASTM B85 A360.0 (F3318); DIN Al 4046-3.2381 — **queste corrispondenze incrociate tra norme sono riportate come nella scheda originale, non verificate singolarmente in questa nota.**
|
||||
|
||||
Proprietà fisiche: densità relativa ≈99,9%; densità 2,67 g/cm³.
|
||||
|
||||
Dati tecnici: accuratezza dimensionale tipica ±0,2/0,3 mm (quota <150 mm), ±0,05 mm ogni 25 mm (quota ≥150 mm); rugosità superficiale as-built Ra 5–9 µm, dopo lavorazione/lucidatura Ra <1,6 µm.
|
||||
|
||||
Proprietà meccaniche (metodo di prova ASTM E8/E8M, provino non lavorato, asse Z):
|
||||
| Proprietà | As-built | Distensione (stress relieved) |
|
||||
|---|---|---|
|
||||
| Resistenza a trazione Rm | 400 ± 5 MPa | 270 ± 5 MPa |
|
||||
| Snervamento Rp0,2% | 255 ± 5 MPa | 160 ± 5 MPa |
|
||||
| Allungamento a rottura | 4,5 ± 1% | 11 ± 1% |
|
||||
| Modulo di Young | 70 ± 3 GPa | 70 ± 3 GPa |
|
||||
| Durezza Brinell (DIN EN ISO 6506-1) | 120 ± 5 HBW | — |
|
||||
| Conducibilità termica (ASTM E1461-13) | 110 ± 5 W/m°C | 170 ± 10 W/m°C |
|
||||
|
||||
Tutti i valori sono dati del produttore, non misure indipendenti: il disclaimer della scheda originale esclude l'uso per specifiche di progettazione o controllo qualità.
|
||||
|
||||
## Esempio
|
||||
Non applicabile (nota di dati di materiale, non caso applicativo documentato).
|
||||
|
||||
## Fonti e collegamenti
|
||||
[[SRC - ADDITIVA - Schede tecniche leghe metalliche per AM]] · [[Leghe Metalliche per AM (Alluminio, Rame, Titanio, Superleghe Inconel)]] · [[Powder Bed Fusion (SLS, SLM, DMLS, EBM)]] · [[Indice - Materiali]]
|
||||
@@ -0,0 +1,55 @@
|
||||
---
|
||||
id: "am-inconel-718-slm-dmls"
|
||||
title: "Inconel 718 per SLM/DMLS"
|
||||
type: "concetto"
|
||||
status: "da_verificare"
|
||||
created: "2026-09-10"
|
||||
updated: "2026-09-10"
|
||||
language: "it"
|
||||
tags: ["am/concetto", "am/materiale"]
|
||||
aliases: ["INCONEL 718", "Superlega Inconel 718", "Alloy 718"]
|
||||
sources: ["[[SRC - ADDITIVA - Schede tecniche leghe metalliche per AM]]"]
|
||||
material: "superlega a base nichel-cromo (Inconel 718)"
|
||||
process: "powder bed fusion (SLM/DMLS)"
|
||||
---
|
||||
|
||||
# Inconel 718 per SLM/DMLS
|
||||
|
||||
## In breve
|
||||
INCONEL® 718 è una superlega nichel-cromo ad alta resistenza e resistenza alla corrosione, versione indurita per invecchiamento della "sorella" lega 625, processabile per powder bed fusion metallica (SLM/DMLS). Intervallo di temperatura di esercizio dichiarato: da -196 °C a 700 °C. [Fonte: scheda tecnica produttore ADDITIVA; [[SRC - ADDITIVA - Schede tecniche leghe metalliche per AM]]]
|
||||
|
||||
## Spiegazione
|
||||
L'indurimento per invecchiamento (precipitation hardening) produce precipitati nella microstruttura che ancorano i grani del metallo, aumentandone significativamente la resistenza. La scheda indica caratteristiche di saldabilità notevoli, in particolare resistenza alla cricca post-saldatura, e buone resistenze a trazione, fatica, creep e rottura. Applicazioni tipiche indicate dal produttore: motori a getto, razzi a propellente liquido, anelli, casse e parti metalliche per motori aeronautici e turbine a gas terrestri, serbatoi criogenici, elementi di fissaggio ad alta temperatura; impiegata anche nel settore oil & gas per resistenza a cloruri, corrosione da sforzo e cricche da solfuri. Lavorabilità post-stampa dichiarata: lavorazione meccanica, saldatura, pallinatura, lucidatura, rivestimento.
|
||||
|
||||
## Condizioni di applicazione
|
||||
Dati riferiti al processo SLM/DMLS, stato "as-built" o trattato termicamente secondo il ciclo AMS 5662 (vedi sotto). Macchina, fornitore di polvere e parametri di processo non specificati: valori indicativi del produttore ADDITIVA, non generalizzabili.
|
||||
|
||||
## Dati o formule
|
||||
Composizione chimica (% in peso, dato produttore): Ni 50,0–55,0%; Cr 17,0–21,0%; Nb 4,7–5,5%; Mo 2,8–3,3%; Ti 0,6–1,2%; Al 0,2–0,8%; Co ≤1,0%; Cu ≤0,3%; C ≤0,08%; Mn ≤0,35%; Si ≤0,35%; P ≤0,015%; S ≤0,015%.
|
||||
|
||||
Designazioni citate: UNS N07718; AMS 5596–5832; ASTM B670–F3055; DIN 2.4668 — riportate come nella scheda originale, non verificate singolarmente in questa nota.
|
||||
|
||||
Proprietà fisiche: densità relativa ≈99,9%; densità 8,15 g/cm³.
|
||||
|
||||
Trattamento termico dichiarato (AMS 5662), in due fasi: 1) ricottura, 20→980 °C, mantenimento 980 °C per 1 ora, raffreddamento a 20 °C; 2) invecchiamento, 20→720 °C, mantenimento 720 °C per 8 ore, 720→620 °C, mantenimento 620 °C per 10 ore, raffreddamento a 20 °C.
|
||||
|
||||
Dati tecnici: accuratezza dimensionale tipica ±0,2/0,3 mm (quota <150 mm), ±0,05 mm ogni 25 mm (quota ≥150 mm); rugosità superficiale as-built Ra 5–9 µm, dopo lavorazione/lucidatura Ra <1,6 µm.
|
||||
|
||||
Proprietà meccaniche (metodo di prova ISO 6892-1:2009(B) Annex D):
|
||||
| Proprietà | As-built | Trattato termicamente (AMS 5662) |
|
||||
|---|---|---|
|
||||
| Resistenza a trazione | 1020 ± 15 MPa | 1400 ± 15 MPa |
|
||||
| Snervamento Rp0,2% | 630 ± 15 MPa | 1140 ± 15 MPa |
|
||||
| Allungamento a rottura | 30 ± 5% | 10 ± 2% |
|
||||
| Modulo di Young | 185 ± 10 GPa | 210 ± 10 GPa |
|
||||
| Durezza (DIN EN ISO 6508-1) | 30 HRC | 46 HRC |
|
||||
|
||||
Proprietà termiche: temperatura massima di esercizio a lungo termine ≈700 °C (1300 °F); conducibilità termica 6–12 W/mK.
|
||||
|
||||
Tutti i valori sono dati del produttore, non misure indipendenti: il disclaimer della scheda originale esclude l'uso per specifiche di progettazione o controllo qualità.
|
||||
|
||||
## Esempio
|
||||
Non applicabile (nota di dati di materiale, non caso applicativo documentato).
|
||||
|
||||
## Fonti e collegamenti
|
||||
[[SRC - ADDITIVA - Schede tecniche leghe metalliche per AM]] · [[Leghe Metalliche per AM (Alluminio, Rame, Titanio, Superleghe Inconel)]] · [[Powder Bed Fusion (SLS, SLM, DMLS, EBM)]] · [[Indice - Materiali]]
|
||||
@@ -19,6 +19,11 @@ Indice da sviluppare: Metalli; polimeri; ceramici; compositi; feedstock; conserv
|
||||
- [[Polimeri per Material Extrusion (PLA, ABS, PETG, Nylon)]]
|
||||
- [[Resine Fotopolimeriche per SLA (Standard, Tough, Flexible, Dental)]]
|
||||
- [[Leghe Metalliche per AM (Alluminio, Rame, Titanio, Superleghe Inconel)]]
|
||||
- [[Aluminium AlSi10Mg per SLM-DMLS]] (dati produttore ADDITIVA)
|
||||
- [[Inconel 718 per SLM-DMLS]] (dati produttore ADDITIVA)
|
||||
- [[Scalmalloy per SLM-DMLS]] (dati produttore ADDITIVA)
|
||||
- [[Stainless Steel 316L per SLM-DMLS]] (dati produttore ADDITIVA)
|
||||
- [[Titanium Ti6Al4V (Grado 23) per SLM-DMLS]] (dati produttore ADDITIVA)
|
||||
|
||||
## Domande da sviluppare
|
||||
- Quali concetti e definizioni servono per questo ambito?
|
||||
|
||||
@@ -95,4 +95,7 @@ Esempi illustrativi citati dal docente (non casi di prova documentati con dati m
|
||||
- Prezzi del titanio e delle altre leghe in rupie indiane per kg di polvere: non verificati, nessuna data di riferimento o fonte di mercato citata; da trattare come ordine di grandezza indicativo, non come dato di costo affidabile.
|
||||
- Riferimenti a ISRO, Agnikool, Skyroot e uso di CuCrZr per componenti di razzi: citati dal docente senza fonte primaria nel video, da trattare come aneddoto di settore fino a verifica.
|
||||
|
||||
> [!info] Dati di produttore disponibili per leghe specifiche
|
||||
> Le stime generiche di questa nota (non verificate, senza lega/produttore specifico) possono essere confrontate con dati di scheda tecnica reali, per lega e stato (as-built/trattato termicamente), nelle note: [[Aluminium AlSi10Mg per SLM-DMLS]], [[Inconel 718 per SLM-DMLS]], [[Scalmalloy per SLM-DMLS]], [[Stainless Steel 316L per SLM-DMLS]], [[Titanium Ti6Al4V (Grado 23) per SLM-DMLS]] — fonte: [[SRC - ADDITIVA - Schede tecniche leghe metalliche per AM]]. Sono comunque dati di un singolo produttore/service bureau, non una norma: il confronto va fatto con cautela (lega, lotto polvere e macchina non sono gli stessi).
|
||||
|
||||
[[Indice - Materiali]] · [[SRC - freeCodeCamp GaugeHow - 3D Printing and Additive Manufacturing Full Course]] · [[RIA - freeCodeCamp GaugeHow - 3D Printing and Additive Manufacturing Full Course]] · [[Polimeri per Material Extrusion (PLA, ABS, PETG, Nylon)]] · [[Resine Fotopolimeriche per SLA (Standard, Tough, Flexible, Dental)]]
|
||||
|
||||
@@ -0,0 +1,54 @@
|
||||
---
|
||||
id: "am-scalmalloy-slm-dmls"
|
||||
title: "Scalmalloy per SLM/DMLS"
|
||||
type: "concetto"
|
||||
status: "da_verificare"
|
||||
created: "2026-09-10"
|
||||
updated: "2026-09-10"
|
||||
language: "it"
|
||||
tags: ["am/concetto", "am/materiale"]
|
||||
aliases: ["Scalmalloy®", "Lega Al-Mg-Sc"]
|
||||
sources: ["[[SRC - ADDITIVA - Schede tecniche leghe metalliche per AM]]"]
|
||||
material: "lega alluminio-magnesio-scandio (Scalmalloy)"
|
||||
process: "powder bed fusion (SLM/DMLS)"
|
||||
---
|
||||
|
||||
# Scalmalloy per SLM/DMLS
|
||||
|
||||
## In breve
|
||||
Scalmalloy è una lega alluminio-magnesio-scandio ad alto rapporto resistenza/peso, elevata rigidità, buona saldabilità e duttilità, sviluppata come alternativa alle leghe di alluminio serie 7000 ad alta resistenza. [Fonte: scheda tecnica produttore ADDITIVA; [[SRC - ADDITIVA - Schede tecniche leghe metalliche per AM]]]
|
||||
|
||||
## Spiegazione
|
||||
La bassa densità permette proprietà specifiche (normalizzate per densità) indicate dal produttore come competitive anche rispetto alle leghe più resistenti in assoluto. Rispetto ad altre leghe di alluminio per manifattura additiva, il produttore dichiara una resistenza alla corrosione particolare e una microstruttura stabile fino a 250 °C. Applicazioni tipiche indicate: componenti fortemente sollecitati in aerospaziale, robotica, settore marino e motorsport; materiale approvato secondo regolamento FIA (affermazione del produttore, normativa specifica non verificata in questa scheda). Lavorabilità post-stampa dichiarata: lavorazione meccanica, saldatura, pallinatura, lucidatura, rivestimento.
|
||||
|
||||
## Condizioni di applicazione
|
||||
Dati riferiti al processo SLM/DMLS, stato "as-built" o trattato termicamente (distensione: 20→325 °C in 1 ora, mantenimento 325 °C per 4 ore, raffreddamento a 20 °C). Macchina, fornitore di polvere e parametri di processo non specificati: valori indicativi del produttore ADDITIVA, non generalizzabili.
|
||||
|
||||
## Dati o formule
|
||||
Composizione chimica (% in peso, dato produttore): Al bilancio; Mg 4,0–4,9%; Sc 0,6–0,8%; Mn 0,3–0,8%; Zr 0,2–0,5%; Fe ≤0,4%; Si ≤0,4%; Zn ≤0,25%; Ti ≤0,15%; Cu ≤0,10%.
|
||||
|
||||
Proprietà fisiche: densità relativa ≈99,5%; densità 2,67 g/cm³.
|
||||
|
||||
Dati tecnici: accuratezza dimensionale tipica ±0,2/0,3 mm (quota <150 mm), ±0,05 mm ogni 25 mm (quota ≥150 mm); rugosità superficiale as-built Ra 5–9 µm, dopo lavorazione/lucidatura Ra <1,6 µm.
|
||||
|
||||
Proprietà meccaniche (metodo di prova ASTM E8/E8M, provino non lavorato, asse Z):
|
||||
| Proprietà | As-built | Trattato termicamente |
|
||||
|---|---|---|
|
||||
| Resistenza a trazione Rm | 330 ± 5 MPa | 555 ± 10 MPa |
|
||||
| Snervamento Rp0,2% | 260 ± 5 MPa | 515 ± 10 MPa |
|
||||
| Allungamento a rottura | 19 ± 2% | 14 ± 2% |
|
||||
| Modulo di Young | n.d. | 72 ± 3 GPa |
|
||||
| Durezza Hv10 | n.d. | 160 |
|
||||
| Conducibilità termica (ASTM E1461-13) | n.d. | 95 W/m·K |
|
||||
|
||||
("n.d." = non dichiarato per lo stato as-built nella scheda originale.)
|
||||
|
||||
Confronto qualitativo riportato dal produttore (testo web complementare): a temperatura ambiente Scalmalloy ha resistenza significativamente superiore a quella di AlSi10Mg — **confronto diretto non quantificato nella fonte, riportato come affermazione del produttore**; vedi [[Aluminium AlSi10Mg per SLM-DMLS]] per i valori dell'altra lega.
|
||||
|
||||
Tutti i valori sono dati del produttore, non misure indipendenti: il disclaimer della scheda originale esclude l'uso per specifiche di progettazione o controllo qualità.
|
||||
|
||||
## Esempio
|
||||
Non applicabile (nota di dati di materiale, non caso applicativo documentato).
|
||||
|
||||
## Fonti e collegamenti
|
||||
[[SRC - ADDITIVA - Schede tecniche leghe metalliche per AM]] · [[Aluminium AlSi10Mg per SLM-DMLS]] · [[Leghe Metalliche per AM (Alluminio, Rame, Titanio, Superleghe Inconel)]] · [[Powder Bed Fusion (SLS, SLM, DMLS, EBM)]] · [[Indice - Materiali]]
|
||||
@@ -0,0 +1,46 @@
|
||||
---
|
||||
id: "am-stainless-steel-316l-slm-dmls"
|
||||
title: "Stainless Steel 316L per SLM/DMLS"
|
||||
type: "concetto"
|
||||
status: "da_verificare"
|
||||
created: "2026-09-10"
|
||||
updated: "2026-09-10"
|
||||
language: "it"
|
||||
tags: ["am/concetto", "am/materiale"]
|
||||
aliases: ["Acciaio inossidabile 316L", "AISI 316L", "SS 316L"]
|
||||
sources: ["[[SRC - ADDITIVA - Schede tecniche leghe metalliche per AM]]"]
|
||||
material: "acciaio inossidabile austenitico (316L)"
|
||||
process: "powder bed fusion (SLM/DMLS)"
|
||||
---
|
||||
|
||||
# Stainless Steel 316L per SLM/DMLS
|
||||
|
||||
## In breve
|
||||
L'acciaio inossidabile 316L è una lega austenitica cromo-nichel-molibdeno a basso tenore di carbonio, con alta resistenza alla corrosione, processabile per powder bed fusion metallica (SLM/DMLS). [Fonte: scheda tecnica produttore ADDITIVA; [[SRC - ADDITIVA - Schede tecniche leghe metalliche per AM]]]
|
||||
|
||||
## Spiegazione
|
||||
Il molibdeno conferisce elevata resistenza alla corrosione; il basso tenore di carbonio migliora la resistenza alla corrosione intergranulare e la saldabilità, rendendo generalmente non necessario un trattamento termico post-saldatura. Il produttore dichiara assenza di suscettibilità a corrosione per vaiolatura (pitting) o interstiziale in soluzioni ricche di cloruri. Applicazioni tipiche indicate: prototipi resistenti ad acidi/corrosione e componenti in serie unica o di produzione in automotive, cantieristica navale, aerospaziale, settore alimentare/bevande (tubi e contenitori resistenti alla corrosione), chimico, farmaceutico, oil & gas; esempi applicativi citati nel testo web complementare: collettori di scarico, componenti per forni, scambiatori di calore, parti di motori a getto, attrezzature farmaceutiche/fotografiche, componenti di valvole e pompe, apparecchiature per processi chimici, serbatoi, evaporatori, attrezzature per l'industria della carta/pasta di cellulosa/tessile e parti esposte ad ambienti marini. Lavorabilità post-stampa dichiarata: lavorazione meccanica, saldatura, pallinatura, lucidatura, rivestimento.
|
||||
|
||||
## Condizioni di applicazione
|
||||
Dati riferiti al processo SLM/DMLS, stato "as-built" (la scheda riporta un solo set di valori meccanici, non un confronto as-built/trattato termicamente come per le altre leghe di questa serie). Distensione (stress relief) indicata come opzionale, per parti sensibili a deformazione: 20→550 °C in 3 ore, mantenimento 550 °C per 6 ore, raffreddamento a 20 °C. Macchina, fornitore di polvere e parametri di processo non specificati: valori indicativi del produttore ADDITIVA, non generalizzabili.
|
||||
|
||||
## Dati o formule
|
||||
Composizione chimica (% in peso, dato produttore): Fe bilancio; Cr 16–18%; Ni 11–13%; Mo 2,0–3,0%; Mn ≤2,00%; Si ≤0,75%; Cu ≤0,50%; P ≤0,25%; N ≤0,10%; S ≤0,10%; O ≤0,10%; C ≤0,03%.
|
||||
|
||||
Designazioni citate: UNS S31603; AMS 5507–5653; ASTM A240; DIN 1.4404 – ISO 5832-1 — riportate come nella scheda originale, non verificate singolarmente in questa nota.
|
||||
|
||||
Proprietà fisiche: densità relativa ≈99,9%; densità 7,90 g/cm³.
|
||||
|
||||
Dati tecnici: accuratezza dimensionale tipica ±0,2/0,3 mm (quota <150 mm), ±0,05 mm ogni 25 mm (quota ≥150 mm); rugosità superficiale as-built Ra 5–9 µm, dopo lavorazione/lucidatura Ra <1,6 µm.
|
||||
|
||||
Proprietà meccaniche as-built (metodo di prova ASTM E8/E8M, provino non lavorato, asse Z): resistenza a trazione Rm 640 ± 20 MPa; snervamento Rp0,2% 470 ± 20 MPa; allungamento a rottura 60 ± 10%; modulo di Young 170 ± 20 GPa; durezza (DIN EN ISO 6508-1) 18 HRC.
|
||||
|
||||
Proprietà termiche: temperatura massima di esercizio a lungo termine ≈400 °C (752 °F); conducibilità termica ≈15 W/mK.
|
||||
|
||||
Tutti i valori sono dati del produttore, non misure indipendenti: il disclaimer della scheda originale esclude l'uso per specifiche di progettazione o controllo qualità.
|
||||
|
||||
## Esempio
|
||||
Non applicabile (nota di dati di materiale, non caso applicativo documentato).
|
||||
|
||||
## Fonti e collegamenti
|
||||
[[SRC - ADDITIVA - Schede tecniche leghe metalliche per AM]] · [[Leghe Metalliche per AM (Alluminio, Rame, Titanio, Superleghe Inconel)]] · [[Powder Bed Fusion (SLS, SLM, DMLS, EBM)]] · [[Indice - Materiali]]
|
||||
@@ -0,0 +1,53 @@
|
||||
---
|
||||
id: "am-titanium-ti6al4v-grado23-slm-dmls"
|
||||
title: "Titanium Ti6Al4V (Grado 23) per SLM/DMLS"
|
||||
type: "concetto"
|
||||
status: "da_verificare"
|
||||
created: "2026-09-10"
|
||||
updated: "2026-09-10"
|
||||
language: "it"
|
||||
tags: ["am/concetto", "am/materiale"]
|
||||
aliases: ["Ti6Al4V", "Ti-6Al-4V ELI", "Titanio Grado 23"]
|
||||
sources: ["[[SRC - ADDITIVA - Schede tecniche leghe metalliche per AM]]"]
|
||||
material: "lega di titanio Ti6Al4V, Grado 23 (ELI)"
|
||||
process: "powder bed fusion (SLM/DMLS)"
|
||||
---
|
||||
|
||||
# Titanium Ti6Al4V (Grado 23) per SLM/DMLS
|
||||
|
||||
## In breve
|
||||
Ti6Al4V è una lega di titanio leggera con elevate proprietà meccaniche (tenacità a frattura, resistenza a fatica, resistenza alla corrosione), bassa densità specifica e biocompatibilità, processabile per powder bed fusion metallica (SLM/DMLS). La scheda si riferisce al Grado 23 (variante ELI, extra-low interstitials). [Fonte: scheda tecnica produttore ADDITIVA; [[SRC - ADDITIVA - Schede tecniche leghe metalliche per AM]]]
|
||||
|
||||
## Spiegazione
|
||||
Il Grado 23 si differenzia dal Grado 5 principalmente per il tenore di ossigeno ridotto (massimo 0,13%), che migliora duttilità e tenacità a frattura a fronte di una lieve riduzione di resistenza. Applicazioni tipiche indicate: strutture aeronautiche critiche per frattura, componenti leggeri per motorsport e aerospaziale, impianti chirurgici e strumentazione medicale; il testo web complementare aggiunge: componenti a bassa/alta temperatura, fissaggi, dischi, mozzi, distanziali, tenute, pale di compressore, parti strutturali e componenti complessi di motori a turbina. Lavorabilità post-stampa dichiarata: lavorazione meccanica, saldatura, pallinatura, lucidatura, rivestimento.
|
||||
|
||||
## Condizioni di applicazione
|
||||
Dati riferiti al processo SLM/DMLS, stato "as-built" o trattato termicamente (ricottura sotto atmosfera di argon: 20→750 °C in 4 ore, mantenimento 750 °C per 1 ora, raffreddamento a 20 °C). Macchina, fornitore di polvere e parametri di processo non specificati: valori indicativi del produttore ADDITIVA, non generalizzabili.
|
||||
|
||||
## Dati o formule
|
||||
Composizione chimica (% in peso, dato produttore): Ti bilancio; Al 5,5–6,8%; V 3,5–4,5%; Fe ≤0,25%; O ≤0,13%; C ≤0,08%; N ≤0,05%; H ≤0,012%.
|
||||
|
||||
Designazioni citate: UNS R56401; AMS 4956; ASTM B348 Grade 23; DIN EN 3.7164 – ISO 5832-3 — riportate come nella scheda originale, non verificate singolarmente in questa nota.
|
||||
|
||||
Proprietà fisiche: densità relativa ≈99,9%; densità 4,43 g/cm³.
|
||||
|
||||
Dati tecnici: accuratezza dimensionale tipica ±0,2/0,3 mm (quota <150 mm), ±0,05 mm ogni 25 mm (quota ≥150 mm); rugosità superficiale as-built Ra 5–9 µm, dopo lavorazione/lucidatura Ra <1,6 µm.
|
||||
|
||||
Proprietà meccaniche (metodo di prova ASTM E8/E8M, provino non lavorato, asse Z):
|
||||
| Proprietà | As-built | Trattato termicamente |
|
||||
|---|---|---|
|
||||
| Resistenza a trazione Rm | 1180 ± 30 MPa | 1100 ± 20 MPa |
|
||||
| Snervamento Rp0,2% | 1080 ± 30 MPa | 1060 ± 20 MPa |
|
||||
| Allungamento a rottura | 7 ± 1% | 12 ± 1% |
|
||||
| Modulo di Young | 110 ± 3 GPa | 120 ± 5 GPa |
|
||||
| Durezza (DIN EN ISO 6508-1) | 37 HRC | 37 HRC |
|
||||
|
||||
Proprietà termiche: temperatura massima di esercizio a lungo termine ≈355 °C (670 °F); conducibilità termica 7 W/mK.
|
||||
|
||||
Tutti i valori sono dati del produttore, non misure indipendenti: il disclaimer della scheda originale esclude l'uso per specifiche di progettazione o controllo qualità.
|
||||
|
||||
## Esempio
|
||||
Non applicabile (nota di dati di materiale, non caso applicativo documentato).
|
||||
|
||||
## Fonti e collegamenti
|
||||
[[SRC - ADDITIVA - Schede tecniche leghe metalliche per AM]] · [[Leghe Metalliche per AM (Alluminio, Rame, Titanio, Superleghe Inconel)]] · [[Powder Bed Fusion (SLS, SLM, DMLS, EBM)]] · [[Indice - Materiali]]
|
||||
@@ -15,6 +15,8 @@ sources: []
|
||||
|
||||
- [[SRC - NIST - What is Additive Manufacturing]]
|
||||
- [[SRC - freeCodeCamp GaugeHow - 3D Printing and Additive Manufacturing Full Course]]
|
||||
- [[SRC - Zhou et al. 2024 - Additive Manufacturing A Comprehensive Review]]
|
||||
- [[SRC - ADDITIVA - Schede tecniche leghe metalliche per AM]]
|
||||
|
||||
Aggiungi ogni nuova scheda fonte qui. Usa [[Modello - Fonte]].
|
||||
|
||||
|
||||
@@ -0,0 +1,46 @@
|
||||
---
|
||||
id: "am-src-additiva-schede-tecniche-leghe-metalliche"
|
||||
title: "ADDITIVA — Schede tecniche leghe metalliche per manifattura additiva (SLM/DMLS)"
|
||||
type: "fonte"
|
||||
status: "da_verificare"
|
||||
created: "2026-09-10"
|
||||
updated: "2026-09-10"
|
||||
language: "it"
|
||||
tags: ["am/fonte"]
|
||||
aliases: ["ADDITIVA datasheet", "ADDITIVA material data sheet"]
|
||||
sources: []
|
||||
accessed: "2026-09-10"
|
||||
---
|
||||
|
||||
# ADDITIVA — Schede tecniche leghe metalliche per manifattura additiva (SLM/DMLS)
|
||||
|
||||
## Riferimento bibliografico
|
||||
- Ente/produttore: ADDITIVA (servizio di manifattura additiva metallica; ragione sociale completa e sito web non acquisiti in questo clip — **da verificare**).
|
||||
- Tipo di documento: schede tecniche materiale ("data sheet"), una per lega, in formato PDF (originariamente .docx secondo il nome file incorporato nel testo, es. `ADDITIVA_Aluminium AlSi10Mg_rev010.docx`), con numero di revisione.
|
||||
- Documenti acquisiti (5 leghe, ciascuna con numero di revisione proprio e allegato conservato in `90 Allegati`, non modificare gli originali):
|
||||
1. Aluminium AlSi10Mg — rev. 010 — [[90 Allegati/ADDITIVA_Aluminium AlSi10Mg_rev010.pdf|ADDITIVA_Aluminium AlSi10Mg_rev010.pdf]] + [[90 Allegati/ADDITIVA_Aluminium AlSi10Mg_web|ADDITIVA_Aluminium AlSi10Mg_web]] (testo pagina web complementare)
|
||||
2. INCONEL 718 — rev. 006 — [[90 Allegati/ADDITIVA_INCONEL718_rev006.pdf|ADDITIVA_INCONEL718_rev006.pdf]] + [[90 Allegati/ADDITIVA_Inconel 718_web|ADDITIVA_Inconel 718_web]]
|
||||
3. Scalmalloy — rev. 005 — [[90 Allegati/ADDITIVA_Scalmalloy_rev005.pdf|ADDITIVA_Scalmalloy_rev005.pdf]] + [[90 Allegati/ADDITIVA_Scalmalloy_web|ADDITIVA_Scalmalloy_web]]
|
||||
4. Stainless Steel 316L — rev. 006 — [[90 Allegati/ADDITIVA_Stainless Steel 316L_rev006.pdf|ADDITIVA_Stainless Steel 316L_rev006.pdf]] + [[90 Allegati/ADDITIVA_Stainless Steel 316L_web|ADDITIVA_Stainless Steel 316L_web]]
|
||||
5. Titanium Ti6Al4V — rev. 009 — [[90 Allegati/ADDITIVA_Titanium Ti6Al4V_rev009.pdf|ADDITIVA_Titanium Ti6Al4V_rev009.pdf]] + [[90 Allegati/ADDITIVA_Titanium Ti6Al4V_web|ADDITIVA_Titanium Ti6Al4V_web]]
|
||||
- Processo di riferimento dichiarato nelle schede: SLM/DMLS (selective laser melting / direct metal laser sintering), powder bed fusion metallica.
|
||||
- Accesso: 2026-09-10, tramite Obsidian Web Clipper. **Il link di download presente in ciascun clip è un URL S3 firmato con scadenza (pochi minuti): non utilizzabile come riferimento stabile e già scaduto al momento della lettura.** Non è stata acquisita la URL pubblica del sito ADDITIVA né il PDF originale in locale — **da recuperare per una citazione stabile** (salvare il PDF in `90 Allegati` o annotare la URL pubblica della pagina/documento).
|
||||
- Ogni scheda include, oltre ai dati del PDF ufficiale, un breve testo descrittivo aggiuntivo (probabilmente dalla pagina web del prodotto ADDITIVA, stesso materiale, nessuna URL propria acquisita), usato come fonte complementare per le applicazioni tipiche.
|
||||
|
||||
## Ambito e qualità della fonte
|
||||
Scheda tecnica di produttore/service bureau di manifattura additiva: fonte di parte (il produttore descrive i propri materiali/processi), non peer-reviewed né indipendente. Contiene però dati quantitativi con metodo di prova dichiarato (es. ASTM E8/E8M, ISO 6892-1, DIN EN ISO 6506-1/6508-1, ASTM E1461-13), quindi più utile di una fonte puramente divulgativa per proprietà meccaniche indicative — ma va trattata come dato del produttore, non come misura indipendente o valore di norma. Ogni scheda include un disclaimer esplicito del produttore: "This data sheet contains approximate values that may vary with build conditions [...] should not be used for design specifications or quality control" — vincolo da rispettare in ogni nota derivata.
|
||||
|
||||
## Sezioni lette e localizzatori
|
||||
Testo integrale di ciascuna scheda (1 pagina per materiale). Localizzatore usato nelle note derivate: nome del materiale (una sola pagina per scheda, non servono ulteriori riferimenti di pagina).
|
||||
|
||||
## Risultati utili e limiti
|
||||
Dati utili per ciascuna lega: composizione chimica (intervalli %), proprietà fisiche (densità, densità relativa), trattamento termico dichiarato (stress relief o tempra/invecchiamento secondo norma), accuratezza dimensionale tipica, rugosità superficiale (as-built e dopo lavorazione), proprietà meccaniche in stato as-built e trattato termicamente (resistenza a trazione, snervamento, allungamento a rottura, modulo di Young, durezza), conducibilità termica, temperatura massima di esercizio.
|
||||
|
||||
Limiti:
|
||||
- Nessuna informazione sulla macchina specifica, sui parametri di processo (potenza laser, velocità di scansione, spessore layer) né sul lotto di polvere: i valori vanno considerati indicativi del produttore, non generalizzabili ad altre macchine/fornitori di polvere.
|
||||
- Il disclaimer del produttore esclude esplicitamente l'uso di questi dati per specifiche di progettazione o controllo qualità.
|
||||
- Origine/identità legale di ADDITIVA non verificata in questa scheda.
|
||||
- Le due fonti per materiale (PDF ufficiale + testo web complementare) potrebbero provenire da versioni/revisioni diverse del contenuto del produttore: eventuali discrepanze sono segnalate nelle note derivate.
|
||||
|
||||
## Elaborazioni collegate
|
||||
[[Aluminium AlSi10Mg per SLM-DMLS]] · [[Inconel 718 per SLM-DMLS]] · [[Scalmalloy per SLM-DMLS]] · [[Stainless Steel 316L per SLM-DMLS]] · [[Titanium Ti6Al4V (Grado 23) per SLM-DMLS]]
|
||||
@@ -0,0 +1,50 @@
|
||||
---
|
||||
id: "am-src-zhou-2024-comprehensive-review"
|
||||
title: "Zhou et al. (2024) — Additive Manufacturing: A Comprehensive Review"
|
||||
type: "fonte"
|
||||
status: "da_verificare"
|
||||
created: "2026-09-10"
|
||||
updated: "2026-09-10"
|
||||
language: "it"
|
||||
tags: ["am/fonte"]
|
||||
aliases: ["Zhou 2024", "Comprehensive Review Sensors 2024"]
|
||||
sources: []
|
||||
doi: "10.3390/s24092668"
|
||||
url: "https://doi.org/10.3390/s24092668"
|
||||
accessed: "2026-09-10"
|
||||
edition: "Sensors 2024, 24, 2668"
|
||||
---
|
||||
|
||||
# Zhou et al. (2024) — Additive Manufacturing: A Comprehensive Review
|
||||
|
||||
## Riferimento bibliografico
|
||||
- Autori: Longfei Zhou, Jenna Miller, Jeremiah Vezza, Maksim Mayster, Muhammad Raffay, Quentin Justice, Zainab Al Tamimi, Gavyn Hansotte, Lavanya Devi Sunkara, Jessica Bernat.
|
||||
- Affiliazione: Department of Biomedical, Industrial and Systems Engineering, School of Engineering and Computing, Gannon University, Erie, PA, USA.
|
||||
- Titolo: "Additive Manufacturing: A Comprehensive Review".
|
||||
- Rivista: *Sensors* 2024, 24(9), 2668. Articolo di tipo Review.
|
||||
- DOI: https://doi.org/10.3390/s24092668
|
||||
- Editore: MDPI, Basel, Svizzera. Licenza: Creative Commons Attribution (CC BY 4.0), open access.
|
||||
- Ricevuto: 1 marzo 2024; revisionato: 19 aprile 2024; accettato: 20 aprile 2024; pubblicato: 23 aprile 2024.
|
||||
- Data di accesso: 2026-09-10, tramite ResearchGate (pagina articolo con testo integrale disponibile).
|
||||
- Allegato: estratto testuale integrale (Obsidian Web Clipper dalla pagina ResearchGate) conservato in [[90 Allegati/(PDF) Additive Manufacturing_ A Comprehensive Review|(PDF) Additive Manufacturing_ A Comprehensive Review]]; non modificare l'originale. Non è il PDF impaginato originale, solo il testo estratto. **Il link di download presente nel clip è un URL firmato temporaneo (scaduto): non utilizzabile come riferimento stabile.** Riferimento stabile da usare: il DOI sopra indicato.
|
||||
|
||||
## Ambito e qualità della fonte
|
||||
Articolo di rassegna (review) peer-reviewed, pubblicato su rivista indicizzata (MDPI *Sensors*), con bibliografia numerata e affiliazione accademica verificabile. Qualità nettamente superiore rispetto a fonti divulgative (es. corsi video): utilizzabile come riferimento primario per definizioni, classificazioni di processo e confronti tecnologici, fermo restando che è comunque una fonte secondaria (sintesi della letteratura) e non riporta dati sperimentali originali degli autori.
|
||||
|
||||
## Sezioni lette e localizzatori
|
||||
Testo integrale (44 pagine, numerate "Sensors 2024, 24, 2668 X of 44" nel testo estratto). Struttura dell'articolo:
|
||||
1. Introduzione (§1).
|
||||
2. Processo di manifattura additiva — flusso di lavoro: design e modellazione (§2.1), conversione in STL (§2.2), slicing (§2.3), preparazione/stampa/post-processing (§2.4).
|
||||
3. Tecnologie di manifattura additiva (§3), con tabella comparativa (Table 1) e sottosezioni dedicate: Material Extrusion (§3.1), VAT Polymerization (§3.2), Material Jetting (§3.3), Binder Jetting (§3.4), Selective Laser Sintering (§3.5), Selective Laser Melting (§3.6), Direct Metal Laser Sintering (§3.7), Electron Beam Melting (§3.8), Multi-Jet Fusion (§3.9), Direct Energy Deposition (§3.10), Carbon Fiber Reinforcement (§3.11), Laminated Object Manufacturing (§3.12).
|
||||
4. Tendenze future e sfide (§4): 3D bioprinting (§4.1), 3D food printing (§4.2), stampa 3D su larga scala (§4.3), 4D printing (§4.4), AM basata su IA (§4.5), innovazioni in materiali/controllo qualità/post-processing (§4.6), standardizzazione e regolamentazione (§4.7), economia circolare e sostenibilità (§4.8).
|
||||
5. Conclusioni (§5).
|
||||
|
||||
Localizzatori usati nelle note derivate: `[§X.Y]` per la sezione, con eventuale numero di pagina "X of 44" quando disponibile.
|
||||
|
||||
## Risultati utili e limiti
|
||||
Fonte di alta qualità per: classificazione delle tecnologie AM (12 famiglie/varianti trattate, più dettagliata della classificazione ASTM a 7 famiglie usata nel corso video già presente nel vault), confronto sistematico vantaggi/limiti/materiali per tecnologia (Table 1, §3), flusso di lavoro CAD→STL→slicing→stampa→post-processing, e panoramica delle tendenze emergenti (bioprinting, food printing, stampa su larga scala, 4D printing, AM basata su IA) assente nella fonte video già processata.
|
||||
|
||||
Limiti: è una review, quindi le affermazioni tecniche derivano da fonti terze citate con numero (es. `[3]`, `[124]`) che non sono state verificate singolarmente in questa scheda — i riferimenti numerici citati nelle note derivate vanno intesi come "citati da Zhou et al." e non come verifica diretta della fonte primaria originale. Non riporta dati sperimentali quantitativi propri (es. proprietà meccaniche misurate); per questi vedere le schede fonte dei produttori/datasheet (es. [[SRC - ADDITIVA - Schede tecniche leghe metalliche per AM]]).
|
||||
|
||||
## Elaborazioni collegate
|
||||
[[RIA - Zhou et al. 2024 - Additive Manufacturing A Comprehensive Review]]
|
||||
@@ -14,6 +14,7 @@ sources: []
|
||||
# Indice riassunti
|
||||
|
||||
- [[RIA - freeCodeCamp GaugeHow - 3D Printing and Additive Manufacturing Full Course]]
|
||||
- [[RIA - Zhou et al. 2024 - Additive Manufacturing A Comprehensive Review]]
|
||||
|
||||
Usa [[Modello - Riassunto]] e collega la scheda fonte per ogni nuovo riassunto.
|
||||
|
||||
|
||||
+43
@@ -0,0 +1,43 @@
|
||||
---
|
||||
id: "am-ria-zhou-2024-comprehensive-review"
|
||||
title: "Riassunto — Zhou et al. (2024), Additive Manufacturing: A Comprehensive Review"
|
||||
type: "riassunto"
|
||||
status: "da_verificare"
|
||||
created: "2026-09-10"
|
||||
updated: "2026-09-10"
|
||||
language: "it"
|
||||
tags: ["am/riassunto"]
|
||||
aliases: []
|
||||
sources: ["[[SRC - Zhou et al. 2024 - Additive Manufacturing A Comprehensive Review]]"]
|
||||
---
|
||||
|
||||
# Riassunto — Zhou et al. (2024), Additive Manufacturing: A Comprehensive Review
|
||||
|
||||
## Fonte e copertura
|
||||
[[SRC - Zhou et al. 2024 - Additive Manufacturing A Comprehensive Review]]. Articolo di rassegna peer-reviewed, testo integrale letto (44 pagine).
|
||||
|
||||
## Sintesi
|
||||
La rassegna definisce l'AM come tecnologia matura, passata da strumento di prototipazione rapida (anni '80) a metodo di produzione a pieno titolo, applicabile a polimeri, metalli, ceramiche e compositi. Descrive il flusso di lavoro generale (progettazione CAD → conversione STL → slicing/G-code → stampa e post-processing), poi tratta 12 tecnologie/varianti AM con principio di funzionamento, vantaggi, limiti, materiali tipici e applicazioni, per poi chiudere con una panoramica di tendenze emergenti e temi trasversali (bioprinting, food printing, stampa su larga scala, 4D printing, AM basata su IA, innovazioni di materiali/qualità/post-processing, standardizzazione, economia circolare).
|
||||
|
||||
## Metodo e contesto
|
||||
Rassegna della letteratura (review paper), non uno studio sperimentale: sintetizza e cita fonti terze numerate. Utile come riferimento strutturale e per la classificazione tecnologica, meno utile per dati quantitativi di proprietà dei materiali (per cui servono datasheet di produttore o norme).
|
||||
|
||||
## Risultati principali
|
||||
- **Flusso AM** in 5 fasi: design/modellazione CAD, conversione a STL (triangolazione, requisito di modello "watertight"/manifold), slicing (generazione G-code, parametri di stampa: altezza layer, densità di riempimento, supporti, velocità), stampa e post-processing (rimozione supporti, finitura superficiale, cura UV per resine, trattamenti termici per metalli). [§2.1–§2.4]
|
||||
- **Confronto sistematico di 12 tecnologie AM** (Table 1, §3): FDM, VAT Polymerization (VP), Material Jetting (MJ), Binder Jetting (BJ), Selective Laser Sintering (SLS), Selective Laser Melting (SLM), Direct Metal Laser Sintering (DMLS), Electron Beam Melting (EBM), Multi-Jet Fusion (MJF), Direct Energy Deposition (DED), Carbon Fiber Reinforcement (CFR), Laminated Object Manufacturing (LOM) — ciascuna con vantaggi, limiti e materiali comuni sintetizzati in tabella. Classificazione più granulare (12 voci) di quella ASTM a 7 famiglie usata nella fonte video già presente nel vault ([[AM - Classificazione ASTM per i processi di stampa 3D]]); utile per un confronto incrociato.
|
||||
- **Tendenze future** (§4): bioprinting 3D di tessuti/organi (bioinchiostri, vascolarizzazione), food printing 3D (sfide reologiche dei materiali alimentari), stampa su larga scala (edilizia, componenti aerospaziali di grandi dimensioni), 4D printing (materiali intelligenti, leghe a memoria di forma come nichel-titanio), AM basata su intelligenza artificiale (monitoraggio in tempo reale, digital twin, manutenzione predittiva), innovazioni di materiali/multimateriale/ibridazione con sottrattiva, standardizzazione e regolamentazione (assenza di standard universalmente accettati, criticità per settori regolamentati come aerospaziale/medicale), economia circolare e sostenibilità.
|
||||
- **Considerazioni economiche** (§4.8): ROI dell'AM variabile per tecnologia e settore — FDM per prototipazione a basso costo, SLS/DMLS per componenti funzionali finali a più alto valore, SLA/MJ per parti ad alto dettaglio (es. dentale/medicale); ROI più marcato in aerospaziale e medicale, dove il costo del fallimento è alto e il valore della personalizzazione è significativo.
|
||||
|
||||
## Limiti e questioni aperte
|
||||
- Le affermazioni tecniche della rassegna derivano da fonti terze citate con numero (es. `[3]`, `[124]`), non verificate singolarmente in questa scheda: da trattare come "riportato da Zhou et al. (2024)", non come fatto verificato alla fonte primaria originale.
|
||||
- Nessun dato quantitativo di proprietà meccaniche misurate: per questo servono datasheet di produttore (vedi [[SRC - ADDITIVA - Schede tecniche leghe metalliche per AM]]) o norme.
|
||||
- Il link di accesso originale (ResearchGate, download firmato temporaneo) non è una URL stabile: usare il DOI per citazioni future.
|
||||
|
||||
## Note da ricavare
|
||||
La rassegna offre materiale sufficiente per arricchire con citazioni verificabili le note di concetto già presenti nel vault (derivate dalla fonte video, marcate `da_verificare`), in particolare:
|
||||
- [[AM - Classificazione ASTM per i processi di stampa 3D]]: incrociare con la classificazione a 12 voci di Table 1 (§3).
|
||||
- [[Flusso di lavoro e formati file per la stampa 3D]]: incrociare con §2.1–§2.4 (requisiti STL, ruolo dello slicing).
|
||||
- Note tecnologiche in `02 Processi/`: aggiungere citazione a vantaggi/limiti/materiali di Table 1 per ciascuna famiglia di processo.
|
||||
- Nuove note pianificate (non derivabili dalle fonti già presenti nel vault): 3D bioprinting, 4D printing e leghe a memoria di forma, AM basata su intelligenza artificiale/digital twin, stampa 3D su larga scala — da collocare rispettivamente in `01 Fondamenti` o in una futura sottosezione di `02 Processi`/`08 Applicazioni ed economia` a seconda dello sviluppo del vault.
|
||||
|
||||
[[Indice riassunti]]
|
||||
File diff suppressed because it is too large
Load Diff
@@ -0,0 +1,51 @@
|
||||
[Download](https://presentations-decks-uploads-prod.s3.amazonaws.com/7403838/3888537/5e2dce5faba1a8500f30c5dafc639e14e28d093eade06720d37f6c08e055c4c5.pdf?X-Amz-Algorithm=AWS4-HMAC-SHA256&X-Amz-Date=20260910T072618Z&X-Amz-SignedHeaders=host&X-Amz-Expires=60&X-Amz-Credential=AKIAZ32RUKUMSNCVYAKB%2F20260910%2Fus-east-1%2Fs3%2Faws4_request&X-Amz-Signature=9cd4cf230f73e325ba058cf47282725825a2fb61c4faea6f24ad0f75d6315ae8)
|
||||
|
||||
This data sheet contains approximate values that may vary with build conditions and is intended for reference and comparison purposes only. It should not be used for
|
||||
design specifications or quality control. The performance characteristics of the material can be affected (±) by, but not limited to, part design, part geometries,
|
||||
application and operating conditions. Each user is responsible for determining that the material is safe, lawful and technica lly suitable for the intended laws and
|
||||
regulations. ADDIT IVA makes no warranties of any kind, express or implied, including, but not limited to, the warranties of merchantability, fi tness for a particular use, or
|
||||
warranty against patent infringement. ADDITIVA excludes liability, however arising, for any inaccura cies in this document.
|
||||
ADDITIVA\_Aluminium AlSi10Mg\_rev010.docx 9
|
||||
Aluminium AlSi10Mg is a common casting alloy with good castability. It is typically used for thin \- walled, complex
|
||||
components and applications requiring a combination of good thermal properties and low weight. It offers excellent
|
||||
strength, hardness, and dyn amic performance, making it suitable for parts subjected to high loads. Traditionally, cast
|
||||
parts made from this aluminium alloy are heat \- treated to enhance mechanical properties, typically via the T6 cycle of
|
||||
solution annealing, quenching, and age hardeni ng.
|
||||
The SLM/DMLS process is notable for its extremely rapid melting and re \- solidification, allowing mechanical properties
|
||||
in the as \- built condition to be comparable to those of T6 heat \- treated cast parts. Thanks to its high strength \- to \- weight
|
||||
ratio, AlSi10Mg i s an excellent choice for automotive and aerospace applications, especially gearboxes, housings, and
|
||||
brackets that endure significant loading. Components can be machined, spark \- eroded, welded, shot \- peened, polished,
|
||||
and coated.
|
||||
USA UNS European Union / EN ASTM DIN
|
||||
A0 3600 – A13600 EN AC \- 430 00 B 85 A360.0 (F3318) Al 4046 \- 3.2381
|
||||
Chemical composition Physical properties
|
||||
Al – Aluminium balance Relative density Approx. 99.9%
|
||||
Si – Silicon 9.0÷11.0% Density 2.67 g/cm 3
|
||||
Mg – Magnesium 0.20÷0.45%
|
||||
Fe – Iron ≤ 0.55% Heat Treatment (stress relief)
|
||||
Mn – Manganese ≤ 0.45% 20°C → 300 °C 1 hour
|
||||
Ti – Titanium ≤ 0.15% 300 °C 2 hours
|
||||
Cu – Copper ≤ 0.10% 300 °C → 20°C \-
|
||||
Zn – Zinc ≤ 0.10%
|
||||
Ni – Nickel ≤ 0.05%
|
||||
C – Carbon ≤ 0.05%
|
||||
Technical data
|
||||
Typical part accuracy (quote < 150 mm) ± 0.2/0.3 mm
|
||||
Typical part accuracy (quote ≥ 150 mm) ± 0.05mm each 25mm
|
||||
Surface roughness (as built) Ra: 5 ÷ 9 µm
|
||||
Surface roughness (after machining / polishing) Ra < 1.6 µm
|
||||
Mechanical properties
|
||||
Mechanical data Test method As Built Stress relieved
|
||||
Tensile strenght (Rm)
|
||||
ASTM E8 / E8M
|
||||
(unmachined specimen, Z \- axis)
|
||||
4 0 0 ± 5 MPa 2 70 ± 5 MPa
|
||||
Yield strenght (Rp 0.2%) 2 55 ± 5 MPa 1 60 ± 5 MPa
|
||||
Elongation at break 4,5 ± 1 % 11 ± 1 %
|
||||
Young’s modulus 70 ± 3 GPa 70 ± 3 GPa
|
||||
Hardness Brinell DIN EN ISO 6506 \- 1 120 ± 5 HBW
|
||||
Thermal conductivity ASTM E1461 \- 13 110 ± 5 W/m°C 170 ± 10 W/m°C
|
||||
|
||||
Pagina 1 di 1
|
||||
|
||||
|
||||
@@ -0,0 +1,7 @@
|
||||
AlSi10Mg is an aluminium-based alloy widely used for functional parts as well as prototypes. It offers good corrosion resistance, good electrical conductivity, high dynamic toughness, excellent thermal conductivity.
|
||||
|
||||
Conventionally cast parts in this type of aluminium alloy are often heat-treated to improve the mechanical properties, for example, applying the T6 cycle of solution annealing, quenching and age hardening. The SLM / DMLS process is characterised by extremely rapid melting and solidification: this enables mechanical properties in the as-built condition similar to T6 heat-treated cast parts.
|
||||
|
||||
Due to its high strength-to-weight ratio, AlSi10Mg is a good choice for automotive, aerospace and automation applications, notably gearboxes, engine parts, ductwork, heat exchangers, high-pressure pipes, manifolds, housings and brackets subject to high loading.
|
||||
|
||||
Parts can be machined, spark-eroded, welded, micro shot-peened, polished and coated.
|
||||
@@ -0,0 +1,53 @@
|
||||
[Download](https://presentations-decks-uploads-prod.s3.amazonaws.com/7403838/3888537/12414a9d77c0e8922332cee99c8836e36d7746ccda751d87f542742c6a6e80bf.pdf?X-Amz-Algorithm=AWS4-HMAC-SHA256&X-Amz-Date=20260910T074626Z&X-Amz-SignedHeaders=host&X-Amz-Expires=60&X-Amz-Credential=AKIAZ32RUKUMSNCVYAKB%2F20260910%2Fus-east-1%2Fs3%2Faws4_request&X-Amz-Signature=d38ee3ee79ae440a58c93667816572b64134f9419059e2abe0f290894ab91842)
|
||||
|
||||
This data sheet contains approximate values that may vary with build conditions and is intended for reference and comparison purposes only. It should not be used for
|
||||
design specifications or quality control. The performance characteristics of the material can be affected (±) by, but are not limited to, part design, part geometries,
|
||||
application and operating conditions. Each user is responsible for determining that the material is safe, lawful and technica lly suitable for the intended laws and
|
||||
regulations. A DDITIVA makes no warranties of any kind, express or implied, including, but not limited to, the warranties of merchantability, fitness for a particular use, or
|
||||
warranty against patent infringement. ADDITIVA excludes liability, however arising, for any inac curacies in this document.
|
||||
ADDITIVA\_INCONEL718\_rev006.docx
|
||||
INCONEL® alloy 718 is a high \- strength, corrosion \- resistant nickel \- chromium material. Similar to its sister alloy 625,
|
||||
Inconel 718 is an age \- hardened version of alloy 625. Ageing (or precipitation hardening) produces precipitates within
|
||||
the microstructure t hat pin the metal's grains in place. As a result, the material typically becomes significantly
|
||||
stronger. Service temperatures range from \- 196°C to 700°C (\- 321°F to 1.300°F). Its welding characteristics, especially
|
||||
its resistance to post \- weld cracking, are outstanding. Good tensile, fatigue, creep, and rupture strengths have led to its
|
||||
use in a wide range of applications. The alloy is utilised in jet engines, liquid \- fuelled rockets, rings, casings, and metal
|
||||
parts for aircraft and land \- based gas turbine engi nes, cryogenic tankage, and high \- temperature fasteners. INCONEL
|
||||
718 is also employed in the oil and gas drilling and production industries due to its high strength and resistance to
|
||||
chlorides, stress corrosion, and sulphide stress cracking. Parts can be ma chined, welded, shot \- peened, polished, and
|
||||
coated.
|
||||
UNS AMS ASTM DIN
|
||||
N07718 5596 \- 5832 B670 – F3055 2.4668
|
||||
Chemical composition Physical properties
|
||||
Ni – Nickel 50.0÷55.0% Relative density Approx. 99.9%
|
||||
Cr – Chromium 17.0÷21.0% Density 8.15 g/cm 3
|
||||
Nb – Niobium 4.7÷5.5% Heat Treatment (AMS 5662)
|
||||
Mo – Molybdenum 2.8÷3.3% STEP 1 – Annealing
|
||||
Ti – Titanium 0.6÷1.2% 20°C → 980°C \-
|
||||
Al – Aluminium 0.2÷0.8% 980°C 1 hour
|
||||
Co – Cobalt ≤ 1.0% 980°C → 20°C \-
|
||||
Cu – Copper ≤ 0.3% STEP 2 – Ageing
|
||||
C – Carbon ≤ 0.08% 20°C → 720°C \-
|
||||
Mn – Manganese ≤ 0.35% 720°C 8 hours
|
||||
Si – Silicon ≤ 0.35% 720°C → 620°C 2 hours
|
||||
P – Phosphorus ≤ 0.015% 620°C 10 hours
|
||||
S – Sulfur ≤ 0.015% 620°C → 20°C \-
|
||||
Technical data
|
||||
Typical part accuracy (quote < 150 mm) ± 0.2/0.3 mm
|
||||
Typical part accuracy (quote ≥ 150 mm) ± 0.05mm each 25mm
|
||||
Surface roughness (as built) Ra: 5 ÷ 9 µm
|
||||
Surface roughness (after machining / polishing) Ra < 1.6 µm
|
||||
Mechanical properties
|
||||
Mechanical data Test method As Built Heat Treated AMS 5662
|
||||
Tensile strenght ISO 6892 \- 1:2009(B) Annex D 1020 ± 15 MPa 1.400 ± 15 MPa
|
||||
Yield strenght (Rp 0.2%) ISO 6892 \- 1:2009(B) Annex D 630 ± 15 MPa 1.1 4 0 ± 15 MPa
|
||||
Elongation at break ISO 6892 \- 1:2009(B) Annex D 30 ± 5 % 10 ± 2%
|
||||
Young’s modulus 1 85 ± 1 0 GPa 210 ± 1 0 GPa
|
||||
Hardness DIN EN ISO 6508 \- 1 30 HRC 46 HRC
|
||||
Thermal properties
|
||||
Maximum long \- term operating temperature Approx. 700°C / 1.300 °F
|
||||
Thermal conductivity 6 ÷ 12 W/mK
|
||||
|
||||
Pagina 1 di 1
|
||||
|
||||
|
||||
@@ -0,0 +1,3 @@
|
||||
INCONEL® alloy 718 is a high-strength, corrosion-resistant Nickel-Chromium material. Service temperatures range from -196°C to 700°C (-321°F÷1.300°F).
|
||||
|
||||
Its welding characteristics, especially its resistance to post-weld cracking, are outstanding. Good tensile, fatigue, creep and rupture strengths enable its use in a wide range of applications. The alloy is used in jet engines, liquid-fueled rockets, rings, casings and metal parts for aircraft and land-based gas turbine engines, cryogenic tankage, high-temperature fasteners. Inconel 718 is also used in the oil and gas drilling and production industries due to its high strength and resistance to chlorides, stress corrosion and sulfide stress cracking. Parts can be machined, welded, shot-peened, polished and coated.
|
||||
@@ -0,0 +1,51 @@
|
||||
[Download](https://presentations-decks-uploads-prod.s3.amazonaws.com/7403838/3888537/015f9cccb16a040bbe73d9165683ae703829853f3adb06aa6caa84933942c279.pdf?X-Amz-Algorithm=AWS4-HMAC-SHA256&X-Amz-Date=20260910T074528Z&X-Amz-SignedHeaders=host&X-Amz-Expires=60&X-Amz-Credential=AKIAZ32RUKUMSNCVYAKB%2F20260910%2Fus-east-1%2Fs3%2Faws4_request&X-Amz-Signature=b5380a5416d932e91fed1229d5d9c2b262541eb248cfcdcc0aa8e78640e3a799)
|
||||
|
||||
This data sheet contains approximate values that may vary with build conditions and is intended for reference and comparison purposes only. It should not be used for
|
||||
design specifications or quality control. The performance characteristics of the material can be affected (±) by, but not limited to, part design, part geometries,
|
||||
application and operating conditions. Each user is responsible for determining that the material is safe, lawful and technica lly suitable for the intended laws and
|
||||
regulations. ADDIT IVA makes no warranties of any kind, express or implied, including, but not limited to, the warranties of merchantability, fi tness for a particular use, or
|
||||
warranty against patent infringement. ADDITIVA excludes liability, however arising, for any inaccura cies in this document.
|
||||
ADDITIVA\_Scalmalloy\_rev005.docx
|
||||
Scalmalloy is an aluminium \- magnesium \- scandium alloy that offers excellent stiffness, an exceptionally high strength \-
|
||||
to \- weight ratio, superb weldability and ductility, and low density to reduce parasitic mass from non \- structural
|
||||
features. It can effectively replace high \- strength 7000 series aluminium alloys in plate or forging form. Thanks to its
|
||||
low density, Scalmalloy provides density \- specific properties that are highly competitive, even when compared with
|
||||
the strongest alternatives. Compared with other al uminium alloys used in additive manufacturing, Scalmalloy delivers
|
||||
a unique level of corrosion resistance and maintains a highly stable microstructure up to 250°C, making it suitable for
|
||||
a broad range of high \- performance applications.
|
||||
Combining high strength with excellent ductility and processability, it is the ideal material for heavily loaded
|
||||
components, which is why it is already employed in many critical applications. Scalmalloy has an established track
|
||||
record across a wide range o f fields, including a erospace, robotics, marine, and motorsport, and is an approved
|
||||
material under FIA regulations.
|
||||
Chemical composition Physical properties
|
||||
Al – Aluminium balance Relative density Approx. 99.5 %
|
||||
Mg – Magnesium 4.0÷4.9 % Density 2.67 g/cm 3
|
||||
Sc \- Scandium 0.6 ÷0.8%
|
||||
Mn – Manganese 0.3 ÷0.8%
|
||||
Zr – Zirconium 0.2÷0.5 %
|
||||
Fe – Iron ≤ 0.4 %
|
||||
Si – Silicon ≤ 0.4 %
|
||||
Zn – Zinc ≤ 0.25 % Heat Treatment (stress relief)
|
||||
Ti – Titanium ≤ 0.15 % 20°C → 325 °C 1 hour
|
||||
Cu – Copper ≤ 0.10 % 325 °C 4 hours
|
||||
325 °C → 20°C \-
|
||||
Technical data
|
||||
Typical part accuracy (quote < 150 mm) ± 0.2/0.3 mm
|
||||
Typical part accuracy (quote ≥ 150 mm) ± 0.05mm each 25mm
|
||||
Surface roughness (as \- built) Ra: 5 ÷ 9 µm
|
||||
Surface roughness (after machining / polishing) Ra < 1.6 µm
|
||||
Mechanical properties
|
||||
Mechanical data Test method As \- Built Heat Treated
|
||||
Tensile streng th (Rm)
|
||||
ASTM E8 / E8M
|
||||
(unmachined specimen, Z \- axis)
|
||||
330 ± 5 MPa 5 5 5 ± 10 MPa
|
||||
Yield strength (Rp 0.2%) 260 ± 5 MPa 51 5 ± 10 MPa
|
||||
Elongation at break 19 ± 2 % 1 4 ± 2 %
|
||||
Young’s modulus na 72 ± 3 GPa
|
||||
Hardness Hv10 na 160
|
||||
Thermal conductivity ASTM E1461 \- 13 na 95 W/m·K
|
||||
|
||||
Pagina 1 di 1
|
||||
|
||||
|
||||
@@ -0,0 +1,4 @@
|
||||
At room temperature, Scalmalloy has significantly higher strength than aluminium AlSi10Mg. Compared to other aluminium alloys for Additive Manufacturing, Scalmalloy offers a unique corrosion resistance level and a highly stable microstructure up to 250°C, which makes it well-suited for a wide range of high-performance applications.
|
||||
|
||||
Scalmalloy is particularly suited to applications within motorsport, aerospace, aircraft construction, and advanced engineering with high strength and low density.
|
||||
Parts can be machined, welded, shot-peened, polished and coated.
|
||||
@@ -0,0 +1,53 @@
|
||||
[Download](https://presentations-decks-uploads-prod.s3.amazonaws.com/7403838/3888537/d7d22c9c3f0b5ebadec559f8674a1cc0830ef7ceed32211f489adeefce60aefe.pdf?X-Amz-Algorithm=AWS4-HMAC-SHA256&X-Amz-Date=20260910T074648Z&X-Amz-SignedHeaders=host&X-Amz-Expires=60&X-Amz-Credential=AKIAZ32RUKUMSNCVYAKB%2F20260910%2Fus-east-1%2Fs3%2Faws4_request&X-Amz-Signature=9af994d3996464c9abb7aa76139830a4591bb294404a2ad9757ebc9e7cc99f68)
|
||||
|
||||
This data sheet contains approximate values that may vary with build conditions and is intended for reference and comparison purposes only. It should not be used for
|
||||
design specifications or quality control. The performance characteristics of the material may be affected (±) by, but are not limited to, part design, part geometries,
|
||||
application and operating conditions. Each user is responsible for determining that the material is safe, lawful and technica lly suitable for the intended laws and
|
||||
regulations. A DDITIVA makes no warranties of any kind, express or implied, including, but not limited to, the warranties of merchantability, fitness for a particular use, or
|
||||
warranty against patent infringement. ADDITIVA excludes liability, however arising, for any inac curacies in this document.
|
||||
ADDITIVA\_Stainless Steel 316L\_rev006.docx
|
||||
Stainless Steel 316L is a fully austenitic chromium \- nickel \- molybdenum steel. Molybdenum provides high corrosion
|
||||
resistance. Its very low carbon content also improves resistance to intergranular corrosion and enhances weldability.
|
||||
Post \- weld heat treatment i s generally unnecessary. Stainless Steel 316L is not susceptible to pitting or crevice corrosion
|
||||
in chloride \- rich solutions.
|
||||
Stainless Steel 316L is used to manufacture acid \- and corrosion \- resistant prototypes, as well as unique or series \-
|
||||
production parts,in sectors such as automotive, shipbuilding, aerospace, food and beverage (including corrosion \-
|
||||
resistant pipes and containers), chemical, pharmaceutical, oil, and gas.
|
||||
Parts made from stainless steel 316L can be machined, welded, shot \- peened, polished, and coated.
|
||||
UNS AMS ASTM DIN
|
||||
S31603 5507 \- 5653 A240 DIN 1.4404 – ISO 5832 \- 1
|
||||
Chemical composition Physical properties
|
||||
Fe – Iron balance Relative density Approx. 99.9%
|
||||
Cr – Chromium 16÷18% Density 7.90 g/cm 3
|
||||
Ni – Nickel 11÷13%
|
||||
Mo – Molybdenum 2.0÷3.0% Heat Treatment (stress relief)
|
||||
Mn – Manganese ≤ 2.00% optional for parts sensitive to warpage
|
||||
Si – Silicon ≤ 0.75% 20°C → 550°C 3 hours
|
||||
Cu – Copper ≤ 0.50% 550°C 6 hours
|
||||
P – Phosphorus ≤ 0.25% 550°C → 20°C \-
|
||||
N – Nitrogen ≤ 0.10%
|
||||
S – Sulfur ≤ 0.10%
|
||||
O – Oxygen ≤ 0.10%
|
||||
C – Carbon ≤ 0.03%
|
||||
Technical data
|
||||
Typical part accuracy (quote < 150 mm) ± 0.2/0.3 mm
|
||||
Typical part accuracy (quote ≥ 150 mm) ± 0.05mm each 25mm
|
||||
Surface roughness (as built) Ra: 5 ÷ 9 µm
|
||||
Surface roughness (after machining / polishing) Ra < 1.6 µm
|
||||
Mechanical properties
|
||||
Mechanical data Test method As Built Heat Treated
|
||||
Tensile strenght (Rm)
|
||||
ASTM E8 / E8M
|
||||
(unmachined specimen, Z \- axis)
|
||||
6 4 0 ± 2 0 MPa
|
||||
Yield strength (Rp 0.2%) 4 7 0 ± 2 0 MPa
|
||||
Elongation at break 6 0 ± 10 %
|
||||
Young’s modulus 17 0 ± 2 0 GPa
|
||||
Hardness DIN EN ISO 6508 \- 1 18 HRC
|
||||
Thermal properties
|
||||
Maximum long \- term operating temperature Approx. 400°C / 752 °F
|
||||
Thermal conductivity Approx.15 W/mK
|
||||
|
||||
Pagina 1 di 1
|
||||
|
||||
|
||||
@@ -0,0 +1,5 @@
|
||||
Stainless Steel 316L is a fully austenitic, corrosion-resistant Chromium-Nickel-Molybdenum steel. The molybdenum gives the material a high corrosion resistance.
|
||||
|
||||
The low carbon content also improves resistance to inter-granular corrosion and weldability. Heat treatment after laser melting is normally not necessary. Stainless Steel 316L is not susceptible to pitting in chloride-containing solutions. Stainless Steel 316L is used for manufacturing acid and corrosion resistant prototypes, unique or series production parts in the following fields: automotive, shipbuilding, aerospace, food and beverage (i.e. corrosion-resistant pipes and containers), chemical, pharmaceutical, oil and gas industries. Typical applications are exhaust manifolds, furnace parts, heat exchangers, jet engine parts, pharmaceutical and photographic equipment, valve and pump parts, chemical processing equipment, tanks, evaporators. It also is used in pulp, paper, and textile processing equipment and for any parts exposed to marine environments.
|
||||
|
||||
Parts can be machined, welded, shot-peened, polished and coated.
|
||||
@@ -0,0 +1,46 @@
|
||||
[Download](https://presentations-decks-uploads-prod.s3.amazonaws.com/7403838/3888537/b21445edf69ed40915ebe94e04aa1abba12ed7a762bba4c4de6051a539f246c2.pdf?X-Amz-Algorithm=AWS4-HMAC-SHA256&X-Amz-Date=20260910T073256Z&X-Amz-SignedHeaders=host&X-Amz-Expires=60&X-Amz-Credential=AKIAZ32RUKUMSNCVYAKB%2F20260910%2Fus-east-1%2Fs3%2Faws4_request&X-Amz-Signature=72fa95bd59f9e1e43ac334dc465810fca266e953ab393c3fa20b00f2108696ac)
|
||||
|
||||
This data sheet contains approximate values that may vary with build conditions and is intended for reference and comparison purposes only. It should not be used for
|
||||
design specifications or quality control. The performance characteristics of the material can be affected (±) by, but not limited to, part design, part geometries,
|
||||
application and operating conditions. Each user is responsible for determining that the material is safe, lawful and technica lly suitable for the intended laws and
|
||||
regulations. ADDIT IVA makes no warranties of any kind, express or implied, including, but not limited to, the warranties of merchantability, fi tness for a particular use, or
|
||||
warranty against patent infringement. ADDITIVA excludes liability, however arising, for any inaccura cies in this document.
|
||||
ADDITIVA\_Titanium Ti6Al4V\_rev009.docx
|
||||
Titanium Ti6Al4V is a lightweight alloy renowned for its excellent mechanical properties, including fracture toughness,
|
||||
fatigue strength, and corrosion resistance, together with low specific weight and biocompatibility. Grade 23 differs from
|
||||
Grade 5 primar ily in its reduced oxygen content (maximum 0.13% in Grade 23), which enhances ductility and fracture
|
||||
toughness, although it slightly reduces strength. Grade 23 is widely used in fracture \- critical airframe structures,
|
||||
lightweight components for the motorspo rts and aerospace sectors, and surgical implants and medical instruments.
|
||||
UNS AMS ASTM DIN
|
||||
R 56401 4956 B 348 Grade 23 EN 3.7164 ISO 5832 \- 3
|
||||
Chemical composition Physical properties
|
||||
Ti – Titanium b alance Relative density Approx. 99.9%
|
||||
Al – Aluminium 5.5÷6.8% Density 4.43 g/cm 3
|
||||
V – Vanadium 3.5÷4.5%
|
||||
Fe – Iron ≤ 0.25% Heat Treatment (Annealing)
|
||||
O – Oxygen ≤ 0.13% under Argon atmosphere
|
||||
C – Carbon ≤ 0.08% 20°C → 7 50 °C 4 hours
|
||||
N – Nitrogen ≤ 0.05% 7 50 °C 1 hours
|
||||
H – Hydrogen ≤ 0.012% 7 50 °C → 20°C \-
|
||||
Technical data
|
||||
Typical part accuracy (quote < 150 mm) ± 0.2/0.3 mm
|
||||
Typical part accuracy (quote ≥ 150 mm) ± 0.05mm each 25mm
|
||||
Surface roughness (as built) Ra: 5 ÷ 9 µm
|
||||
Surface roughness (after machining / polishing) Ra < 1.6 µm
|
||||
Mechanical properties
|
||||
Mechanical data Test method As \- Built Heat Treated
|
||||
Tensile streng th (Rm)
|
||||
ASTM E8 / E8M
|
||||
(unmachined specimen, Z \- axis)
|
||||
1.1 8 0 ± 3 0 MPa 1.100 ± 20 MPa
|
||||
Yield strength (Rp 0.2%) 1.0 8 0 ± 3 0 MPa 1.0 6 0 ± 20 MPa
|
||||
Elongation at break 7 ± 1 % 1 2 ± 1 %
|
||||
Young’s modulus 11 0 ± 3 GPa 1 20 ± 5 GPa
|
||||
Hardness DIN EN ISO 6508 \- 1 3 7 HRC 3 7 HRC
|
||||
Thermal properties
|
||||
Maximum long \- term operating temperature Approx 355°C / 67 0°F
|
||||
Thermal conductivity 7 W/mK
|
||||
|
||||
Pagina 1 di 1
|
||||
|
||||
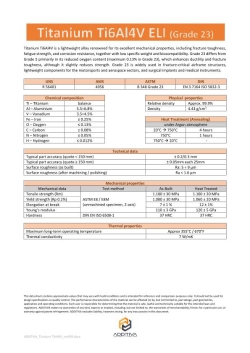
|
||||
@@ -0,0 +1,7 @@
|
||||
Titanium Ti6Al4V is a light alloy with excellent mechanical properties, fracture toughness, fatigue strength and corrosion resistance combined with low specific weight and biocompatibility.
|
||||
|
||||
Grade 23 differs from Grade 5 by the reduced oxygen content (max 0.13% in Grade 23): this ensures improved ductility and fracture toughness, with a slight reduction in strength.
|
||||
|
||||
Typical applications can be fracture-critical parts, low and high-temperature components and structures, such as fasteners, discs, hubs, spacers, seals, compressor blades, structural parts and complex turbine engine components. Ti6Al4V is ideal for many high-performance engineering applications in aerospace and motorsport and the production of biomedical implants due to its higher strength, low modulus, and fatigue resistance.
|
||||
|
||||
Parts can be machined, welded, shot-peened, polished and coated.
|
||||
Reference in New Issue
Block a user