Promuove pacchetto AM01-AM12 a riferimento primario; elabora guida ADDMAN e review particle damping
Su decisione dell'utente, il pacchetto di note AM01-AM12 (basato su fonti
NIST, Loughborough University, norme e produttori) viene promosso a
riferimento tecnico primario per le rispettive famiglie di processo,
distribuito in 01 Fondamenti, 02 Processi, 14 Glossario e 10 Fonti
(AM90 - Fonti, bibliografia a 38 fonti). Le note equivalenti derivate
dal corso video freeCodeCamp/GaugeHow restano come approfondimento,
con un rimando "Vedi anche" alla nuova nota primaria.

Elabora inoltre i restanti documenti acquisiti in 00 Inbox:
- Yu et al. 2026, review su additively manufactured particle damping
  structures: scheda fonte, riassunto e nota di concetto in
  04 Progettazione.
- ADDMAN (2024), "A Guide to Designing for Additive Manufacturing"
  (guida di produttore via MinerU): scheda fonte, riassunto e tre
  note di concetto (regole dimensionali, regole/difetti per processo,
  strumenti software).
- iamrapid.com e IQS Directory: schede fonte minime per tracciabilita',
  contenuto ridondante rispetto a fonti di qualita' superiore, nessuna
  nota derivata.
- Scartati duplicati esatti gia' archiviati in 90 Allegati.

Aggiorna tutti gli indici coinvolti e sposta gli originali elaborati
da 00 Inbox a 90 Allegati.

Co-Authored-By: Claude Sonnet 5 <noreply@anthropic.com>
This commit is contained in:

 Claude Sonnet 5
Vendored
+1
-1
@@ -17,6 +17,6 @@
|
||||
"repelStrength": 10,
|
||||
"linkStrength": 1,
|
||||
"linkDistance": 250,
|
||||
"scale": 3.8634105686174873,
|
||||
"scale": 1.9655560456566548,
|
||||
"close": true
|
||||
}
|
||||
@@ -18,6 +18,13 @@ Raccogli qui appunti veloci e riferimenti da classificare. Sposta i file binari
|
||||
- [x] freeCodeCamp/GaugeHow — 3D Printing & Additive Manufacturing Full Course: trascrizione acquisita, tradotta e trasformata in note; originale spostato in [[90 Allegati/3D Printing & Additive Manufacturing – Full Course|3D Printing & Additive Manufacturing – Full Course]], vedi [[SRC - freeCodeCamp GaugeHow - 3D Printing and Additive Manufacturing Full Course]].
|
||||
- [x] Zhou et al. 2024, "Additive Manufacturing: A Comprehensive Review" (Sensors, CC BY 4.0): riassunto e scheda fonte creati, originale spostato in `90 Allegati`, vedi [[SRC - Zhou et al. 2024 - Additive Manufacturing A Comprehensive Review]].
|
||||
- [x] ADDITIVA — schede tecniche leghe metalliche per SLM/DMLS (AlSi10Mg, Inconel 718, Scalmalloy, Stainless Steel 316L, Titanium Ti6Al4V): tradotte in 5 note di concetto in `03 Materiali`, originali spostati in `90 Allegati`, vedi [[SRC - ADDITIVA - Schede tecniche leghe metalliche per AM]].
|
||||
- [x] Yu et al. 2026, "Additively Manufactured Particle Damping Structures: A Review" (Additive Manufacturing Letters): scheda fonte, riassunto e nota di concetto creati in `04 Progettazione`, originale spostato in `90 Allegati`, vedi [[SRC - Yu et al. 2026 - Additively Manufactured Particle Damping Structures Review]].
|
||||
- [x] IQS Directory — Additive Manufacturing Guide (esportazione highlights JSON): scheda fonte minima creata per tracciabilità, contenuto ridondante rispetto a fonti di qualità superiore già nel vault, nessuna nota derivata; originale spostato in `90 Allegati`, vedi [[SRC - IQS Directory - Additive Manufacturing Guide]].
|
||||
- [x] **AM00–AM12 + AM90**: su decisione dell'utente, promosse a riferimento tecnico primario (fonti NIST, Loughborough University, norme, produttori — più solide del corso video). Distribuite in `01 Fondamenti` (AM00, AM01, AM11→"Confronto tecnologie e materiali"), `02 Processi` (AM02–AM10), `14 Glossario` (AM12, fuso in `Glossario.md`) e `10 Fonti` (AM90 - Fonti, bibliografia condivisa). Le note equivalenti derivate dal corso video restano con un rimando "Vedi anche" alla nuova nota primaria.
|
||||
- [x] Duplicati esatti già archiviati (trascrizione video, highlights JSON iamrapid): scartati come richiesto, invece di essere rielaborati.
|
||||
- [x] ADDMAN (2024), "A Guide to Designing for Additive Manufacturing" (acquisita via MinerU): scheda fonte, riassunto e 2 note in `04 Progettazione` (regole dimensionali; regole/difetti per processo) create; originali spostati in `90 Allegati`, vedi [[SRC - ADDMAN 2024 - A Guide to Designing for Additive Manufacturing]].
|
||||
- [x] iamrapid.com — Design for Additive Manufacturing Rules & Guide: scheda fonte minima per tracciabilità, contenuto ridondante rispetto a fonti superiori già nel vault, nessuna nota derivata; originale spostato in `90 Allegati`, vedi [[SRC - iamrapid.com - Design for Additive Manufacturing Rules and Guide]].
|
||||
- [x] Nota software: [[Strumenti software per progettazione e simulazione in AM]] creata in `05 Parametri e simulazione` a partire dal capitolo 4 della guida ADDMAN.
|
||||
|
||||
[[Metodo di lavoro]]
|
||||
|
||||
|
||||
@@ -13,6 +13,9 @@ sources: ["[[SRC - freeCodeCamp GaugeHow - 3D Printing and Additive Manufacturin
|
||||
|
||||
# Classificazione ASTM per i processi di stampa 3D
|
||||
|
||||
> [!info] Vedi anche — riferimento primario aggiornato
|
||||
> [[AM01 - Fondamenti e panoramica]] copre la stessa classificazione con fonti più solide (NIST, Loughborough University, norma ISO/ASTM 52900) ed è la nota di riferimento primaria per questo tema. Questa nota resta come approfondimento basato su una singola fonte video.
|
||||
|
||||
## In breve
|
||||
Il corso presenta una classificazione in 7 famiglie di processo di manifattura additiva (attribuita ad "ASTM/ASM"), più un ottavo raggruppamento "ibrido" che combina AM e manifattura sottrattiva. [Fonte: modulo 2, [0:49:17]–[1:00:51]; [[SRC - freeCodeCamp GaugeHow - 3D Printing and Additive Manufacturing Full Course]]] **Nota terminologica**: la classificazione standard di riferimento nel settore è ASTM F42/ISO 52900, che definisce 7 categorie di processo; il corso le attribuisce genericamente ad "ASM", possibile imprecisione del docente — da verificare rispetto al testo della norma ISO/ASTM 52900 prima di citare questa classificazione come normativa.
|
||||
|
||||
|
||||
@@ -13,6 +13,9 @@ sources: ["[[SRC - NIST - What is Additive Manufacturing]]"]
|
||||
|
||||
# Introduzione alla manifattura additiva
|
||||
|
||||
> [!info] Vedi anche — riferimento primario aggiornato
|
||||
> [[AM01 - Fondamenti e panoramica]] copre lo stesso argomento con fonti più solide (NIST, Loughborough University, norme) ed è la nota di riferimento primaria per questo tema. Questa nota resta come approfondimento introduttivo basato su una singola pagina NIST.
|
||||
|
||||
## Definizione
|
||||
La manifattura additiva realizza parti aggiungendo materiale progressivamente, tipicamente strato su strato. È comunemente chiamata stampa 3D. [Fonte: NIST, apertura della pagina; [[SRC - NIST - What is Additive Manufacturing]]]
|
||||
|
||||
|
||||
@@ -13,6 +13,9 @@ sources: ["[[SRC - freeCodeCamp GaugeHow - 3D Printing and Additive Manufacturin
|
||||
|
||||
# Manifattura additiva vs manifattura sottrattiva
|
||||
|
||||
> [!info] Vedi anche — riferimento primario aggiornato
|
||||
> [[AM01 - Fondamenti e panoramica]] e [[Confronto tecnologie e materiali]] coprono argomenti correlati con fonti più solide (NIST, Loughborough University, norme, produttori) e sono i riferimenti primari per questo tema. Questa nota resta come approfondimento basato su una singola fonte video.
|
||||
|
||||
## In breve
|
||||
La manifattura additiva (AM) crea un oggetto aggiungendo materiale uno strato alla volta, a partire da un modello CAD affettato in layer 2D; la manifattura sottrattiva parte da un blocco di materiale e lo asporta (es. fresatura CNC) fino alla forma desiderata. [Fonte: modulo 2, [0:36:21]–[0:37:54]; [[SRC - freeCodeCamp GaugeHow - 3D Printing and Additive Manufacturing Full Course]]]
|
||||
|
||||
|
||||
@@ -0,0 +1,43 @@
|
||||
---
|
||||
id: "am-course-am00"
|
||||
title: "Additive manufacturing — Percorso di riferimento sui processi"
|
||||
type: "indice"
|
||||
status: "pronto"
|
||||
created: "2026-09-10"
|
||||
updated: "2026-09-10"
|
||||
language: "it"
|
||||
tags: ["am/concetto"]
|
||||
aliases: []
|
||||
sources: ["[[AM90 - Fonti#S01]]", "[[AM90 - Fonti#S02]]"]
|
||||
---
|
||||
|
||||
# Additive manufacturing — Percorso di riferimento sui processi
|
||||
|
||||
## Percorso di lettura
|
||||
Serie di note tecniche in italiano, preparate il 10 settembre 2026 a partire da fonti primarie (NIST, Loughborough University, norme, documentazione di produttori — vedi [[AM90 - Fonti]]), poi promosse a riferimento tecnico principale per le rispettive famiglie di processo in `01 Fondamenti` e `02 Processi`, sostituendo come fonte primaria le note equivalenti derivate in precedenza da un singolo corso video (vedi il richiamo "Vedi anche" in ciascuna nota superseduta). Copre le sette famiglie principali; la PBF è suddivisa fra metalli e polimeri per evitare confronti impropri.
|
||||
|
||||
Le note sono sintesi originali con riferimenti. Le sezioni denominate "esempio ragionato", "schema" o "proposta" sono elaborazioni didattiche, non risultati sperimentali. I valori dell'esempio economico sono inventati e dichiarati come tali. Le fonti dei produttori sono usate per descrivere i loro processi; i claim promozionali non sono adottati come leggi generali.
|
||||
|
||||
## Note di riferimento
|
||||
- [[AM01 - Fondamenti e panoramica|Che cos'è l'additive manufacturing]] (01 Fondamenti)
|
||||
- [[AM02 - Estrusione di materiale|Material extrusion: FFF, FDM, pellet, paste e metallo legato]] (02 Processi)
|
||||
- [[AM03 - Fotopolimerizzazione in vasca|Vat photopolymerization: SLA, DLP e MSLA]] (02 Processi)
|
||||
- [[AM04 - PBF dei metalli|Powder bed fusion dei metalli: LPBF, SLM, DMLS ed EB-PBF]] (02 Processi)
|
||||
- [[AM05 - PBF dei polimeri|Powder bed fusion dei polimeri: SLS, MJF e SAF]] (02 Processi)
|
||||
- [[AM06 - Binder jetting|Binder jetting: polvere, legante e consolidamento]] (02 Processi)
|
||||
- [[AM07 - Material jetting|Material jetting: gocce, fotopolimeri e multimateriale]] (02 Processi)
|
||||
- [[AM08 - Deposizione a energia diretta|Directed energy deposition: laser, fascio elettronico e WAAM]] (02 Processi)
|
||||
- [[AM09 - Laminazione di fogli|Sheet lamination: LOM e ultrasonic additive manufacturing]] (02 Processi)
|
||||
- [[AM10 - Processi specialistici|Processi specialistici e confini della manifattura additiva]] (02 Processi)
|
||||
- [[Confronto tecnologie e materiali|Come confrontare tecnologie, materiali e componenti stampati]] (01 Fondamenti)
|
||||
- [[Glossario|Glossario ragionato di manifattura additiva]] (14 Glossario)
|
||||
|
||||
## Provenienza e uso con IA
|
||||
[[AM90 - Fonti]] contiene i riferimenti, le sezioni utilizzate e i limiti di consultazione. Ogni nota riporta anche link diretti vicino alle affermazioni pertinenti.
|
||||
|
||||
Le note hanno stato `da_verificare`: fonti e coerenza editoriale sono state controllate, ma non è stata eseguita una revisione tecnica indipendente né una validazione sperimentale. Questo stato non significa che il testo sia un modello vuoto.
|
||||
|
||||
## Ambito e limiti
|
||||
Non sono cataloghi completi di leghe, ricette macchina o istruzioni di certificazione. I numeri di tolleranza e resistenza richiedono schede dedicate a sistema, materiale e stato del componente. Microstampa, cold spray e ceramiche sono introdotti nella nota specialistica; biostampa ed edilizia richiedono raccolte specifiche successive.
|
||||
|
||||
Il corso usa testo, tabelle e collegamenti; non contiene diagrammi costruiti con simboli Markdown.
|
||||
@@ -0,0 +1,62 @@
|
||||
---
|
||||
id: "am-course-am01"
|
||||
title: "Che cos’è l’additive manufacturing"
|
||||
type: "concetto"
|
||||
status: "da_verificare"
|
||||
created: "2026-09-10"
|
||||
updated: "2026-09-10"
|
||||
language: "it"
|
||||
tags: ["am/concetto"]
|
||||
aliases: ["Additive manufacturing", "Manifattura additiva", "AM"]
|
||||
sources: ["[[AM90 - Fonti#S01]]", "[[AM90 - Fonti#S02]]", "[[AM90 - Fonti#S16]]", "[[AM90 - Fonti#S32]]", "[[AM90 - Fonti#S37]]"]
|
||||
---
|
||||
|
||||
# Che cos’è l’additive manufacturing
|
||||
|
||||
## Definizione e idea centrale
|
||||
L’additive manufacturing (AM), o manifattura additiva, è un insieme di processi che costruiscono un oggetto a partire da una descrizione digitale, aggiungendo e consolidando materiale dove occorre. Nella maggior parte delle tecnologie la costruzione procede per strati. Il materiale può arrivare come filamento, granulo, polvere, filo metallico, resina, pasta o foglio: non esiste una sola “stampante 3D” valida per tutti questi casi. [S01 — NIST — What is Additive Manufacturing?](https://www.nist.gov/additive-manufacturing/what-additive-manufacturing)
|
||||
|
||||
Nella lavorazione sottrattiva, come fresatura e tornitura, l’utensile rimuove materiale da un grezzo. Nella formatura o nello stampaggio, una forma o uno stampo determina la geometria. L’AM rende la geometria dipendente soprattutto dal modello e dal percorso di deposizione o esposizione. Questo non elimina la necessità di utensili e lavorazioni: un pezzo additivo può essere successivamente fresato, rettificato o trattato.
|
||||
|
||||
## Dal modello al componente
|
||||
1. **Requisiti:** funzione, carichi, ambiente, durata, quantità e criteri di accettazione.
|
||||
2. **Modellazione:** CAD o geometria ricostruita; controllo di spessori, cavità e superfici.
|
||||
3. **Preparazione:** orientamento, eventuali supporti, disposizione dei pezzi e suddivisione in strati, detta slicing.
|
||||
4. **Fabbricazione:** la macchina esegue traiettorie o espone sezioni secondo il processo scelto.
|
||||
5. **Post processing:** raffreddamento, pulizia, rimozione supporti, eventuale cura o sinterizzazione e finitura.
|
||||
6. **Verifica:** confronto tra il componente reale e i requisiti iniziali.
|
||||
|
||||
Questa sequenza è una sintesi didattica: alcune operazioni si ripetono e nei sistemi ibridi si alternano. Il file digitale è l’inizio della produzione, non una garanzia delle proprietà finali. Il ruolo di misure e standard è evidenziato da NIST. [S01 — NIST — What is Additive Manufacturing?](https://www.nist.gov/additive-manufacturing/what-additive-manufacturing)
|
||||
|
||||
## Sette famiglie, molte varianti
|
||||
| Famiglia | Come prende forma il componente | Approfondimento |
|
||||
|---|---|---|
|
||||
| Material extrusion, MEX | Materiale spinto attraverso un ugello | [[AM02 - Estrusione di materiale]] |
|
||||
| Vat photopolymerization, VPP | Resina in vasca consolidata dalla luce | [[AM03 - Fotopolimerizzazione in vasca]] |
|
||||
| Powder bed fusion, PBF | Zone di polvere fuse mediante energia termica | [[AM04 - PBF dei metalli]] e [[AM05 - PBF dei polimeri]] |
|
||||
| Binder jetting, BJT | Legante depositato su polvere | [[AM06 - Binder jetting]] |
|
||||
| Material jetting, MJT | Deposizione di gocce del materiale costruttivo | [[AM07 - Material jetting]] |
|
||||
| Directed energy deposition, DED | Alimentazione e fusione localizzata del materiale | [[AM08 - Deposizione a energia diretta]] |
|
||||
| Sheet lamination, SHL | Unione e sagomatura di fogli | [[AM09 - Laminazione di fogli]] |
|
||||
|
||||
Questa tassonomia distingue il meccanismo di fabbricazione. FDM, PolyJet e altri nomi commerciali non sono nuove famiglie. La norma di riferimento terminologico qui identificata è ISO/ASTM 52900:2021; queste dispense non riproducono il testo normativo. [S02 — Loughborough University — The 7 Categories of Additive Manufacturing](https://www.lboro.ac.uk/research/amrg/about/the7categoriesofadditivemanufacturing/) [S37 — ISO — ISO/ASTM 52900:2021](https://www.iso.org/standard/74514.html)
|
||||
|
||||
## Perché può essere conveniente
|
||||
Il beneficio più interessante spesso è cambiare il progetto: integrare funzioni, ridurre assemblaggi, realizzare geometrie interne o adattare un prodotto a una singola esigenza. Può risultare utile anche abbreviare l’iterazione fra due prototipi senza costruire uno stampo nuovo. Non segue però che qualunque oggetto stampato costi meno: la convenienza dipende dal caso. [S32 — NIST — Costs and Cost Effectiveness of Additive Manufacturing](https://www.nist.gov/publications/costs-and-cost-effectiveness-additive-manufacturing)
|
||||
|
||||
**Esempio ragionato, non caso sperimentale:** immagina un distributore con molti condotti. Stampare lo stesso blocco pieno progettato per la fresatura potrebbe aggiungere costo senza beneficio. Ridisegnare i condotti per integrare più raccordi potrebbe ridurre giunzioni e ingombro. Prima di scegliere l’AM devi però verificare che la polvere possa uscire, che le superfici interne siano accettabili e che il pezzo sia ispezionabile. Il vantaggio geometrico e il limite produttivo vanno valutati insieme.
|
||||
|
||||
## Perché le proprietà non dipendono solo dal materiale
|
||||
“Acciaio” o “nylon” identifica una famiglia chimica, non un componente qualificato. Occorre indicare grado, forma di alimentazione, macchina, parametri, orientamento e stato finale. Un fotopolimero che imita l’ABS non è automaticamente ABS. Una parte che esce da un processo con legante non è necessariamente già densa. Una resistenza a trazione elevata non dimostra resistenza a fatica elevata: difetti e loro posizione possono dominare il comportamento ciclico. [S16 — NIST — Additive Manufacturing Fatigue and Fracture](https://www.nist.gov/programs-projects/additive-manufacturing-fatigue-and-fracture)
|
||||
|
||||
## Come leggere queste dispense
|
||||
Il livello è introduttivo-universitario, con ragionamento ingegneristico e termini inglesi per facilitare ulteriori ricerche. I materiali elencati sono esempi rappresentativi; la compatibilità va verificata sul sistema concreto. Le note trattano tutte le sette famiglie e le varianti più rilevanti, non ogni brevetto o denominazione commerciale esistente. Per metodi specialistici e sviluppi recenti vedi [[AM10 - Processi specialistici]].
|
||||
|
||||
Per consolidare lo studio: spiega con parole tue la differenza fra generare la forma e ottenere le proprietà finali. È il collegamento che permette di capire tutte le tecnologie successive.
|
||||
|
||||
|
||||
## Fonti e navigazione
|
||||
|
||||
Riferimenti di questa nota: [[AM90 - Fonti#S01|S01]], [[AM90 - Fonti#S02|S02]], [[AM90 - Fonti#S16|S16]], [[AM90 - Fonti#S32|S32]], [[AM90 - Fonti#S37|S37]].
|
||||
|
||||
[[AM00 - Inizia qui|Indice del corso]] · [[AM90 - Fonti|Bibliografia e limiti delle fonti]]
|
||||
@@ -0,0 +1,80 @@
|
||||
---
|
||||
id: "am-course-am11"
|
||||
title: "Come confrontare tecnologie, materiali e componenti stampati"
|
||||
type: "concetto"
|
||||
status: "da_verificare"
|
||||
created: "2026-09-10"
|
||||
updated: "2026-09-10"
|
||||
language: "it"
|
||||
tags: ["am/concetto"]
|
||||
aliases: ["Scelta tecnologia", "Confronto tecnologie", "DfAM"]
|
||||
sources: ["[[AM90 - Fonti#S03]]", "[[AM90 - Fonti#S06]]", "[[AM90 - Fonti#S08]]", "[[AM90 - Fonti#S11]]", "[[AM90 - Fonti#S12]]", "[[AM90 - Fonti#S16]]", "[[AM90 - Fonti#S18]]", "[[AM90 - Fonti#S24]]", "[[AM90 - Fonti#S27]]", "[[AM90 - Fonti#S30]]", "[[AM90 - Fonti#S32]]"]
|
||||
---
|
||||
|
||||
# Come confrontare tecnologie, materiali e componenti stampati
|
||||
|
||||
## Il confronto parte dalla funzione
|
||||
La domanda “qual è la tecnologia migliore?” è incompleta. Una forma per presentazione, una dima, un componente caricato ciclicamente e un oggetto personalizzato hanno criteri diversi. Le tabelle seguenti sono una sintesi orientativa delle dispense collegate, non un catalogo di prestazioni certificate.
|
||||
|
||||
## Matrice orientativa dei materiali
|
||||
| Processo | Alimentazione rappresentativa | Tipo di componente dopo il ciclo completo |
|
||||
|---|---|---|
|
||||
| FFF/FDM | Filamento termoplastico, eventualmente caricato | Polimero o composito |
|
||||
| Estrusione metallica legata | Polvere metallica in legante | Metallo dopo rimozione legante e sinterizzazione |
|
||||
| SLA/DLP/MSLA | Resina fotosensibile | Fotopolimero curato |
|
||||
| LCM ceramica | Sospensione ceramica fotosensibile | Ceramica dopo ciclo termico |
|
||||
| LPBF / EB-PBF | Polvere metallica specifica | Metallo consolidato e successivamente trattato secondo requisiti |
|
||||
| SLS / MJF / SAF | Polvere termoplastica specifica | Polimero consolidato |
|
||||
| Binder jetting metallico | Polvere e legante | Metallo dopo consolidamento finale |
|
||||
| Material jetting | Fotopolimeri, cere o altre formulazioni compatibili | Dipende dalla formulazione e dal percorso |
|
||||
| DED / WAAM | Filo o polvere metallica | Deposito o preforma metallica |
|
||||
| LOM / UAM | Fogli / nastri | Laminato, modello o struttura metallica secondo il processo |
|
||||
|
||||
La tabella riprende [[AM02 - Estrusione di materiale]], [[AM03 - Fotopolimerizzazione in vasca]], [[AM04 - PBF dei metalli]], [[AM05 - PBF dei polimeri]], [[AM06 - Binder jetting]], [[AM07 - Material jetting]], [[AM08 - Deposizione a energia diretta]] e [[AM09 - Laminazione di fogli]], dove sono riportate le rispettive fonti. Non indica compatibilità di ogni materiale con ogni macchina.
|
||||
|
||||
## Tre livelli di compatibilità
|
||||
1. **Fisica:** il materiale può essere trasformato con quel principio?
|
||||
2. **Tecnologica:** esiste una combinazione macchina-feedstock-parametri capace di produrre il risultato?
|
||||
3. **Applicativa:** quel risultato soddisfa i requisiti del componente e dispone di evidenze sufficienti?
|
||||
|
||||
Questa distinzione è un criterio editoriale e ingegneristico. Evita di passare da “esiste un articolo su questa lega” a “posso usarla in produzione con questa macchina”.
|
||||
|
||||
## Pro e contro: criteri da misurare
|
||||
| Aspetto | Domanda utile | Errore frequente |
|
||||
|---|---|---|
|
||||
| Resistenza | A quale carico, direzione, temperatura e durata? | Usare una sola resistenza a trazione |
|
||||
| Precisione | Quale quota è misurata e dopo quali trattamenti? | Scambiare spessore strato e tolleranza |
|
||||
| Rugosità | Quale superficie e con quale accesso alla finitura? | Valutare solo una faccia esterna |
|
||||
| Leggerezza | A parità di funzione e durata? | Confrontare masse di progetti non equivalenti |
|
||||
| Complessità | Il pezzo è anche pulibile e ispezionabile? | Considerare solo la generazione della forma |
|
||||
| Produttività | Quanti pezzi accettati nel ciclo completo? | Contare solo il tempo di stampa |
|
||||
| Costo | Quali operazioni, scarti e controlli sono inclusi? | Confrontare soltanto i consumabili |
|
||||
| Ripetibilità | Qual è la dispersione su più costruzioni? | Generalizzare da un campione riuscito |
|
||||
|
||||
Queste domande non attribuiscono un primato a una tecnologia. Sono uno schema proposto per raccogliere dati confrontabili.
|
||||
|
||||
## Un modello di costo didattico
|
||||
Considera il costo totale del lotto come somma di preparazione, fabbricazione, materiali, post processing, controlli e rilavorazioni. Dividilo per il numero di pezzi accettati, non per quello di pezzi avviati. Se confronti stampaggio o fusione, rendi esplicito anche come viene ripartito il costo degli utensili. NIST SP 1176 affronta la convenienza economica dell’AM; il suo anno è 2014 e non viene usato per fornire prezzi attuali. [S32 — NIST — Costs and Cost Effectiveness of Additive Manufacturing](https://www.nist.gov/publications/costs-and-cost-effectiveness-additive-manufacturing)
|
||||
|
||||
**Esempio numerico inventato per spiegare il calcolo:** un lotto costa complessivamente 600 euro e produce dieci pezzi accettati; il costo medio è 60 euro. Se il costo resta uguale ma i pezzi accettati sono otto, il costo medio diventa 75 euro. Non sono preventivi: mostrano perché la resa produttiva conta.
|
||||
|
||||
## Qualità meccanica
|
||||
La letteratura NIST sulla fatica mostra l’importanza delle discontinuità e dei pori come possibili origini del danneggiamento. [S16 — NIST — Additive Manufacturing Fatigue and Fracture](https://www.nist.gov/programs-projects/additive-manufacturing-fatigue-and-fracture) In un confronto devi quindi conservare almeno geometria della prova, orientamento, finitura, trattamenti, condizioni del carico e numerosità dei campioni. Una frase come “resistente quanto il metallo tradizionale” non è sufficientemente definita per essere riutilizzata da un agente IA.
|
||||
|
||||
## Mini-casi di ragionamento
|
||||
- **Modello visivo:** prioritari dettaglio, colore e superficie; una prova meccanica può non essere l’obiettivo.
|
||||
- **Dima di officina:** prioritari stabilità sotto carico, usura e ambiente; la somiglianza estetica è secondaria.
|
||||
- **Condotto complesso:** prioritari geometria interna, pulizia e controllo; realizzare la forma non risolve tutta la produzione.
|
||||
- **Preforma grande:** importante il bilancio tra deposito e asportazione finale; il massimo dettaglio in stampa può non essere necessario.
|
||||
|
||||
Sono scenari didattici, non raccomandazioni di acquisto o processi già qualificati.
|
||||
|
||||
## Scheda minima da chiedere a un fornitore
|
||||
Materiale e grado; macchina e processo; orientamento; stato finale; quote e metodo di misura; dati meccanici con condizioni; operazioni incluse; tracciabilità e limiti dichiarati. Se una voce manca, conservarla come incognita invece di sostituirla con un valore generico trovato online.
|
||||
|
||||
|
||||
## Fonti e navigazione
|
||||
|
||||
Riferimenti di questa nota: [[AM90 - Fonti#S03|S03]], [[AM90 - Fonti#S06|S06]], [[AM90 - Fonti#S08|S08]], [[AM90 - Fonti#S11|S11]], [[AM90 - Fonti#S12|S12]], [[AM90 - Fonti#S16|S16]], [[AM90 - Fonti#S18|S18]], [[AM90 - Fonti#S24|S24]], [[AM90 - Fonti#S27|S27]], [[AM90 - Fonti#S30|S30]], [[AM90 - Fonti#S32|S32]].
|
||||
|
||||
[[AM00 - Inizia qui|Indice del corso]] · [[AM90 - Fonti|Bibliografia e limiti delle fonti]]
|
||||
@@ -13,6 +13,9 @@ sources: ["[[SRC - freeCodeCamp GaugeHow - 3D Printing and Additive Manufacturin
|
||||
|
||||
# Flusso di lavoro e formati file per la stampa 3D
|
||||
|
||||
> [!info] Vedi anche — riferimento correlato
|
||||
> [[AM01 - Fondamenti e panoramica]] descrive lo stesso flusso "dal modello al componente" con fonti più solide (NIST). Questa nota resta come riferimento primario per il dettaglio sui formati file (STL, OBJ, VRML, 3MF, AMF), non coperto in AM01.
|
||||
|
||||
## In breve
|
||||
Il corso descrive il flusso di lavoro standard della stampa 3D come una sequenza: modello CAD 3D → file STL (o formato equivalente) → dati sezionati (slicing) → file di job specifico per macchina/processo → pezzo stampato → post-processing. Fino allo slicing il flusso è indicato come identico per tutte le famiglie di processo AM (PBF, FDM, ecc.); da quel punto in poi il job file diventa specifico della tecnologia e della macchina. [Fonte: modulo 4, [2:27:09]–[2:30:30]; [[SRC - freeCodeCamp GaugeHow - 3D Printing and Additive Manufacturing Full Course]]] Il formato di interscambio più usato per passare dal CAD al software di stampa è l'STL, basato su tessellazione triangolare della sola superficie; formati più recenti (OBJ, VRML/WRL, 3MF, AMF) aggiungono in vario grado colore, materiale e texture. [2:37:19]–[2:46:55]
|
||||
|
||||
|
||||
@@ -16,11 +16,17 @@ sources: []
|
||||
Indice da sviluppare: Terminologia IT/EN; catena digitale; confronto tra processi; criteri di selezione; grandezze e unità.
|
||||
|
||||
## Note disponibili
|
||||
Riferimento primario (fonti NIST, Loughborough University, norme):
|
||||
- [[AM00 - Inizia qui|Percorso di riferimento sui processi]]
|
||||
- [[AM01 - Fondamenti e panoramica]]
|
||||
- [[Confronto tecnologie e materiali]]
|
||||
|
||||
Note derivate dal corso video (approfondimento, vedi rimando alle note sopra):
|
||||
- [[AM - Introduzione]]
|
||||
- [[AM - Industry 4.0 e ruolo della stampa 3D]]
|
||||
- [[AM - Manifattura additiva vs manifattura sottrattiva]]
|
||||
- [[AM - Classificazione ASTM per i processi di stampa 3D]]
|
||||
- [[Flusso di lavoro e formati file per la stampa 3D]]
|
||||
- [[Flusso di lavoro e formati file per la stampa 3D]] (riferimento primario per i formati file, non superseduta)
|
||||
|
||||
## Domande da sviluppare
|
||||
- Quali concetti e definizioni servono per questo ambito?
|
||||
|
||||
@@ -0,0 +1,59 @@
|
||||
---
|
||||
id: "am-course-am02"
|
||||
title: "Material extrusion: FFF, FDM, pellet, paste e metallo legato"
|
||||
type: "concetto"
|
||||
status: "da_verificare"
|
||||
created: "2026-09-10"
|
||||
updated: "2026-09-10"
|
||||
language: "it"
|
||||
tags: ["am/concetto", "am/processo"]
|
||||
aliases: ["FFF", "FDM", "MEX", "DIW", "Material extrusion"]
|
||||
sources: ["[[AM90 - Fonti#S03]]", "[[AM90 - Fonti#S04]]", "[[AM90 - Fonti#S05]]", "[[AM90 - Fonti#S06]]", "[[AM90 - Fonti#S07]]", "[[AM90 - Fonti#S36]]"]
|
||||
---
|
||||
|
||||
# Material extrusion: FFF, FDM, pellet, paste e metallo legato
|
||||
|
||||
## Come funziona
|
||||
Un ugello deposita un cordone e costruisce contorni e riempimenti. Nella FFF, fused filament fabrication, il filamento viene alimentato e riscaldato; il materiale estruso aderisce ai cordoni già depositati. FDM è una denominazione commerciale storicamente associata a Stratasys. L’estrusione non è solo la stampante domestica: il principio può essere applicato ad alimentazioni e materiali diversi. [S03 — Loughborough University — Material Extrusion](https://www.lboro.ac.uk/research/amrg/about/the7categoriesofadditivemanufacturing/materialextrusion/)
|
||||
|
||||
Il cordone ha una larghezza finita: uno spigolo, una parete e una cavità risultano dalla combinazione fra traiettoria e forma depositata. Aumentare la velocità di movimento non basta a rendere veloce il processo se l’estrusore non riesce a fornire la portata richiesta. Il riempimento interno, o infill, è geometria progettata: un valore nominale del 100% non è una misura sperimentale dell’assenza di vuoti.
|
||||
|
||||
## Il legame fra strati
|
||||
Nei termoplastici, la saldatura tra cordoni richiede contatto e mobilità delle catene polimeriche. Il materiale caldo deposita energia anche nella superficie precedente; raffreddandosi, la possibilità di interdiffusione diminuisce. Lo studio di Seppala e colleghi collega misure termiche, reologia e prove di frattura allo sviluppo del legame interstrato. Ne deriva una conseguenza pratica: la storia termica conta, non soltanto il nome del filamento. [S05 — Seppala et al. — Weld formation during material extrusion additive manufacturing](https://www.nist.gov/publications/weld-formation-during-material-extrusion-additive-manufacturing)
|
||||
|
||||
Orientare una zona caricata perpendicolarmente alle interfacce può rendere il legame fra strati decisivo. Una superficie esterna apparentemente integra non dimostra la qualità del collegamento interno. Il comportamento va valutato nella direzione e nello stato di condizionamento pertinenti.
|
||||
|
||||
## Materiali e alimentazioni
|
||||
| Variante | Materiali rappresentativi | Aspetto da verificare |
|
||||
|---|---|---|
|
||||
| Filamento termoplastico | PLA, PETG, ABS, ASA, PA, PC, TPU | Temperature, umidità, adesione e requisiti della macchina |
|
||||
| Filamento con cariche | Polimero con fibre corte o particelle | Usura ugello e proprietà effettive del composito |
|
||||
| Rinforzo continuo | Matrice termoplastica con fibre continue | Percorso delle fibre e direzione dei carichi |
|
||||
| Pellet / granulo | Termoplastici e compound compatibili | Dosaggio, essiccazione, scala del cordone |
|
||||
| Paste / direct ink writing | Sospensioni ceramiche e altre paste formulate | Reologia, mantenimento della forma e consolidamento successivo |
|
||||
| Metallo legato | Polvere metallica dispersa in legante | Debinding e sinterizzazione dopo la stampa |
|
||||
|
||||
Prusa documenta requisiti differenti fra filamenti, fra cui camera, essiccazione e ugelli resistenti all’usura; non tutti sono intercambiabili. [S04 — Prusa — Filament Material Guide](https://help.prusa3d.com/filament-material-guide) Le fibre corte disperse e le fibre continue sono architetture differenti: le seconde permettono di disporre il rinforzo lungo percorsi scelti. Non basta la dicitura “carbonio” per equiparare due pezzi. [S07 — Markforged — Carbon Fiber 3D Printing: An Introductory Guide](https://static.markforged.com/downloads/MF_White_paper_carbon_fiber.pdf)
|
||||
|
||||
La DIW usa la deformabilità della pasta per estrudere e la sua capacità di mantenere la forma dopo la deposizione. Per le ceramiche, NIST studia specificamente le sospensioni concentrate e la loro reologia: essere estrudibile non basta a essere dimensionalmente stabile. [S36 — NIST — Ceramic Additive Manufacturing](https://www.nist.gov/mml/mmsd/primary-focus-areas/ceramic-additive-manufacturing)
|
||||
|
||||
## Estrusione di metallo: cosa accade dopo
|
||||
Il filamento metallico legato forma un pezzo verde, cioè una struttura di particelle tenute dal legante. Il debinding rimuove una parte del legante; il ciclo termico elimina il residuo e sinterizza le particelle. La densificazione comporta ritiro e richiede gestione di atmosfera e sostegno della geometria. Il pezzo può poi essere trattato e lavorato. La guida Markforged descrive questa catena: non è fusione di filo metallico nell’ugello e non è una semplice sostituzione del PLA. [S06 — Markforged — Guide to Metal FFF 3D Printing](https://static.markforged.com/downloads/MF_White_paper_Metal_FFF_3D_Printing_Guide.pdf)
|
||||
|
||||
## Vantaggi e limiti
|
||||
Per iterazioni geometriche e attrezzaggi semplici, l’estrusione consente una catena accessibile e modifiche rapide. I limiti più evidenti sono tracce dei cordoni, necessità di supportare alcune geometrie e dipendenza del risultato dalla deposizione. [S03 — Loughborough University — Material Extrusion](https://www.lboro.ac.uk/research/amrg/about/the7categoriesofadditivemanufacturing/materialextrusion/) La resistenza del filamento di partenza non deve essere assegnata direttamente al pezzo: interfacce, riempimento e orientamento partecipano alla risposta meccanica. [S05 — Seppala et al. — Weld formation during material extrusion additive manufacturing](https://www.nist.gov/publications/weld-formation-during-material-extrusion-additive-manufacturing)
|
||||
|
||||
## Esempio di scelta ragionata
|
||||
Per una dima di posizionamento, separa tre domande: la forma è corretta, la dima si deforma sotto serraggio, la superficie si consuma? Un prototipo geometrico economico può rispondere alla prima e non alle altre. Prima di aggiungere fibra, prova a ragionare su spessore, nervature e orientamento. È un esempio didattico, non una prescrizione di materiale.
|
||||
|
||||
## Da registrare in una prova
|
||||
Grado e lotto del materiale, essiccazione, ugello, temperature, orientamento, spessore strato, pareti, infill, velocità, supporti, condizionamento e metodo di prova. Questi campi sono una proposta di tracciabilità per rendere confrontabili i risultati.
|
||||
|
||||
Collegamenti: [[AM01 - Fondamenti e panoramica]] · [[AM06 - Binder jetting]] · [[Confronto tecnologie e materiali]]
|
||||
|
||||
|
||||
## Fonti e navigazione
|
||||
|
||||
Riferimenti di questa nota: [[AM90 - Fonti#S03|S03]], [[AM90 - Fonti#S04|S04]], [[AM90 - Fonti#S05|S05]], [[AM90 - Fonti#S06|S06]], [[AM90 - Fonti#S07|S07]], [[AM90 - Fonti#S36|S36]].
|
||||
|
||||
[[AM00 - Inizia qui|Indice del corso]] · [[AM90 - Fonti|Bibliografia e limiti delle fonti]]
|
||||
@@ -0,0 +1,59 @@
|
||||
---
|
||||
id: "am-course-am03"
|
||||
title: "Vat photopolymerization: SLA, DLP e MSLA"
|
||||
type: "concetto"
|
||||
status: "da_verificare"
|
||||
created: "2026-09-10"
|
||||
updated: "2026-09-10"
|
||||
language: "it"
|
||||
tags: ["am/concetto", "am/processo"]
|
||||
aliases: ["SLA", "DLP", "MSLA", "VPP", "Vat photopolymerization"]
|
||||
sources: ["[[AM90 - Fonti#S08]]", "[[AM90 - Fonti#S09]]", "[[AM90 - Fonti#S10]]", "[[AM90 - Fonti#S11]]"]
|
||||
---
|
||||
|
||||
# Vat photopolymerization: SLA, DLP e MSLA
|
||||
|
||||
## Principio fisico
|
||||
Una resina fotosensibile viene esposta selettivamente. Dove l’esposizione produce una conversione sufficiente, si forma una struttura solida; il ciclo ricrea una nuova sezione di materiale da esporre. La geometria nasce quindi da una trasformazione chimica attivata dalla luce, non dal raffreddamento di un termoplastico fuso. NIST descrive questa famiglia come vat photopolymerization. [S10 — NIST — Vat Photopolymerization](https://www.nist.gov/additive-manufacturing/research-areas/technologies/vat-photopolymerization)
|
||||
|
||||
## Tre modi di generare la sezione
|
||||
| Variante | Come viene distribuita la luce | Conseguenza da comprendere |
|
||||
|---|---|---|
|
||||
| SLA a laser | Un fascio percorre la sezione | Tempo legato anche alla traiettoria e al sistema di scansione |
|
||||
| DLP | Un proiettore genera l’immagine della sezione | Importano ottica, dimensione proiettata e uniformità |
|
||||
| MSLA, spesso LCD | Una sorgente illumina una maschera selettiva | Importano pixel, trasmissione e collimazione della luce |
|
||||
|
||||
La parola SLA talvolta è usata in senso ampio per la stereolitografia; qui “SLA a laser” evita ambiguità. MSLA significa stereolitografia mascherata e non identifica obbligatoriamente ogni dettaglio della sorgente. La guida Formlabs chiarisce anche che un pixel più piccolo non è una garanzia di accuratezza dimensionale: la resina e la distribuzione dell’esposizione partecipano al risultato. [S09 — Formlabs — SLA vs DLP vs MSLA vs LCD](https://formlabs.com/blog/sla-dlp-msla-lcd-resin-3d-printer-comparison/)
|
||||
|
||||
## Architettura e ciclo
|
||||
Nei sistemi top-down si espone la superficie superiore del bagno e la piattaforma procede nel liquido. Nei sistemi bottom-up si espone attraverso il fondo trasparente; tra due strati occorre ristabilire lo spazio con nuova resina. Le modalità di distacco e ricopertura differiscono tra macchine. I supporti hanno una funzione geometrica e di stabilizzazione durante la costruzione. [S08 — Loughborough University — Vat Photopolymerisation](https://www.lboro.ac.uk/research/amrg/about/the7categoriesofadditivemanufacturing/vatphotopolymerisation/) [S09 — Formlabs — SLA vs DLP vs MSLA vs LCD](https://formlabs.com/blog/sla-dlp-msla-lcd-resin-3d-printer-comparison/)
|
||||
|
||||
## Materiali
|
||||
Si utilizzano formulazioni fotopolimeriche rigide, flessibili o destinate a requisiti specifici. Il nome commerciale “ABS-like” descrive un obiettivo di comportamento, non una composizione identica all’ABS termoplastico. Per scegliere occorrono dati sullo stato finale: conversione, post-cura, temperatura di prova, durata del carico e ambiente.
|
||||
|
||||
Esistono anche sospensioni fotosensibili caricate con ceramica. In LCM, ad esempio, la forma è prodotta con una fase fotopolimerizzabile, ma la ceramica finale richiede rimozione degli organici e sinterizzazione. La stabilità durante questo percorso è parte del processo, non una finitura estetica opzionale. [S11 — Lithoz — A Leader in the Additive Manufacturing Space](https://www.lithoz.com/en/lithoz-a-leader-in-the-additive-manufacturing-space/)
|
||||
|
||||
## Vantaggi
|
||||
La famiglia è utile per dettagli fini e superfici adatte alla verifica visiva, per modelli e geometrie che richiedono una deposizione molto selettiva. Il vantaggio di esporre una sezione in parallelo dipende però anche dai tempi di movimento e ricopertura. Valutare solo il tempo di esposizione trascura una parte del ciclo. La qualità superficiale e la necessità di post-cura sono discusse dalla guida universitaria. [S08 — Loughborough University — Vat Photopolymerisation](https://www.lboro.ac.uk/research/amrg/about/the7categoriesofadditivemanufacturing/vatphotopolymerisation/)
|
||||
|
||||
## Limiti e qualità del componente
|
||||
Una geometria corretta può ancora richiedere lavaggio e cura secondo le istruzioni della resina. Supporti e loro rimozione possono lasciare segni; cavità chiuse pongono il problema della resina intrappolata. I materiali vanno valutati per il loro comportamento a lungo termine, non solo appena stampati. La sequenza di lavorazione deve rimanere associata alla scheda materiale. [S08 — Loughborough University — Vat Photopolymerisation](https://www.lboro.ac.uk/research/amrg/about/the7categoriesofadditivemanufacturing/vatphotopolymerisation/)
|
||||
|
||||
**Ragionamento applicativo:** un modello estetico di una clip può essere convincente pur non replicando la durata a flessione della clip industriale. Per validare il montaggio basta forse la forma; per validare la vita utile servono una formulazione appropriata e prove ripetute. Il termine “funzionale” deve quindi essere completato con la funzione effettivamente verificata.
|
||||
|
||||
## Parametri da comprendere
|
||||
Spessore dello strato, energia di esposizione, uniformità luminosa, orientamento e strategia dei supporti non sono variabili indipendenti. Una sezione chiusa o una parete sottile possono reagire diversamente alla stessa impostazione. Registrare resina, lotto, temperatura e post-cura permette di attribuire correttamente le differenze. È una guida alla documentazione delle prove, non una ricetta di esposizione.
|
||||
|
||||
## Domande di ripasso
|
||||
- Perché la dimensione del pixel non coincide con la tolleranza del pezzo?
|
||||
- Qual è la differenza fra una resina caricata e una ceramica sinterizzata?
|
||||
- Una superficie liscia basta a dimostrare resistenza strutturale?
|
||||
|
||||
Collegamenti: [[AM07 - Material jetting]] · [[AM10 - Processi specialistici]] · [[Confronto tecnologie e materiali]]
|
||||
|
||||
|
||||
## Fonti e navigazione
|
||||
|
||||
Riferimenti di questa nota: [[AM90 - Fonti#S08|S08]], [[AM90 - Fonti#S09|S09]], [[AM90 - Fonti#S10|S10]], [[AM90 - Fonti#S11|S11]].
|
||||
|
||||
[[AM00 - Inizia qui|Indice del corso]] · [[AM90 - Fonti|Bibliografia e limiti delle fonti]]
|
||||
@@ -0,0 +1,53 @@
|
||||
---
|
||||
id: "am-course-am04"
|
||||
title: "Powder bed fusion dei metalli: LPBF, SLM, DMLS ed EB-PBF"
|
||||
type: "concetto"
|
||||
status: "da_verificare"
|
||||
created: "2026-09-10"
|
||||
updated: "2026-09-10"
|
||||
language: "it"
|
||||
tags: ["am/concetto", "am/processo"]
|
||||
aliases: ["LPBF", "SLM", "DMLS", "EBM", "EB-PBF", "PBF-LB/M"]
|
||||
sources: ["[[AM90 - Fonti#S12]]", "[[AM90 - Fonti#S13]]", "[[AM90 - Fonti#S14]]", "[[AM90 - Fonti#S15]]", "[[AM90 - Fonti#S16]]", "[[AM90 - Fonti#S17]]"]
|
||||
---
|
||||
|
||||
# Powder bed fusion dei metalli: LPBF, SLM, DMLS ed EB-PBF
|
||||
|
||||
## Il principio comune
|
||||
La macchina stende uno strato di polvere su una piattaforma. La sorgente energetica consolida selettivamente le regioni della sezione; la piattaforma avanza e la stesura si ripete. Nella LPBF metallica il laser produce un piccolo bagno fuso che solidifica, collegandosi alla parte sottostante. La polvere non consolidata viene rimossa al termine. NIST descrive e studia sia il processo di fusione sia la stesura, che determina le condizioni locali del letto. [S12 — NIST — Powder Bed Fusion](https://www.nist.gov/additive-manufacturing/research-areas/technologies/powder-bed-fusion)
|
||||
|
||||
## Nomenclatura: SLM e DMLS
|
||||
LPBF significa laser powder bed fusion. Si incontrano anche PBF-LB/M, laser beam su metallo, e nomi come SLM e DMLS. Non è corretto dedurre che ogni processo chiamato DMLS saldi soltanto particelle senza fusione: EOS colloca esplicitamente la propria tecnologia DMLS nella LPBF e oggi la descrive in termini di laser melting. Conviene identificare meccanismo, materiale e macchina, anziché affidarsi alla parola “sintering” presente nei nomi storici. [S13 — EOS — DMLS Metal 3D Printing](https://www.eos.info/about-us/what-we-do/dmls)
|
||||
|
||||
## Che cosa fa la macchina oltre a muovere il laser
|
||||
Il sistema di alimentazione, il recoater, l’atmosfera e la piattaforma termica contribuiscono al processo. Il fascio non incontra sempre lo stesso bersaglio: polvere, superficie consolidata, spruzzi e zone già riscaldate hanno condizioni diverse. Per questo potenza nominale e velocità non descrivono da sole il risultato. NIST misura proprio l’assorbimento dinamico della luce, che può variare rapidamente con superficie e geometria del bagno. [S12 — NIST — Powder Bed Fusion](https://www.nist.gov/additive-manufacturing/research-areas/technologies/powder-bed-fusion) [S15 — NIST — Measuring dynamic light absorption during laser welding and laser powder bed fusion](https://www.nist.gov/programs-projects/measuring-dynamic-light-absorption-during-laser-welding-and-laser-powder-bed)
|
||||
|
||||
## Materiali rappresentativi
|
||||
Acciai inossidabili e da utensili, leghe di titanio, alluminio, nichel, cobalto-cromo e rame sono esempi di famiglie presenti nei portafogli industriali. La loro disponibilità non significa che ogni lega della famiglia sia facile da stampare. Occorrono una polvere adeguata e una combinazione documentata di sistema e parametri; EOS distingue anche livelli diversi di maturità dei propri processi. Per il vault, “stampabile” deve quindi essere accompagnato da macchina o processo qualificato. [S14 — EOS — Metal Powder for 3D Printing](https://www.eos.info/metal-solutions/metal-materials)
|
||||
|
||||
## Difetti: una spiegazione causale
|
||||
**Mancanza di fusione, lack of fusion:** alcune regioni non vengono collegate adeguatamente. Il difetto può lasciare una discontinuità capace di concentrare le tensioni. **Pori da gas:** cavità intrappolate nel materiale. **Keyhole:** una cavità di vapore modifica la geometria e l’assorbimento del bagno; se instabile, può favorire l’intrappolamento di pori. NIST mostra difetti di mancata fusione sulle superfici di frattura e studia direttamente l’interazione fra cavità e luce. [S16 — NIST — Additive Manufacturing Fatigue and Fracture](https://www.nist.gov/programs-projects/additive-manufacturing-fatigue-and-fracture) [S15 — NIST — Measuring dynamic light absorption during laser welding and laser powder bed fusion](https://www.nist.gov/programs-projects/measuring-dynamic-light-absorption-during-laser-welding-and-laser-powder-bed)
|
||||
|
||||
Da qui segue un criterio ingegneristico: “più energia” non è sinonimo di “migliore”. Correggere un problema di legame può introdurre una diversa instabilità se si agisce senza comprendere il meccanismo. Una mappa di processo deve essere verificata sul materiale e sulla macchina, non copiata da una lega simile.
|
||||
|
||||
## EB-PBF: fascio elettronico
|
||||
Nella electron beam powder bed fusion la sorgente è un fascio di elettroni. Il funzionamento in vuoto e a temperature di processo elevate caratterizza le piattaforme industriali pertinenti. Colibrium descrive, per Q10plus, la lavorazione in vuoto ad alta temperatura e la riduzione delle tensioni residue. È una riduzione, non una prova di assenza assoluta di tensioni o difetti. Le applicazioni al titanio sono importanti, ma le disponibilità vanno verificate per macchina. [S17 — Colibrium Additive — Q10plus EB-PBF](https://www.colibriumadditive.com/printers/eb-pbf-printers/q10-plus)
|
||||
|
||||
Nel confronto con LPBF non basta domandare quale fascio sia “migliore”: occorre considerare dettaglio richiesto, superficie finale, materiali disponibili, gestione termica, rimozione della polvere e qualifica. La maggiore temperatura di costruzione cambia la storia del materiale e non rende automaticamente equivalenti i due processi.
|
||||
|
||||
## Vantaggi, limiti e post processing
|
||||
La libertà geometrica rende queste tecnologie interessanti per integrare funzioni e per forme difficili da ricavare per accesso diretto dell’utensile. EOS indica applicazioni aerospaziali, medicali, automobilistiche e negli utensili. [S13 — EOS — DMLS Metal 3D Printing](https://www.eos.info/about-us/what-we-do/dmls) Il confronto concreto deve includere supporti, accessibilità dei canali, superfici funzionali e controlli: un condotto realizzabile non è necessariamente pulibile o ispezionabile.
|
||||
|
||||
La sequenza dopo stampa va definita per il componente: rimozione della polvere, separazione dalla piattaforma, rimozione supporti, eventuali trattamenti e lavorazione delle quote critiche. Non assegnare una resistenza o una tolleranza senza chiarire lo stato finale. Un campione lucidato non descrive automaticamente una parete interna rimasta grezza.
|
||||
|
||||
## Esempio ragionato
|
||||
Per una staffa alleggerita, valuta prima il percorso dei carichi. Un reticolo che riduce massa può aggiungere superfici difficili da finire. La prova di trazione del materiale non risponde da sola alla domanda “quanto dura questa staffa?”. Servono prove coerenti con geometria, orientamento e uso. Questo esempio illustra un metodo di selezione, non una verifica progettuale.
|
||||
|
||||
Collegamenti: [[AM05 - PBF dei polimeri]] · [[AM08 - Deposizione a energia diretta]] · [[Confronto tecnologie e materiali]]
|
||||
|
||||
|
||||
## Fonti e navigazione
|
||||
|
||||
Riferimenti di questa nota: [[AM90 - Fonti#S12|S12]], [[AM90 - Fonti#S13|S13]], [[AM90 - Fonti#S14|S14]], [[AM90 - Fonti#S15|S15]], [[AM90 - Fonti#S16|S16]], [[AM90 - Fonti#S17|S17]].
|
||||
|
||||
[[AM00 - Inizia qui|Indice del corso]] · [[AM90 - Fonti|Bibliografia e limiti delle fonti]]
|
||||
@@ -0,0 +1,54 @@
|
||||
---
|
||||
id: "am-course-am05"
|
||||
title: "Powder bed fusion dei polimeri: SLS, MJF e SAF"
|
||||
type: "concetto"
|
||||
status: "da_verificare"
|
||||
created: "2026-09-10"
|
||||
updated: "2026-09-10"
|
||||
language: "it"
|
||||
tags: ["am/concetto", "am/processo"]
|
||||
aliases: ["SLS", "MJF", "SAF", "PBF polimerica"]
|
||||
sources: ["[[AM90 - Fonti#S18]]", "[[AM90 - Fonti#S19]]", "[[AM90 - Fonti#S20]]", "[[AM90 - Fonti#S38]]"]
|
||||
---
|
||||
|
||||
# Powder bed fusion dei polimeri: SLS, MJF e SAF
|
||||
|
||||
## Una famiglia, tre modalità di riscaldamento
|
||||
Qui il materiale costruttivo è una polvere polimerica. La polvere che circonda il pezzo normalmente lo sostiene senza supporti dedicati come quelli della stampa a resina. Il ciclo comprende stesura, riscaldamento selettivo e raffreddamento; l’estrazione avviene separando i pezzi dalla polvere restante. Questo permette di distribuire più oggetti nel volume di costruzione, ma richiede di poter rimuovere la polvere dalle geometrie interne. [S18 — Formlabs — Selective Laser Sintering: Complete Guide](https://formlabs.com/blog/what-is-selective-laser-sintering/)
|
||||
|
||||
## SLS: Selective Laser Sintering
|
||||
Il letto viene preriscaldato e il laser fornisce l’energia necessaria alle zone selezionate. Il raffreddamento controllato contribuisce alla stabilità geometrica. Nel linguaggio industriale moderno, SLS indica spesso i processi polimerici, mentre LPBF metallica indica la fusione laser dei metalli: condividono il letto di polvere, non tutti i dettagli termici o metallurgici. [S18 — Formlabs — Selective Laser Sintering: Complete Guide](https://formlabs.com/blog/what-is-selective-laser-sintering/)
|
||||
|
||||
**Lettura ingegneristica:** il tempo non è soltanto la scansione. Preparazione del letto, raffreddamento e depolverazione fanno parte del tempo necessario a disporre di pezzi utilizzabili. Una macchina veloce a fondere può lasciare un collo di bottiglia nelle operazioni successive.
|
||||
|
||||
## MJF: Multi Jet Fusion
|
||||
HP MJF deposita agenti sul letto: il fusing agent identifica le regioni da consolidare e il detailing agent modula il processo vicino ai dettagli. Una sorgente termica provoca la fusione selettiva. La testina non depone il volume del componente come nel material jetting: il materiale costruttivo è già nel letto. Non si tratta neppure di incollare una polvere come nel binder jetting. HP classifica MJF e SLS nella PBF. [S19 — HP — Comparing Binder Jetting, Material Jetting, MJF and SLS](https://www.hp.com/us-en/printers/3d-printers/learning-center/3d-print-binder-vs-material-jetting.html)
|
||||
|
||||
L’azione su aree estese modifica il rapporto fra complessità della sezione e tempo di fabbricazione. Non va tradotta automaticamente in un vantaggio di produttività per ogni ordine: contano riempimento della camera, altezza, materiale e disponibilità delle stazioni di raffreddamento e pulizia.
|
||||
|
||||
## SAF: Selective Absorption Fusion
|
||||
Stratasys SAF utilizza testine industriali per distribuire un fluido che aumenta l’assorbimento termico e una lampada infrarossa per consolidare le particelle selezionate. È quindi una PBF polimerica con assorbimento selettivo. Condivide con MJF l’idea di usare un agente e calore, ma non è lo stesso sistema: gestione della polvere, sequenza termica e materiali appartengono alla piattaforma specifica. [S20 — Stratasys — SAF Technology](https://www.stratasys.com/uk/guide-to-3d-printing/technologies-and-materials/saf-technology/)
|
||||
|
||||
## Materiali
|
||||
Per SLS, esempi diffusi sono PA12, PA11, TPU e polveri composite; il portafoglio concreto dipende dalla macchina. [S18 — Formlabs — Selective Laser Sintering: Complete Guide](https://formlabs.com/blog/what-is-selective-laser-sintering/) MJF utilizza anch’essa termoplastici in polvere, frequentemente poliammidi. [S19 — HP — Comparing Binder Jetting, Material Jetting, MJF and SLS](https://www.hp.com/us-en/printers/3d-printers/learning-center/3d-print-binder-vs-material-jetting.html) Non trasferire un grado fra SLS, MJF e SAF soltanto perché il nome chimico coincide: una polvere comprende anche caratteristiche di particella e comportamento termico.
|
||||
|
||||
Per costruire una scheda materiale utile, chiedi la compatibilità con la piattaforma, lo stato del materiale dopo stampa, il condizionamento e i dati di prova. Il marchio “nylon” da solo lascia aperte troppe variabili per un confronto strutturale.
|
||||
|
||||
## Superficie e post processing
|
||||
I pezzi estratti richiedono pulizia. Le superfici possono conservare una tessitura dovuta alle particelle; a seconda dell’obiettivo seguono trattamenti di finitura. HP descrive la presenza di polvere residua esposta in modo diverso ad agenti e calore: il materiale rimosso dal pezzo non va considerato identico, senza verifica, alla polvere nuova. [S38 — HP — 3D Printing Post-processing](https://www.hp.com/us-en/printers/3d-printers/learning-center/3d-printing-post-processing.html)
|
||||
|
||||
Tintura, rivestimento o levigatura devono comparire nello stato del componente quando se ne riportano prestazioni e dimensioni. Un miglioramento estetico non dimostra da solo il mantenimento di tutti i requisiti funzionali.
|
||||
|
||||
## Pro e contro nel progetto
|
||||
L’assenza ordinaria di supporti dedicati favorisce geometrie intricate e assemblaggi progettati con giochi. [S18 — Formlabs — Selective Laser Sintering: Complete Guide](https://formlabs.com/blog/what-is-selective-laser-sintering/) Restano da valutare estrazione della polvere, distorsione, superfici di contatto e costo dell’intero lotto. È scorretto dichiarare tutte queste parti perfettamente isotrope: i dati direzionali devono provenire dalla combinazione reale di sistema e materiale.
|
||||
|
||||
**Esempio ragionato:** per venti involucri differenti, la possibilità di riempire una camera con geometrie diverse può essere utile. Per un solo involucro urgente, attendere l’allestimento e il ciclo completo di una camera può cambiare la scelta. Non esiste una soglia di quantità valida per tutte le geometrie.
|
||||
|
||||
Collegamenti: [[AM04 - PBF dei metalli]] · [[AM06 - Binder jetting]] · [[AM07 - Material jetting]]
|
||||
|
||||
|
||||
## Fonti e navigazione
|
||||
|
||||
Riferimenti di questa nota: [[AM90 - Fonti#S18|S18]], [[AM90 - Fonti#S19|S19]], [[AM90 - Fonti#S20|S20]], [[AM90 - Fonti#S38|S38]].
|
||||
|
||||
[[AM00 - Inizia qui|Indice del corso]] · [[AM90 - Fonti|Bibliografia e limiti delle fonti]]
|
||||
@@ -0,0 +1,61 @@
|
||||
---
|
||||
id: "am-course-am06"
|
||||
title: "Binder jetting: polvere, legante e consolidamento"
|
||||
type: "concetto"
|
||||
status: "da_verificare"
|
||||
created: "2026-09-10"
|
||||
updated: "2026-09-10"
|
||||
language: "it"
|
||||
tags: ["am/concetto", "am/processo"]
|
||||
aliases: ["BJT", "Binder jetting", "Pezzo verde"]
|
||||
sources: ["[[AM90 - Fonti#S21]]", "[[AM90 - Fonti#S22]]", "[[AM90 - Fonti#S23]]"]
|
||||
---
|
||||
|
||||
# Binder jetting: polvere, legante e consolidamento
|
||||
|
||||
## Principio
|
||||
La macchina distribuisce una polvere e deposita selettivamente un legante liquido. Ripetendo i due passaggi si ottiene una forma tridimensionale. La testa definisce dove le particelle devono rimanere unite; il materiale circostante sostiene il volume durante la costruzione. La famiglia si distingue dalla fusione a letto di polvere perché la generazione iniziale della forma è affidata al legante. [S21 — Loughborough University — Binder Jetting](https://www.lboro.ac.uk/research/amrg/about/the7categoriesofadditivemanufacturing/binderjetting/)
|
||||
|
||||
## La domanda decisiva: quale oggetto esce dalla macchina?
|
||||
Nel binder jetting metallico esce un pezzo verde. La catena produttiva deve includere le operazioni che trasformano quella struttura in una parte metallica utilizzabile. La deposizione del legante e il consolidamento finale sono separati: il percorso digitale va preparato pensando anche al forno, come indica il materiale introduttivo Desktop Metal. [S22 — Desktop Metal — Introduction to the Binder Jetting Process](https://www.desktopmetal.com/resources/intro-binder-jet-3dprinting-process)
|
||||
|
||||
## Materiali e varianti applicative
|
||||
| Ambito | Che cosa viene formato | Passaggio da chiarire |
|
||||
|---|---|---|
|
||||
| Metalli | Polvere metallica legata | Debinding, sinterizzazione e possibili lavorazioni |
|
||||
| Ceramiche | Polvere ceramica legata | Consolidamento e ritiro specifici del sistema |
|
||||
| Sabbie da fonderia | Stampo o anima di sabbia legata | Requisiti dello stampo e successiva colata |
|
||||
| Modelli dimostrativi | Polveri e leganti formulati per il modello | Trattamento finale e limitazioni d’impiego |
|
||||
|
||||
Questi percorsi non sono equivalenti. Uno stampo stampato in sabbia serve a produrre un altro oggetto; non bisogna descriverlo come un componente metallico stampato direttamente. Le applicazioni dipendono dal sistema polvere-legante. [S21 — Loughborough University — Binder Jetting](https://www.lboro.ac.uk/research/amrg/about/the7categoriesofadditivemanufacturing/binderjetting/)
|
||||
|
||||
## Sinterizzazione: ritiro e deformazione
|
||||
Con il riscaldamento le particelle si consolidano e il corpo densifica. La geometria stampata deve anticipare il ritiro; non sempre basta ingrandire uniformemente il modello, perché peso, forma e sostegno possono influenzare la deformazione. Desktop Metal descrive ritiro, distorsione e uso di compensazioni geometriche e supporti di sinterizzazione. Le capacità di un software non eliminano la necessità di verificare il ciclo concreto. [S23 — Desktop Metal — Process Simulation and Sintering](https://www.desktopmetal.com/press/press-release-desktop-metal-launches-new-process-simulation-software-for-metal-additive-manufacturing-1)
|
||||
|
||||
La percentuale di ritiro non è una costante del binder jetting. Per usarla in un progetto occorrono almeno materiale, feedstock, geometria e ciclo. In queste dispense non viene proposta una percentuale generica da applicare ai CAD.
|
||||
|
||||
## Produttività: stampa e forno
|
||||
Le testine che agiscono su aree estese consentono di costruire più forme nello stesso letto; questa è una caratteristica del processo descritta da Desktop Metal. [S22 — Desktop Metal — Introduction to the Binder Jetting Process](https://www.desktopmetal.com/resources/intro-binder-jet-3dprinting-process) La produttività utile, però, è il numero di parti accettate per unità di tempo: se estrazione, manipolazione o forno non sostengono il flusso, la velocità di stampa non determina da sola il risultato economico.
|
||||
|
||||
## Parametri da documentare
|
||||
Per un confronto sperimentale registra polvere e granulometria dichiarata, legante, strato, strategia di deposizione, densità del verde, rimozione legante e ciclo termico. Registra anche orientamento in forno e superfici di appoggio. È una proposta di tracciabilità: non tutti i sistemi espongono gli stessi parametri all’operatore.
|
||||
|
||||
## Pro e contro dei componenti
|
||||
Il vantaggio potenziale è ottenere molte forme senza utensili dedicati alla geometria di ciascuna. Il limite principale da studiare nei metalli è la distanza fra forma verde e forma finale. Fragilità in manipolazione e deformazione durante il consolidamento devono essere gestite; la sola riuscita della stampa non conclude il processo. [S23 — Desktop Metal — Process Simulation and Sintering](https://www.desktopmetal.com/press/press-release-desktop-metal-launches-new-process-simulation-software-for-metal-additive-manufacturing-1)
|
||||
|
||||
**Esempio ragionato:** una piccola leva con un foro preciso può risultare stampabile, ma richiedere ripresa del foro dopo forno. Nel confronto con fresatura o MIM includi questa operazione e il suo posizionamento. Se il vantaggio resta solo nel prezzo della polvere, il confronto è incompleto.
|
||||
|
||||
## Errori da evitare
|
||||
- Confondere binder jetting e MJF perché entrambi usano testine.
|
||||
- Chiamare denso un pezzo solo perché mantiene la forma.
|
||||
- Applicare dati di uno stampo in sabbia a una lega sinterizzata.
|
||||
- Presentare la compensazione del ritiro come garanzia di ogni tolleranza.
|
||||
|
||||
Collegamenti: [[AM02 - Estrusione di materiale]] · [[AM05 - PBF dei polimeri]] · [[Confronto tecnologie e materiali]]
|
||||
|
||||
|
||||
## Fonti e navigazione
|
||||
|
||||
Riferimenti di questa nota: [[AM90 - Fonti#S21|S21]], [[AM90 - Fonti#S22|S22]], [[AM90 - Fonti#S23|S23]].
|
||||
|
||||
[[AM00 - Inizia qui|Indice del corso]] · [[AM90 - Fonti|Bibliografia e limiti delle fonti]]
|
||||
@@ -0,0 +1,52 @@
|
||||
---
|
||||
id: "am-course-am07"
|
||||
title: "Material jetting: gocce, fotopolimeri e multimateriale"
|
||||
type: "concetto"
|
||||
status: "da_verificare"
|
||||
created: "2026-09-10"
|
||||
updated: "2026-09-10"
|
||||
language: "it"
|
||||
tags: ["am/concetto", "am/processo"]
|
||||
aliases: ["MJT", "PolyJet", "Material jetting", "DOD"]
|
||||
sources: ["[[AM90 - Fonti#S24]]", "[[AM90 - Fonti#S25]]", "[[AM90 - Fonti#S26]]"]
|
||||
---
|
||||
|
||||
# Material jetting: gocce, fotopolimeri e multimateriale
|
||||
|
||||
## Come si costruisce la forma
|
||||
Una testa deposita gocce del materiale costruttivo sulle posizioni desiderate. Le gocce vengono consolidate e si ripete la deposizione sugli strati successivi. Il materiale può essere emesso in modo continuo oppure solo quando richiesto, modalità drop-on-demand. NIST presenta il principio e la relazione con il funzionamento delle testine inkjet. [S26 — NIST — Material Jetting](https://www.nist.gov/additive-manufacturing/research-areas/technologies/material-jetting)
|
||||
|
||||
La differenza rispetto al binder jetting è essenziale: nel MJT le gocce costituiscono il materiale della parte, mentre nel BJT uniscono una polvere già presente. La presenza di ugelli o della parola “jet” nel nome commerciale non basta a classificare una macchina.
|
||||
|
||||
## PolyJet e fotopolimeri
|
||||
Nei sistemi PolyJet si utilizzano fotopolimeri, con formulazioni rigide, trasparenti o rubber-like e possibilità di combinazioni compatibili con la piattaforma. Il catalogo Stratasys presenta, per esempio, famiglie flessibili e materiali per verifica del design. Si tratta di descrizioni del produttore: “simile alla gomma” non identifica automaticamente una gomma vulcanizzata, né garantisce lo stesso invecchiamento. [S25 — Stratasys — PolyJet Materials](https://www.stratasys.com/en/materials/materials-catalog/polyjet-materials/)
|
||||
|
||||
Il multimateriale permette di differenziare regioni di un modello. Per confrontare due parti occorre però sapere quali formulazioni sono state utilizzate e come sono state distribuite. Una miscela digitale non equivale a una nuova lega o a un termoplastico convenzionale solo perché imita una certa durezza.
|
||||
|
||||
## Materiali e condizioni di getto
|
||||
La formazione di gocce impone requisiti al fluido: viscosità e comportamento all’ugello condizionano deposizione e continuità. Fra gli esempi tradizionali figurano fotopolimeri e cere, con solidificazione o cura secondo il sistema. La guida universitaria tratta questi meccanismi e la necessità frequente di un materiale di supporto. [S24 — Loughborough University — Material Jetting](https://www.lboro.ac.uk/research/amrg/about/the7categoriesofadditivemanufacturing/materialjetting/)
|
||||
|
||||
Esistono sviluppi di getto con altre formulazioni; non sono qui equiparati alla stampa PolyJet. Per un sistema a particelle o sospensioni occorre verificare separatamente l’eventuale trattamento termico successivo.
|
||||
|
||||
## Supporti e accessibilità
|
||||
La deposizione di supporto consente di mantenere geometrie durante la costruzione; dopo stampa il supporto deve essere rimosso con il metodo previsto dal sistema. Questo requisito è discusso nella guida Loughborough. [S24 — Loughborough University — Material Jetting](https://www.lboro.ac.uk/research/amrg/about/the7categoriesofadditivemanufacturing/materialjetting/) Dal punto di vista progettuale, una cavità che non consente pulizia può annullare il beneficio della libertà geometrica. L’accesso per pulire va pensato prima della stampa.
|
||||
|
||||
## Per quali domande è utile
|
||||
Un modello multimateriale può essere particolarmente informativo per verificare forma, percezione tattile, trasparenze e accoppiamento fra regioni rigide e flessibili. Questi usi sono coerenti con il portafoglio per prototipazione del produttore. [S25 — Stratasys — PolyJet Materials](https://www.stratasys.com/en/materials/materials-catalog/polyjet-materials/) La domanda corretta resta: quale requisito sto validando? La somiglianza visiva non dimostra equivalenza strutturale.
|
||||
|
||||
## Limiti da valutare
|
||||
Prima di una scelta controlla stabilità nel tempo, ambiente di utilizzo, requisiti di finitura e costo del materiale di supporto. Per una valutazione economica registra anche pulizia, sprechi di cambio materiale e numero di pezzi accettati. Sono criteri di confronto, non valori universali del processo.
|
||||
|
||||
**Esempio ragionato:** per il prototipo di un’impugnatura, regioni rigide e morbide permettono una valutazione ergonomica. Se lo stesso oggetto deve poi lavorare per anni con oli, calore e serraggio, occorre una validazione diversa. Non trasferire l’esito della prova ergonomica alla durata in esercizio.
|
||||
|
||||
## Che cosa annotare nel vault
|
||||
Sistema, materiali e combinazioni, orientamento, supporti, pulizia, stato superficiale e data della prova. Per modelli multicolore, distingui valutazione cromatica e misura meccanica. Ogni risultato deve rimanere attribuito alla regione e alla formulazione corrispondenti.
|
||||
|
||||
Collegamenti: [[AM03 - Fotopolimerizzazione in vasca]] · [[AM06 - Binder jetting]] · [[Confronto tecnologie e materiali]]
|
||||
|
||||
|
||||
## Fonti e navigazione
|
||||
|
||||
Riferimenti di questa nota: [[AM90 - Fonti#S24|S24]], [[AM90 - Fonti#S25|S25]], [[AM90 - Fonti#S26|S26]].
|
||||
|
||||
[[AM00 - Inizia qui|Indice del corso]] · [[AM90 - Fonti|Bibliografia e limiti delle fonti]]
|
||||
@@ -0,0 +1,61 @@
|
||||
---
|
||||
id: "am-course-am08"
|
||||
title: "Directed energy deposition: laser, fascio elettronico e WAAM"
|
||||
type: "concetto"
|
||||
status: "da_verificare"
|
||||
created: "2026-09-10"
|
||||
updated: "2026-09-10"
|
||||
language: "it"
|
||||
tags: ["am/concetto", "am/processo"]
|
||||
aliases: ["DED", "LMD", "WAAM", "DED-arc"]
|
||||
sources: ["[[AM90 - Fonti#S27]]", "[[AM90 - Fonti#S28]]", "[[AM90 - Fonti#S29]]"]
|
||||
---
|
||||
|
||||
# Directed energy deposition: laser, fascio elettronico e WAAM
|
||||
|
||||
## La differenza rispetto al letto di polvere
|
||||
Nella DED il materiale viene alimentato nella zona in cui si concentra l’energia, e consolidato mentre viene depositato. La testa può aggiungere materiale su una base o su un componente esistente. NIST descrive il caso di alimentazione di polvere nel bagno generato dal laser: particelle e gas interagiscono con una superficie in evoluzione. [S27 — NIST — Directed Energy Deposition](https://www.nist.gov/additive-manufacturing/research-areas/technologies/directed-energy-deposition)
|
||||
|
||||
Il volume nasce seguendo cordoni e traiettorie, non fondendo una sezione all’interno di un letto già distribuito. Questo cambia accessibilità, dimensione del deposito e possibilità di lavorare su pezzi esistenti. La riparazione è fra gli usi caratteristici riportati da Loughborough. [S29 — Loughborough University — Directed Energy Deposition](https://www.lboro.ac.uk/research/amrg/about/the7categoriesofadditivemanufacturing/directedenergydeposition/)
|
||||
|
||||
## Varianti principali
|
||||
| Variante | Alimentazione e sorgente | Tema dominante |
|
||||
|---|---|---|
|
||||
| DED a laser con polvere | Polvere diretta verso il bagno laser | Cattura del materiale e stabilità del bagno |
|
||||
| DED a laser con filo | Filo e riscaldamento localizzato laser | Coordinamento fra avanzamento filo e traiettoria |
|
||||
| DED a fascio elettronico | Tipicamente filo, in ambiente appropriato al fascio | Gestione della camera e della costruzione |
|
||||
| DED-arc / WAAM | Filo e arco elettrico | Deposito di preforme e storia termica |
|
||||
|
||||
Le varianti condividono l’alimentazione localizzata, ma non vanno considerate intercambiabili. Una qualifica per una sorgente non qualifica automaticamente le altre. [S27 — NIST — Directed Energy Deposition](https://www.nist.gov/additive-manufacturing/research-areas/technologies/directed-energy-deposition) [S28 — TWI — Wire Arc Additive Manufacturing](https://www.twi-global.com/technical-knowledge/job-knowledge/arc-based-additive-manufacturing-137) [S29 — Loughborough University — Directed Energy Deposition](https://www.lboro.ac.uk/research/amrg/about/the7categoriesofadditivemanufacturing/directedenergydeposition/)
|
||||
|
||||
## WAAM: Wire Arc Additive Manufacturing
|
||||
WAAM utilizza la deposizione ad arco da filo per costruire una preforma. TWI impiega anche la denominazione DED-arc e ne descrive la capacità di avvicinarsi alla forma finale senza stampi complessi. L’interesse è forte per strutture in cui la produzione di un grezzo convenzionale e la successiva asportazione richiedono molto materiale o tempo. La dimensione del cordone e le lavorazioni finali devono entrare nel confronto. [S28 — TWI — Wire Arc Additive Manufacturing](https://www.twi-global.com/technical-knowledge/job-knowledge/arc-based-additive-manufacturing-137)
|
||||
|
||||
**Ragionamento:** per una nervatura estesa può essere accettabile depositare rapidamente materiale e fresare le facce finali. Per un microcanale, la stessa scala del deposito può essere incompatibile con il dettaglio richiesto. Non serve una graduatoria assoluta: servono requisiti geometrici.
|
||||
|
||||
## Materiali
|
||||
Si tratta prevalentemente di processi metallici. La scelta del filo o della polvere richiede compatibilità con sorgente, substrato e ciclo di deposito. Quando si aggiunge materiale a una parte esistente, il materiale del substrato partecipa al problema: la sola scheda del consumabile non descrive l’interfaccia ottenuta. Le possibilità di riparazione e aggiunta sono discusse dalla fonte universitaria. [S29 — Loughborough University — Directed Energy Deposition](https://www.lboro.ac.uk/research/amrg/about/the7categoriesofadditivemanufacturing/directedenergydeposition/)
|
||||
|
||||
Per documentare una lega nel vault, specifica forma di alimentazione e processo. Scrivere soltanto “titanio per DED” non permette di sapere se esista un processo validato per il sistema disponibile.
|
||||
|
||||
## Parametri e stabilità
|
||||
NIST studia gli effetti di potenza laser, portata di polvere, gas e distanza della testa dalla superficie, mostrando anche l’espulsione di particelle. Questi fattori influenzano l’ambiente del bagno e non devono essere ridotti a un solo parametro. [S27 — NIST — Directed Energy Deposition](https://www.nist.gov/additive-manufacturing/research-areas/technologies/directed-energy-deposition) Per WAAM, la gestione del cordone e della sequenza di costruzione va letta insieme alla necessità di ottenere una preforma ripetibile. [S28 — TWI — Wire Arc Additive Manufacturing](https://www.twi-global.com/technical-knowledge/job-knowledge/arc-based-additive-manufacturing-137)
|
||||
|
||||
Come schema di prova, registra anche temperatura tra passate, ordine delle traiettorie, condizioni della base e stato prima delle lavorazioni finali. Sono campi proposti per evitare confronti privi di contesto.
|
||||
|
||||
## Vantaggi e limiti
|
||||
Riparare una regione o aggiungere una funzione a un oggetto esistente può essere più interessante che produrlo interamente da zero. [S29 — Loughborough University — Directed Energy Deposition](https://www.lboro.ac.uk/research/amrg/about/the7categoriesofadditivemanufacturing/directedenergydeposition/) Il limite da valutare è l’intera interfaccia: geometria, continuità del deposito, materiale preesistente e accesso della testa. La riparazione di un componente non si considera validata soltanto perché la forma è stata ricostruita.
|
||||
|
||||
## Sistemi ibridi e post processing
|
||||
Un percorso additivo-sottrattivo può alternare deposizione e lavorazioni per raggiungere superfici o quote che la sola deposizione non fornisce. Per un preventivo tecnico va dichiarato ciò che viene misurato prima e dopo la lavorazione, non solo il tempo di arco acceso o laser acceso.
|
||||
|
||||
**Esempio ragionato:** per ricostruire una sede usurata, la decisione richiede materiale originale, causa dell’usura, volume da aggiungere, accesso per deposito e ripresa finale. Senza questi elementi “DED per riparazione” descrive una possibilità, non una soluzione già dimostrata.
|
||||
|
||||
Collegamenti: [[AM04 - PBF dei metalli]] · [[AM10 - Processi specialistici]] · [[Confronto tecnologie e materiali]]
|
||||
|
||||
|
||||
## Fonti e navigazione
|
||||
|
||||
Riferimenti di questa nota: [[AM90 - Fonti#S27|S27]], [[AM90 - Fonti#S28|S28]], [[AM90 - Fonti#S29|S29]].
|
||||
|
||||
[[AM00 - Inizia qui|Indice del corso]] · [[AM90 - Fonti|Bibliografia e limiti delle fonti]]
|
||||
@@ -0,0 +1,51 @@
|
||||
---
|
||||
id: "am-course-am09"
|
||||
title: "Sheet lamination: LOM e ultrasonic additive manufacturing"
|
||||
type: "concetto"
|
||||
status: "da_verificare"
|
||||
created: "2026-09-10"
|
||||
updated: "2026-09-10"
|
||||
language: "it"
|
||||
tags: ["am/concetto", "am/processo"]
|
||||
aliases: ["SHL", "LOM", "UAM", "Sheet lamination"]
|
||||
sources: ["[[AM90 - Fonti#S30]]", "[[AM90 - Fonti#S31]]"]
|
||||
---
|
||||
|
||||
# Sheet lamination: LOM e ultrasonic additive manufacturing
|
||||
|
||||
## Principio
|
||||
La forma viene ottenuta unendo fogli o nastri e sagomandoli. Il materiale non deve quindi arrivare come polvere o goccia: lo spessore del foglio contribuisce alla discretizzazione della costruzione. La famiglia comprende tecnologie molto diverse, fra cui laminated object manufacturing e ultrasonic additive manufacturing. [S30 — Loughborough University — Sheet Lamination](https://www.lboro.ac.uk/research/amrg/about/the7categoriesofadditivemanufacturing/sheetlamination/)
|
||||
|
||||
## LOM: Laminated Object Manufacturing
|
||||
Nei sistemi LOM classici, fogli, spesso di carta, vengono incollati e tagliati secondo le sezioni. Il materiale esterno alla parte deve poi essere separato. Le tecniche di suddivisione dello scarto ne facilitano la rimozione. Questi modelli sono utili soprattutto per rappresentazione della forma; non vanno equiparati a parti metalliche strutturali soltanto perché appartengono alla stessa famiglia additiva. [S30 — Loughborough University — Sheet Lamination](https://www.lboro.ac.uk/research/amrg/about/the7categoriesofadditivemanufacturing/sheetlamination/)
|
||||
|
||||
## UAM: Ultrasonic Additive Manufacturing
|
||||
Nastri metallici vengono uniti mediante azione ultrasonica e pressione, senza fondere globalmente il materiale. La lavorazione CNC può essere integrata per definire geometrie e rimuovere materiale. La descrizione universitaria menziona alluminio, rame, acciaio e titanio e la possibilità di combinare materiali, entro i limiti del processo di giunzione. [S30 — Loughborough University — Sheet Lamination](https://www.lboro.ac.uk/research/amrg/about/the7categoriesofadditivemanufacturing/sheetlamination/)
|
||||
|
||||
Il termine “bassa temperatura” è relativo ai processi di fusione e non significa assenza di sollecitazioni o necessità di controllo. Per confrontare componenti serve verificare l’unione tra strati, non solo conoscere le proprietà del nastro di partenza.
|
||||
|
||||
## Perché interessa per componenti multifunzionali
|
||||
NASA documenta un progetto di UAM per materiali strutturali con capacità integrate. Il valore è la possibilità di pensare alla struttura insieme alle funzioni incorporate, non solo come un blocco omogeneo. La scheda di progetto è evidenza di ricerca applicativa; non è una certificazione generale di qualunque componente costruito con UAM. [S31 — NASA TechPort — UAM with Embedded Capabilities](https://techport.nasa.gov/projects/90165)
|
||||
|
||||
## Come ragionare sui limiti
|
||||
La progettazione deve considerare l’accesso per unire i fogli, l’accesso dell’utensile per sagomare e la possibilità di liberare lo scarto. Se una cavità viene chiusa troppo presto, la successiva lavorazione può diventare impossibile. Questo è un criterio di pianificazione del processo: la sequenza di aggiunta e taglio fa parte della fattibilità geometrica.
|
||||
|
||||
Anche un materiale combinato va descritto come tale. Se due metalli sono uniti in strati, non basta assegnare al componente la resistenza di uno dei due: l’interfaccia e la direzione di carico richiedono una valutazione specifica.
|
||||
|
||||
## Esempio didattico
|
||||
Immagina un elemento che deve trasferire calore e contenere una funzione di misura. L’interesse della laminazione è poter ragionare su come costruire attorno a tale funzione. Le domande da risolvere sono: la sequenza consente l’inserimento, il processo danneggia l’elemento integrato, la struttura rimane ispezionabile e la riparazione è possibile? Sono domande progettuali, non la descrizione di un prototipo già verificato.
|
||||
|
||||
## Vantaggi e controindicazioni da confrontare
|
||||
La laminazione permette di partire da fogli e di integrare operazioni di taglio. Il valore applicativo è molto diverso fra un modello cartaceo e una struttura metallica unita. Per una scelta sensata confronta costo del materiale, qualità delle interfacce, scarto, accessibilità e proprietà nelle direzioni pertinenti. Una finitura esterna accurata non dimostra da sola integrità interna.
|
||||
|
||||
## Dati per il vault
|
||||
Registra metallo o foglio, spessore, condizioni di superficie, sistema di unione, sequenza di taglio, combinazioni di materiali, zone integrate e controlli delle interfacce. Questo elenco è una proposta di documentazione per rendere una futura scheda caso realmente utilizzabile.
|
||||
|
||||
Collegamenti: [[AM01 - Fondamenti e panoramica]] · [[AM10 - Processi specialistici]]
|
||||
|
||||
|
||||
## Fonti e navigazione
|
||||
|
||||
Riferimenti di questa nota: [[AM90 - Fonti#S30|S30]], [[AM90 - Fonti#S31|S31]].
|
||||
|
||||
[[AM00 - Inizia qui|Indice del corso]] · [[AM90 - Fonti|Bibliografia e limiti delle fonti]]
|
||||
@@ -0,0 +1,51 @@
|
||||
---
|
||||
id: "am-course-am10"
|
||||
title: "Processi specialistici e confini della manifattura additiva"
|
||||
type: "concetto"
|
||||
status: "da_verificare"
|
||||
created: "2026-09-10"
|
||||
updated: "2026-09-10"
|
||||
language: "it"
|
||||
tags: ["am/concetto", "am/processo"]
|
||||
aliases: ["Cold spray", "CSAM", "2PP", "CAL", "Stampa volumetrica"]
|
||||
sources: ["[[AM90 - Fonti#S33]]", "[[AM90 - Fonti#S34]]", "[[AM90 - Fonti#S35]]", "[[AM90 - Fonti#S36]]"]
|
||||
---
|
||||
|
||||
# Processi specialistici e confini della manifattura additiva
|
||||
|
||||
## Perché una nota separata
|
||||
Le sette famiglie sono una mappa utile; non esauriscono tutte le architetture ibride o le tecniche sperimentali. Qui sono raccolti metodi che richiedono cautele terminologiche o una scala di osservazione diversa. Non costituiscono una nuova tassonomia normativa.
|
||||
|
||||
## Cold spray additive manufacturing
|
||||
Nel cold spray particelle vengono accelerate da un gas e colpiscono il substrato allo stato solido. La deformazione intensa all’impatto favorisce il contatto e la formazione del deposito. TWI descrive rivestimenti, riparazioni e costruzioni near-net-shape, con metalli e alcune combinazioni specifiche. Il gas può essere riscaldato: “cold” non significa necessariamente ambiente freddo, ma distingue il meccanismo dalla deposizione basata sulla fusione delle particelle. [S33 — TWI — Cold Spraying](https://www.twi-global.com/what-we-do/research-and-technology/technologies/coating-and-surface-engineering/cold-spraying)
|
||||
|
||||
Il possibile vantaggio è limitare gli effetti associati al passaggio liquido-solido; la qualità dipende comunque da materiali e interfaccia. Non va assunto che ogni polvere metallica aderisca allo stesso modo o che un deposito sia automaticamente equivalente a un materiale massivo. Nel vault è utile registrare substrato, particelle, condizioni del gas e trattamenti finali. Queste sono domande di caratterizzazione, non parametri di esecuzione.
|
||||
|
||||
La collocazione del cold spray nei gruppi di AM allo stato solido varia fra le fonti: non lo si deve presentare senza precisazioni come una normale DED a fusione.
|
||||
|
||||
## Two-photon polymerization, 2PP
|
||||
La 2PP usa impulsi laser ultracorti per attivare una resina fotosensibile in un volume focalizzato molto piccolo. Nanoscribe descrive questa tecnologia per microfabbricazione: la localizzazione della trasformazione permette geometrie che richiedono una scala molto più fine di quella dei componenti meccanici ordinari. La scheda del produttore è un riferimento sul principio, non una misura comparativa universale. [S34 — Nanoscribe — Microfabrication Technologies](https://www.nanoscribe.com/en/microfabrication-technologies/)
|
||||
|
||||
La domanda progettuale cambia: dimensioni del campo, geometria ottica, rimozione del materiale non trasformato e misura del micro-oggetto possono contare più della massa depositata all’ora. Un processo eccellente per una microstruttura non diventa per questo conveniente per un involucro di grandi dimensioni. Non confondere dimensione del dettaglio, dimensione totale e tempo complessivo.
|
||||
|
||||
## Stampa volumetrica e computed axial lithography
|
||||
Le tecniche volumetriche combinano esposizioni nel volume, invece di completare necessariamente ogni strato prima del successivo. Toombs e colleghi descrivono micro-CAL con nanocomposito fotosensibile contenente silice, seguito da sinterizzazione, per ottenere geometrie in vetro. Il lavoro dimostra una specifica via sperimentale; non prova che resine opache o qualunque componente industriale siano immediatamente compatibili. [S35 — Toombs et al. — Volumetric AM of Silica Glass with micro-CAL](https://arxiv.org/abs/2110.01651)
|
||||
|
||||
L’interesse didattico è capire che “tipicamente strato su strato” descrive bene gran parte dell’AM, ma non ogni metodo emergente. Il problema si sposta su propagazione della luce, materiale, ricostruzione delle esposizioni e trasformazioni successive. Valutare separatamente forma appena ottenuta e materiale finale resta necessario.
|
||||
|
||||
## Direct ink writing e ceramiche
|
||||
Una sospensione concentrata deve fluire durante l’estrusione e conservare la geometria dopo. NIST studia la reologia delle sospensioni ceramiche e il monitoraggio dell’evoluzione del materiale. Questa famiglia di problemi mostra perché la “stampabilità” non si esaurisce nella possibilità di passare da un ugello: conta anche ciò che avviene dopo la deposizione. [S36 — NIST — Ceramic Additive Manufacturing](https://www.nist.gov/mml/mmsd/primary-focus-areas/ceramic-additive-manufacturing)
|
||||
|
||||
Per paste, biomateriali e materiali cementizi servono approfondimenti specifici su consolidamento, ambiente e requisiti d’uso. Queste dispense non trasferiscono a tali ambiti i dati dei polimeri o dei metalli; biostampa e stampa edilizia restano percorsi applicativi da sviluppare con fonti dedicate.
|
||||
|
||||
## Come valutare un annuncio di nuova tecnologia
|
||||
Chiedi quale materiale viene depositato, come si consolida, che cosa è stato realmente dimostrato e su quale geometria. Distingui un campione riuscito, una capacità ripetibile e un processo qualificato. Un nome nuovo può indicare una variante di esposizione o alimentazione, senza costituire un nuovo principio fisico.
|
||||
|
||||
Collegamenti: [[AM02 - Estrusione di materiale]] · [[AM03 - Fotopolimerizzazione in vasca]] · [[AM08 - Deposizione a energia diretta]]
|
||||
|
||||
|
||||
## Fonti e navigazione
|
||||
|
||||
Riferimenti di questa nota: [[AM90 - Fonti#S33|S33]], [[AM90 - Fonti#S34|S34]], [[AM90 - Fonti#S35|S35]], [[AM90 - Fonti#S36|S36]].
|
||||
|
||||
[[AM00 - Inizia qui|Indice del corso]] · [[AM90 - Fonti|Bibliografia e limiti delle fonti]]
|
||||
@@ -14,6 +14,9 @@ process: "binder jetting"
|
||||
|
||||
# Binder Jetting
|
||||
|
||||
> [!info] Vedi anche — riferimento primario aggiornato
|
||||
> [[AM06 - Binder jetting]] copre lo stesso processo con fonti più solide (Loughborough University, Desktop Metal) ed è la nota di riferimento primaria per questo tema. Questa nota resta come approfondimento basato su una singola fonte video.
|
||||
|
||||
## Principio e terminologia
|
||||
Famiglia di processo: binder jetting. Un letto di polvere viene steso a strati, come nella powder bed fusion; ma invece di fondere/sinterizzare la polvere con una sorgente di energia, una testina di stampa deposita selettivamente un legante liquido (binder) secondo il dato di layer 2D ricavato dallo slicing del modello CAD; il legante lega le particelle di polvere e successivamente viene curato con luce UV. [Fonte: modulo 2, [1:21:00]–[1:26:24]; [[SRC - freeCodeCamp GaugeHow - 3D Printing and Additive Manufacturing Full Course]]]
|
||||
|
||||
|
||||
@@ -14,6 +14,9 @@ process: "directed energy deposition"
|
||||
|
||||
# Directed Energy Deposition (DED) e sistemi ibridi
|
||||
|
||||
> [!info] Vedi anche — riferimento primario aggiornato
|
||||
> [[AM08 - Deposizione a energia diretta]] copre lo stesso processo con fonti più solide (NIST, TWI, Loughborough University) ed è la nota di riferimento primaria per questo tema. Questa nota resta come approfondimento basato su una singola fonte video.
|
||||
|
||||
## Principio e terminologia
|
||||
Famiglia di processo: directed energy deposition (DED), per metalli. Una testa (spesso montata su un braccio o tavola multi-asse) deposita materiale — polvere o filo metallico — mentre una sorgente di energia lo fonde e lo solidifica nella zona definita dal dato di layer 2D ricavato dallo slicing. [Fonte: modulo 2, [1:35:15]–[1:46:39]; [[SRC - freeCodeCamp GaugeHow - 3D Printing and Additive Manufacturing Full Course]]] Varianti citate:
|
||||
- **LMD (Laser Metal Deposition)**, anche note come **LENS** o **DMD**: polvere metallica fine (50–150 micron, dato indicativo del corso) erogata ed contestualmente fusa da una testa laser, in atmosfera di gas inerte protettivo.
|
||||
|
||||
@@ -16,14 +16,24 @@ sources: []
|
||||
Indice da sviluppare: Material extrusion; vat photopolymerization; powder bed fusion; binder jetting; material jetting; directed energy deposition; sheet lamination. Nomi e classificazione da documentare con fonti pertinenti.
|
||||
|
||||
## Note disponibili
|
||||
Riferimento primario (fonti NIST, Loughborough University, norme, produttori — vedi [[AM90 - Fonti]]):
|
||||
- [[AM02 - Estrusione di materiale]]
|
||||
- [[AM03 - Fotopolimerizzazione in vasca]]
|
||||
- [[AM04 - PBF dei metalli]]
|
||||
- [[AM05 - PBF dei polimeri]]
|
||||
- [[AM06 - Binder jetting]]
|
||||
- [[AM07 - Material jetting]]
|
||||
- [[AM08 - Deposizione a energia diretta]]
|
||||
- [[AM09 - Laminazione di fogli]]
|
||||
- [[AM10 - Processi specialistici]] (cold spray, 2PP/microfabbricazione, stampa volumetrica, ceramiche)
|
||||
|
||||
Note derivate dal corso video (approfondimento, vedi rimando alle note sopra):
|
||||
- [[VAT Photopolymerization (SLA, DLP, cDLP)]]
|
||||
- [[Powder Bed Fusion (SLS, SLM, DMLS, EBM)]]
|
||||
- [[Binder Jetting]]
|
||||
- [[Material Extrusion (FDM, FFF)]]
|
||||
- [[Directed Energy Deposition (DED) e sistemi ibridi]]
|
||||
|
||||
Material jetting e sheet lamination sono citate solo nella panoramica di classificazione ([[AM - Classificazione ASTM per i processi di stampa 3D]]): materiale insufficiente per una nota tecnologica dedicata, da completare con fonti aggiuntive.
|
||||
|
||||
## Domande da sviluppare
|
||||
- Quali concetti e definizioni servono per questo ambito?
|
||||
- Quali fonti primarie sostengono le affermazioni?
|
||||
|
||||
@@ -14,6 +14,9 @@ process: "material extrusion"
|
||||
|
||||
# Material Extrusion (FDM, FFF)
|
||||
|
||||
> [!info] Vedi anche — riferimento primario aggiornato
|
||||
> [[AM02 - Estrusione di materiale]] copre lo stesso processo con fonti più solide (Loughborough University, NIST, Prusa, Markforged) ed è la nota di riferimento primaria per questo tema. Questa nota resta come approfondimento basato su una singola fonte video.
|
||||
|
||||
## Principio e terminologia
|
||||
Famiglia di processo: material extrusion, nota commercialmente come FDM (Fused Deposition Modeling) o FFF (Fused Filament Fabrication) — nomi usati come sinonimi nel corso. Un filamento termoplastico viene alimentato tramite rulli a un ugello riscaldato (hotend), che lo fonde e lo depone selettivamente strato per strato, secondo il dato di layer 2D ricavato dallo slicing del modello CAD; a ogni strato completato, la piattaforma scende (o l'estrusore sale) di uno spessore layer. [Fonte: modulo 2, [1:26:57]–[1:34:50]; [[SRC - freeCodeCamp GaugeHow - 3D Printing and Additive Manufacturing Full Course]]]
|
||||
|
||||
|
||||
@@ -14,6 +14,9 @@ process: "powder bed fusion"
|
||||
|
||||
# Powder Bed Fusion (SLS, SLM, DMLS, EBM)
|
||||
|
||||
> [!info] Vedi anche — riferimento primario aggiornato
|
||||
> [[AM04 - PBF dei metalli]] e [[AM05 - PBF dei polimeri]] coprono lo stesso processo (separando metalli e polimeri per evitare confronti impropri) con fonti più solide (NIST, EOS, Formlabs, HP, Colibrium) e sono i riferimenti primari per questo tema. Questa nota resta come approfondimento basato su una singola fonte video.
|
||||
|
||||
## Principio e terminologia
|
||||
Famiglia di processo: powder bed fusion (PBF). Un letto di polvere viene steso a strati; una sorgente di energia (laser nella maggioranza dei casi, o fascio elettronico) fonde o sinterizza selettivamente le particelle di polvere secondo il dato di layer; dopo ogni strato la piattaforma scende di uno spessore layer e un rullo/lama stende nuova polvere. [Fonte: modulo 2, [1:09:53]–[1:20:36]; [[SRC - freeCodeCamp GaugeHow - 3D Printing and Additive Manufacturing Full Course]]] Varianti/nomi commerciali citati:
|
||||
- **SLS (Selective Laser Sintering)**: sinterizzazione laser selettiva, per polimeri termoplastici (es. nylon, alumide).
|
||||
|
||||
@@ -14,6 +14,9 @@ process: "vat photopolymerization"
|
||||
|
||||
# VAT Photopolymerization (SLA, DLP, cDLP)
|
||||
|
||||
> [!info] Vedi anche — riferimento primario aggiornato
|
||||
> [[AM03 - Fotopolimerizzazione in vasca]] copre lo stesso processo con fonti più solide (NIST, Loughborough University, Formlabs, Lithoz) ed è la nota di riferimento primaria per questo tema. Questa nota resta come approfondimento basato su una singola fonte video.
|
||||
|
||||
## Principio e terminologia
|
||||
Famiglia di processo: vat photopolymerization. Una resina fotopolimerica liquida contenuta in una vasca viene polimerizzata (curata) selettivamente da una sorgente luminosa; a curing avvenuto il materiale diventa un polimero solido. Varianti citate nel corso, distinte per sorgente/modalità di energia: [Fonte: modulo 2, [1:00:51]–[1:09:27]; [[SRC - freeCodeCamp GaugeHow - 3D Printing and Additive Manufacturing Full Course]]]
|
||||
- **SLA (Stereolithography Apparatus / stereolitografia)**: sorgente laser che cura la resina punto per punto tramite specchio mobile; piattaforma capovolta che risale strato dopo strato.
|
||||
|
||||
@@ -24,6 +24,9 @@ Indice da sviluppare: Orientamento; supporti; tolleranze; reticoli; ottimizzazio
|
||||
- [[Regole di progettazione DFAM]]
|
||||
- [[Ottimizzazione topologica e design generativo (simulation-driven design)]]
|
||||
- [[Approccio a tre livelli al DFAM - caso studio pedale del freno]]
|
||||
- [[Strutture con smorzamento a particelle (particle damping)]]
|
||||
- [[Regole dimensionali DfAM - overhang, pareti, fori e gap]] (guida produttore ADDMAN)
|
||||
- [[Regole di progettazione e difetti tipici per processo (guida ADDMAN)]] (guida produttore ADDMAN)
|
||||
|
||||
## Domande da sviluppare
|
||||
- Quali concetti e definizioni servono per questo ambito?
|
||||
|
||||
@@ -13,6 +13,9 @@ sources: ["[[SRC - freeCodeCamp GaugeHow - 3D Printing and Additive Manufacturin
|
||||
|
||||
# Regole di progettazione DFAM (limiti e linee guida)
|
||||
|
||||
> [!info] Vedi anche — soglie dimensionali più dettagliate
|
||||
> [[Regole dimensionali DfAM - overhang, pareti, fori e gap]] e [[Regole di progettazione e difetti tipici per processo (guida ADDMAN)]] forniscono soglie numeriche concrete (spessori minimi, angoli, dimensioni di fori) da una guida di produttore, complementari alle regole generali qualitative di questa nota.
|
||||
|
||||
## In breve
|
||||
Il Design for Additive Manufacturing (DFAM) è l'insieme di modifiche geometriche che si applicano a un modello CAD per renderlo compatibile con i limiti fisici del processo di stampa 3D scelto (in particolare la necessità di supporti per feature poco inclinate, fori grandi e overhang), riducendo il rischio di fallimento del build e la quantità di post-processing richiesta. [Fonte: modulo 7, sezione 1, [4:34:53]–[4:44:15]; [[SRC - freeCodeCamp GaugeHow - 3D Printing and Additive Manufacturing Full Course]]]
|
||||
|
||||
|
||||
+53
@@ -0,0 +1,53 @@
|
||||
---
|
||||
id: "am-regole-progettazione-difetti-per-processo-addman"
|
||||
title: "Regole di progettazione e difetti tipici per processo (guida ADDMAN)"
|
||||
type: "concetto"
|
||||
status: "da_verificare"
|
||||
created: "2026-09-10"
|
||||
updated: "2026-09-10"
|
||||
language: "it"
|
||||
tags: ["am/concetto"]
|
||||
aliases: []
|
||||
sources: ["[[SRC - ADDMAN 2024 - A Guide to Designing for Additive Manufacturing]]"]
|
||||
---
|
||||
|
||||
# Regole di progettazione e difetti tipici per processo (guida ADDMAN)
|
||||
|
||||
## In breve
|
||||
Panoramica per le 5 famiglie di processo AM (material extrusion, vat polymerization, material jetting, binder jetting, powder bed fusion) di produttori di macchine, materiali comuni, fasce di costo indicativo e modalità di difetto/considerazioni di progettazione tipiche, secondo la guida di produttore ADDMAN. Da leggere insieme alle note tecnologiche di riferimento primario per ciascun processo (AM02–AM06) per il principio di funzionamento. [Fonte: guida di produttore; [[SRC - ADDMAN 2024 - A Guide to Designing for Additive Manufacturing]]]
|
||||
|
||||
## Spiegazione
|
||||
### Material extrusion (FDM) — vedi [[AM02 - Estrusione di materiale]]
|
||||
Orientamento critico per minimizzare i supporti e massimizzare la resistenza: parti più forti nel piano XY, più deboli in trazione lungo Z. Buona pratica: sovradimensionare i fori e trapanarli alla misura corretta dopo la stampa; filettature meglio ottenute con inserti filettati per accuratezza. Gli spigoli tendono ad arrotondarsi per effetto del tipo di ugello. Larghezza del cordone/feature minima generalmente ≈2× il diametro dell'ugello.
|
||||
|
||||
### Vat polymerization (SLA/DLP) — vedi [[VAT Photopolymerization (SLA, DLP, cDLP)]]
|
||||
Sezioni trasversali più ampie richiedono forze maggiori per il distacco dal film e supporti più densi, oltre a tempi di attesa più lunghi per il flusso del materiale. Rischio di "cupping": geometrie che intrappolano aria tra resina e film, impedendo il corretto flusso della resina e causando fallimenti di stampa — mitigabile con fori di drenaggio/sfiato progettati appositamente nelle cavità interne.
|
||||
|
||||
Volumi di stampa industriali indicati: desktop fino a 150×150×200 mm, professionale fino a ~300 cm³, industriale fino a ~1 m³. Produttori citati: Stratasys, Nexa3D, Formlabs, Astra3D, Carbon, 3D Systems. Materiali comuni: resine fotopolimeriche (tipicamente proprietarie del produttore macchina), cere colabili, trasparenti, rigide/tough, biocompatibili. Fascia di costo macchina indicativa: entry level <1.000 $, prosumer 5.000–10.000 $, industriale 20.000–1.000.000+ $.
|
||||
|
||||
### Material jetting (PolyJet) — vedi [[Material jetting]]
|
||||
Parti generalmente più fragili delle controparti in nylon/ABS, per la natura della resina acrilica; bassa tolleranza termica e minima elongazione nei materiali rubber-like, che ne limitano l'uso in test funzionali e applicazioni reali. Impostazione "matte": aggiunge un sottile strato di supporto su tutta la superficie indipendentemente da orientamento/necessità. Impostazione "glossy": supporto solo dove strutturalmente richiesto. Dettagli incisi/in rilievo, pareti, fori e perni: dimensione minima consigliata 0,5 mm (profondità/spessore/diametro).
|
||||
|
||||
Volumi di stampa: professionale fino a 100×100×50 mm, industriale fino a 508×508×305 mm. Produttori citati: Stratasys, HP. Materiali comuni: fotopolimeri proprietari (standard/rigido, tipo ABS, tipo PP, alta temperatura, colabile, biocompatibile). Fascia di costo macchina: professionale 50.000–100.000 $, industriale 100.000–1.000.000 $.
|
||||
|
||||
### Binder jetting — vedi [[AM06 - Binder jetting]] e [[Binder Jetting]]
|
||||
Progettazione per il ritiro: la sinterizzazione riduce il volume del pezzo del 15–16%, ma il ritiro è dichiarato prevedibile, ripetibile e modellabile in software, permettendo precisione dimensionale fine nonostante il cambio di dimensione. Libertà geometrica quasi completa: canali interni complessi, reticoli, spigoli vivi, meccanismi incapsulati. Porosità: la contrazione dal pezzo verde al pezzo sinterizzato finale comporta tipicamente un grado elevato di porosità residua, da considerare per applicazioni critiche (aerospaziale, medicale).
|
||||
|
||||
Volumi di stampa: sviluppo fino a 100×200×100 mm, sistemi di produzione metallici fino a 1×1×1 m, sistemi per sabbia fino a 2×2×1 m, sistemi polimerici fino a 380×380×380 mm. Produttori citati: HP, GE, ExOne, Rapidia, Desktop Metal. Materiali comuni: acciaio inox 316L, maraging steel, 17-4PH, nichel 625/718, rame, sabbia, nylon. Fascia di costo macchina industriale: 50.000–1.000.000+ $.
|
||||
|
||||
### Powder bed fusion (metallo e polimero) — vedi [[AM04 - PBF dei metalli]], [[AM05 - PBF dei polimeri]] e [[Powder Bed Fusion (SLS, SLM, DMLS, EBM)]]
|
||||
Prevenzione del warping: parti lunghe e piatte oltre ~15 cm (6") sono indicate come inclini alla deformazione; consigliata consultazione con un ingegnere AM esperto per capire come le parti possono deformarsi. Risoluzione delle feature: consigliato progettare feature >0,7 mm. Progettazione per la rimozione della polvere: da considerare in fase di progetto (SLS richiede rimozione della polvere da tutte le superfici del pezzo). Overhang e supporti ("ancore"): necessari per mitigare il warping e ancorare il pezzo al piatto di build; la loro rimozione post-stampa può influenzare la finitura superficiale. Tensioni residue: causa di warping o cricche per raffreddamento non uniforme. Finitura superficiale: i pezzi as-built hanno tipicamente superficie ruvida, spesso da post-processare.
|
||||
|
||||
Volumi di stampa per fascia di potenza laser: piccola (100–200 W) fino a 150×150×150 mm, media (200–500 W) fino a 350×350×400 mm, grande (500–1200 W) fino a 600×600×1000 mm. Produttori citati: EOS, Velo3D, Renishaw, GE Additive, TRUMPF, SLM Solutions, DMG Mori, 3D Systems, AddUp. Materiali comuni: metallo (316L, maraging steel, 17-4PH, nichel 625, Ti64, cobalto-cromo) e polimero (AlSi10Mg — probabile errore di categorizzazione nella fonte, l'AlSi10Mg è una lega di alluminio non un polimero, **segnalato come anomalia da verificare**; nylon, PEEK, PEKK, TPU, TPE, polipropilene). Fascia di costo macchina: entry level ~30.000 $, industriale 20.000–2.000.000+ $.
|
||||
|
||||
## Condizioni di applicazione
|
||||
Ogni sezione di questa nota è specifica per la famiglia di processo indicata: non trasferire una regola (es. spessore minimo feature, soglia di warping) da un processo all'altro. I produttori di macchine e le fasce di costo elencate sono un'istantanea indicativa del mercato al momento della pubblicazione della guida (2024): da aggiornare con fonti correnti prima di un uso commerciale.
|
||||
|
||||
## Dati o formule
|
||||
Vedi le soglie numeriche riportate per processo nella sezione "Spiegazione" sopra. Tutte le cifre sono **dati di produttore (ADDMAN), non verificati indipendentemente in questa nota**.
|
||||
|
||||
## Esempio
|
||||
Non applicabile (nota di panoramica per processo, non caso applicativo documentato).
|
||||
|
||||
## Fonti e collegamenti
|
||||
[[SRC - ADDMAN 2024 - A Guide to Designing for Additive Manufacturing]] · [[RIA - ADDMAN 2024 - A Guide to Designing for Additive Manufacturing]] · [[Regole dimensionali DfAM - overhang, pareti, fori e gap]] · [[Indice - Progettazione DfAM]] · [[Indice - Processi]]
|
||||
@@ -0,0 +1,61 @@
|
||||
---
|
||||
id: "am-regole-dimensionali-dfam-overhang-pareti-fori"
|
||||
title: "Regole dimensionali DfAM: overhang, pareti, fori e gap"
|
||||
type: "concetto"
|
||||
status: "da_verificare"
|
||||
created: "2026-09-10"
|
||||
updated: "2026-09-10"
|
||||
language: "it"
|
||||
tags: ["am/concetto"]
|
||||
aliases: ["Regola dei 45 gradi", "45 degree rule", "Overhang rule", "Minimum wall thickness AM"]
|
||||
sources: ["[[SRC - ADDMAN 2024 - A Guide to Designing for Additive Manufacturing]]"]
|
||||
---
|
||||
|
||||
# Regole dimensionali DfAM: overhang, pareti, fori e gap
|
||||
|
||||
## In breve
|
||||
Regole pratiche di progettazione per feature dimensionali critiche in stampa 3D: angolo di overhang senza supporto (regola dei 45°), spessore minimo delle pareti verticali e dimensione minima/massima di fori e gap. Sono regole pratiche di un produttore (ADDMAN), non tolleranze normative: valide come punto di partenza, da verificare con il fornitore/macchina specifico prima di un uso in produzione. [Fonte: guida di produttore; [[SRC - ADDMAN 2024 - A Guide to Designing for Additive Manufacturing]]]
|
||||
|
||||
## Spiegazione
|
||||
### Overhang e regola dei 45°
|
||||
Gli overhang — sezioni del pezzo che sporgono senza materiale sottostante — tendono a cedimento (drooping, per raffreddamento insufficiente prima della solidificazione) o curling (sollevamento dei bordi per raffreddamento non uniforme) se non supportati adeguatamente. La regola pratica generale: overhang con angolo ≤45° rispetto al piano di build non richiedono tipicamente supporti; oltre questa soglia il supporto diventa necessario.
|
||||
|
||||
Considerazioni specifiche per processo/materiale:
|
||||
- **Metallo (powder bed fusion)**: uno spessore maggiore della parete centrale (core wall) consente overhang leggermente più ampi, ma anche con spessore ottimale gli overhang oltre 3 mm sono inclini a deformazione.
|
||||
- **Material extrusion (FDM)**: overhang fino a circa 2–3 larghezze di cordone sono generalmente gestibili senza supporto; oltre, il rischio di cedimento/drooping aumenta.
|
||||
- **SLS (powder bed fusion polimerica)**: può non richiedere supporti, a differenza della maggior parte degli altri processi (la polvere circostante non fusa funge da supporto naturale).
|
||||
|
||||
I compromessi legati ai supporti: tempo di stampa e materiale aggiuntivo, lavoro di rimozione post-stampa, possibile degrado della finitura superficiale nelle zone di contatto.
|
||||
|
||||
### Pareti verticali: spessore minimo e aspect ratio
|
||||
Le pareti verticali (perpendicolari al piatto di stampa) tendono a essere strutturalmente più stabili delle pareti angolate, permettendo profili più sottili. Soglie pratiche indicate:
|
||||
- Spessore **sotto 0,5 mm**: feature a rischio di incoerenze o fallimento di stampa.
|
||||
- Spessore **sotto 2 mm**: consigliata consultazione con un ingegnere AM esperto per valutare fattibilità, modifiche necessarie o strutture di supporto.
|
||||
- Pareti sottili, anche se stampate con successo, possono presentare fragilità in post-processing (rischio di rottura durante pulizia/finitura).
|
||||
- Esistono limitazioni di altezza per pareti oltre 2 mm di spessore, dipendenti dalla tecnologia specifica (non quantificate nella fonte).
|
||||
|
||||
### Fori e gap
|
||||
- **Fori orizzontali**: tipicamente richiedono strutture di supporto interne; geometrie alternative (goccia, diamante, ovale) possono eliminare la necessità di supporto e ridurre il lavoro di post-processing.
|
||||
- **Filettature**: possono essere stampate ma con precisione inferiore a filettature lavorate o stampate a iniezione; per applicazioni ad alta precisione/durata, preferibili inserti filettati.
|
||||
- **Fori verticali**: generalmente visibili nell'intervallo 0,5–1 mm; fori più piccoli a rischio di intasamento da polvere residua (processi a letto di polvere).
|
||||
- **Fori orizzontali — soglie dimensionali**: sotto 4–5 layer di diametro possono non essere visibili; sotto 10–15 layer possono uscire deformati (a diamante) o non funzionali, a seconda di processo/materiale; sopra 8 mm di diametro possono perdere la forma circolare; deformità significative possono causare il fallimento dell'intera build.
|
||||
- **Gap funzionali**: la spaziatura tra pareti deve tenere conto del rigonfiamento dei bordi (edge swelling) e della rimozione di polvere/fibre residue; il gap necessario dipende dai parametri di stampa e tende a crescere con lo spessore della parte circostante (vale anche per fori lungo l'asse Z).
|
||||
- **Fori angolati**: tendono a allungarsi durante la stampa rispetto alla dimensione di progetto, per effetto dell'inclinazione rispetto al piatto di build.
|
||||
|
||||
## Condizioni di applicazione
|
||||
Regole generali di produttore, senza associazione esplicita a una macchina, materiale o set di parametri di processo specifico: da trattare come punto di partenza indicativo, non come tolleranza garantita. Vanno verificate con il fornitore/macchina specifico prima dell'uso in produzione, specialmente per applicazioni critiche.
|
||||
|
||||
## Dati o formule
|
||||
Soglie numeriche citate (tutte **dato di produttore, non verificato indipendentemente**):
|
||||
- Overhang senza supporto: ≤45° dal piano di build (regola generale).
|
||||
- Overhang in metallo: rischio di deformazione oltre 3 mm anche con parete centrale ottimizzata.
|
||||
- Overhang FDM: gestibile fino a ~2–3 larghezze di cordone.
|
||||
- Spessore parete minimo: 0,5 mm (soglia di rischio), 2 mm (soglia di consultazione ingegneristica).
|
||||
- Fori verticali: visibilità tipica 0,5–1 mm.
|
||||
- Fori orizzontali: soglia di visibilità/funzionalità 4–5 e 10–15 layer di diametro; perdita di forma circolare sopra 8 mm.
|
||||
|
||||
## Esempio
|
||||
Non applicabile (nota di regole dimensionali generali, non caso applicativo documentato).
|
||||
|
||||
## Fonti e collegamenti
|
||||
[[SRC - ADDMAN 2024 - A Guide to Designing for Additive Manufacturing]] · [[RIA - ADDMAN 2024 - A Guide to Designing for Additive Manufacturing]] · [[Regole di progettazione e difetti tipici per processo (guida ADDMAN)]] · [[Orientamento e strutture di supporto]] · [[Regole di progettazione DFAM]] · [[Indice - Progettazione DfAM]]
|
||||
@@ -0,0 +1,42 @@
|
||||
---
|
||||
id: "am-particle-damping-strutture-am"
|
||||
title: "Strutture con smorzamento a particelle (particle damping) per AM"
|
||||
type: "concetto"
|
||||
status: "da_verificare"
|
||||
created: "2026-09-10"
|
||||
updated: "2026-09-10"
|
||||
language: "it"
|
||||
tags: ["am/concetto"]
|
||||
aliases: ["Particle damping", "AMPD", "Smorzamento a particelle", "Retained powder damping"]
|
||||
sources: ["[[SRC - Yu et al. 2026 - Additively Manufactured Particle Damping Structures Review]]"]
|
||||
process: "powder bed fusion (PBF-LB/M metallico), tecnica di progettazione DfAM"
|
||||
---
|
||||
|
||||
# Strutture con smorzamento a particelle (particle damping) per AM
|
||||
|
||||
## In breve
|
||||
Il particle damping è una tecnica di smorzamento passivo delle vibrazioni in cui l'energia vibrazionale viene dissipata dal movimento relativo, dagli urti e dall'attrito di particelle libere all'interno di una cavità. La manifattura additiva permette di integrare questa cavità direttamente nel componente stampato — progettata insieme al percorso di carico strutturale — invece di aggiungere un dispositivo di smorzamento separato, dando origine alle "additively manufactured particle damping structures" (AMPD). [Fonte: review sistematica; [[SRC - Yu et al. 2026 - Additively Manufactured Particle Damping Structures Review]], §1]
|
||||
|
||||
## Spiegazione
|
||||
Esistono due famiglie principali di approccio, con controllo diverso sul mezzo smorzante: [§3]
|
||||
- **Direct retained-powder**: la polvere metallica non fusa durante la stampa PBF-LB/M viene trattenuta all'interno di cavità sigillate. Si distingue tra cavità semplici senza struttura interna progettata, e cavità con strutture interne progettate (partizioni, nervature, reticoli, sottostrutture risonanti), che aggiungono una variabile di controllo ulteriore su come il volume di polvere è distribuito.
|
||||
- **Post-filled**: l'AM crea la struttura ospite (cavità, inserto o modulo), mentre il mezzo smorzante (particelle) viene introdotto e sigillato dopo la fabbricazione, con controllo indipendente su morfologia e rapporto di riempimento delle particelle.
|
||||
|
||||
Due assi di progetto per gli approcci a polvere trattenuta diretta: posizionamento della cavità (in base al modo vibrazionale target, all'asse neutro, a cavità multiple distribuite, o al layout del componente) e design interno della cavità (semplice, suddivisa, con elementi interni, reticolo, risonatore locale). Il posizionamento della cavità può contare quanto il suo volume, perché la polvere trattenuta deve potersi muovere relativamente alle pareti della cavità sotto la sollecitazione attiva. [§4]
|
||||
|
||||
La mobilità della polvere — non solo la sua presenza — determina se lo smorzamento si attiva: uno studio citato nella review (Westbeld et al., non verificato direttamente in questa nota) confronta provini in AlSi10Mg con polvere mobile o sinterizzata rispetto a riferimenti solidi, trovando che la sinterizzazione globale non produce smorzamento significativo, mentre la polvere mobile produce un aumento del fattore di perdita relativo fino al 1425% (**dato citato dalla review, non verificato alla fonte primaria**). [§3, Tabella 2]
|
||||
|
||||
## Condizioni di applicazione
|
||||
Tecnica applicabile principalmente a componenti realizzati per powder bed fusion laser di metalli (PBF-LB/M), dove la polvere non fusa è già presente come sottoprodotto del processo e può essere intenzionalmente trattenuta in cavità progettate. La risposta di smorzamento dipende fortemente da: materiale e stato della polvere (dimensione particelle, distribuzione, densità di impaccamento, compattazione), geometria e posizionamento della cavità, ampiezza e tipo di eccitazione (a bassa ampiezza la polvere può muoversi solidalmente con le pareti e dissipare poco; con ampiezza crescente aumentano scorrimento e urti, fino a saturazione/comportamenti non lineari). La review segnala che rapporto di riempimento, densità di impaccamento e percentuale di polvere non fusa sono grandezze correlate ma distinte, da non trattare come intercambiabili. [§4, §5]
|
||||
|
||||
## Dati o formule
|
||||
Nessuna formula generale fornita dalla review. Esempi quantitativi citati (tutti "dato citato dalla review, non verificato alla fonte primaria originale"):
|
||||
- Provini AlSi10Mg con polvere mobile: incremento massimo del fattore di perdita relativo ~1425% rispetto a riferimento solido, sotto chirp periodico a 800 mm/s² nell'intervallo 50–8000 Hz. Polvere sinterizzata: nessuno smorzamento significativo. [Tabella 2, Westbeld et al.]
|
||||
- Pale in IN718 con tasche interne di polvere trattenuta vs pale completamente fuse: fattore di qualità ridotto di circa il 45% e 60% su due modi, con aumento della resistenza a fatica. [Tabella 2, Scott-Emuakpor et al.]
|
||||
- Utensile TPMS post-filled: con 145 g di massa di riempimento, rapporto di smorzamento 0,03 ed efficienza di dissipazione energetica 48%; a basso riempimento l'utensile può avere prestazioni peggiori di uno pieno. [Tabella 2, Han et al.]
|
||||
|
||||
## Esempio
|
||||
Applicazioni studiate in letteratura secondo la review (non casi verificati in questa nota, solo citati): pale simil-lama, utensili di lavorazione, supporti ottici sensibili alle vibrazioni, concetti di design leggero basati su ottimizzazione topologica. [§1]
|
||||
|
||||
## Fonti e collegamenti
|
||||
[[SRC - Yu et al. 2026 - Additively Manufactured Particle Damping Structures Review]] · [[RIA - Yu et al. 2026 - Additively Manufactured Particle Damping Structures Review]] · [[Geometrie complesse - strutture reticolari e canali interni]] · [[Powder Bed Fusion (SLS, SLM, DMLS, EBM)]] · [[Indice - Progettazione DfAM]]
|
||||
@@ -17,6 +17,7 @@ Indice da sviluppare: Parametri macchina; finestre di processo; disegno degli es
|
||||
|
||||
## Note disponibili
|
||||
- [[Slicing e preparazione del job]]
|
||||
- [[Strumenti software per progettazione e simulazione in AM]]
|
||||
|
||||
## Domande da sviluppare
|
||||
- Quali concetti e definizioni servono per questo ambito?
|
||||
|
||||
+50
@@ -0,0 +1,50 @@
|
||||
---
|
||||
id: "am-strumenti-software-progettazione-simulazione"
|
||||
title: "Strumenti software per progettazione e simulazione in AM"
|
||||
type: "concetto"
|
||||
status: "da_verificare"
|
||||
created: "2026-09-10"
|
||||
updated: "2026-09-10"
|
||||
language: "it"
|
||||
tags: ["am/concetto"]
|
||||
aliases: ["CAD per AM", "FEA additive manufacturing", "Software DfAM", "Topology optimization software"]
|
||||
sources: ["[[SRC - ADDMAN 2024 - A Guide to Designing for Additive Manufacturing]]"]
|
||||
---
|
||||
|
||||
# Strumenti software per progettazione e simulazione in AM
|
||||
|
||||
## In breve
|
||||
Panoramica delle categorie di strumenti software che accompagnano il flusso di progettazione per AM: CAD, formati file di interscambio, simulazione/analisi agli elementi finiti (FEA), ottimizzazione topologica, e strumenti di simulazione/compensazione specifici per il processo additivo. [Fonte: guida di produttore; [[SRC - ADDMAN 2024 - A Guide to Designing for Additive Manufacturing]]]
|
||||
|
||||
## Spiegazione
|
||||
### CAD e formati file
|
||||
Due famiglie di rappresentazione geometrica hanno ruoli diversi nel flusso AM:
|
||||
- **Modelli NURBS ("file CAD")**: costituiti da punti connessi da curve; usati da software CAD (es. SolidWorks, Onshape, Pro-E/Creo); utenti tipici ingegneri/progettisti CAD; più facili da modificare; convertibili in altri formati CAD come STEP o Parasolid.
|
||||
- **Mesh poligonali ("file .stl")**: costituite da migliaia o milioni di piccoli triangoli; tipiche di software di modellazione 3D artistica (es. Blender, Maya); formato usato dalle stampanti/software di slicing e generato dalla scansione 3D; più difficili da modificare/riconvertire in altri formati.
|
||||
|
||||
La scansione 3D produce dati "point cloud", che devono essere convertiti in formato .stl (es. con software come GeoMagic) prima di poter essere stampati; anche i file CAD NURBS devono essere convertiti in .stl per la stampa. I modelli a superficie (poly mesh) devono essere convertiti per includere dati volumetrici: un modello a sola superficie non può essere sezionato (sliced) dal software di stampa.
|
||||
|
||||
Requisiti per un file pronto alla stampa: il modello deve essere "watertight" (senza vuoti), tutte le superfici e i corpi devono essere "collegati" (nessun modello disconnesso), e il file deve essere almeno in formato CAD o poligonale (i dati di sola point cloud non sono utilizzabili direttamente).
|
||||
|
||||
Produttori/software CAD citati nella guida (per categoria, non esaustivo): Autodesk (AutoCAD), PTC (Fusion 360, Inventor, Creo), Siemens (Revit, NX), Dassault Systèmes (SketchUp), ANSYS (SpaceClaim), Hexagon (Solid Edge, SOLIDWORKS, BricsCAD, CATIA), Bentley Systems (DraftSight, MicroStation, KeyCreator), ZWSOFT (ZWCAD).
|
||||
|
||||
### Simulazione e analisi delle prestazioni
|
||||
Il software di simulazione ingegneristica (inclusa l'analisi agli elementi finiti, FEA) è usato per ottimizzazione di volume/peso, analisi di trasferimento termico, calcoli di sforzo/deformazione e simulazione di flusso fluidodinamico, permettendo di valutare un pezzo senza costruire un prototipo fisico — utile quando il prototipo sarebbe costoso, pericoloso o difficile da testare nella realtà. La FEA simula e predice la risposta di materiali e strutture a fattori ambientali (forza, calore, vibrazione), per identificare potenziali cedimenti e ottimizzare il progetto prima della prototipazione fisica.
|
||||
|
||||
### Ottimizzazione topologica e strumenti di lightweighting
|
||||
Strumenti per affrontare sfide ingegneristiche come alleggerimento, gestione termica, personalizzazione di massa, materiali architettati (es. reticoli). Spesso parte di pacchetti software più ampi o disponibili come applicazioni dedicate, tipicamente basati su dati FEA o di altra simulazione. L'ottimizzazione topologica ha segnato, secondo la guida, uno spostamento significativo verso progetti che minimizzano l'uso di materiale, coerente con la capacità dell'AM di aggiungere materiale solo dove strutturalmente necessario (vedi anche [[Ottimizzazione topologica e design generativo (simulation-driven design)]]).
|
||||
|
||||
### Simulazione e compensazione di processo
|
||||
Prevedere il comportamento del materiale durante la deposizione strato per strato è complesso, per la variabilità intrinseca delle proprietà del materiale, dell'adesione tra strati e del comportamento termico. Gli strumenti di simulazione/compensazione di processo mirano a prevedere e compensare distorsioni o imperfezioni prima della stampa. Secondo la guida, questi strumenti sono più maturi e diffusi per i processi metallici (dove le variabili — proprietà del materiale, parametri laser, distribuzione granulometrica della polvere, velocità di raffreddamento — sono più numerose ed estreme) rispetto ai processi polimerici, dove il valore resta comunque utile per verificare come adattare il modello a processi diversi.
|
||||
|
||||
## Condizioni di applicazione
|
||||
Categorie di strumenti generiche, non legate a un processo AM specifico salvo dove indicato (es. maggiore maturità della simulazione di processo per il metallo rispetto al polimero). Elenchi di produttori software forniti dalla fonte come panoramica di mercato al 2024, non come raccomandazione né lista esaustiva.
|
||||
|
||||
## Dati o formule
|
||||
Nessun dato quantitativo verificabile in questa nota. **Claim commerciale non verificato** citato dalla fonte: la tecnologia proprietaria "ADDCAAM"/InterFill 3D di ADDMAN, applicata a file FDM sezionati per creare una struttura di riempimento interbloccata, è dichiarata dal produttore capace di produrre parti "70% più resistenti e con porosità 100 volte inferiore rispetto agli standard di settore" — affermazione di marketing del produttore della fonte stessa, non verificata in questa scheda: da non citare come dato tecnico generale.
|
||||
|
||||
## Esempio
|
||||
Non applicabile (nota di panoramica di categorie software, non caso applicativo documentato).
|
||||
|
||||
## Fonti e collegamenti
|
||||
[[SRC - ADDMAN 2024 - A Guide to Designing for Additive Manufacturing]] · [[RIA - ADDMAN 2024 - A Guide to Designing for Additive Manufacturing]] · [[Slicing e preparazione del job]] · [[Ottimizzazione topologica e design generativo (simulation-driven design)]] · [[Indice - Parametri e simulazione]]
|
||||
@@ -0,0 +1,249 @@
|
||||
---
|
||||
id: "am-course-am90"
|
||||
title: "Fonti e criteri di attendibilità"
|
||||
type: "fonte"
|
||||
status: "pronto"
|
||||
created: "2026-09-10"
|
||||
updated: "2026-09-10"
|
||||
language: "it"
|
||||
tags: ["am/dispense", "am/tecnologie"]
|
||||
aliases: []
|
||||
sources: []
|
||||
---
|
||||
|
||||
# Fonti e criteri di attendibilità
|
||||
|
||||
## Metodo di consultazione
|
||||
Accesso web: 2026-09-10. I riferimenti qui elencati sono quelli utilizzati nelle dispense. Le descrizioni indicano se è stato consultato testo della pagina, abstract o soltanto un estratto indicizzato. Non vengono presentati come letti integralmente video, norme a pagamento o PDF non analizzati.
|
||||
|
||||
Le fonti universitarie storiche sono usate per principi generali. Alcune pagine riportano denominazioni, esempi macchina e semplificazioni datate: non sono stati riprodotti intervalli numerici generici o equivalenze improprie. Le fonti industriali descrivono piattaforme specifiche; le loro affermazioni comparative restano attribuite.
|
||||
|
||||
Le sintesi non costituiscono una revisione sistematica della letteratura. Per applicazioni strutturali serviranno articoli completi, dati specifici e validazione pertinente.
|
||||
|
||||
## S01
|
||||
|
||||
[NIST — What is Additive Manufacturing?](https://www.nist.gov/additive-manufacturing/what-additive-manufacturing)
|
||||
|
||||
Pagina istituzionale; sezioni Summary e How Does Additive Work. Definizione e percorso digitale.
|
||||
|
||||
## S02
|
||||
|
||||
[Loughborough University — The 7 Categories of Additive Manufacturing](https://www.lboro.ac.uk/research/amrg/about/the7categoriesofadditivemanufacturing/)
|
||||
|
||||
Indice universitario delle sette famiglie. Riferimenti storici: usato per la tassonomia, non per prestazioni di macchine attuali.
|
||||
|
||||
## S03
|
||||
|
||||
[Loughborough University — Material Extrusion](https://www.lboro.ac.uk/research/amrg/about/the7categoriesofadditivemanufacturing/materialextrusion/)
|
||||
|
||||
Sezioni descrittive del processo. Esempi macchina e intervalli numerici datati non utilizzati.
|
||||
|
||||
## S04
|
||||
|
||||
[Prusa — Filament Material Guide](https://help.prusa3d.com/filament-material-guide)
|
||||
|
||||
Tabella del produttore: materiali, hardware, gestione umidità. Indicazioni dipendenti dal sistema, non ricette universali.
|
||||
|
||||
## S05
|
||||
|
||||
[Seppala et al. — Weld formation during material extrusion additive manufacturing](https://www.nist.gov/publications/weld-formation-during-material-extrusion-additive-manufacturing)
|
||||
|
||||
Abstract e scheda NIST di articolo Soft Matter, 2017; DOI 10.1039/C7SM00950J. Interdiffusione e storia termica del legame interstrato; testo integrale non analizzato.
|
||||
|
||||
## S06
|
||||
|
||||
[Markforged — Guide to Metal FFF 3D Printing](https://static.markforged.com/downloads/MF_White_paper_Metal_FFF_3D_Printing_Guide.pdf)
|
||||
|
||||
Guida del produttore, PDF 10 pagine. Sezioni debinding, sintering e post-processing, soprattutto pagine del file 7–9. Non trasferire dati a sistemi diversi.
|
||||
|
||||
## S07
|
||||
|
||||
[Markforged — Carbon Fiber 3D Printing: An Introductory Guide](https://static.markforged.com/downloads/MF_White_paper_carbon_fiber.pdf)
|
||||
|
||||
Estratto indicizzato, sezione Continuous Fibers, pagina stampata 7. Usato solo per distinguere fibre corte e rinforzo continuo; PDF completo non analizzato.
|
||||
|
||||
## S08
|
||||
|
||||
[Loughborough University — Vat Photopolymerisation](https://www.lboro.ac.uk/research/amrg/about/the7categoriesofadditivemanufacturing/vatphotopolymerisation/)
|
||||
|
||||
Principio, supporti, rimozione resina e post-cura. Le indicazioni di lavaggio non sono adottate come procedura operativa universale.
|
||||
|
||||
## S09
|
||||
|
||||
[Formlabs — SLA vs DLP vs MSLA vs LCD](https://formlabs.com/blog/sla-dlp-msla-lcd-resin-3d-printer-comparison/)
|
||||
|
||||
Guida del produttore: architetture di esposizione e distinzione fra risoluzione e accuratezza. Esclusi claim di superiorità generale.
|
||||
|
||||
## S10
|
||||
|
||||
[NIST — Vat Photopolymerization](https://www.nist.gov/additive-manufacturing/research-areas/technologies/vat-photopolymerization)
|
||||
|
||||
Introduzione istituzionale alla fotopolimerizzazione.
|
||||
|
||||
## S11
|
||||
|
||||
[Lithoz — A Leader in the Additive Manufacturing Space](https://www.lithoz.com/en/lithoz-a-leader-in-the-additive-manufacturing-space/)
|
||||
|
||||
Estratto indicizzato del produttore: LCM e sequenza stampa, debinding, sinterizzazione. Nessuna prestazione numerica ricavata.
|
||||
|
||||
## S12
|
||||
|
||||
[NIST — Powder Bed Fusion](https://www.nist.gov/additive-manufacturing/research-areas/technologies/powder-bed-fusion)
|
||||
|
||||
Principio, strumenti AMMT e AMRC; descrizione della stesura e fusione di polveri metalliche.
|
||||
|
||||
## S13
|
||||
|
||||
[EOS — DMLS Metal 3D Printing](https://www.eos.info/about-us/what-we-do/dmls)
|
||||
|
||||
Sezione What is Metal Additive Manufacturing: DMLS come tecnologia LPBF. Nomenclatura del produttore.
|
||||
|
||||
## S14
|
||||
|
||||
[EOS — Metal Powder for 3D Printing](https://www.eos.info/metal-solutions/metal-materials)
|
||||
|
||||
Portafoglio e Quality Triangle: polvere, parametri, sistema; maturità diversa dei processi. Non è una lista di compatibilità universale.
|
||||
|
||||
## S15
|
||||
|
||||
[NIST — Measuring dynamic light absorption during laser welding and laser powder bed fusion](https://www.nist.gov/programs-projects/measuring-dynamic-light-absorption-during-laser-welding-and-laser-powder-bed)
|
||||
|
||||
Descrizione del progetto: assorbimento variabile, cavità keyhole e intrappolamento di pori.
|
||||
|
||||
## S16
|
||||
|
||||
[NIST — Additive Manufacturing Fatigue and Fracture](https://www.nist.gov/programs-projects/additive-manufacturing-fatigue-and-fracture)
|
||||
|
||||
Descrizione e immagini di frattura: difetti lack-of-fusion e pori. Usato per meccanismi, non per affermazioni assolute sul mercato.
|
||||
|
||||
## S17
|
||||
|
||||
[Colibrium Additive — Q10plus EB-PBF](https://www.colibriumadditive.com/printers/eb-pbf-printers/q10-plus)
|
||||
|
||||
Pagina macchina: vuoto ad alta temperatura e riduzione delle tensioni residue. Esempio specifico, non garanzia per ogni EB-PBF.
|
||||
|
||||
## S18
|
||||
|
||||
[Formlabs — Selective Laser Sintering: Complete Guide](https://formlabs.com/blog/what-is-selective-laser-sintering/)
|
||||
|
||||
Sezioni How SLS Works, Materials e Workflow. Esclusi prezzi e confronti promozionali generalizzati.
|
||||
|
||||
## S19
|
||||
|
||||
[HP — Comparing Binder Jetting, Material Jetting, MJF and SLS](https://www.hp.com/us-en/printers/3d-printers/learning-center/3d-print-binder-vs-material-jetting.html)
|
||||
|
||||
Sezioni MJF vs Binder Jetting e MJF vs SLS and FDM. Agenti e fusione termica; non assunto che isotropia sia perfetta.
|
||||
|
||||
## S20
|
||||
|
||||
[Stratasys — SAF Technology](https://www.stratasys.com/uk/guide-to-3d-printing/technologies-and-materials/saf-technology/)
|
||||
|
||||
Sezione How does SAF work: fluido assorbente e lampada infrarossa. Non utilizzati claim di primato economico o ambientale.
|
||||
|
||||
## S21
|
||||
|
||||
[Loughborough University — Binder Jetting](https://www.lboro.ac.uk/research/amrg/about/the7categoriesofadditivemanufacturing/binderjetting/)
|
||||
|
||||
Principio polvere-legante e caratteristiche generali; informazioni storiche da integrare con il produttore.
|
||||
|
||||
## S22
|
||||
|
||||
[Desktop Metal — Introduction to the Binder Jetting Process](https://www.desktopmetal.com/resources/intro-binder-jet-3dprinting-process)
|
||||
|
||||
Testo della pagina Binder Jetting 101–103. Video non trascritti né analizzati.
|
||||
|
||||
## S23
|
||||
|
||||
[Desktop Metal — Process Simulation and Sintering](https://www.desktopmetal.com/press/press-release-desktop-metal-launches-new-process-simulation-software-for-metal-additive-manufacturing-1)
|
||||
|
||||
Comunicato 6 novembre 2020, sezione Challenges of Sintering: ritiro, distorsione, compensazione. Le promesse del software non sono validate qui.
|
||||
|
||||
## S24
|
||||
|
||||
[Loughborough University — Material Jetting](https://www.lboro.ac.uk/research/amrg/about/the7categoriesofadditivemanufacturing/materialjetting/)
|
||||
|
||||
Descrizione di gocce, DOD, viscosità e supporti. La lista generica dei polimeri non è adottata come composizione delle resine PolyJet.
|
||||
|
||||
## S25
|
||||
|
||||
[Stratasys — PolyJet Materials](https://www.stratasys.com/en/materials/materials-catalog/polyjet-materials/)
|
||||
|
||||
Catalogo produttore: fotopolimeri rigidi, trasparenti e rubber-like. Proprietà e disponibilità dipendono dalla resina e dalla macchina.
|
||||
|
||||
## S26
|
||||
|
||||
[NIST — Material Jetting](https://www.nist.gov/additive-manufacturing/research-areas/technologies/material-jetting)
|
||||
|
||||
Introduzione a deposizione continua e drop-on-demand.
|
||||
|
||||
## S27
|
||||
|
||||
[NIST — Directed Energy Deposition](https://www.nist.gov/additive-manufacturing/research-areas/technologies/directed-energy-deposition)
|
||||
|
||||
Introduzione e Schlieren Imaging: alimentazione polvere, gas, interazione con bagno e spruzzi.
|
||||
|
||||
## S28
|
||||
|
||||
[TWI — Wire Arc Additive Manufacturing](https://www.twi-global.com/technical-knowledge/job-knowledge/arc-based-additive-manufacturing-137)
|
||||
|
||||
Introduzione: DED-arc, preforme near-net-shape e deposito da filo. Esclusi intervalli di produttività come garanzia.
|
||||
|
||||
## S29
|
||||
|
||||
[Loughborough University — Directed Energy Deposition](https://www.lboro.ac.uk/research/amrg/about/the7categoriesofadditivemanufacturing/directedenergydeposition/)
|
||||
|
||||
Principio e uso per riparazione o aggiunta a componenti esistenti.
|
||||
|
||||
## S30
|
||||
|
||||
[Loughborough University — Sheet Lamination](https://www.lboro.ac.uk/research/amrg/about/the7categoriesofadditivemanufacturing/sheetlamination/)
|
||||
|
||||
Sezioni processo e materiali: LOM, UAM e integrazione con CNC.
|
||||
|
||||
## S31
|
||||
|
||||
[NASA TechPort — UAM with Embedded Capabilities](https://techport.nasa.gov/projects/90165)
|
||||
|
||||
Scheda di progetto, estratto indicizzato: materiali strutturali multifunzionali e capacità integrate. Non dimostra produzione seriale generalizzata.
|
||||
|
||||
## S32
|
||||
|
||||
[NIST — Costs and Cost Effectiveness of Additive Manufacturing](https://www.nist.gov/publications/costs-and-cost-effectiveness-additive-manufacturing)
|
||||
|
||||
Thomas e Gilbert, 2014, NIST SP 1176, DOI 10.6028/NIST.SP.1176. Consultati abstract e scheda; usati concetti, non prezzi storici.
|
||||
|
||||
## S33
|
||||
|
||||
[TWI — Cold Spraying](https://www.twi-global.com/what-we-do/research-and-technology/technologies/coating-and-surface-engineering/cold-spraying)
|
||||
|
||||
Sezioni principio, benefici e materiali: impatto allo stato solido; riparazione, rivestimento e costruzione near-net-shape.
|
||||
|
||||
## S34
|
||||
|
||||
[Nanoscribe — Microfabrication Technologies](https://www.nanoscribe.com/en/microfabrication-technologies/)
|
||||
|
||||
Estratto indicizzato del produttore: 2PP con impulsi femtosecondi. Claim comparativi sulla risoluzione non utilizzati.
|
||||
|
||||
## S35
|
||||
|
||||
[Toombs et al. — Volumetric AM of Silica Glass with micro-CAL](https://arxiv.org/abs/2110.01651)
|
||||
|
||||
Abstract del preprint 2021: illuminazione tomografica di nanocomposito e sinterizzazione. Risultati sperimentali, non catalogo di processo.
|
||||
|
||||
## S36
|
||||
|
||||
[NIST — Ceramic Additive Manufacturing](https://www.nist.gov/mml/mmsd/primary-focus-areas/ceramic-additive-manufacturing)
|
||||
|
||||
Estratto istituzionale: sospensioni ceramiche, reologia, DIW e caratterizzazione durante il processo.
|
||||
|
||||
## S37
|
||||
|
||||
[ISO — ISO/ASTM 52900:2021](https://www.iso.org/standard/74514.html)
|
||||
|
||||
Scheda pubblica della norma, titolo e ambito. Testo normativo integrale non consultato; nessuna dichiarazione di conformità.
|
||||
|
||||
## S38
|
||||
|
||||
[HP — 3D Printing Post-processing](https://www.hp.com/us-en/printers/3d-printers/learning-center/3d-printing-post-processing.html)
|
||||
|
||||
Estratto produttore: pulizia della polvere residua e finiture di componenti MJF.
|
||||
@@ -17,6 +17,11 @@ sources: []
|
||||
- [[SRC - freeCodeCamp GaugeHow - 3D Printing and Additive Manufacturing Full Course]]
|
||||
- [[SRC - Zhou et al. 2024 - Additive Manufacturing A Comprehensive Review]]
|
||||
- [[SRC - ADDITIVA - Schede tecniche leghe metalliche per AM]]
|
||||
- [[SRC - Yu et al. 2026 - Additively Manufactured Particle Damping Structures Review]]
|
||||
- [[SRC - IQS Directory - Additive Manufacturing Guide]] (fonte di parte, non usata per note di concetto)
|
||||
- [[AM90 - Fonti]] — bibliografia annotata con 38 fonti (S01–S38: NIST, Loughborough University, norme ISO/ASTM, produttori), usata come riferimento condiviso dalle note [[AM01 - Fondamenti e panoramica]]–[[AM10 - Processi specialistici]], [[Confronto tecnologie e materiali]] e [[Glossario]]. Non segue il formato scheda singola per fonte: mantiene la struttura ad ancore (`#S01` ecc.) già usata dai wikilink di quelle note.
|
||||
- [[SRC - ADDMAN 2024 - A Guide to Designing for Additive Manufacturing]]
|
||||
- [[SRC - iamrapid.com - Design for Additive Manufacturing Rules and Guide]] (fonte di parte, non usata per note di concetto)
|
||||
|
||||
Aggiungi ogni nuova scheda fonte qui. Usa [[Modello - Fonte]].
|
||||
|
||||
|
||||
@@ -0,0 +1,43 @@
|
||||
---
|
||||
id: "am-src-addman-2024-dfam-guide"
|
||||
title: "ADDMAN (2024) — A Guide to Designing for Additive Manufacturing"
|
||||
type: "fonte"
|
||||
status: "da_verificare"
|
||||
created: "2026-09-10"
|
||||
updated: "2026-09-10"
|
||||
language: "it"
|
||||
tags: ["am/fonte"]
|
||||
aliases: ["ADDMAN DfAM Guide", "ADDMAN eBook DfAM"]
|
||||
sources: []
|
||||
accessed: "2026-09-10"
|
||||
edition: "2024, eBook"
|
||||
---
|
||||
|
||||
# ADDMAN (2024) — A Guide to Designing for Additive Manufacturing
|
||||
|
||||
## Riferimento bibliografico
|
||||
- Titolo: "A Guide to Designing for Additive Manufacturing".
|
||||
- Ente: ADDMAN Group (ADDMAN®), produttore/service bureau statunitense di manifattura additiva metallica e polimerica (gruppo verticalmente integrato: prototipazione, stampa, post-processing); co-branding "DINSMORE®" nella pagina finale, non identificato con certezza in questa scheda.
|
||||
- Formato: eBook/guida tecnica di produttore, ~49 pagine secondo il proprio indice.
|
||||
- Estrazione: testo acquisito tramite MinerU (strumento di conversione PDF→Markdown/JSON) dal file originale "ADDMAN_DfAM-Guide2024"; non è chiaro se il PDF originale sia stato scaricato dal sito ADDMAN o da terzi — **URL pubblica non acquisita in questo clip, da recuperare per una citazione stabile**.
|
||||
- Data di accesso: 2026-09-10.
|
||||
- Allegati: estratto Markdown completo in [[90 Allegati/MinerU_markdown_ADDMAN_DfAM-Guide2024|MinerU_markdown_ADDMAN_DfAM-Guide2024]]; dati strutturati grezzi dell'estrazione (bounding box, layout) in [[90 Allegati/MinerU_ADDMAN_DfAM-Guide2024|MinerU_ADDMAN_DfAM-Guide2024 (JSON)]], non analizzati in dettaglio in questa scheda. Non modificare gli originali.
|
||||
|
||||
## Ambito e qualità della fonte
|
||||
Guida tecnica di un produttore/service bureau di AM, non peer-reviewed, senza citazioni bibliografiche interne (le immagini citano fonti terze per attribuzione, non per supportare affermazioni tecniche). Qualità paragonabile ad altri white paper di produttore già usati nel vault (es. Markforged, EOS, HP citati in [[AM90 - Fonti]]): utile per regole di progettazione pratiche e ordini di grandezza dimensionali, ma le affermazioni comparative o le prestazioni di prodotti proprietari (es. la tecnologia "ADDCAAM"/InterFill 3D) vanno trattate come claim commerciali non verificati, non come dati di riferimento generali.
|
||||
|
||||
## Sezioni lette e localizzatori
|
||||
Testo integrale (indice a pagina 1 del documento). Struttura:
|
||||
- Introduzione: cos'è l'AM, anisotropia, stabilità dimensionale/ritiro/warping, risoluzione e rugosità.
|
||||
- Capitolo 1 — DfAM e considerazioni tecniche: regola dei 45°/overhang orizzontali (§1.2–1.3), spessore minimo e aspect ratio delle pareti verticali (§1.4), progettazione di fori/gap (§1.5).
|
||||
- Capitolo 2 — Approfondimento tecnologico: material extrusion, vat polymerization, material jetting, binder jetting, powder bed fusion — per ciascuna: volumi di stampa industriali, produttori di macchine, materiali comuni, fasce di costo, linee guida di progettazione e modalità di difetto comuni.
|
||||
- Capitolo 3 — "DfAM 201": progettazione per il processo/finitura corretti, per funzionalità migliorata, per riduzione di materiale, per consolidamento di parti; benefici di velocità, costo e prestazioni.
|
||||
- Capitolo 4 — Software e strumenti: CAD, formati file (NURBS vs mesh poligonale/STL), simulazione/FEA, ottimizzazione topologica, strumenti di simulazione/compensazione di processo; tecnologia proprietaria ADDCAAM/InterFill 3D.
|
||||
|
||||
Localizzatore usato nelle note derivate: titolo di sezione/capitolo.
|
||||
|
||||
## Risultati utili e limiti
|
||||
Fonte utile per regole dimensionali pratiche con valori numerici specifici (es. spessore minimo parete 0,5 mm, soglia di consultazione ingegneristica 2 mm, overhang >3 mm a rischio deformazione in metallo, feature PBF >0,7 mm, ritiro da sinterizzazione in binder jetting 15–16%) e per una panoramica per-processo di produttori di macchine, materiali comuni e fasce di costo indicativo. Limiti: nessuna fonte primaria citata per i valori numerici (sono presentati come regole pratiche del produttore, non come dati di prova); il capitolo 4 include una promozione esplicita del prodotto proprietario "ADDCAAM" (claim "70% più resistente, 100 volte meno porosità rispetto agli standard di settore") non verificabile con questa fonte — **da trattare come claim commerciale, non come dato tecnico**.
|
||||
|
||||
## Elaborazioni collegate
|
||||
[[RIA - ADDMAN 2024 - A Guide to Designing for Additive Manufacturing]]
|
||||
@@ -0,0 +1,35 @@
|
||||
---
|
||||
id: "am-src-iqs-directory-am-guide"
|
||||
title: "IQS Directory — Additive Manufacturing: 3D Printing Guide & Benefits"
|
||||
type: "fonte"
|
||||
status: "da_verificare"
|
||||
created: "2026-09-10"
|
||||
updated: "2026-09-10"
|
||||
language: "it"
|
||||
tags: ["am/fonte"]
|
||||
aliases: []
|
||||
sources: []
|
||||
url: "https://www.iqsdirectory.com/articles/additive-manufacturing.html"
|
||||
accessed: "2026-09-10"
|
||||
---
|
||||
|
||||
# IQS Directory — Additive Manufacturing: 3D Printing Guide & Benefits
|
||||
|
||||
## Riferimento bibliografico
|
||||
- Ente: IQS Directory (directory B2B di fornitori industriali, contenuto redatto dal team editoriale interno, non firma individuale).
|
||||
- Titolo pagina: "Additive Manufacturing: 3D Printing Guide & Benefits".
|
||||
- URL: https://www.iqsdirectory.com/articles/additive-manufacturing.html
|
||||
- Data di accesso: 2026-09-10, tramite Obsidian Web Clipper (esportazione "highlights", un solo estratto corrispondente all'intera pagina).
|
||||
- Allegato: estratto HTML/testo conservato in [[90 Allegati/obsidian-web-clipper-highlights-202609101040|obsidian-web-clipper-highlights-202609101040]] (formato JSON dell'esportazione Web Clipper); non modificare l'originale.
|
||||
|
||||
## Ambito e qualità della fonte
|
||||
Contenuto editoriale di una directory commerciale di fornitori, non un ente tecnico/normativo né una pubblicazione accademica. Il vault segue già la regola di escludere claim promozionali dalle affermazioni generali (vedi [[AM90 - Fonti]] per il precedente adottato in altre note del vault). Questa fonte è di qualità nettamente inferiore rispetto a NIST, Loughborough University, norme ISO/ASTM o riviste peer-reviewed già presenti nel vault.
|
||||
|
||||
## Sezioni lette e localizzatori
|
||||
Introduzione e Capitolo 1 "What is Additive Manufacturing?" (definizione generica di AM/ALM, cenni a prototipazione rapida e produzione di piccoli lotti). Il resto della pagina (processo, prodotti, vantaggi, attrezzature) non è stato analizzato in dettaglio in questa scheda.
|
||||
|
||||
## Risultati utili e limiti
|
||||
Nessun contenuto tecnico non già coperto, con qualità di fonte superiore, da [[SRC - Zhou et al. 2024 - Additive Manufacturing A Comprehensive Review]], [[SRC - freeCodeCamp GaugeHow - 3D Printing and Additive Manufacturing Full Course]] o dalle fonti NIST/Loughborough citate in [[AM90 - Fonti]] (bibliografia presente in Inbox, non ancora integrata nel vault). **Non usata per derivare note di concetto**: contenuto ridondante rispetto a fonti già disponibili di qualità superiore. Conservata solo per tracciabilità dell'acquisizione.
|
||||
|
||||
## Elaborazioni collegate
|
||||
Nessuna nota derivata da questa fonte.
|
||||
+51
@@ -0,0 +1,51 @@
|
||||
---
|
||||
id: "am-src-yu-2026-particle-damping-review"
|
||||
title: "Yu et al. (2026) — Additively Manufactured Particle Damping Structures: A Review"
|
||||
type: "fonte"
|
||||
status: "da_verificare"
|
||||
created: "2026-09-10"
|
||||
updated: "2026-09-10"
|
||||
language: "it"
|
||||
tags: ["am/fonte"]
|
||||
aliases: ["Yu 2026", "AMPD review", "Particle damping review"]
|
||||
sources: []
|
||||
doi: "10.1016/j.addlet.2026.100417"
|
||||
url: "https://doi.org/10.1016/j.addlet.2026.100417"
|
||||
accessed: "2026-09-10"
|
||||
edition: "Additive Manufacturing Letters, 2026, articolo 100417 (short review)"
|
||||
---
|
||||
|
||||
# Yu et al. (2026) — Additively Manufactured Particle Damping Structures: A Review
|
||||
|
||||
## Riferimento bibliografico
|
||||
- Titolo: "Additively manufactured particle damping structures: A review of manufacturing and filling approaches, design variables and evidence comparability".
|
||||
- Autori: Weijia Yu, Marcus Oel, Jens Niedermeyer, Lennart Mesecke, Ina Meyer, Roland Lachmayer.
|
||||
- Tipo di articolo: short review, pubblicato su *Additive Manufacturing Letters* (Elsevier), 2026, articolo 100417.
|
||||
- DOI: https://doi.org/10.1016/j.addlet.2026.100417
|
||||
- Materiale supplementare (non consultato in questa scheda): tabella di evidenza AMPD (108 record, formato Excel), protocollo di ricerca/mappatura, script MATLAB per le figure; depositati anche su Zenodo (DOI concept 10.5281/zenodo.20112102), file di deposito soggetti a embargo fino al 31/12/2026 secondo l'articolo.
|
||||
- Dichiarazione IA: gli autori dichiarano l'uso di OpenAI Codex e ChatGPT solo per editing linguistico/revisione editoriale, non per generare contenuto scientifico o classificazioni.
|
||||
- Data di accesso: 2026-09-10, tramite Obsidian Web Clipper dalla pagina ScienceDirect. Allegato: estratto testuale conservato in [[90 Allegati/Additively manufactured particle damping structures_ A review of manufacturing and filling approaches, design variables and evidence comparability|Additively manufactured particle damping structures — estratto testuale]]; non modificare l'originale. Non è il PDF impaginato, solo testo estratto dalla pagina.
|
||||
|
||||
## Ambito e qualità della fonte
|
||||
Review sistematica peer-reviewed, con metodologia esplicita (ricerca strutturata su Scopus, Web of Science, Google Scholar, citation tracking; tabella di evidenza con 108 record bibliografici, classificati in 79 "unità di evidenza" indipendenti secondo regole documentate). Qualità elevata: la review è essa stessa centrata sul tema della comparabilità e qualità dell'evidenza (esattamente il tipo di rigore richiesto dal metodo di questo vault), quindi è una fonte primaria affidabile per la classificazione del tema, anche se sintetizza a sua volta letteratura terza (le singole affermazioni sui risultati numerici dei 108 record non sono state verificate singolarmente in questa scheda).
|
||||
|
||||
## Sezioni lette e localizzatori
|
||||
Testo integrale (sezioni 1–8 più materiale editoriale). Struttura:
|
||||
1. Introduzione (§1).
|
||||
2. Base di evidenza e framework di classificazione (§2).
|
||||
3. Confini tra approcci di manifattura e riempimento (§3).
|
||||
4. Variabili di progetto per la polvere trattenuta diretta (§4).
|
||||
5. Evidenza di validazione e comparabilità delle metriche (§5).
|
||||
6. Completezza di reporting e necessità di comparabilità (§6).
|
||||
7. Implicazioni progettuali (§7).
|
||||
8. Conclusioni (§8).
|
||||
|
||||
Localizzatore usato nelle note derivate: `[§X]`.
|
||||
|
||||
## Risultati utili e limiti
|
||||
Fonte di alta qualità per: classificazione degli approcci di "particle damping" additivamente fabbricato (AMPD), variabili di progetto (posizionamento e forma della cavità), metodi di validazione/test e — punto di forza specifico — un'analisi sistematica delle lacune di reporting nella letteratura AMPD, con una checklist minima di reporting proposta dagli autori (Tabella 4 dell'articolo).
|
||||
|
||||
Limiti: è una review, quindi i dati quantitativi sui singoli studi (es. Tabella 2, casi Westbeld et al., Scott-Emuakpor et al., Han et al.) sono citati "come riportato da Yu et al. (2026)" e non sono stati verificati alla fonte primaria originale in questa scheda. Argomento di nicchia (smorzamento vibrazionale tramite polvere/particelle trattenute in cavità stampate), non copre l'AM in generale.
|
||||
|
||||
## Elaborazioni collegate
|
||||
[[RIA - Yu et al. 2026 - Additively Manufactured Particle Damping Structures Review]]
|
||||
@@ -0,0 +1,34 @@
|
||||
---
|
||||
id: "am-src-iamrapid-dfam-guide"
|
||||
title: "iamrapid.com — Design for Additive Manufacturing (DfAM): Rules & Guide"
|
||||
type: "fonte"
|
||||
status: "da_verificare"
|
||||
created: "2026-09-10"
|
||||
updated: "2026-09-10"
|
||||
language: "it"
|
||||
tags: ["am/fonte"]
|
||||
aliases: []
|
||||
sources: []
|
||||
url: "https://iamrapid.com/"
|
||||
accessed: "2026-09-10"
|
||||
---
|
||||
|
||||
# iamrapid.com — Design for Additive Manufacturing (DfAM): Rules & Guide
|
||||
|
||||
## Riferimento bibliografico
|
||||
- Ente: iamrapid.com, fornitore di servizi di stampa 3D con sede a Bangalore, India.
|
||||
- Titolo pagina: "Design for Additive Manufacturing (DfAM): Rules & Guide" (parte di una serie di guide del sito).
|
||||
- Data di accesso: 2026-09-10, tramite Obsidian Web Clipper.
|
||||
- Allegato: testo estratto conservato in [[90 Allegati/Design for Additive Manufacturing (DfAM)_ Rules & Guide|Design for Additive Manufacturing (DfAM)_ Rules & Guide]]; non modificare l'originale.
|
||||
|
||||
## Ambito e qualità della fonte
|
||||
Contenuto editoriale di un service bureau commerciale, non un ente tecnico/normativo né una pubblicazione peer-reviewed. Qualità paragonabile a [[SRC - IQS Directory - Additive Manufacturing Guide]]: divulgativo, orientato a promuovere i servizi del sito.
|
||||
|
||||
## Sezioni lette e localizzatori
|
||||
Introduzione e sezione "What is Additive Manufacturing?" con elenco di ragioni per cui la progettazione conta in AM (geometrie complesse, efficienza materiale, personalizzazione, riduzione time-to-market, costo, prestazioni, superamento vincoli tradizionali, consolidamento, manifattura distribuita, miglioramento continuo) e una rassegna introduttiva delle tecnologie AM comuni (FDM, SLA, ecc.). Resto della pagina non analizzato in dettaglio in questa scheda.
|
||||
|
||||
## Risultati utili e limiti
|
||||
Contenuto in gran parte ridondante rispetto a fonti di qualità superiore già nel vault, in particolare [[SRC - ADDMAN 2024 - A Guide to Designing for Additive Manufacturing]] (guida di produttore molto più dettagliata e con regole dimensionali concrete) e [[SRC - Zhou et al. 2024 - Additive Manufacturing A Comprehensive Review]] (fonte peer-reviewed). **Non usata per derivare note di concetto**: conservata solo per tracciabilità dell'acquisizione.
|
||||
|
||||
## Elaborazioni collegate
|
||||
Nessuna nota derivata da questa fonte.
|
||||
@@ -15,6 +15,8 @@ sources: []
|
||||
|
||||
- [[RIA - freeCodeCamp GaugeHow - 3D Printing and Additive Manufacturing Full Course]]
|
||||
- [[RIA - Zhou et al. 2024 - Additive Manufacturing A Comprehensive Review]]
|
||||
- [[RIA - Yu et al. 2026 - Additively Manufactured Particle Damping Structures Review]]
|
||||
- [[RIA - ADDMAN 2024 - A Guide to Designing for Additive Manufacturing]]
|
||||
|
||||
Usa [[Modello - Riassunto]] e collega la scheda fonte per ogni nuovo riassunto.
|
||||
|
||||
|
||||
@@ -0,0 +1,49 @@
|
||||
---
|
||||
id: "am-ria-addman-2024-dfam-guide"
|
||||
title: "Riassunto — ADDMAN (2024), A Guide to Designing for Additive Manufacturing"
|
||||
type: "riassunto"
|
||||
status: "da_verificare"
|
||||
created: "2026-09-10"
|
||||
updated: "2026-09-10"
|
||||
language: "it"
|
||||
tags: ["am/riassunto"]
|
||||
aliases: []
|
||||
sources: ["[[SRC - ADDMAN 2024 - A Guide to Designing for Additive Manufacturing]]"]
|
||||
---
|
||||
|
||||
# Riassunto — ADDMAN (2024), A Guide to Designing for Additive Manufacturing
|
||||
|
||||
## Fonte e copertura
|
||||
[[SRC - ADDMAN 2024 - A Guide to Designing for Additive Manufacturing]]. eBook di produttore, testo integrale letto (introduzione, capitoli 1–4).
|
||||
|
||||
## Sintesi
|
||||
Guida pratica di progettazione per AM pubblicata da ADDMAN Group, organizzata in: introduzione (anisotropia, stabilità dimensionale/ritiro/warping, risoluzione e rugosità), regole dimensionali generali (overhang e regola dei 45°, spessore minimo e aspect ratio delle pareti verticali, progettazione di fori e gap), un approfondimento per le 5 famiglie di processo principali (material extrusion, vat polymerization, material jetting, binder jetting, powder bed fusion) con volumi di stampa, produttori di macchine, materiali comuni, fasce di costo e modalità di difetto tipiche, una sezione "DfAM 201" su processo/finitura corretti, funzionalità migliorata, riduzione di materiale e consolidamento di parti con benefici di velocità/costo/prestazioni, e infine un capitolo su software e strumenti (CAD, formati file, simulazione/FEA, ottimizzazione topologica, strumenti di simulazione/compensazione di processo).
|
||||
|
||||
## Metodo e contesto
|
||||
Guida di produttore/service bureau, non uno studio sperimentale: le regole dimensionali sono presentate come pratiche consolidate del settore, senza citazione di fonte primaria o condizioni di prova (macchina, materiale, parametri). Da trattare come regole pratiche indicative, non come tolleranze di progetto garantite.
|
||||
|
||||
## Risultati principali
|
||||
- **Regola dei 45°**: overhang con angolo ≤45° dal piano di build generalmente non richiedono supporti; oltre questa soglia il supporto diventa necessario. In metallo, pareti centrali (core wall) più spesse permettono overhang leggermente maggiori, ma oltre 3 mm il rischio di deformazione aumenta anche con spessore ottimale. In material extrusion (FDM), overhang fino a 2–3 larghezze di cordone sono generalmente gestibili senza supporto.
|
||||
- **Pareti verticali**: spessore minimo consigliato 0,5 mm (sotto rischio di inconsistenze/fallimento di stampa); sotto i 2 mm consigliata consultazione con un ingegnere AM esperto.
|
||||
- **Fori e gap**: fori verticali tipicamente visibili tra 0,5–1 mm; fori orizzontali sotto 4–5 layer di diametro possono non essere visibili/funzionali, sopra 8 mm possono perdere la forma circolare; forme alternative (goccia, diamante, ovale) possono eliminare la necessità di supporti nei fori orizzontali.
|
||||
- **Panoramica per processo** (produttori di macchine, materiali comuni, fasce di costo indicativo e difetti tipici):
|
||||
- *Material extrusion*: orientamento critico per ridurre supporti e massimizzare resistenza (più forte nel piano XY, più debole in trazione lungo Z); sovradimensionare i fori e trapanarli dopo la stampa; spigoli tendono ad arrotondarsi; larghezza cordone ≈2× il diametro ugello.
|
||||
- *Vat polymerization* (SLA/DLP): sezioni trasversali grandi richiedono supporti più densi e tempi di attesa maggiori; rischio di "cupping" (aria intrappolata) in geometrie cave, da mitigare con fori di drenaggio.
|
||||
- *Material jetting* (PolyJet): parti generalmente più fragili (resina acrilica) con bassa tolleranza termica; impostazione "matte" aggiunge supporto sottile su tutta la superficie, "glossy" solo dove necessario; dettagli minimi consigliati ≥0,5 mm.
|
||||
- *Binder jetting*: ritiro da sinterizzazione del 15–16% (prevedibile e modellabile); ampia libertà geometrica (canali interni, reticoli, spigoli vivi); porosità residua nel pezzo sinterizzato finale, da considerare in applicazioni critiche (aerospaziale, medicale).
|
||||
- *Powder bed fusion*: parti lunghe e piatte (>15 cm) inclini al warping; feature consigliate >0,7 mm; rimozione polvere da considerare in fase di progetto (SLS richiede rimozione da tutte le superfici); supporti/ancoraggi necessari per mitigare warping; tensioni residue causa di deformazione/cricche da raffreddamento non uniforme; finitura superficiale as-built ruvida.
|
||||
- **Capitolo software**: CAD basato su NURBS (modifica facile, convertibile in STEP/PARASOLID) vs mesh poligonali/STL (usate per lo slicing, difficili da modificare); requisiti file per la stampa: modello "watertight", superfici/corpi connessi; strumenti di simulazione/FEA per stress, calore, fluidodinamica; strumenti di ottimizzazione topologica per lightweighting/reticoli; strumenti di simulazione e compensazione di processo per prevedere distorsioni (più maturi per metallo che per polimero).
|
||||
- **Claim commerciale non verificato**: ADDMAN promuove la propria tecnologia proprietaria "ADDCAAM"/InterFill 3D, dichiarando parti "70% più resistenti e con 100 volte meno porosità rispetto agli standard di settore" — **claim di produttore, non un dato verificato in questa scheda, da non citare come fatto generale**.
|
||||
|
||||
## Limiti e questioni aperte
|
||||
- Nessuna fonte primaria citata per le soglie dimensionali (0,5 mm, 2 mm, 3 mm, 0,7 mm, ritiro 15–16% ecc.): da trattare come regole pratiche di un singolo produttore, non come tolleranze di norma.
|
||||
- Nessuna specifica di macchina, materiale esatto o parametri di processo associata alle soglie: **non generalizzare** a un fornitore/macchina diverso da ADDMAN senza verifica.
|
||||
- Claim "ADDCAAM" (70% più resistente, 100x meno porosità) non verificabile con questa fonte: marketing di prodotto proprietario.
|
||||
|
||||
## Note da ricavare
|
||||
- Nota di concetto in `04 Progettazione`: regole dimensionali generali (overhang/45°, pareti, fori/gap) — capitolo 1.
|
||||
- Nota di concetto in `04 Progettazione`: regole di progettazione e difetti tipici per processo, con panoramica produttori/materiali/costi — capitolo 2.
|
||||
- Nota di concetto in `05 Parametri e simulazione`: strumenti software per progettazione e simulazione (CAD, FEA, ottimizzazione topologica, simulazione/compensazione di processo) — capitolo 4.
|
||||
- Le sezioni su funzionalità migliorata, riduzione di materiale, consolidamento parti e benefici di velocità/costo (capitolo 3, "DfAM 201") si sovrappongono a note già esistenti derivate dal corso video ([[Geometrie complesse - strutture reticolari e canali interni]], [[Tecniche di alleggerimento (lightweighting)]], [[Consolidamento di componenti (part consolidation)]]): da usare in futuro come fonte aggiuntiva di arricchimento/verifica per quelle note, non richiedono nuove note dedicate.
|
||||
|
||||
[[Indice riassunti]]
|
||||
+41
@@ -0,0 +1,41 @@
|
||||
---
|
||||
id: "am-ria-yu-2026-particle-damping-review"
|
||||
title: "Riassunto — Yu et al. (2026), Additively Manufactured Particle Damping Structures: A Review"
|
||||
type: "riassunto"
|
||||
status: "da_verificare"
|
||||
created: "2026-09-10"
|
||||
updated: "2026-09-10"
|
||||
language: "it"
|
||||
tags: ["am/riassunto"]
|
||||
aliases: []
|
||||
sources: ["[[SRC - Yu et al. 2026 - Additively Manufactured Particle Damping Structures Review]]"]
|
||||
---
|
||||
|
||||
# Riassunto — Yu et al. (2026), Additively Manufactured Particle Damping Structures: A Review
|
||||
|
||||
## Fonte e copertura
|
||||
[[SRC - Yu et al. 2026 - Additively Manufactured Particle Damping Structures Review]]. Short review peer-reviewed, testo integrale letto (sezioni 1–8).
|
||||
|
||||
## Sintesi
|
||||
Il particle damping è un metodo di smorzamento passivo delle vibrazioni: l'energia vibrazionale viene dissipata tramite il movimento relativo, gli urti e l'attrito di particelle libere all'interno di una cavità. La manifattura additiva permette di integrare questo meccanismo direttamente nel componente stampato, progettando insieme il percorso di carico strutturale e le cavità/volumi riempiti di particelle, invece di aggiungere un dispositivo di smorzamento separato — dando origine alle "additively manufactured particle damping structures" (AMPD). Il mezzo smorzante può essere polvere di stampa non fusa e trattenuta durante la powder bed fusion laser di metalli (PBF-LB/M), oppure particelle introdotte dopo la fabbricazione (post-filled). La review organizza sistematicamente la letteratura AMPD (108 record bibliografici, 79 "unità di evidenza" indipendenti) per confrontare approcci di manifattura/riempimento, variabili di progetto della cavità, metodi di validazione e completezza del reporting, evidenziando che risultati numerici di smorzamento provenienti da approcci fisicamente diversi non sono direttamente confrontabili.
|
||||
|
||||
## Metodo e contesto
|
||||
Metodologia di review sistematica: ricerca su Scopus (database primario), con controlli complementari su Web of Science e Google Scholar, più citation tracking avanti/indietro. Prima ricerca completata il 14 gennaio 2026, aggiornamento finale il 12 giugno 2026. Le pubblicazioni sono classificate in "unità di evidenza" (contributo indipendentemente contabile: gruppo di provini, dataset sperimentale o contributo di modello originale), con regole documentate per evitare doppi conteggi di dati riusati. Cinque livelli di validazione definiti: Concept, Numerical, Specimen, Component, Application (Tabella 1 dell'articolo).
|
||||
|
||||
## Risultati principali
|
||||
- **Classificazione degli approcci AMPD** [§3]: 79 unità di evidenza totali, di cui 29 "direct retained-powder" senza strutture interne progettate (cavità sigillata semplice), 35 "direct retained-powder" con strutture interne progettate (partizioni, nervature, reticoli, risonatori), e 15 "post-filled" (particelle introdotte e sigillate dopo la stampa). La maggior parte usa PBF-LB/M, che lascia polvere non fusa in cavità chiuse.
|
||||
- **Variabili di progetto per la polvere trattenuta diretta** [§4], su 64 unità di evidenza dirette: asse di posizionamento della cavità (mode-targeted 20, cavity variation 28, multiple cavities 6, component layout 6, neutral axis 4) e asse di design interno (simple cavity 29, divided cavities 19, internal features 7, local resonator 5, lattice cavity 4). Cavità ratio, volume frazionario, percentuale di polvere non fusa, rapporto di riempimento delle particelle e densità di impaccamento sono descritti come grandezze correlate ma distinte, da non trattare come intercambiabili.
|
||||
- **Evidenza di validazione e metriche** [§5]: sulle 64 unità dirette, metodi di test principali: 26 harmonic/swept-sine, 15 impact-hammer FRF, 9 numerico/modellazione, 7 misto/operativo, 5 impulso/decadimento libero, 2 shock/transitorio. Nessuna unità usa random/broadband come metodo primario — segnalato come lacuna di validazione (carico di servizio rappresentativo). Distribuzione per livello di validazione: 41 specimen, 9 numerical, 7 component, 7 application — evidenza concentrata a livello di provino, poco a livello di componente/applicazione.
|
||||
- **Completezza del reporting** [§6]: le lacune maggiori riguardano rapporto di riempimento delle particelle (Reported solo in 5/64 unità), densità di impaccamento/stato della polvere (38/64 Reported), ripetibilità/incertezza (33/64 Reported) e ciclo di vita/degrado (25/64 Reported, 34/64 Not reported — la lacuna maggiore). Gli autori propongono una checklist minima di reporting per lavori futuri (Tabella 4: identità dell'approccio, cavità e struttura, stato di polvere/particelle, condizioni di prova, baseline e metrica, ripetibilità e servizio).
|
||||
- **Implicazioni progettuali** [§7]: la scelta della via AMPD (diretta senza/con strutture interne, o post-filled) dovrebbe precedere l'ottimizzazione di dettaglio della cavità; posizionamento e design della cavità formano un unico problema di ottimizzazione; la validazione dovrebbe progredire da meccanismo/attivazione, a risposta di componente integrato, a prestazione funzionale e stabilità nel tempo.
|
||||
|
||||
## Limiti e questioni aperte
|
||||
- I dati quantitativi dei singoli studi citati (es. Tabella 2: Westbeld et al. — provini AlSi10Mg, incremento massimo del fattore di perdita relativo 1425% con polvere mobile; Scott-Emuakpor et al. — pale IN718, riduzione del fattore di qualità ~45–60% con aumento della resistenza a fatica; Han et al. — utensile TPMS post-filled, rapporto di smorzamento 0,03 ed efficienza di dissipazione energetica 48% a 145 g di riempimento) sono riportati "come citati da Yu et al. (2026)", non verificati alla fonte primaria originale in questa scheda.
|
||||
- Materiale supplementare (tabella di evidenza completa, protocollo, script) non consultato in questa scheda; utile per approfondimenti futuri.
|
||||
- Argomento di nicchia, specifico per PBF-LB/M metallico: non generalizzabile ad altri processi AM senza verifica.
|
||||
|
||||
## Note da ricavare
|
||||
- Nota di concetto in `04 Progettazione` su "particle damping" come tecnica DfAM abilitata dall'AM (cavità interne progettate), collegata a [[Geometrie complesse - strutture reticolari e canali interni]].
|
||||
- Possibile nota futura in `06 Difetti e qualità` sulla checklist di reporting/validazione proposta (Tabella 4), come esempio di buona pratica di documentazione delle prove — coerente con le regole di tracciabilità già richieste dal [[Metodo di lavoro]] del vault.
|
||||
|
||||
[[Indice riassunti]]
|
||||
@@ -1,22 +1,61 @@
|
||||
---
|
||||
id: "am-glossario"
|
||||
title: "Glossario"
|
||||
type: "indice"
|
||||
status: "pronto"
|
||||
type: "glossario"
|
||||
status: "da_verificare"
|
||||
created: "2026-09-10"
|
||||
updated: "2026-09-10"
|
||||
language: "it"
|
||||
tags: ["am/indice"]
|
||||
tags: ["am/glossario"]
|
||||
aliases: []
|
||||
sources: []
|
||||
sources: ["[[AM90 - Fonti#S37]]", "[[AM90 - Fonti#S05]]", "[[AM90 - Fonti#S09]]", "[[AM90 - Fonti#S15]]", "[[AM90 - Fonti#S23]]"]
|
||||
---
|
||||
|
||||
# Glossario
|
||||
|
||||
| Termine IT | Termine EN / acronimo | Nota |
|
||||
|---|---|---|
|
||||
| Manifattura additiva | Additive manufacturing / AM | [[AM - Introduzione]] |
|
||||
Le definizioni seguenti sono formulazioni didattiche sintetiche, non citazioni testuali normative. Il riferimento terminologico generale è [S37 — ISO — ISO/ASTM 52900:2021](https://www.iso.org/standard/74514.html); le spiegazioni applicative sono sviluppate nelle note collegate.
|
||||
|
||||
Aggiungi definizioni solo con una nota o fonte di supporto.
|
||||
| Termine IT/EN | Nota |
|
||||
|---|---|
|
||||
| Manifattura additiva / Additive manufacturing / AM | [[AM - Introduzione]] |
|
||||
| Feedstock | Materiale alimentato al processo: polvere, filo, filamento, resina, foglio ecc. |
|
||||
| Slicing | Suddivisione della geometria in sezioni per preparare la costruzione |
|
||||
| Layer / strato | Incremento con cui molti processi costruiscono il volume |
|
||||
| Build | Singola costruzione o ciclo che può contenere più componenti |
|
||||
| Build orientation | Orientamento del componente durante la fabbricazione |
|
||||
| Supporto | Struttura ausiliaria che contribuisce alla costruzione e spesso va rimossa |
|
||||
| Recoater | Dispositivo che distribuisce un nuovo strato di polvere |
|
||||
| Melt pool | Bagno localizzato di materiale fuso |
|
||||
| Hatch | Traiettoria o schema di scansione delle regioni interne di una sezione |
|
||||
| Infill | Riempimento interno progettato; non è una misura della densità del materiale |
|
||||
| Anisotropia | Dipendenza di una proprietà dalla direzione considerata |
|
||||
| Warping | Deformazione geometrica che altera la forma desiderata |
|
||||
| Lack of fusion | Discontinuità legata a insufficiente collegamento di regioni del materiale |
|
||||
| Keyhole | Cavità di vapore nel bagno, che può modificare assorbimento e porosità |
|
||||
| Green part / pezzo verde | Corpo formato da particelle tenute dal legante, prima del consolidamento finale |
|
||||
| Debinding | Rimozione del legante secondo il processo specifico |
|
||||
| Sinterizzazione | Consolidamento termico delle particelle, spesso con densificazione e ritiro |
|
||||
| Post-cura | Trattamento successivo per raggiungere lo stato previsto di un fotopolimero |
|
||||
| As-built | Stato dopo la costruzione; precisare quali operazioni siano già state eseguite |
|
||||
| Near-net-shape | Forma vicina a quella finale, che può richiedere lavorazioni successive |
|
||||
| Accuratezza | Vicinanza al valore o alla geometria di riferimento |
|
||||
| Ripetibilità | Coerenza fra risultati ottenuti ripetendo una procedura in condizioni definite |
|
||||
| Risoluzione | Capacità di distinguere o generare dettagli; non coincide automaticamente con accuratezza |
|
||||
| Tolleranza | Intervallo ammesso per una caratteristica del componente |
|
||||
| Qualificazione | Dimostrazione documentata che un processo soddisfa requisiti definiti |
|
||||
|
||||
[[Home]]
|
||||
Aggiungi nuove definizioni solo con una nota o fonte di supporto.
|
||||
|
||||
Per acronimi e famiglie di processo: [[AM01 - Fondamenti e panoramica]]. Per la differenza tra risoluzione e accuratezza: [[AM03 - Fotopolimerizzazione in vasca]]. Per difetti e proprietà nella PBF metallica: [[AM04 - PBF dei metalli]]. Per pezzo verde, debinding e ritiro: [[AM06 - Binder jetting]].
|
||||
|
||||
## Tre frasi da correggere
|
||||
"Stampo a strati sottili, quindi rispetto qualsiasi tolleranza": manca la verifica dimensionale.
|
||||
|
||||
"Il materiale è carbonio": manca la matrice e non è chiaro se le fibre siano corte o continue.
|
||||
|
||||
"Il pezzo è stampato, quindi è finito": mancano lo stato del materiale e le operazioni richieste.
|
||||
|
||||
## Fonti e navigazione
|
||||
Riferimenti di questa nota: [[AM90 - Fonti#S37|S37]], [[AM90 - Fonti#S05|S05]], [[AM90 - Fonti#S09|S09]], [[AM90 - Fonti#S15|S15]], [[AM90 - Fonti#S23|S23]].
|
||||
|
||||
[[AM01 - Fondamenti e panoramica]] · [[AM90 - Fonti|Bibliografia e limiti delle fonti]] · [[Home]]
|
||||
|
||||
+466
@@ -0,0 +1,466 @@
|
||||
## Published by: Elsevier
|
||||
|
||||
### Published by
|
||||
|
||||
[](https://www.sciencedirect.com/journal/additive-manufacturing-letters "Go to Additive Manufacturing Letters on ScienceDirect")
|
||||
|
||||
## Short reviewAdditively manufactured particle damping structures: A review of manufacturing and filling approaches, design variables and evidence comparability
|
||||
|
||||
,,,,,
|
||||
|
||||
[View **PDF**](https://www.sciencedirect.com/science/article/pii/S2772369026000642/pdfft?md5=cba1ac2d869f0e06cdfb0cbb3e12bde4&pid=1-s2.0-S2772369026000642-main.pdf)
|
||||
|
||||
[10.1016/j.addlet.2026.100417](https://doi.org/10.1016/j.addlet.2026.100417)
|
||||
|
||||
## Highlights
|
||||
|
||||
## Keywords
|
||||
|
||||
Additive manufacturing
|
||||
|
||||
;
|
||||
|
||||
Particle damping
|
||||
|
||||
;
|
||||
|
||||
Powder bed fusion
|
||||
|
||||
;
|
||||
|
||||
Structural damping
|
||||
|
||||
;
|
||||
|
||||
Vibration mitigation
|
||||
|
||||
- [Previous article in this issue](https://www.sciencedirect.com/science/article/pii/S2772369026000575)
|
||||
- [Next article in this issue](https://www.sciencedirect.com/science/article/pii/S2772369026000629)
|
||||
|
||||
## 1\. Introduction
|
||||
|
||||
Lightweight and functional additively manufactured components are increasingly used in high performance applications,, where vibration can limit structural performance, process stability or functional precision. Additional damping is attractive in such cases, but external damping devices can add mass, occupy design space or disturb the component function,. Particle damping offers a compact passive approach in which vibration energy is dissipated through relative particle motion, impacts and frictional contacts when particles have sufficient freedom to move inside a cavity,.
|
||||
|
||||
Additive manufacturing changes how this mechanism can be integrated. Internal cavities, local architecture and particle filled volumes can be designed together with the structural load path, so particle damping can be integrated within the printed component instead of added as a separate damping element,,. In additively manufactured particle damping structures (AMPDs), the damping medium may be unfused build powder retained during powder bed fusion of metals using a laser beam (PBF-LB/M) or particles introduced after fabrication. summarizes these manufacturing and filling approaches and their integration into AMPD structures. This integration has been studied, for example, for blade like parts,,, machining tools,, vibration sensitive optical holders and topology based lightweight design concepts.
|
||||
|
||||

|
||||
|
||||
Download: Download high-res image (277KB)
|
||||
|
||||
The recent AMPD literature has moved beyond isolated feasibility demonstrations. Retained powder beams,, blades, walls, gears, optical holders and tooling elements have shown measurable reductions in vibration response or increases in damping under specific test conditions. These examples indicate a broad application space, but they are spread across different manufacturing and filling approaches, powder or particle states, cavity designs, reported frequency ranges and evaluation methods.
|
||||
|
||||
This creates a comparability problem that goes beyond terminology. Similar AMPD terminology can describe retained build powder, particles introduced after fabrication or related particle damping concepts, although these approaches differ in how the damping medium is created, controlled and qualified,,,. Reported damping improvements therefore cannot be interpreted as transferable design evidence by metric value alone. The central question is whether these case specific AMPD results can be organized into transferable design guidance without merging physically different manufacturing and filling approaches.
|
||||
|
||||
Prior reviews provide complementary foundations for this question. Gagnon et al. synthesize particle-damper modeling, discrete-element calibration and experimental testing, while Ehlers et al. focus on design guidelines for laser-beam-melted retained-powder dampers. Niedermeyer et al. examine compressor-blade requirements and AMPD potential, and Zhu et al. review tuned particle dampers across mechanisms, models and applications. The present review builds on these reviews by comparing AMPD manufacturing and filling approaches, their testing methods and the way performance is reported. This comparison shows which findings can be considered together and where differences among evidence units still limit broader design guidance.
|
||||
|
||||
This review addresses that question by organizing a structured AMPD evidence table with 108 publication records around explicit boundaries between manufacturing and filling approaches. It focuses on where AMPD has been applied, which reported frequency ranges and validation evidence are available, and which cavity, powder or particle, excitation, metric and reporting variables should be considered before results are compared across evidence units. It also derives a compact reporting set that improves comparability in future AMPD work.
|
||||
|
||||
## 2\. Evidence base and classification framework
|
||||
|
||||
The synthesis uses a structured AMPD evidence table with 108 publication records (R1–R108). Scopus was used as the primary database, with complementary Web of Science searches, Google Scholar checks, and backward and forward citation tracking. The first complete search round was completed on 14 January 2026, and the final update search was conducted on 12 June 2026 using the same retrieval logic.
|
||||
|
||||
The first author conducted the keyword searches, compiled the evidence table and manually checked its publication records and classifications against the corresponding sources. Eligibility and ambiguous cases were assessed using the documented rules. Supplementary File 1 is the AMPD evidence table with the publication records, evidence-unit assignments and coded data. Supplementary File 2 is the AMPD Search and Mapping Protocol with the search and figure classification rules. The verified table was then processed using a MATLAB script to generate the figures and supporting count tables.
|
||||
|
||||
A publication record is one bibliographic row in the evidence table. For,,,, an evidence unit is the smallest independently countable contribution, such as a distinct specimen group, experimental data set or original model contribution. Potentially duplicate and overlapping publication records were checked during selection, and alternate publication records based on the same specimens, data or experiment were combined into one evidence unit. Similar authorship or topic alone was not treated as evidence of duplication. Publication records containing both unique and reused evidence were retained and flagged in the evidence table.
|
||||
|
||||
In the manuscript, the evidence table has two practical roles. It defines how the publication records are grouped by manufacturing and filling approach, and it keeps the evidence unit counts traceable. Publication records were classified as AMPD when additive manufacturing defined the damping structure and loose unfused powder or inserted particles were the damping medium. Related publication records were kept when they helped compare manufacturing and filling approaches, but they were not included in the direct retained-powder or post-filled AMPD evidence unit counts. Publication records representing reviews, providing limited detail or showing substantial overlap were retained for context when useful, but were not treated as evidence units in the figures when they mainly synthesized or reused earlier data. Each publication record was coded for process, powder and cavity descriptors, validation level, reported frequency ranges, excitation regime, response metrics, baseline information, limitations and its role in forming evidence units.
|
||||
|
||||
## 3\. Manufacturing and filling approach boundaries
|
||||
|
||||
Manufacturing and filling approach is the primary classification variable. It describes how the damping medium is created, retained or introduced in the additively manufactured structure.
|
||||
|
||||
summarizes 79 independent AMPD evidence units derived from the 108 publication records in the evidence table. These comprise 29 direct retained-powder evidence units without designed internal structures, 35 direct retained-powder evidence units with designed internal structures and 15 post-filled evidence units. The horizontal bars show the number of evidence units in each manufacturing and filling category, and the colored segments show validation level. The evidence table lists the publication records corresponding to each evidence unit.,, examine the 64 direct retained-powder evidence units.
|
||||
|
||||
Validation level was classified independently of manufacturing and filling approach. It describes the context in which a result was obtained. The five definitions are given in.
|
||||
|
||||
separates direct retained-powder AMPD into two categories according to the presence of designed internal structures. In both categories, loose or partially mobile unfused build powder remains inside sealed printed volumes and contributes to damping,,. Many use PBF-LB/M, which leaves unfused powder inside closed cavities,,. The first category contains 29 evidence units with simple sealed cavities and no designed internal structures. Examples include wall, specimen and beam evidence units,,,.
|
||||
|
||||
Table 1. Definitions of the validation levels used in this review.
|
||||
|
||||
| Level | Definition |
|
||||
| --- | --- |
|
||||
| Concept | Concept or contextual contribution without original numerical analysis or physical testing. |
|
||||
| Numerical | Modeling, simulation or optimization as the primary contribution, without new physical damping tests. |
|
||||
| Specimen | Tests on coupons, beams, blocks, dampers or other bench-scale specimens. |
|
||||
| Component | Tests on a functional component or subsystem outside its final service environment. |
|
||||
| Application | Tests under application-relevant loading or environmental conditions, or with a functional performance metric. |
|
||||
|
||||

|
||||
|
||||
Download: Download high-res image (256KB)
|
||||
|
||||

|
||||
|
||||
Download: Download high-res image (263KB)
|
||||
|
||||
Table 2. Representative comparisons within evidence units for the three AMPD categories in.
|
||||
|
||||
| Category and source | Comparison | Test and reported result | Main insight |
|
||||
| --- | --- | --- | --- |
|
||||
| Direct retained-powder, simple cavity. Westbeld et al.. | AlSi10Mg specimens with mobile or sintered powder were compared with solid references. The evidence unit included 44 cavity specimens, 18 solid specimens and four measurements per specimen. | Periodic chirp at 800 mm/s <sup>2</sup> over 50–8000 Hz. Global sintering produced no significant particle damping. Mobile powder produced a maximum relative loss factor increase of 1425%. | Powder mobility determines whether damping is activated. |
|
||||
| Direct retained-powder, internal pockets. Scott-Emuakpor et al.. | Four IN718 AMPD blades were compared with four fully fused blades. | A 0–6000 Hz sweep was followed by modal and fatigue tests. Mean quality factor decreased by about 45% and 60% at two modes, while fatigue resistance increased. | Modal response and durability should be evaluated together. |
|
||||
| Post-filled TPMS tool. Han et al.. | Four tool variants were compared with a solid tool under 16 cutting condition groups. Repeat count was not reported. | Dry turning with modes near 1299, 1303 and 5119 Hz. At 145 g fill mass, damping ratio reached 0.03 and energy dissipation efficiency reached 48%. Low fill could underperform the solid tool. | Fill state and operating condition determine the functional benefit. |
|
||||
|
||||
The second category contains 35 evidence units with designed internal structures. Examples include divided cavities, ribs, lattice cavities, resonant features and flexure guided structures,,,,,. Internal design adds a distinct design variable by changing how the powder volume is arranged within the printed structure.
|
||||
|
||||
The third category contains 15 post-filled AMPD evidence units. In this category, additive manufacturing creates the host structure, cavity, insert or module, while the particle damping medium is introduced and sealed after fabrication. Mixed retained and inserted cases are included in this category. Examples include additively manufactured toolholder and machining evidence units,, post-filled inserts or modules, and TPMS-based particle dampers,. Six related publication records outside these definitions remain as unplotted context in the evidence table,,,.
|
||||
|
||||
gives one representative comparison from each AMPD category in. The complete performance summary is provided in the evidence table.
|
||||
|
||||
The distribution of validation levels in shows where the available evidence is concentrated. Most evidence in the two direct retained-powder categories comes from specimen tests, including walls and beams,,,,. Component and application evidence is less common and appears in blades,, gears, optical holders and post-filled machining systems. Nine numerical evidence units address particle behavior, packing density control and design optimization,,,. Section therefore examines cavity placement and internal design in the 64 direct retained-powder evidence units.
|
||||
|
||||
## 4\. Direct retained-powder design variables
|
||||
|
||||
After the manufacturing and filling approach boundaries in, focuses on the direct retained-powder subset. It maps the cavity placement and cavity design classifications of 64 independent evidence units. The figure shows how retained powder volumes are positioned and shaped internally, so the following discussion can focus on design patterns instead of repeating the approach boundary.
|
||||
|
||||
Each direct retained-powder evidence unit contributes to one primary placement class and one primary cavity design class in. Detailed class definitions and precedence rules for cases with multiple applicable descriptions are provided in Supplementary File 2.
|
||||
|
||||
The placement axis describes the logic used to locate the powder volume. Mode targeted evidence units place cavities with respect to modal or operational response, including modal displacement, antinode, strain or forced response regions,,. Neutral axis evidence units use a low strain or neutral axis region as the placement reference when damping space must be balanced with stiffness or functional geometry,,. Multiple cavities describe distributed powder pockets or chamber arrays within one structure,,. Component layout covers cases where the available part geometry or functional space drives the cavity position, as in gears, instrumentation rake bodies and tooling elements,,. Cavity variation is retained as the fallback placement category when cavity position is compared together with size, number or other cavity design parameters and no single placement rule dominates,,.
|
||||
|
||||
The design axis describes the internal form of the powder containing volume. Simple cavity evidence units use closed or sealed powder volumes without designed internal structures,. Divided cavities split the powder space into chambers, pockets or partitioned regions,. Internal features add ribs, stiffening features or other obstacles inside the cavity,,. Lattice cavity evidence units combine retained powder with lattice type members or chambered lattice structures,,. Local resonator evidence units couple retained powder to a resonant substructure or absorber type design,. In this classification, multiple cavities and divided cavities are not duplicates. The first describes distributed placement of powder volumes, while the second describes subdivision of the cavity interior.
|
||||
|
||||
The plotted counts show where direct retained-powder AMPD design evidence is concentrated. Cavity variation is the largest placement category with 28 evidence units, followed by mode targeted placement with 20 evidence units. Multiple cavities and component layout each contain 6 evidence units, and neutral axis placement contains 4 evidence units. On the design axis, simple cavities and divided cavities form the largest categories with 29 and 19 evidence units, followed by internal features with 7 evidence units. Local resonators appear in 5 evidence units and lattice cavities in 4 evidence units. The most populated cells are cavity variation with simple cavities, mode targeted placement with simple cavities and mode targeted placement with divided cavities. This pattern shows that the direct retained-powder literature is weighted toward modal placement, cavity design comparisons and simple or partitioned cavity designs.
|
||||
|
||||
This classification supports a more specific design interpretation. Cavity placement can matter as much as cavity volume because retained powder must move relative to the cavity walls under the active response,,. At the same time, cavity design strategy changes both powder motion and structural response, because partitions, ribs, lattice members and resonant substructures can modify particle travel distance, contact conditions, local stiffness and coupling to a target mode,,,. Their benefit is conditional because the same feature that redirects particles can also reduce clearance, restrict powder mobility or change the load carrying geometry,,. Geometry descriptors should therefore be read together with powder state and baseline definition. Cavity ratio, cavity volume fraction, unfused powder volume percentage, particle filling ratio and packing density describe related but different quantities, and they should not be treated as interchangeable damping predictors,,,.
|
||||
|
||||
This design classification provides the context for comparing reported frequency ranges, excitation regimes and validation metrics in Section.
|
||||
|
||||
## 5\. Validation evidence and metric comparability
|
||||
|
||||
After the manufacturing and filling approach boundaries in and the direct retained-powder design variables in, the next comparison is how these designs have been tested. maps the frequency information reported for 64 direct retained-powder AMPD evidence units. It separates impact-hammer FRF, impulse or free decay, shock or transient loading, harmonic or swept-sine testing, random or broadband testing, mixed or operational testing and numerical or modeling-only work as primary evaluation methods. Detailed method definitions and assignment rules are provided in Supplementary File 2, while the primary and secondary method classifications for each evidence unit are listed in Supplementary File 1.
|
||||
|
||||
The 64 evidence units comprise 26 harmonic or swept-sine, 15 impact-hammer FRF, 9 numerical or modeling-only, 7 mixed or operational, 5 impulse or free-decay and 2 shock or transient evaluations. None uses random or broadband testing as its primary method, although broadband input appears as a secondary method in some mixed or operational evidence units.
|
||||
|
||||

|
||||
|
||||
Download: Download high-res image (1MB)
|
||||
|
||||
Of the 64 evidence units, 18 report continuous ranges, 6 discrete point sets, 28 modal-frequency sets and 8 local bands. Four lack a verifiable numeric frequency or mode and remain listed as no numeric beside their source labels. Filled circles mark continuous-range endpoints and discrete points, filled diamonds mark modal frequencies and filled squares mark local-band endpoints. Each source mark uses the color assigned to its validation level. Ranges beginning at 0 Hz are shown from the 1-Hz limit of the logarithmic axis.
|
||||
|
||||
The frequency information in becomes meaningful when the input method and response metric are read together. Impact-hammer FRF tests identify modes and describe damping or response amplitude around resonance. Impulse or free-decay tests obtain modal damping from the response after release or impulse. Shock or transient tests quantify the decay after a short input through measures such as quality factor and damping ratio. Harmonic or swept-sine tests resolve changes in resonance, loss metrics and dissipated energy across frequency and amplitude.
|
||||
|
||||
Mixed or operational tests connect the vibration response to functional measures such as stress, fatigue or transmissibility,. Numerical evidence units examine particle motion and particle–wall interactions, with experimental calibration determining their design relevance. The absence of random or broadband excitation as a primary method leaves service representative broadband loading as a validation gap.
|
||||
|
||||
These metrics describe different parts of the structural response. Interpreting a lower FRF peak requires checking mass, stiffness and resonance shift together with damping. Comparison across evidence units therefore requires the input type and amplitude, frequency or mode, response location, metric definition and baseline to be reported together. A useful next step is to test several modes with more than one input method on the same specimens and baseline. This would connect modal damping, FRF amplitude, energy loss and functional response under controlled conditions.
|
||||
|
||||
Excitation amplitude is a design variable in AMPD because the particle motion changes as the input increases. At low input, the powder can move with the cavity walls and dissipate little energy. As relative motion develops, sliding and collisions increase dissipation. Further increases can produce saturation, softening, hysteresis or jump behavior,,. Characterizing this working range requires damping measurements at several specified amplitudes. Frequency sweeps should therefore be repeated at controlled amplitudes and in both sweep directions, with response amplitude and activation or saturation thresholds reported. The resulting frequency and amplitude maps would show whether a design remains effective across its intended load range.
|
||||
|
||||
PBF-LB/M feedstock powder introduces a second design dimension. Micrometer scale powder has a greater relative influence of attractive and surface forces than the millimeter scale particles used in many classical dampers,. Its mobility also depends on material, particle size distribution, surface condition, packing density and compaction,,,. The same nominal cavity geometry can therefore show different damping when the powder material or state changes. Controlled comparisons across materials should hold cavity geometry, structural baseline and excitation constant while varying powder material, size distribution, packing and compaction. maps testing conditions and validation levels, while the evidence table records the particle descriptors and powder state needed for this comparison.
|
||||
|
||||

|
||||
|
||||
Download: Download high-res image (349KB)
|
||||
|
||||
Table 3. Baseline comparisons for three recurring research purposes in the reviewed AMPD literature.
|
||||
|
||||
| Purpose | Suitable comparison | Supported interpretation |
|
||||
| --- | --- | --- |
|
||||
| Mechanism attribution | Compare retained-powder specimens with corresponding empty cavity, solid or altered powder state specimens. Keep the boundary condition and excitation consistent, and report changes in mass, stiffness, natural frequency and mode shape,,. | Whether the measured response is consistent with particle mobility and dissipation at the tested mode, amplitude and powder state. |
|
||||
| Design trade-off under stated constraints | Compare feasible designs under the same functional requirements and report the relevant mass, stiffness, strength, manufacturing and frequency constraints,,. | The vibration benefit obtained within the tested design constraints, including damping and changes in resonance. |
|
||||
| Functional performance and durability | Compare the AMPD design with a functional reference under the same mounting, loading and environmental conditions, and include repeated specimens or cyclic states where available,,. | The functional benefit and its repeatability or stability over the tested conditions and duration. |
|
||||
|
||||
Taken together, the 64 evidence units comprise 41 specimen evidence units, 9 numerical evidence units, 7 component evidence units and 7 application evidence units. The distribution is concentrated at specimen level, while component and application evidence each account for 7 evidence units.
|
||||
|
||||
The testing and frequency evidence in must be interpreted together with the reported response metric and baseline because a reduction in vibration response can arise from particle dissipation, changes in mass or stiffness, a shift in resonance, or a combination of these effects. The baseline must therefore be chosen according to the question being tested. summarizes the baseline implications derived from analysis through three recurring research purposes: identifying the contribution of particle mobility, evaluating vibration performance under stated design constraints, and testing functional performance and durability. For each purpose, the table links a suitable comparison with the conclusion that the available evidence can support. The reporting information needed for these comparisons is examined in Section.
|
||||
|
||||
## 6\. Reporting completeness and comparability needs
|
||||
|
||||
Comparisons across AMPD evidence units become difficult when important experimental information is incomplete or reported in different ways. therefore examines the reporting completeness of 64 direct retained-powder AMPD evidence units. The fields cover the information needed to describe their designs, tests and validation results, with detailed definitions in Supplementary File 2 and the corresponding evidence in Supplementary File 1. Each field is classified as Reported, Partly reported, Not reported or Not applicable. The applicable denominator includes the first three statuses, while Not applicable is shown separately.
|
||||
|
||||
shows that basic descriptions of AMPD design and testing are available in most evidence units. AM process and material and boundary condition each reach the Reported threshold in 60 evidence units. Cavity metric reaches it in 59 evidence units, geometry in 58 evidence units and excitation level in 50 evidence units. The largest gaps are concentrated in particle fill ratio, packing density or powder state, repeatability or uncertainty, and lifecycle or degradation. The following paragraphs discuss why these four areas remain incomplete and how they affect comparison and reproducibility.
|
||||
|
||||
Particle fill ratio and packing density describe two linked controls of retained powder motion. Fill ratio sets the powder amount relative to cavity volume, while packing density and powder state determine how that material is arranged and constrained. In, particle fill ratio is Reported in 5 evidence units, Partly reported in 56 and Not reported in 3. Packing density or powder state is Reported in 38 evidence units, Partly reported in 25 and Not reported in 1. The distinction is mechanically important. Fill ratio governs the overall free space available for particle motion. Packing density, compaction and cohesion govern the internal contact network, frictional sliding and the excitation threshold required to mobilize the powder,,,. Identical cavity geometry and nominal fill ratio can therefore produce different damping after processing or repeated loading changes the powder state. Future AMPD work should report a clearly defined volume or mass basis together with the measured powder state before and after testing, allowing particle activation and energy dissipation to be linked to a reproducible internal condition.
|
||||
|
||||
Repeatability or uncertainty is Reported in 33 evidence units, Partly reported in 28, Not reported in 1 and Not applicable in 2. The large Partly reported group mainly contains specimen or repeat counts without a measure of variation. Repeated measurements on one specimen characterize variation in the test and response. Measurements across specimens and builds capture variation introduced by manufacturing and the retained powder state. Local packing, compaction and powder redistribution can change the damping response under nominally identical geometry and loading,,. Repeated runs can provide a precise mean for one specimen. Reproducibility across specimens and builds requires separate replication. Future AMPD work should distinguish repeated runs, specimens and builds and report dispersion or uncertainty at each level together with the corresponding powder state.
|
||||
|
||||
Table 4. Proposed minimum AMPD reporting checklist for future work.
|
||||
|
||||
| Reporting item | Minimum information | Risk if omitted |
|
||||
| --- | --- | --- |
|
||||
| Approach identity | Identify retained build powder, post-filled particles or another related approach. Report sealing and powder removal where relevant. | Routes may be compared although their damping media are created and controlled differently. |
|
||||
| Cavity and structure | Report cavity placement, wall thickness, internal design, mass change and geometry relevant to stiffness. | Geometry or stiffness effects may be attributed to powder damping. |
|
||||
| Powder or particle state | Report particle material and size, retained powder condition, packing density or fill measure, and heat treatment or compaction history. | Fill ratio, packing density and powder state may be treated as equivalent. |
|
||||
| Test condition | Report input type and amplitude, frequency range or test points, mounting and signal chain. | Results may be compared across different particle activation conditions. |
|
||||
| Baseline and metric | Define the reference and report AMPD and reference mass, powder or particle mass where available, natural-frequency shift, stiffness change or a justified proxy, and the response or functional metric. | Mass, stiffness and detuning may confound interpretation of the damping benefit. |
|
||||
| Repeatability and service | Report specimen and repeat counts, uncertainty, repeated excitation effects, degradation and powder state after testing. | Initial performance may be interpreted as repeatable or durable. |
|
||||
|
||||
Lifecycle or degradation is Reported in 25 evidence units, Partly reported in 2, Not reported in 34 and Not applicable in 3, making it the largest Not reported group in. Most evidence units therefore characterize AMPD performance in its initial state, leaving stability under mechanical and thermal history unresolved. Retained powder damping is state dependent. Repeated resonance passes and high strain dwell can compact, redistribute or locally fuse the powder,,. Heat treatment can form sintered contacts and reduce particle mobility, while later excitation can fragment some contacts and change the response again. Degradation can therefore involve transitions between loose, compacted, trapped and sintered powder states, with corresponding changes in activation and energy dissipation,. Application validation should track damping against load cycles, amplitude and thermal history and document the powder state before and after testing. This would show whether the damping response remains stable, changes gradually or undergoes an irreversible loss.
|
||||
|
||||
These reporting gaps motivate the AMPD reporting checklist in. The checklist combines the weak reporting fields in with the manufacturing and filling approach, cavity design and validation variables discussed above. It lists the minimum information that future AMPD work should report before results are compared across manufacturing and filling approaches, cavity designs, test conditions and baselines.
|
||||
|
||||
## 7\. Design implications
|
||||
|
||||
This section discusses the design implications of the reviewed evidence and priorities for future AMPD research.
|
||||
|
||||
The first design implication from the manufacturing and filling categories in and is that the AMPD route should be selected according to the design variable that must remain controllable in the intended application. Direct retained-powder designs without designed internal structures provide control through cavity placement and geometry, designed internal structures add coupled control through internal design, and post-filled designs provide independent control of particle morphology and fill ratio after fabrication,,,,,,,. This route decision should precede detailed cavity optimization.
|
||||
|
||||
The second design implication from Section and is that cavity placement and cavity design form one optimization problem for direct retained-powder AMPDs. The target mode, load path and functional response define where retained powder motion is useful, while structural and manufacturing constraints define which internal design is feasible,,,,,,. The selected combination should then be judged using application measures such as cutting stability, forced response or optical stability,,.
|
||||
|
||||
The third design implication from the validation levels in Section and is that each level should answer a different question through its test method, frequency evidence and reported metric. Numerical evidence units can identify candidate modes and response bands and screen particle activation trends,,. At specimen level, harmonic or swept-sine tests and impact-hammer FRFs should map activation, amplitude dependence and modal damping across several amplitudes and modes,,. Component tests should retain the relevant modal or local frequency information while adding mounting, stiffness, resonance shifts and modal coupling,,. Across both routes, application tests should reproduce operational inputs and connect frequency response to functional measures such as forced response, fatigue, cutting stability or optical stability,,,,,,. Repeatability and response stability under repeated excitation or service exposure then become part of qualification,,,,. Validation should therefore progress from mechanism and activation maps, through integrated component response, to functional performance and stability over time.
|
||||
|
||||
The fourth design implication from the reporting completeness analysis in Section and is that a transferable AMPD design must be defined across its full lifecycle. Its initial particle or powder condition, variation across specimens and builds, and changes during repeated use form one continuous design record that links the manufactured state to reproducibility and stability under operating conditions,,,,,.
|
||||
|
||||
In summary, the preceding design implications point to four research priorities. First, shared reference geometries and open data for each evidence unit should connect damping metrics to matched baselines. Second, nondestructive indicators of retained powder state should be calibrated against mobility and dynamic response. Third, lifecycle tests should quantify compaction, sintering, recovery, leakage and fatigue interactions. Fourth, multiscale models should propagate manufacturing, material-batch, boundary-condition and internal-state variability into response uncertainty. Together, these priorities connect AMPD design choices with the modeling, validation and reporting needed to compare performance across machines, materials, heat treatments and service conditions.
|
||||
|
||||
## 8\. Conclusions
|
||||
|
||||
This review connects the classification of AMPD manufacturing and filling approaches with cavity design, testing methods, reported performance and the evidence still needed for reliable comparison and qualification. The main conclusions follow this sequence from route selection and design to validation, reporting completeness and future development:
|
||||
|
||||
- •
|
||||
The evidence table contains 108 publication records and yields 79 independent AMPD evidence units, comprising 64 direct retained-powder evidence units and 15 post-filled evidence units. The detailed design, frequency and reporting analyses use the 64 direct evidence units, while the 15 post-filled evidence units remain in the route and performance comparisons. Six related publication records remain in the evidence table as context. Because the two AMPD routes create and control the damping medium differently, the manufacturing and filling approach is the starting point for design interpretation.
|
||||
- •
|
||||
The review also establishes a common framework for comparing direct retained-powder AMPD evidence units across cavity placement, internal design, validation level, testing method, frequency evidence and reported performance. This framework places each result within the design and test conditions under which it was obtained. The synthesis retains the original response metric and comparison baseline, making differences among evidence units visible and supporting more consistent interpretation.
|
||||
- •
|
||||
The largest reporting gaps concern particle fill ratio, packing density and particle or powder state, repeatability or uncertainty, and lifecycle or degradation. Reporting these fields links the initial internal condition to variation across specimens and builds and to changes during repeated use or service. This evidence supports evaluation of reproducibility and stability under the intended operating conditions.
|
||||
|
||||
This review therefore provides a unified basis for future AMPD research by connecting route selection, performance interpretation and the evidence required for reproducible and transferable design across materials, manufacturing processes and operating conditions.
|
||||
|
||||
## CRediT authorship contribution statement
|
||||
|
||||
**Weijia Yu:** Writing – review & editing, Writing – original draft, Visualization, Software, Methodology, Investigation, Formal analysis, Data curation, Conceptualization. **Marcus Oel:** Writing – review & editing. **Jens Niedermeyer:** Writing – review & editing. **Lennart Mesecke:** Writing – review & editing. **Ina Meyer:** Writing – review & editing. **Roland Lachmayer:** Writing – review & editing, Supervision.
|
||||
|
||||
## Declaration of generative AI and AI-assisted technologies in the manuscript preparation process
|
||||
|
||||
During the preparation of this work the authors used OpenAI Codex and ChatGPT to support language polishing, editorial revision, and preparation checks for the manuscript, figures and supplementary materials. The tools were not used to independently generate scientific content, evidence classification decisions, data, results or interpretations. After using these tools, the authors reviewed, verified and edited the content as needed and take full responsibility for the content of the published article.
|
||||
|
||||
## Funding
|
||||
|
||||
This research did not receive any specific grant from funding agencies in the public, commercial, or not-for-profit sectors.
|
||||
|
||||
## Declaration of competing interest
|
||||
|
||||
The authors declare that they have no known competing financial interests or personal relationships that could have appeared to influence the work reported in this paper.
|
||||
|
||||
## Appendix A. Supplementary data
|
||||
|
||||
The following is the Supplementary material related to this article. [Download: Download zip file (3MB)](https://ars.els-cdn.com/content/image/1-s2.0-S2772369026000642-mmc1.zip "Download zip file (3MB)")
|
||||
|
||||
MMC S1. AMPD evidence table, search and mapping protocol, MATLAB code, and supporting figure-classification files.
|
||||
|
||||
## Data availability
|
||||
|
||||
The evidence table, search and mapping protocol, and figure generation files supporting this review are supplied as supplementary material. Supplementary file 1 contains the AMPD evidence table in Excel format and includes the master evidence table used for screening, extraction, manufacturing and filling approach classification, figure classification and synthesis. Supplementary file 2 combines the AMPD Search and Mapping Protocol with the figure generation and classification note for the four evidence figures shown as manuscript Figures 2 to 5, including search sources, eligibility rules, controlled vocabulary, figure filters, derived classes and classification rules. Supplementary file 3 is the MATLAB script used to generate the four evidence figures from the supplied evidence table, including supporting count tables. Zenodo version 3 is registered at [10.5281/zenodo.21980315](https://doi.org/10.5281/zenodo.21980315), and the all-versions concept DOI is [10.5281/zenodo.20112102](https://doi.org/10.5281/zenodo.20112102). The Zenodo metadata are public, while the deposited files are embargoed until 31 December 2026. The supplementary files supplied with the resubmission provide the immediately accessible reproducibility package.
|
||||
|
||||
## References
|
||||
|
||||
[^1]: ## 1\. Introduction
|
||||
|
||||
Lightweight and functional additively manufactured components are increasingly used in high performance applications,, where vibration can limit structural performance, process stability or functional precision. Additional damping is attractive in such cases, but external damping devices can add mass, occupy design space or disturb the component function,. Particle damping offers a compact passive approach in which vibration energy is dissipated through relative particle motion, impacts and frictional contacts when particles have sufficient freedom to move inside a cavity,.
|
||||
|
||||
Additive manufacturing changes how this mechanism can be integrated. Internal cavities, local architecture and particle filled volumes can be designed together with the structural load path, so particle damping can be integrated within the printed component instead of added as a separate damping element,,. In additively manufactured particle damping structures (AMPDs), the damping medium may be unfused build powder retained during powder bed fusion of metals using a laser beam (PBF-LB/M) or particles introduced after fabrication. summarizes these manufacturing and filling approaches and their integration into AMPD structures. This integration has been studied, for example, for blade like parts,,, machining tools,, vibration sensitive optical holders and topology based lightweight design concepts.
|
||||
|
||||

|
||||
|
||||
Download: Download high-res image (277KB)
|
||||
|
||||
The recent AMPD literature has moved beyond isolated feasibility demonstrations. Retained powder beams,, blades, walls, gears, optical holders and tooling elements have shown measurable reductions in vibration response or increases in damping under specific test conditions. These examples indicate a broad application space, but they are spread across different manufacturing and filling approaches, powder or particle states, cavity designs, reported frequency ranges and evaluation methods.
|
||||
|
||||
This creates a comparability problem that goes beyond terminology. Similar AMPD terminology can describe retained build powder, particles introduced after fabrication or related particle damping concepts, although these approaches differ in how the damping medium is created, controlled and qualified,,,. Reported damping improvements therefore cannot be interpreted as transferable design evidence by metric value alone. The central question is whether these case specific AMPD results can be organized into transferable design guidance without merging physically different manufacturing and filling approaches.
|
||||
|
||||
Prior reviews provide complementary foundations for this question. Gagnon et al. synthesize particle-damper modeling, discrete-element calibration and experimental testing, while Ehlers et al. focus on design guidelines for laser-beam-melted retained-powder dampers. Niedermeyer et al. examine compressor-blade requirements and AMPD potential, and Zhu et al. review tuned particle dampers across mechanisms, models and applications. The present review builds on these reviews by comparing AMPD manufacturing and filling approaches, their testing methods and the way performance is reported. This comparison shows which findings can be considered together and where differences among evidence units still limit broader design guidance.
|
||||
|
||||
This review addresses that question by organizing a structured AMPD evidence table with 108 publication records around explicit boundaries between manufacturing and filling approaches. It focuses on where AMPD has been applied, which reported frequency ranges and validation evidence are available, and which cavity, powder or particle, excitation, metric and reporting variables should be considered before results are compared across evidence units. It also derives a compact reporting set that improves comparability in future AMPD work.
|
||||
|
||||
## 2\. Evidence base and classification framework
|
||||
|
||||
The synthesis uses a structured AMPD evidence table with 108 publication records (R1–R108). Scopus was used as the primary database, with complementary Web of Science searches, Google Scholar checks, and backward and forward citation tracking. The first complete search round was completed on 14 January 2026, and the final update search was conducted on 12 June 2026 using the same retrieval logic.
|
||||
|
||||
The first author conducted the keyword searches, compiled the evidence table and manually checked its publication records and classifications against the corresponding sources. Eligibility and ambiguous cases were assessed using the documented rules. Supplementary File 1 is the AMPD evidence table with the publication records, evidence-unit assignments and coded data. Supplementary File 2 is the AMPD Search and Mapping Protocol with the search and figure classification rules. The verified table was then processed using a MATLAB script to generate the figures and supporting count tables.
|
||||
|
||||
A publication record is one bibliographic row in the evidence table. For,,,, an evidence unit is the smallest independently countable contribution, such as a distinct specimen group, experimental data set or original model contribution. Potentially duplicate and overlapping publication records were checked during selection, and alternate publication records based on the same specimens, data or experiment were combined into one evidence unit. Similar authorship or topic alone was not treated as evidence of duplication. Publication records containing both unique and reused evidence were retained and flagged in the evidence table.
|
||||
|
||||
In the manuscript, the evidence table has two practical roles. It defines how the publication records are grouped by manufacturing and filling approach, and it keeps the evidence unit counts traceable. Publication records were classified as AMPD when additive manufacturing defined the damping structure and loose unfused powder or inserted particles were the damping medium. Related publication records were kept when they helped compare manufacturing and filling approaches, but they were not included in the direct retained-powder or post-filled AMPD evidence unit counts. Publication records representing reviews, providing limited detail or showing substantial overlap were retained for context when useful, but were not treated as evidence units in the figures when they mainly synthesized or reused earlier data. Each publication record was coded for process, powder and cavity descriptors, validation level, reported frequency ranges, excitation regime, response metrics, baseline information, limitations and its role in forming evidence units.
|
||||
|
||||
## 3\. Manufacturing and filling approach boundaries
|
||||
|
||||
Manufacturing and filling approach is the primary classification variable. It describes how the damping medium is created, retained or introduced in the additively manufactured structure.
|
||||
|
||||
summarizes 79 independent AMPD evidence units derived from the 108 publication records in the evidence table. These comprise 29 direct retained-powder evidence units without designed internal structures, 35 direct retained-powder evidence units with designed internal structures and 15 post-filled evidence units. The horizontal bars show the number of evidence units in each manufacturing and filling category, and the colored segments show validation level. The evidence table lists the publication records corresponding to each evidence unit.,, examine the 64 direct retained-powder evidence units.
|
||||
|
||||
Validation level was classified independently of manufacturing and filling approach. It describes the context in which a result was obtained. The five definitions are given in.
|
||||
|
||||
separates direct retained-powder AMPD into two categories according to the presence of designed internal structures. In both categories, loose or partially mobile unfused build powder remains inside sealed printed volumes and contributes to damping,,. Many use PBF-LB/M, which leaves unfused powder inside closed cavities,,. The first category contains 29 evidence units with simple sealed cavities and no designed internal structures. Examples include wall, specimen and beam evidence units,,,.
|
||||
|
||||
Table 1. Definitions of the validation levels used in this review.
|
||||
|
||||
| Level | Definition |
|
||||
| --- | --- |
|
||||
| Concept | Concept or contextual contribution without original numerical analysis or physical testing. |
|
||||
| Numerical | Modeling, simulation or optimization as the primary contribution, without new physical damping tests. |
|
||||
| Specimen | Tests on coupons, beams, blocks, dampers or other bench-scale specimens. |
|
||||
| Component | Tests on a functional component or subsystem outside its final service environment. |
|
||||
| Application | Tests under application-relevant loading or environmental conditions, or with a functional performance metric. |
|
||||
|
||||

|
||||
|
||||
Download: Download high-res image (256KB)
|
||||
|
||||

|
||||
|
||||
Download: Download high-res image (263KB)
|
||||
|
||||
Table 2. Representative comparisons within evidence units for the three AMPD categories in.
|
||||
|
||||
| Category and source | Comparison | Test and reported result | Main insight |
|
||||
| --- | --- | --- | --- |
|
||||
| Direct retained-powder, simple cavity. Westbeld et al.. | AlSi10Mg specimens with mobile or sintered powder were compared with solid references. The evidence unit included 44 cavity specimens, 18 solid specimens and four measurements per specimen. | Periodic chirp at 800 mm/s <sup>2</sup> over 50–8000 Hz. Global sintering produced no significant particle damping. Mobile powder produced a maximum relative loss factor increase of 1425%. | Powder mobility determines whether damping is activated. |
|
||||
| Direct retained-powder, internal pockets. Scott-Emuakpor et al.. | Four IN718 AMPD blades were compared with four fully fused blades. | A 0–6000 Hz sweep was followed by modal and fatigue tests. Mean quality factor decreased by about 45% and 60% at two modes, while fatigue resistance increased. | Modal response and durability should be evaluated together. |
|
||||
| Post-filled TPMS tool. Han et al.. | Four tool variants were compared with a solid tool under 16 cutting condition groups. Repeat count was not reported. | Dry turning with modes near 1299, 1303 and 5119 Hz. At 145 g fill mass, damping ratio reached 0.03 and energy dissipation efficiency reached 48%. Low fill could underperform the solid tool. | Fill state and operating condition determine the functional benefit. |
|
||||
|
||||
The second category contains 35 evidence units with designed internal structures. Examples include divided cavities, ribs, lattice cavities, resonant features and flexure guided structures,,,,,. Internal design adds a distinct design variable by changing how the powder volume is arranged within the printed structure.
|
||||
|
||||
The third category contains 15 post-filled AMPD evidence units. In this category, additive manufacturing creates the host structure, cavity, insert or module, while the particle damping medium is introduced and sealed after fabrication. Mixed retained and inserted cases are included in this category. Examples include additively manufactured toolholder and machining evidence units,, post-filled inserts or modules, and TPMS-based particle dampers,. Six related publication records outside these definitions remain as unplotted context in the evidence table,,,.
|
||||
|
||||
gives one representative comparison from each AMPD category in. The complete performance summary is provided in the evidence table.
|
||||
|
||||
The distribution of validation levels in shows where the available evidence is concentrated. Most evidence in the two direct retained-powder categories comes from specimen tests, including walls and beams,,,,. Component and application evidence is less common and appears in blades,, gears, optical holders and post-filled machining systems. Nine numerical evidence units address particle behavior, packing density control and design optimization,,,. Section therefore examines cavity placement and internal design in the 64 direct retained-powder evidence units.
|
||||
|
||||
## 4\. Direct retained-powder design variables
|
||||
|
||||
After the manufacturing and filling approach boundaries in, focuses on the direct retained-powder subset. It maps the cavity placement and cavity design classifications of 64 independent evidence units. The figure shows how retained powder volumes are positioned and shaped internally, so the following discussion can focus on design patterns instead of repeating the approach boundary.
|
||||
|
||||
Each direct retained-powder evidence unit contributes to one primary placement class and one primary cavity design class in. Detailed class definitions and precedence rules for cases with multiple applicable descriptions are provided in Supplementary File 2.
|
||||
|
||||
The placement axis describes the logic used to locate the powder volume. Mode targeted evidence units place cavities with respect to modal or operational response, including modal displacement, antinode, strain or forced response regions,,. Neutral axis evidence units use a low strain or neutral axis region as the placement reference when damping space must be balanced with stiffness or functional geometry,,. Multiple cavities describe distributed powder pockets or chamber arrays within one structure,,. Component layout covers cases where the available part geometry or functional space drives the cavity position, as in gears, instrumentation rake bodies and tooling elements,,. Cavity variation is retained as the fallback placement category when cavity position is compared together with size, number or other cavity design parameters and no single placement rule dominates,,.
|
||||
|
||||
The design axis describes the internal form of the powder containing volume. Simple cavity evidence units use closed or sealed powder volumes without designed internal structures,. Divided cavities split the powder space into chambers, pockets or partitioned regions,. Internal features add ribs, stiffening features or other obstacles inside the cavity,,. Lattice cavity evidence units combine retained powder with lattice type members or chambered lattice structures,,. Local resonator evidence units couple retained powder to a resonant substructure or absorber type design,. In this classification, multiple cavities and divided cavities are not duplicates. The first describes distributed placement of powder volumes, while the second describes subdivision of the cavity interior.
|
||||
|
||||
The plotted counts show where direct retained-powder AMPD design evidence is concentrated. Cavity variation is the largest placement category with 28 evidence units, followed by mode targeted placement with 20 evidence units. Multiple cavities and component layout each contain 6 evidence units, and neutral axis placement contains 4 evidence units. On the design axis, simple cavities and divided cavities form the largest categories with 29 and 19 evidence units, followed by internal features with 7 evidence units. Local resonators appear in 5 evidence units and lattice cavities in 4 evidence units. The most populated cells are cavity variation with simple cavities, mode targeted placement with simple cavities and mode targeted placement with divided cavities. This pattern shows that the direct retained-powder literature is weighted toward modal placement, cavity design comparisons and simple or partitioned cavity designs.
|
||||
|
||||
This classification supports a more specific design interpretation. Cavity placement can matter as much as cavity volume because retained powder must move relative to the cavity walls under the active response,,. At the same time, cavity design strategy changes both powder motion and structural response, because partitions, ribs, lattice members and resonant substructures can modify particle travel distance, contact conditions, local stiffness and coupling to a target mode,,,. Their benefit is conditional because the same feature that redirects particles can also reduce clearance, restrict powder mobility or change the load carrying geometry,,. Geometry descriptors should therefore be read together with powder state and baseline definition. Cavity ratio, cavity volume fraction, unfused powder volume percentage, particle filling ratio and packing density describe related but different quantities, and they should not be treated as interchangeable damping predictors,,,.
|
||||
|
||||
This design classification provides the context for comparing reported frequency ranges, excitation regimes and validation metrics in Section.
|
||||
|
||||
## 5\. Validation evidence and metric comparability
|
||||
|
||||
After the manufacturing and filling approach boundaries in and the direct retained-powder design variables in, the next comparison is how these designs have been tested. maps the frequency information reported for 64 direct retained-powder AMPD evidence units. It separates impact-hammer FRF, impulse or free decay, shock or transient loading, harmonic or swept-sine testing, random or broadband testing, mixed or operational testing and numerical or modeling-only work as primary evaluation methods. Detailed method definitions and assignment rules are provided in Supplementary File 2, while the primary and secondary method classifications for each evidence unit are listed in Supplementary File 1.
|
||||
|
||||
The 64 evidence units comprise 26 harmonic or swept-sine, 15 impact-hammer FRF, 9 numerical or modeling-only, 7 mixed or operational, 5 impulse or free-decay and 2 shock or transient evaluations. None uses random or broadband testing as its primary method, although broadband input appears as a secondary method in some mixed or operational evidence units.
|
||||
|
||||

|
||||
|
||||
Download: Download high-res image (1MB)
|
||||
|
||||
Of the 64 evidence units, 18 report continuous ranges, 6 discrete point sets, 28 modal-frequency sets and 8 local bands. Four lack a verifiable numeric frequency or mode and remain listed as no numeric beside their source labels. Filled circles mark continuous-range endpoints and discrete points, filled diamonds mark modal frequencies and filled squares mark local-band endpoints. Each source mark uses the color assigned to its validation level. Ranges beginning at 0 Hz are shown from the 1-Hz limit of the logarithmic axis.
|
||||
|
||||
The frequency information in becomes meaningful when the input method and response metric are read together. Impact-hammer FRF tests identify modes and describe damping or response amplitude around resonance. Impulse or free-decay tests obtain modal damping from the response after release or impulse. Shock or transient tests quantify the decay after a short input through measures such as quality factor and damping ratio. Harmonic or swept-sine tests resolve changes in resonance, loss metrics and dissipated energy across frequency and amplitude.
|
||||
|
||||
Mixed or operational tests connect the vibration response to functional measures such as stress, fatigue or transmissibility,. Numerical evidence units examine particle motion and particle–wall interactions, with experimental calibration determining their design relevance. The absence of random or broadband excitation as a primary method leaves service representative broadband loading as a validation gap.
|
||||
|
||||
These metrics describe different parts of the structural response. Interpreting a lower FRF peak requires checking mass, stiffness and resonance shift together with damping. Comparison across evidence units therefore requires the input type and amplitude, frequency or mode, response location, metric definition and baseline to be reported together. A useful next step is to test several modes with more than one input method on the same specimens and baseline. This would connect modal damping, FRF amplitude, energy loss and functional response under controlled conditions.
|
||||
|
||||
Excitation amplitude is a design variable in AMPD because the particle motion changes as the input increases. At low input, the powder can move with the cavity walls and dissipate little energy. As relative motion develops, sliding and collisions increase dissipation. Further increases can produce saturation, softening, hysteresis or jump behavior,,. Characterizing this working range requires damping measurements at several specified amplitudes. Frequency sweeps should therefore be repeated at controlled amplitudes and in both sweep directions, with response amplitude and activation or saturation thresholds reported. The resulting frequency and amplitude maps would show whether a design remains effective across its intended load range.
|
||||
|
||||
PBF-LB/M feedstock powder introduces a second design dimension. Micrometer scale powder has a greater relative influence of attractive and surface forces than the millimeter scale particles used in many classical dampers,. Its mobility also depends on material, particle size distribution, surface condition, packing density and compaction,,,. The same nominal cavity geometry can therefore show different damping when the powder material or state changes. Controlled comparisons across materials should hold cavity geometry, structural baseline and excitation constant while varying powder material, size distribution, packing and compaction. maps testing conditions and validation levels, while the evidence table records the particle descriptors and powder state needed for this comparison.
|
||||
|
||||

|
||||
|
||||
Download: Download high-res image (349KB)
|
||||
|
||||
Table 3. Baseline comparisons for three recurring research purposes in the reviewed AMPD literature.
|
||||
|
||||
| Purpose | Suitable comparison | Supported interpretation |
|
||||
| --- | --- | --- |
|
||||
| Mechanism attribution | Compare retained-powder specimens with corresponding empty cavity, solid or altered powder state specimens. Keep the boundary condition and excitation consistent, and report changes in mass, stiffness, natural frequency and mode shape,,. | Whether the measured response is consistent with particle mobility and dissipation at the tested mode, amplitude and powder state. |
|
||||
| Design trade-off under stated constraints | Compare feasible designs under the same functional requirements and report the relevant mass, stiffness, strength, manufacturing and frequency constraints,,. | The vibration benefit obtained within the tested design constraints, including damping and changes in resonance. |
|
||||
| Functional performance and durability | Compare the AMPD design with a functional reference under the same mounting, loading and environmental conditions, and include repeated specimens or cyclic states where available,,. | The functional benefit and its repeatability or stability over the tested conditions and duration. |
|
||||
|
||||
Taken together, the 64 evidence units comprise 41 specimen evidence units, 9 numerical evidence units, 7 component evidence units and 7 application evidence units. The distribution is concentrated at specimen level, while component and application evidence each account for 7 evidence units.
|
||||
|
||||
The testing and frequency evidence in must be interpreted together with the reported response metric and baseline because a reduction in vibration response can arise from particle dissipation, changes in mass or stiffness, a shift in resonance, or a combination of these effects. The baseline must therefore be chosen according to the question being tested. summarizes the baseline implications derived from analysis through three recurring research purposes: identifying the contribution of particle mobility, evaluating vibration performance under stated design constraints, and testing functional performance and durability. For each purpose, the table links a suitable comparison with the conclusion that the available evidence can support. The reporting information needed for these comparisons is examined in Section.
|
||||
|
||||
## 6\. Reporting completeness and comparability needs
|
||||
|
||||
Comparisons across AMPD evidence units become difficult when important experimental information is incomplete or reported in different ways. therefore examines the reporting completeness of 64 direct retained-powder AMPD evidence units. The fields cover the information needed to describe their designs, tests and validation results, with detailed definitions in Supplementary File 2 and the corresponding evidence in Supplementary File 1. Each field is classified as Reported, Partly reported, Not reported or Not applicable. The applicable denominator includes the first three statuses, while Not applicable is shown separately.
|
||||
|
||||
shows that basic descriptions of AMPD design and testing are available in most evidence units. AM process and material and boundary condition each reach the Reported threshold in 60 evidence units. Cavity metric reaches it in 59 evidence units, geometry in 58 evidence units and excitation level in 50 evidence units. The largest gaps are concentrated in particle fill ratio, packing density or powder state, repeatability or uncertainty, and lifecycle or degradation. The following paragraphs discuss why these four areas remain incomplete and how they affect comparison and reproducibility.
|
||||
|
||||
Particle fill ratio and packing density describe two linked controls of retained powder motion. Fill ratio sets the powder amount relative to cavity volume, while packing density and powder state determine how that material is arranged and constrained. In, particle fill ratio is Reported in 5 evidence units, Partly reported in 56 and Not reported in 3. Packing density or powder state is Reported in 38 evidence units, Partly reported in 25 and Not reported in 1. The distinction is mechanically important. Fill ratio governs the overall free space available for particle motion. Packing density, compaction and cohesion govern the internal contact network, frictional sliding and the excitation threshold required to mobilize the powder,,,. Identical cavity geometry and nominal fill ratio can therefore produce different damping after processing or repeated loading changes the powder state. Future AMPD work should report a clearly defined volume or mass basis together with the measured powder state before and after testing, allowing particle activation and energy dissipation to be linked to a reproducible internal condition.
|
||||
|
||||
Repeatability or uncertainty is Reported in 33 evidence units, Partly reported in 28, Not reported in 1 and Not applicable in 2. The large Partly reported group mainly contains specimen or repeat counts without a measure of variation. Repeated measurements on one specimen characterize variation in the test and response. Measurements across specimens and builds capture variation introduced by manufacturing and the retained powder state. Local packing, compaction and powder redistribution can change the damping response under nominally identical geometry and loading,,. Repeated runs can provide a precise mean for one specimen. Reproducibility across specimens and builds requires separate replication. Future AMPD work should distinguish repeated runs, specimens and builds and report dispersion or uncertainty at each level together with the corresponding powder state.
|
||||
|
||||
Table 4. Proposed minimum AMPD reporting checklist for future work.
|
||||
|
||||
| Reporting item | Minimum information | Risk if omitted |
|
||||
| --- | --- | --- |
|
||||
| Approach identity | Identify retained build powder, post-filled particles or another related approach. Report sealing and powder removal where relevant. | Routes may be compared although their damping media are created and controlled differently. |
|
||||
| Cavity and structure | Report cavity placement, wall thickness, internal design, mass change and geometry relevant to stiffness. | Geometry or stiffness effects may be attributed to powder damping. |
|
||||
| Powder or particle state | Report particle material and size, retained powder condition, packing density or fill measure, and heat treatment or compaction history. | Fill ratio, packing density and powder state may be treated as equivalent. |
|
||||
| Test condition | Report input type and amplitude, frequency range or test points, mounting and signal chain. | Results may be compared across different particle activation conditions. |
|
||||
| Baseline and metric | Define the reference and report AMPD and reference mass, powder or particle mass where available, natural-frequency shift, stiffness change or a justified proxy, and the response or functional metric. | Mass, stiffness and detuning may confound interpretation of the damping benefit. |
|
||||
| Repeatability and service | Report specimen and repeat counts, uncertainty, repeated excitation effects, degradation and powder state after testing. | Initial performance may be interpreted as repeatable or durable. |
|
||||
|
||||
Lifecycle or degradation is Reported in 25 evidence units, Partly reported in 2, Not reported in 34 and Not applicable in 3, making it the largest Not reported group in. Most evidence units therefore characterize AMPD performance in its initial state, leaving stability under mechanical and thermal history unresolved. Retained powder damping is state dependent. Repeated resonance passes and high strain dwell can compact, redistribute or locally fuse the powder,,. Heat treatment can form sintered contacts and reduce particle mobility, while later excitation can fragment some contacts and change the response again. Degradation can therefore involve transitions between loose, compacted, trapped and sintered powder states, with corresponding changes in activation and energy dissipation,. Application validation should track damping against load cycles, amplitude and thermal history and document the powder state before and after testing. This would show whether the damping response remains stable, changes gradually or undergoes an irreversible loss.
|
||||
|
||||
These reporting gaps motivate the AMPD reporting checklist in. The checklist combines the weak reporting fields in with the manufacturing and filling approach, cavity design and validation variables discussed above. It lists the minimum information that future AMPD work should report before results are compared across manufacturing and filling approaches, cavity designs, test conditions and baselines.
|
||||
|
||||
## 7\. Design implications
|
||||
|
||||
This section discusses the design implications of the reviewed evidence and priorities for future AMPD research.
|
||||
|
||||
The first design implication from the manufacturing and filling categories in and is that the AMPD route should be selected according to the design variable that must remain controllable in the intended application. Direct retained-powder designs without designed internal structures provide control through cavity placement and geometry, designed internal structures add coupled control through internal design, and post-filled designs provide independent control of particle morphology and fill ratio after fabrication,,,,,,,. This route decision should precede detailed cavity optimization.
|
||||
|
||||
The second design implication from Section and is that cavity placement and cavity design form one optimization problem for direct retained-powder AMPDs. The target mode, load path and functional response define where retained powder motion is useful, while structural and manufacturing constraints define which internal design is feasible,,,,,,. The selected combination should then be judged using application measures such as cutting stability, forced response or optical stability,,.
|
||||
|
||||
The third design implication from the validation levels in Section and is that each level should answer a different question through its test method, frequency evidence and reported metric. Numerical evidence units can identify candidate modes and response bands and screen particle activation trends,,. At specimen level, harmonic or swept-sine tests and impact-hammer FRFs should map activation, amplitude dependence and modal damping across several amplitudes and modes,,. Component tests should retain the relevant modal or local frequency information while adding mounting, stiffness, resonance shifts and modal coupling,,. Across both routes, application tests should reproduce operational inputs and connect frequency response to functional measures such as forced response, fatigue, cutting stability or optical stability,,,,,,. Repeatability and response stability under repeated excitation or service exposure then become part of qualification,,,,. Validation should therefore progress from mechanism and activation maps, through integrated component response, to functional performance and stability over time.
|
||||
|
||||
The fourth design implication from the reporting completeness analysis in Section and is that a transferable AMPD design must be defined across its full lifecycle. Its initial particle or powder condition, variation across specimens and builds, and changes during repeated use form one continuous design record that links the manufactured state to reproducibility and stability under operating conditions,,,,,.
|
||||
|
||||
In summary, the preceding design implications point to four research priorities. First, shared reference geometries and open data for each evidence unit should connect damping metrics to matched baselines. Second, nondestructive indicators of retained powder state should be calibrated against mobility and dynamic response. Third, lifecycle tests should quantify compaction, sintering, recovery, leakage and fatigue interactions. Fourth, multiscale models should propagate manufacturing, material-batch, boundary-condition and internal-state variability into response uncertainty. Together, these priorities connect AMPD design choices with the modeling, validation and reporting needed to compare performance across machines, materials, heat treatments and service conditions.
|
||||
|
||||
## 8\. Conclusions
|
||||
|
||||
This review connects the classification of AMPD manufacturing and filling approaches with cavity design, testing methods, reported performance and the evidence still needed for reliable comparison and qualification. The main conclusions follow this sequence from route selection and design to validation, reporting completeness and future development:
|
||||
|
||||
- •
|
||||
The evidence table contains 108 publication records and yields 79 independent AMPD evidence units, comprising 64 direct retained-powder evidence units and 15 post-filled evidence units. The detailed design, frequency and reporting analyses use the 64 direct evidence units, while the 15 post-filled evidence units remain in the route and performance comparisons. Six related publication records remain in the evidence table as context. Because the two AMPD routes create and control the damping medium differently, the manufacturing and filling approach is the starting point for design interpretation.
|
||||
- •
|
||||
The review also establishes a common framework for comparing direct retained-powder AMPD evidence units across cavity placement, internal design, validation level, testing method, frequency evidence and reported performance. This framework places each result within the design and test conditions under which it was obtained. The synthesis retains the original response metric and comparison baseline, making differences among evidence units visible and supporting more consistent interpretation.
|
||||
- •
|
||||
The largest reporting gaps concern particle fill ratio, packing density and particle or powder state, repeatability or uncertainty, and lifecycle or degradation. Reporting these fields links the initial internal condition to variation across specimens and builds and to changes during repeated use or service. This evidence supports evaluation of reproducibility and stability under the intended operating conditions.
|
||||
|
||||
This review therefore provides a unified basis for future AMPD research by connecting route selection, performance interpretation and the evidence required for reproducible and transferable design across materials, manufacturing processes and operating conditions.
|
||||
|
||||
## CRediT authorship contribution statement
|
||||
|
||||
**Weijia Yu:** Writing – review & editing, Writing – original draft, Visualization, Software, Methodology, Investigation, Formal analysis, Data curation, Conceptualization. **Marcus Oel:** Writing – review & editing. **Jens Niedermeyer:** Writing – review & editing. **Lennart Mesecke:** Writing – review & editing. **Ina Meyer:** Writing – review & editing. **Roland Lachmayer:** Writing – review & editing, Supervision.
|
||||
|
||||
## Declaration of generative AI and AI-assisted technologies in the manuscript preparation process
|
||||
|
||||
During the preparation of this work the authors used OpenAI Codex and ChatGPT to support language polishing, editorial revision, and preparation checks for the manuscript, figures and supplementary materials. The tools were not used to independently generate scientific content, evidence classification decisions, data, results or interpretations. After using these tools, the authors reviewed, verified and edited the content as needed and take full responsibility for the content of the published article.
|
||||
|
||||
## Funding
|
||||
|
||||
This research did not receive any specific grant from funding agencies in the public, commercial, or not-for-profit sectors.
|
||||
|
||||
[^2]: Additive manufacturing changes how this mechanism can be integrated. Internal cavities, local architecture and particle filled volumes can be designed together with the structural load path, so particle damping can be integrated within the printed component instead of added as a separate damping element,,. In additively manufactured particle damping structures (AMPDs), the damping medium may be unfused build powder retained during powder bed fusion of metals using a laser beam (PBF-LB/M) or particles introduced after fabrication. summarizes these manufacturing and filling approaches and their integration into AMPD structures. This integration has been studied, for example, for blade like parts,,, machining tools,, vibration sensitive optical holders and topology based lightweight design concepts.
|
||||
|
||||

|
||||
|
||||
Download: Download high-res image (277KB)
|
||||
|
||||
[^3]: | Category and source | Comparison | Test and reported result | Main insight |
|
||||
| --- | --- | --- | --- |
|
||||
| Direct retained-powder, simple cavity. Westbeld et al.. | AlSi10Mg specimens with mobile or sintered powder were compared with solid references. The evidence unit included 44 cavity specimens, 18 solid specimens and four measurements per specimen. | Periodic chirp at 800 mm/s <sup>2</sup> over 50–8000 Hz. Global sintering produced no significant particle damping. Mobile powder produced a maximum relative loss factor increase of 1425%. | Powder mobility determines whether damping is activated. |
|
||||
| Direct retained-powder, internal pockets. Scott-Emuakpor et al.. | Four IN718 AMPD blades were compared with four fully fused blades. | A 0–6000 Hz sweep was followed by modal and fatigue tests. Mean quality factor decreased by about 45% and 60% at two modes, while fatigue resistance increased. | Modal response and durability should be evaluated together. |
|
||||
| Post-filled TPMS tool. Han et al.. | Four tool variants were compared with a solid tool under 16 cutting condition groups. Repeat count was not reported. | Dry turning with modes near 1299, 1303 and 5119 Hz. At 145 g fill mass, damping ratio reached 0.03 and energy dissipation efficiency reached 48%. Low fill could underperform the solid tool. | Fill state and operating condition determine the functional benefit. |
|
||||
|
||||
[^4]: PBF-LB/M feedstock powder introduces a second design dimension. Micrometer scale powder has a greater relative influence of attractive and surface forces than the millimeter scale particles used in many classical dampers,. Its mobility also depends on material, particle size distribution, surface condition, packing density and compaction,,,. The same nominal cavity geometry can therefore show different damping when the powder material or state changes. Controlled comparisons across materials should hold cavity geometry, structural baseline and excitation constant while varying powder material, size distribution, packing and compaction. maps testing conditions and validation levels, while the evidence table records the particle descriptors and powder state needed for this comparison.
|
||||
|
||||

|
||||
|
||||
Download: Download high-res image (349KB)
|
||||
|
||||
Table 3. Baseline comparisons for three recurring research purposes in the reviewed AMPD literature.
|
||||
|
||||
| Purpose | Suitable comparison | Supported interpretation |
|
||||
| --- | --- | --- |
|
||||
| Mechanism attribution | Compare retained-powder specimens with corresponding empty cavity, solid or altered powder state specimens. Keep the boundary condition and excitation consistent, and report changes in mass, stiffness, natural frequency and mode shape,,. | Whether the measured response is consistent with particle mobility and dissipation at the tested mode, amplitude and powder state. |
|
||||
| Design trade-off under stated constraints | Compare feasible designs under the same functional requirements and report the relevant mass, stiffness, strength, manufacturing and frequency constraints,,. | The vibration benefit obtained within the tested design constraints, including damping and changes in resonance. |
|
||||
| Functional performance and durability | Compare the AMPD design with a functional reference under the same mounting, loading and environmental conditions, and include repeated specimens or cyclic states where available,,. | The functional benefit and its repeatability or stability over the tested conditions and duration. |
|
||||
|
||||
[^5]: | Purpose | Suitable comparison | Supported interpretation |
|
||||
| --- | --- | --- |
|
||||
| Mechanism attribution | Compare retained-powder specimens with corresponding empty cavity, solid or altered powder state specimens. Keep the boundary condition and excitation consistent, and report changes in mass, stiffness, natural frequency and mode shape,,. | Whether the measured response is consistent with particle mobility and dissipation at the tested mode, amplitude and powder state. |
|
||||
| Design trade-off under stated constraints | Compare feasible designs under the same functional requirements and report the relevant mass, stiffness, strength, manufacturing and frequency constraints,,. | The vibration benefit obtained within the tested design constraints, including damping and changes in resonance. |
|
||||
| Functional performance and durability | Compare the AMPD design with a functional reference under the same mounting, loading and environmental conditions, and include repeated specimens or cyclic states where available,,. | The functional benefit and its repeatability or stability over the tested conditions and duration. |
|
||||
@@ -0,0 +1,386 @@
|
||||
|
||||
|
||||
## Introduction
|
||||
|
||||
Welcome to "Design for Additive Manufacturing," an extensive guide from [iamrapid.com](https://iamrapid.com/), your trusted 3D printing service provider based in Bangalore, India. This guide will delve into the intricacies of designing specifically for additive manufacturing (AM). This transformative approach allows for creating complex geometries, optimized structures, and customized solutions like never before.
|
||||
|
||||
Additive manufacturing, also known as 3D printing, is reshaping the way products are conceptualized, designed, and manufactured. Its potential is not limited to rapid prototyping, but extends to full-scale production, making it a game-changer in industries such as aerospace, healthcare, automotive, and consumer goods. To fully exploit the capabilities of this technology, it's essential to grasp the principles and best practices for design that can harness the unique benefits of AM.
|
||||
|
||||
Embark on a journey with us as we delve into the crucial considerations, techniques, and tips for designing parts that are not just manufacturable, but also optimized for performance, cost, and innovation. Whether you're a seasoned engineer, a product designer, or an eager enthusiast, this guide is your key to mastering the evolving landscape of additive manufacturing.
|
||||
|
||||
Let's unlock the potential of your designs and bring your ideas to life with the power of 3D printing!
|
||||
|
||||
## What is Additive Manufacturing?
|
||||
|
||||
Additive manufacturing, commonly known as 3D printing, creates objects by adding material layer by layer directly from digital models. Unlike traditional subtractive manufacturing methods that remove material to shape a part, additive manufacturing builds parts with precision and minimal waste. This innovative approach allows for producing complex geometries and customized solutions that were previously unattainable. To understand this further,[click here.](https://iamrapid.com/knowledge-hub/additive-manufacturing-workflow/)
|
||||
|
||||
### Importance of Design in Additive Manufacturing
|
||||
|
||||
Design is the cornerstone of successful additive manufacturing (AM), dictating not only the feasibility and functionality of the final product but also its efficiency, cost, and environmental impact. Understanding and leveraging the principles of AM-specific design can significantly enhance the advantages offered by this transformative technology. Below, we explore the various aspects that underscore the critical importance of design in additive manufacturing.
|
||||
|
||||
- ##### Optimizing for Complex Geometries:
|
||||
AM excels in creating complex geometries that traditional manufacturing methods cannot quickly achieve. **Engineers and Designers can develop intricate structures by designing with AM in mind**, such as lattice frameworks, organic shapes, and internal channels. These designs improve product performance by enhancing strength-to-weight ratios and integrating multiple functions into a single part.
|
||||
|
||||
- ##### Enhancing Material Efficiency and Sustainability:
|
||||
Additive manufacturing builds objects layer by layer, allowing for precise material placement and minimal waste. This contrasts sharply with subtractive manufacturing, which often generates significant material waste.**Designing parts specifically for AM promotes efficient material use**, contributing to sustainability and reducing the overall environmental footprint of manufacturing processes.
|
||||
|
||||
- ##### Facilitating Customization and Personalization:
|
||||
**AM's design flexibility enables the production of customized and personalized products** without extensive retooling. This capability is particularly valuable in healthcare, where tailored implants and prosthetics can significantly improve patient outcomes. This flexibility also benefits consumer goods, allowing for personalized designs catering to individual preferences.
|
||||
|
||||
- ##### Reducing Time to Market:
|
||||
**Designing for AM can accelerate the product development cycle.** Rapid prototyping allows designers to create quickly and test product iterations, refining designs based on real-time feedback. This process reduces development time and speeds up the transition from concept to market-ready product, giving companies a competitive edge in responding to market demands.
|
||||
|
||||
- ##### Achieving Cost-Effectiveness:
|
||||
While the initial setup for AM can be expensive, the long-term benefits often outweigh these costs. **Optimizing designs for AM can reduce the number of parts, streamline assembly processes, and minimize inventory costs.** Additionally, on-demand production eliminates the need for extensive inventories, leading to further cost savings in storage and logistics.
|
||||
|
||||
- ##### Driving Enhanced Performance and Innovation:
|
||||
**Designing for AM encourages innovation by allowing engineers/designers to explore new structures and materials.** This can lead to high-performance components with superior mechanical properties, thermal resistance, or other desired characteristics. The ability to experiment and iterate on designs fosters continuous improvement and technological advancement.
|
||||
|
||||
- ##### Overcoming Traditional Manufacturing Constraints:
|
||||
Traditional manufacturing methods impose various design constraints due to tooling, machining, and fabrication limitations. **AM frees designers from these constraints, enabling greater creative freedom.** This allows for exploring unconventional designs that offer superior performance, aesthetics, and functionality, leading to more innovative products.
|
||||
|
||||
- ##### Integrating Multifunctional Components:
|
||||
**AM allows for creating multifunctional components that combine several parts into one, reducing the need for assembly and improving overall reliability.** Manufacturers can produce more compact and efficient products by designing parts with integrated functions. This integration is particularly advantageous in industries like aerospace and automotive, where space and weight savings are critical.
|
||||
|
||||
- ##### Supporting Distributed Manufacturing:
|
||||
**Designing for AM supports distributed manufacturing, where production can be decentralized and localized.** This approach reduces transportation costs, lowers carbon footprints, and enables on-demand production closer to the end user. Distributed manufacturing enhances supply chain resilience and responsiveness, particularly during disruption.
|
||||
|
||||
- ##### Promoting Continuous Improvement and Iteration:
|
||||
**The iterative nature of AM aligns well with continuous improvement methodologies.** Designers can rapidly prototype, test, and refine products based on real-world feedback, leading to ongoing enhancements. This iterative process fosters innovation and quality improvement, ensuring products remain competitive and meet evolving customer needs.
|
||||
|
||||
By understanding and applying AM-specific design principles, companies can fully harness the potential of additive manufacturing, driving advancements across various industries and shaping the future of production. As you continue to explore and implement AM, thoughtful design will be your key to unlocking its vast possibilities.
|
||||
|
||||
### Types of Additive Manufacturing Processes in Brief
|
||||
|
||||
3D printing technologies, also commonly known as additive manufacturing (Are 3D Printing and Additive Manufacturing the same? [Click here to know](https://iamrapid.com/knowledge-hub/additive-manufacturing-workflow/)), encompass a variety of processes that create objects layer by layer from digital models. Here is a brief overview of the most common 3D printing technologies:
|
||||
|
||||
1. ##### Fused Deposition Modeling (FDM)
|
||||
|
||||
FDM, also known as Fused Filament Fabrication (FFF), is one of the most widely used 3D printing technologies. It works by extruding thermoplastic filament through a heated nozzle, layer by layer, to build up the desired object. FDM is popular for its affordability, ease of use, and versatility, making it ideal for prototyping and hobbyist projects. [Click here](https://iamrapid.com/knowledge-hub/FDM-3D-printing/) to learn more in-depth about FDM.
|
||||
2. ##### Stereolithography (SLA)
|
||||
|
||||
SLA uses a laser to cure liquid resin into hardened plastic in a process called photopolymerization. This technology is known for producing high-resolution, highly detailed parts with smooth surface finishes. SLA is widely used in industries requiring precision, such as jewelry, dental, and medical device manufacturing. [Click here](https://iamrapid.com/knowledge-hub/SLA-3D-printing/) to learn more about SLA.
|
||||
3. ##### Selective Laser Sintering (SLS)
|
||||
|
||||
SLS utilizes a high-powered laser to fuse small particles of polymer powder into a solid structure. Each layer of powder is spread across the build platform and selectively sintered by the laser. SLS is valued for its ability to produce durable, complex geometries without supporting structures, making it suitable for functional prototypes and end-use parts. [Click here](https://iamrapid.com/knowledge-hub/SLS-3D-printing/) to learn more about SLS.
|
||||
4. ##### Digital Light Processing (DLP)
|
||||
|
||||
Similar to SLA, DLP uses light to cure resin, but it differs in that it uses a digital projector screen to flash each layer simultaneously rather than tracing it with a laser. This results in faster print times compared to SLA. DLP is known for high speed and accuracy, making it ideal for detailed models and small parts. [Click here](https://iamrapid.com/3d-printing-services/sla/) to learn more in-depth about DLP.
|
||||
5. ##### Binder Jetting
|
||||
|
||||
Binder jetting involves laying down a layer of powder and then selectively depositing a liquid binder to glue the particles together. This process is repeated layer by layer to build the object. Binder jetting can use various materials, including metals, ceramics, and sand, and is often used for full-color prototypes and metal casting molds. [Click here](https://iamrapid.com/3d-printing-services/) to learn more about Binder Jetting.
|
||||
6. ##### Direct Metal Laser Sintering (DMLS) / Selective Laser Melting (SLM)
|
||||
|
||||
DMLS and SLM are similar technologies that create metal parts by sintering or melting metal powder with a laser. DMLS typically operates at lower temperatures and doesn't fully melt the powder. In contrast, SLM fully melts the powder to form solid metal parts. Both are used for producing robust and complex metal components in the aerospace, automotive, and medical industries. [Click here](https://iamrapid.com/3d-printing-services/dmls/) to learn more about DMLS/SLM.
|
||||
7. ##### Multi Jet Fusion (MJF)
|
||||
Developed by HP, MJF uses an inkjet array to selectively apply fusing agents to a bed of nylon powder, which is then fused by heating elements. This technology allows for the rapid production of highly detailed and durable parts and is particularly effective for functional prototypes and low-volume production runs. [Click here](https://iamrapid.com/3d-printing-services/mjf/) to learn more about MJF.
|
||||
|
||||
### Materials Used in Additive Manufacturing
|
||||
|
||||
In DfAM, having prior knowledge about the materials, their properties, and their applications can significantly enhance the design process. This understanding allows for creating more optimal, manufacturable designs, ensuring that the chosen material aligns with the final product's intended use and performance requirements. By integrating material knowledge early in the design phase, designers can better leverage the full potential of additive manufacturing technologies.
|
||||
|
||||
Below is a brief overview of the primary material categories used in additive manufacturing, highlighting their overall use case scenarios.
|
||||
|
||||
##### 1\. Plastics
|
||||
|
||||
- Thermoplastics: Commonly used in Fused Deposition Modeling (FDM), thermoplastics like [ABS](https://iamrapid.com/materials/ABS/), [PLA](https://iamrapid.com/materials/PLA/), and [PETG](https://iamrapid.com/materials/PETG/) are valued for their ease of use, affordability, and versatility. These materials are ideal for prototyping, hobbyist projects, and functional parts.
|
||||
- High-Performance Plastics:Materials like Nylon, Polycarbonate (PC), and PEEK are used for more demanding applications due to their enhanced mechanical properties, heat resistance, and chemical stability. These are often used in industrial and engineering applications.
|
||||
|
||||
##### 2\. Metals
|
||||
|
||||
- Stainless Steel: Widely used in Direct Metal Laser Sintering (DMLS) and Selective Laser Melting (SLM), stainless steel offers excellent strength, durability, and corrosion resistance. It is used in the aerospace, automotive, and medical industries.
|
||||
- Titanium: Known for its high strength-to-weight ratio and biocompatibility, titanium is used in medical implants, aerospace components, and high-performance engineering parts.
|
||||
- Aluminum: Lightweight and strong, aluminum is used in the AM to produce lightweight parts with good mechanical properties, making it ideal for automotive and aerospace applications.
|
||||
- Other Metals: Cobalt-chrome, Inconel, and copper alloys are used in specialized applications requiring high temperature resistance, corrosion resistance, or electrical conductivity.
|
||||
|
||||
##### 3\. Resins
|
||||
|
||||
- Standard Resins: Used in Stereolithography (SLA) and Digital Light Processing (DLP), standard resins are ideal for creating high-detail prototypes and models. They offer smooth surface finishes and delicate features.
|
||||
- Engineering Resins: These resins, including rigid, flexible, and high-temperature variants, enhance mechanical properties for functional prototypes and end-use parts. Applications include dental, medical, and industrial components.
|
||||
- Biocompatible Resins: Specifically designed for medical and dental applications, these resins meet strict regulatory standards for use in products that come into contact with the human body.
|
||||
|
||||
##### 4\. Composites
|
||||
|
||||
- Fiber-Reinforced Composites: Combining polymers with reinforcing fibers like carbon fiber or fiberglass. These materials offer superior strength and stiffness while remaining lightweight. They are used in aerospace, automotive, and sports equipment.
|
||||
- Metal Matrix Composites (MMCs): TThese composites combine metal powders with ceramic or carbon fibers, enhancing mechanical properties and wear resistance. They are used in high-performance applications where traditional metals may not suffice.
|
||||
- Ceramic Composites: These materials combine ceramic powders with polymers or other binders to create parts with high heat resistance and mechanical strength. Applications include aerospace components and high-temperature industrial parts.
|
||||
|
||||
### Design for Manufacturability (DFM)
|
||||
|
||||
|
||||
|
||||
Design for Manufacturability (DFM) involves optimizing a product design to ensure it can be manufactured quickly and efficiently. In the context of AM, DFM principles help maximize the advantages of additive processes while minimizing potential challenges.
|
||||
|
||||
1. Part Orientation: The orientation of a part during printing affects its strength, surface finish, and print time. Optimal part orientation can improve mechanical properties, reduce the need for supports, and enhance surface quality. Designers should consider the orientation to balance these factors effectively.
|
||||
2. Layer Thickness: The layer thickness in AM influences the resolution, surface finish, and build time. Thinner layers produce finer details and smoother surfaces but increase print time. Designers must choose an appropriate layer thickness based on the required detail and efficiency.
|
||||
3. Support Structures: While AM can create overhangs and intricate features, these often require support structures. Minimizing the need for supports through strategic part orientation and design can reduce post-processing efforts, material waste, and overall print time.
|
||||
4. Surface Finish: The surface finish of AM parts can vary depending on the process and material used. Designers should account for the required surface finish in their designs, considering post-processing steps like sanding, polishing, or coating to achieve the desired result.
|
||||
5. Tolerances and Accuracy: AM processes can produce parts with varying degrees of precision. Designers must understand the specific tolerances of the chosen AM technology to ensure the proper fit and function of assembled components. This involves designing parts with adequate tolerances for their intended applications.
|
||||
6. Post-Processing Requirements: Post-processing can include removing supports, surface finishing, and other treatments to achieve the final part specifications. Designing parts to minimize post-processing can save time and costs, making manufacturing more efficient.
|
||||
|
||||
### Design for Assembly (DFA)
|
||||
|
||||
|
||||
|
||||
Design for Assembly (DFA) focuses on simplifying the assembly process of a product. With AM, many traditional assembly constraints can be bypassed, allowing for more integrated and streamlined designs.
|
||||
|
||||
1. Part Consolidation: The orientation of a part during printing affects its strength, surface finish, and print time. Optimal part orientation can improve mechanical properties, reduce the need for supports, and enhance surface quality. Designers should consider the orientation to balance these factors effectively.
|
||||
2. Snap-Fit and Interlocking Features: The layer thickness in AM influences the resolution, surface finish, and build time. Thinner layers produce finer details and smoother surfaces but increase print time. Designers must choose an appropriate layer thickness based on the required detail and efficiency.
|
||||
3. Modular Design: While AM can create overhangs and intricate features, these often require support structures. Minimizing the need for supports through strategic part orientation and design can reduce post-processing efforts, material waste, and overall print time.
|
||||
4. Ease of Handling: The surface finish of AM parts can vary depending on the process and material used. Designers should account for the required surface finish in their designs, considering post-processing steps like sanding, polishing, or coating to achieve the desired result.
|
||||
|
||||
### Design for Functionality
|
||||
|
||||
|
||||
|
||||
Design for Functionality ensures that the product meets its intended purpose and performs reliably under the specified conditions. AM allows designers to incorporate unique functional features directly into the parts.
|
||||
|
||||
1. Customization and Personalization: AM excels at producing customized and personalized parts without additional cost. Designers can create tailored solutions for individual users or specific applications, such as medical implants, consumer products, and bespoke components.
|
||||
2. Integration of Features: Functional features such as hinges, channels for fluid or airflow, and embedded electronics can be directly integrated into the design. This reduces the need for separate components and enhances the product's overall Functionality.
|
||||
3. Material Selection: The choice of material impacts the final product's Functionality. As discussed earlier, Designers must select materials with the necessary mechanical properties, durability, and environmental resistance for the intended application. AM allows for using a wide range of materials, from plastics and metals to composites and ceramics.
|
||||
4. Performance Optimization: By leveraging AM's capabilities, designers can optimize parts for specific performance criteria, such as weight reduction, improved strength, thermal management, and vibration damping. This often involves advanced simulation and testing to refine the design.
|
||||
|
||||
### Design for Cost Efficiency
|
||||
|
||||
|
||||
|
||||
Design for Cost Efficiency involves creating designs that minimize production costs while maintaining quality and performance. AM offers several innovative design strategies for achieving cost efficiency.
|
||||
|
||||
1. Material Efficiency: Designing parts to use material efficiently can significantly reduce costs. This includes minimizing waste through optimized geometries and internal structures and selecting cost-effective materials that meet performance requirements.
|
||||
2. Production Time: Reducing print time is crucial for cost efficiency. Designers can achieve this by optimizing part orientation, reducing the need for supports, and simplifying geometries where possible. Faster production times lead to lower operational costs and higher throughput.
|
||||
3. Post-Processing Minimization: Post-processing can be a significant cost driver in AM. Designing parts that require minimal post-processing, such as support removal, surface finishing, and assembly, can lower overall production costs and accelerate time-to-market.
|
||||
4. Batch Production and Scaling: While AM is often used for low-volume and customized production, it can also be cost-effective for small to medium quantities batch production. Designing parts for efficient batch processing, including nested arrangements and multi-part builds, can maximize the efficiency of the AM process.
|
||||
|
||||
Understanding and applying these design principles is essential for fully leveraging additive manufacturing's capabilities. These principles help navigate AM's unique opportunities and challenges, ensuring designs are practical, feasible, and economically viable. Staying informed and adaptive in design strategies is critical to achieving sustained success and innovation in this evolving field.
|
||||
|
||||
In addition to the principles mentioned, countless other highly design-specific optimizations exist. These optimizations often rely on the creativity and logical reasoning of the designer. Whether it's finding innovative ways to reduce material usage, improving structural integrity, or enhancing aesthetic appeal, the possibilities for optimization in additive manufacturing are virtually limitless. Designers play a pivotal role in pushing the boundaries of what's possible, continually exploring new techniques, and moving the technology forward. As AM continues to evolve, the collaboration between advanced software tools and human ingenuity will drive unprecedented design and manufacturing innovation levels.
|
||||
|
||||
## CAD Software for Additive Manufacturing
|
||||
|
||||
|
||||
|
||||
Additive manufacturing (AM) heavily relies on Computer-Aided Design (CAD) software to translate innovative ideas into tangible prototypes or end-use products. The CAD software you choose depends on what you are designing. For example, Figurines require freedom to design organic curves and surfaces; another example is Spare parts, which require precision modeling with low tolerances. So, choosing the right software that satisfies your design needs is essential, as it impacts the efficiency, precision, and complexity achievable in your additive manufacturing endeavors. Let's explore some popular CAD software tools.
|
||||
|
||||
### Popular CAD Software Tools
|
||||
|
||||
- Autodesk Fusion 360: Known for its comprehensive cloud-based CAD/CAM/CAE capabilities, Fusion 360 enables seamless collaboration and iteration throughout the design process. Its robust tools for parametric modeling, mesh editing, and generative design make it a go-to choice for additive manufacturing enthusiasts seeking versatility and integration.
|
||||
- SolidWorks: Renowned as an industry standard for mechanical design, SolidWorks specializes in providing powerful parametric modeling capabilities paired with intuitive user interfaces. Its extensive library of features and add-ons facilitates intricate part design and assembly, making it ideal for additive manufacturing applications requiring precision and complexity.
|
||||
- Tinkercad: Tinkercad stands out for its user-friendly, browser-based interface, catering to beginners and educators. Its intuitive drag-and-drop tools allow users to quickly create 3D models suitable for additive manufacturing projects, making it an excellent starting point for early enthusiasts and students exploring the world of 3D design.
|
||||
- Blender: While primarily recognized as a versatile 3D modeling and animation software, Blender's specialty lies in its robust toolset and open-source nature. Its powerful sculpting and mesh editing features enable users to create complex geometries and organic shapes suitable for various designing & AM processes, making it a compelling choice for artists and designers seeking creative freedom.
|
||||
|
||||
Let's take a moment to gather ourselves. We've explored the world of additive manufacturing, including its various processes, available materials, essential design principles, and popular CAD software tools. With this understanding, it's time to examine how you can effectively apply this knowledge as a designer/engineer. So, let's delve into the Design for Additive Manufacturing (DfAM) workflow.
|
||||
|
||||
#### Conceptualization and Ideation
|
||||
|
||||
|
||||
- ##### Define Objectives and Constraints:
|
||||
- - Clearly define the project's goals, including functional requirements, performance targets, and regulatory constraints.
|
||||
- Consider limitations imposed by the chosen additive manufacturing process, such as minimum feature size, build volume, and material compatibility.
|
||||
- ##### Generate and Explore Ideas:
|
||||
- - Conduct brainstorming sessions, sketching exercises, and idea-generation workshops to explore various design possibilities.
|
||||
- Encourage cross-disciplinary collaboration and input from stakeholders to ensure diverse perspectives are considered.
|
||||
- ##### Concept Development and Selection:
|
||||
- - Refine initial concepts based on feasibility, novelty, and alignment with project objectives.
|
||||
- Evaluate and prioritize concepts using technical feasibility, market demand, and potential impact criteria.
|
||||
|
||||
#### CAD Modeling
|
||||
|
||||
|
||||
- ##### Create Detailed 3D Models:
|
||||
- - Utilize CAD software to develop detailed digital models of the intended product or part, considering geometry, dimensions, tolerances, and material properties.
|
||||
- Incorporate features such as fillets, chamfers, and draft angles to improve manufacturability and part quality.
|
||||
- ##### Optimize Designs for Additive Manufacturing:
|
||||
- - Explore design freedom offered by additive manufacturing, including lattice structures, topology optimization, and organic shapes.
|
||||
- Consider design considerations specific to additive manufacturing processes, such as support structures, build orientation, and layer thickness.
|
||||
- Leverage parametric modeling techniques to explore design variations and optimize for performance, cost, and time-to-market.
|
||||
|
||||
#### Simulation and Analysis
|
||||
|
||||
|
||||
- ##### Virtual Testing and Analysis:
|
||||
- - Utilize simulation software to predict and evaluate the behavior of designs under various operating conditions.
|
||||
- Perform structural analysis, thermal simulations, and fluid flow simulations to identify potential performance issues and optimize designs.
|
||||
- ##### Evaluate Manufacturability:
|
||||
- - Assess the manufacturability of designs by simulating the additive manufacturing process in slicing software, which includes build orientation, support structures, and material deposition.
|
||||
- Identify potential issues such as warping, residual stresses, and poor surface finish, and iterate on designs to address them.
|
||||
|
||||
#### Design Optimization
|
||||
|
||||
|
||||
- ##### Iterative Refinement:
|
||||
- - Iterate designs based on simulation results, mock-up feedback, and stakeholder input to address identified issues and optimize performance.
|
||||
- Balance trade-offs between design complexity, part quality, and manufacturing efficiency to achieve the desired outcomes.
|
||||
- ##### Utilize Advanced Optimization Techniques:
|
||||
- - Leverage topology optimization, generative design, and machine learning algorithms to explore design spaces and identify optimal solutions.
|
||||
- Consider multi-objective optimization approaches to simultaneously optimize for conflicting objectives such as weight reduction, stiffness, and cost.
|
||||
- ##### Validate Design Changes:
|
||||
- - Validate design changes through re-simulation and testing to ensure that proposed modifications achieve the desired improvements without introducing new issues.
|
||||
|
||||
#### Prototyping and Testing
|
||||
|
||||
|
||||
- ##### Select Appropriate Additive Manufacturing Method and Materials:
|
||||
- - Choose the most suitable additive manufacturing process based on factors such as part complexity, material properties, surface finish requirements, and production volume. Which additive manufacturing method is right for you? Click here to know.
|
||||
- ##### Fabricate Prototypes:
|
||||
- - Utilize the selected additive manufacturing method to fabricate physical prototypes with accuracy and fidelity to the digital design.
|
||||
- Ensure that the manufacturing parameters, like layer thickness, build orientation, and material selection, are optimized to achieve the desired part quality and performance
|
||||
- ##### Conduct Rigorous Testing:
|
||||
- - Perform comprehensive testing and validation of the prototypes to assess their functional performance, durability, and reliability under real-world conditions.
|
||||
- Use a combination of mechanical testing, environmental testing, and functional testing to evaluate the prototypes' suitability for their intended application.
|
||||
|
||||
#### Final Design Adjustments
|
||||
|
||||
|
||||
- ##### Incorporate Feedback and Lessons Learned:
|
||||
- - Incorporate feedback from prototyping, testing, and stakeholder reviews into final design adjustments.
|
||||
- Address any remaining issues or concerns identified during the development process to ensure the final design meets all requirements and expectations.
|
||||
- ##### Document Design Changes:
|
||||
- - Utilize the selected additive manufacturing method to fabricate physical prototypes with accuracy and fidelity to the digital design.
|
||||
- Ensure that the manufacturing parameters, like layer thickness, build orientation, and material selection, are optimized to achieve the desired part quality and performance
|
||||
- ##### Document Design Changes:
|
||||
- - Document all design changes, revisions, and decisions made throughout the development process to maintain traceability and accountability.
|
||||
- Create detailed design documentation, including engineering drawings, specifications, and Bill of Materials (BOM), to guide manufacturing and assembly processes.
|
||||
- ##### Document Design Changes:
|
||||
- - Finalize the design for production, ensuring that all necessary preparations are made for manufacturing, assembly, and quality control.
|
||||
- Coordinate with manufacturing partners and suppliers to transfer the design into production and ensure a smooth transition from development to deployment.
|
||||
|
||||
#### Final Production through Additive Manufacturing (Optional Step Based on Application of the Design)
|
||||
|
||||
- ##### Scale-Up for Production:
|
||||
- - Transition the optimized design from prototyping to full-scale production using additive manufacturing technologies.
|
||||
- Scale production volumes by optimizing manufacturing processes, streamlining workflows, and maximizing machine utilization.
|
||||
- ##### Manufacturing Process Optimization:
|
||||
- - Fine-tune manufacturing parameters, such as build speed, layer thickness, and material handling, to optimize production efficiency and part quality.
|
||||
- Implement continuous improvement initiatives to identify and address bottlenecks, minimize waste, and enhance productivity throughout the manufacturing process.
|
||||
- ##### Quality Assurance and Control:
|
||||
- - Establish rigorous quality assurance and control measures to ensure manufactured parts' consistency, reliability, and repeatability.
|
||||
- Implement inspection protocols, quality control checks, and validation procedures to verify compliance with design specifications and regulatory requirements.
|
||||
- ##### Supply Chain Integration:
|
||||
- - Integrate additive manufacturing into the broader supply chain ecosystem by collaborating with suppliers, manufacturers, and logistics partners.
|
||||
- Explore opportunities for on-demand manufacturing, distributed production, and agile supply chain strategies to meet evolving market demands and customer requirements.
|
||||
- ##### Post-Processing and Finishing:
|
||||
- - Implement post-processing techniques, such as surface finishing, heat treatment, Painting, and machining, to enhance manufactured parts' aesthetics, functionality, and performance.
|
||||
- Develop standardized post-processing workflows and procedures to ensure consistency and quality across production batches.
|
||||
|
||||
In summary, the Design for Additive Manufacturing (DfAM) workflow provides a structured framework for designers to create innovative, efficient, and manufacturable designs. By following a systematic approach encompassing conceptualization, CAD modeling, simulation, optimization, prototyping, final adjustments, and final production, designers can harness the full potential of additive manufacturing technologies.
|
||||
|
||||
### FDM Design Tips
|
||||
|
||||
- Minimize Overhangs: Keep overhangs below 45 degrees to reduce the need for support.
|
||||
- Consider Layer Orientation: Align layers to maximize strength along the load-bearing direction.
|
||||
- Ensure Adequate Wall Thickness: Use 1-2 mm thick walls for structural integrity.
|
||||
- Add Filets to Corners: Reduce stress concentrations by rounding corners.
|
||||
- Use Chamfers: Replace sharp edges with chamfers to improve print quality and reduce support needs.
|
||||
|
||||
### SLA Design Tips
|
||||
|
||||
- Thin Walls and Fine Details: Keep overhangs below 45 degrees to reduce the need for support.
|
||||
- Include Drainage Holes: Align layers to maximize strength along the load-bearing direction.
|
||||
- Minimize Supports: Use 1-2 mm thick walls for structural integrity.
|
||||
- Avoid Large Flat Surfaces: Reduce stress concentrations by rounding corners.
|
||||
- Prepare for Post-Processing: Replace sharp edges with chamfers to improve print quality and reduce support needs.
|
||||
|
||||
### SLS Design Tips
|
||||
|
||||
- Maintain Minimum Wall Thickness: Use 1-1.5 mm for adequate strength.
|
||||
- Add Escape Holes: Include 2 mm holes for powder removal in cavities.
|
||||
- Design for Moving Parts: Allow 0.5 mm clearance for interlocking parts.
|
||||
- Leverage Surface Texture: Utilize the rough texture for functional or aesthetic purposes.
|
||||
|
||||
### DMLS Design Tips
|
||||
|
||||
- Optimize for Support Removal: Design with easy access for removing supports.
|
||||
- Maintain Consistent Wall Thickness: Use uniform wall thickness to prevent thermal stress.
|
||||
- Include Filets and Chamfers: Reduce sharp edges to minimize stress concentrations.
|
||||
- Plan for Post-Processing: Design for ease of surface finishing and heat treatment.
|
||||
|
||||
### MJF Design Tips
|
||||
|
||||
- Uniform Wall Thickness: Aim for 1-2 mm to prevent warping and ensure strength.
|
||||
- Clearance for Moving Parts: Ensure at least 0.5 mm clearance for articulated parts.
|
||||
- Utilize Escape Holes: Design with holes for powder removal in internal cavities.
|
||||
- Minimize Supports: Use MJF's minimal support requirement by designing self-supporting features.
|
||||
|
||||
For a tabulated summary of the design rules for different 3D printing technologies, refer to the chart below.
|
||||
|
||||
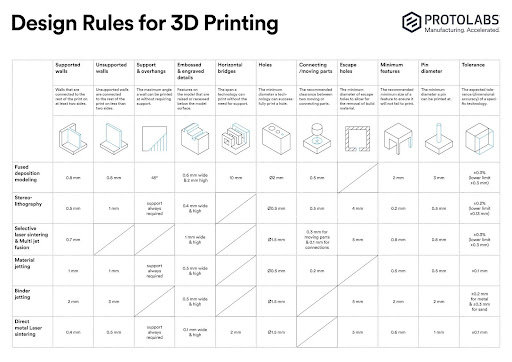
|
||||
|
||||
## Case Studies and Examples
|
||||
|
||||
### Successful Design Projects
|
||||
|
||||
#### General Electric (GE) - Jet Engine Fuel Nozzles
|
||||
|
||||
- Project Overview: General Electric utilized additive manufacturing to redesign the fuel nozzles for their LEAP jet engines. Traditional manufacturing methods required 20 separate parts to be assembled into a single nozzle.
|
||||
- For the design for additive manufacturing (DFAM), GE engineers consolidated the design into a single piece using direct metal laser sintering (DMLS). This significantly reduced the nozzle's complexity and weight while enhancing its durability and performance.
|
||||
- Outcome: The new fuel nozzle design reduced weight by 25% and offered five times the durability of traditionally manufactured nozzles. Integrating multiple components into one streamlined piece also reduced potential points of failure.
|
||||
|
||||
#### Adidas - Futurecraft 4D Shoes
|
||||
|
||||
- Project Overview: Adidas collaborated with Carbon, a leading 3D printing company, to produce the midsole for their Futurecraft 4D shoes. The goal was to create a high-performance shoe with customizable features tailored to individual athletes.
|
||||
- For the design for additive manufacturing (DFAM): Using Digital Light Synthesis (DLS), Adidas created intricate lattice structures in the midsole, optimizing the balance between cushioning and support.
|
||||
- Outcome: The Futurecraft 4D shoes offered enhanced performance and comfort, with the ability to fine-tune the midsole's properties for specific athletic needs. The project demonstrated the potential of additive manufacturing to revolutionize the footwear industry with bespoke designs and rapid prototyping.
|
||||
|
||||
#### Airbus - A350 XWB Cabin Brackets
|
||||
|
||||
- Project Overview: Airbus implemented additive manufacturing to produce over 1,000 parts, including cabin brackets, for its A350 XWB aircraft. These components needed to be lightweight yet strong enough to meet strict aerospace standards.
|
||||
- For the design for additive manufacturing (DFAM): Airbus used Selective Laser Sintering (SLS) to manufacture the brackets from high-performance thermoplastics. This process allowed for complex geometries and weight-optimized designs that were not feasible with traditional manufacturing.
|
||||
- Outcome: Using additive manufacturing in the A350 XWB led to significant weight savings, improved fuel efficiency, and reduced manufacturing costs. This project's success has encouraged the broader adoption of additive manufacturing in the aerospace industry.
|
||||
|
||||
## Common Design Challenges and Solutions
|
||||
|
||||
#### Challenge: Warping in Fused Deposition Modeling (FDM)
|
||||
|
||||
**Solution:** To mitigate warping, designers can use features such as brims and rafts to improve bed adhesion and reduce thermal stress. Additionally, optimizing the part orientation and incorporating gradual transitions in geometry can minimize warping.
|
||||
|
||||
#### Challenge: Surface Finish in Stereolithography (SLA)
|
||||
|
||||
**Solution:** Post-processing techniques, such as sanding, chemical smoothing, and coating, can enhance the surface finish of SLA prints. Designers should also consider using higher resolution settings during printing to reduce the layer visibility.
|
||||
|
||||
#### Challenge: Support Structure Removal in Direct Metal Laser Sintering (DMLS)
|
||||
|
||||
**Solution:** Designing parts with self-supporting angles and minimizing overhangs can reduce the need for support structures. Using lattice structures and strategic support placements can facilitate easier removal and minimize material waste.
|
||||
|
||||
#### Challenge: Inconsistent Material Properties in Multi Jet Fusion (MJF)
|
||||
|
||||
**Solution:** Conduct thorough testing and validation to understand the material properties of MJF-produced parts. Implementing design adjustments, such as uniform wall thickness and consistent part orientation, can enhance material consistency.
|
||||
|
||||
The case studies and examples discussed above highlight the transformative potential of additive manufacturing across various industries. From aviation and footwear to complex aerospace components, Overcoming common design challenges through strategic solutions has demonstrated the feasibility and benefits of this technology.
|
||||
|
||||
## Future Trends in Additive Manufacturing Design
|
||||
|
||||
#### Advances in Materials
|
||||
|
||||
The development of new materials, including high-performance polymers, biocompatible resins, and advanced metal alloys, is expanding additive manufacturing applications. These materials offer improved mechanical properties, biocompatibility, and environmental resistance, opening new possibilities for healthcare, aerospace, and automotive industries.
|
||||
|
||||
#### Innovations in 3D Printing Technologies
|
||||
|
||||
The relentless progress in 3D printing technologies, such as multi-material printing and hybrid manufacturing, is not just enhancing the capabilities and efficiency of additive manufacturing, but also reshaping the very limits of design and manufacturing. These innovations are empowering the production of more intricate and functional parts, heralding a new era in the industry.
|
||||
|
||||
### Impact of AI and Machine Learning
|
||||
|
||||
Artificial intelligence (AI) and machine learning are revolutionizing additive manufacturing, providing powerful tools to enhance design and production processes.
|
||||
|
||||
#### Text-to-3D Generative Software
|
||||
|
||||
Text-to-3D generative software enables users to create 3D models from textual descriptions, significantly streamlining the design process. These tools use natural language processing (NLP) and generative algorithms to interpret textual input and generate accurate, detailed 3D models. This approach simplifies rapid prototyping, allows for extensive customization, and makes 3D design more accessible.
|
||||
|
||||
**Example: Meshy.ai:** Meshy.ai is a leading example of text-to-3D generative software. It allows users to input descriptions, such as "ergonomic office chair," and instantly produces detailed 3D models that can be refined and printed. This tool reduces the time and expertise required for initial model creation, making it a valuable resource for designers and manufacturers.
|
||||
|
||||
#### Generative Design
|
||||
|
||||
Generative design utilizes AI to create multiple options based on specified parameters and constraints, such as material type, weight, and strength. This process involves using algorithms to explore and optimize designs, often producing innovative solutions that human designers might not conceive. Generative design enhances the creation of complex geometries, optimizes performance, and promotes sustainability by reducing material waste.
|
||||
|
||||
**Example: Autodesk Fusion 360:** Autodesk Fusion 360 is a prominent generative design tool. Engineers can input design goals and constraints into the software, generating numerous design iterations that meet these criteria. This allows for selecting the most optimal solution, streamlining the design process, and enhancing efficiency.
|
||||
|
||||
## Conclusion
|
||||
|
||||
Designing for additive manufacturing (AM) isn't just a new approach, it's a transformative one. It opens up possibilities for creating complex, customized, and efficient products that were once unimaginable.
|
||||
|
||||
By understanding various AM processes and materials, designers can fully leverage AM's unique advantages, sparking a new era of design and manufacturing. This guide has covered essential design principles, key considerations, and a comprehensive workflow for AM. AM's benefits, such as customization, complex geometries, reduced material waste, faster prototyping, and cost-effective production, highlight its potential to revolutionize manufacturing.
|
||||
|
||||
As a leading 3D printing partner, [iamrapid.com](https://iamrapid.com/) offers online 3D printing services with an instant quotation system, providing transparent quotes within seconds. At [iamrapid.com](https://iamrapid.com/), you don't just get instant quotations; our advanced quotation software also performs model analysis, including wall thickness analysis, orientation optimization, and repairing parts for optimal printing.
|
||||
|
||||
Moreover, [iamrapid.com](https://iamrapid.com/) excels in complete product design development services, handling the entire design process from ideation to final production-ready design. For further assistance, iamrapid.com is here to support you every step of the way, ensuring your additive manufacturing journey is smooth and successful.
|
||||
|
||||
In summary, designing for additive manufacturing (AM) is a dynamic field with significant opportunities for innovation and efficiency. By following the principles and best practices outlined in this guide, designers can harness AM's full potential to create groundbreaking products.
|
||||
File diff suppressed because it is too large
Load Diff
File diff suppressed because it is too large
Load Diff
File diff suppressed because one or more lines are too long
Reference in New Issue
Block a user